Solutions · family
Engineering
Contract manufacturing: frames, weldments, conveyors, staircases and platforms to EN 1090 EXC2.
- EN 1090-1 EXC2
- laser to 20 mm
- machining to 6.2 m / 16 t
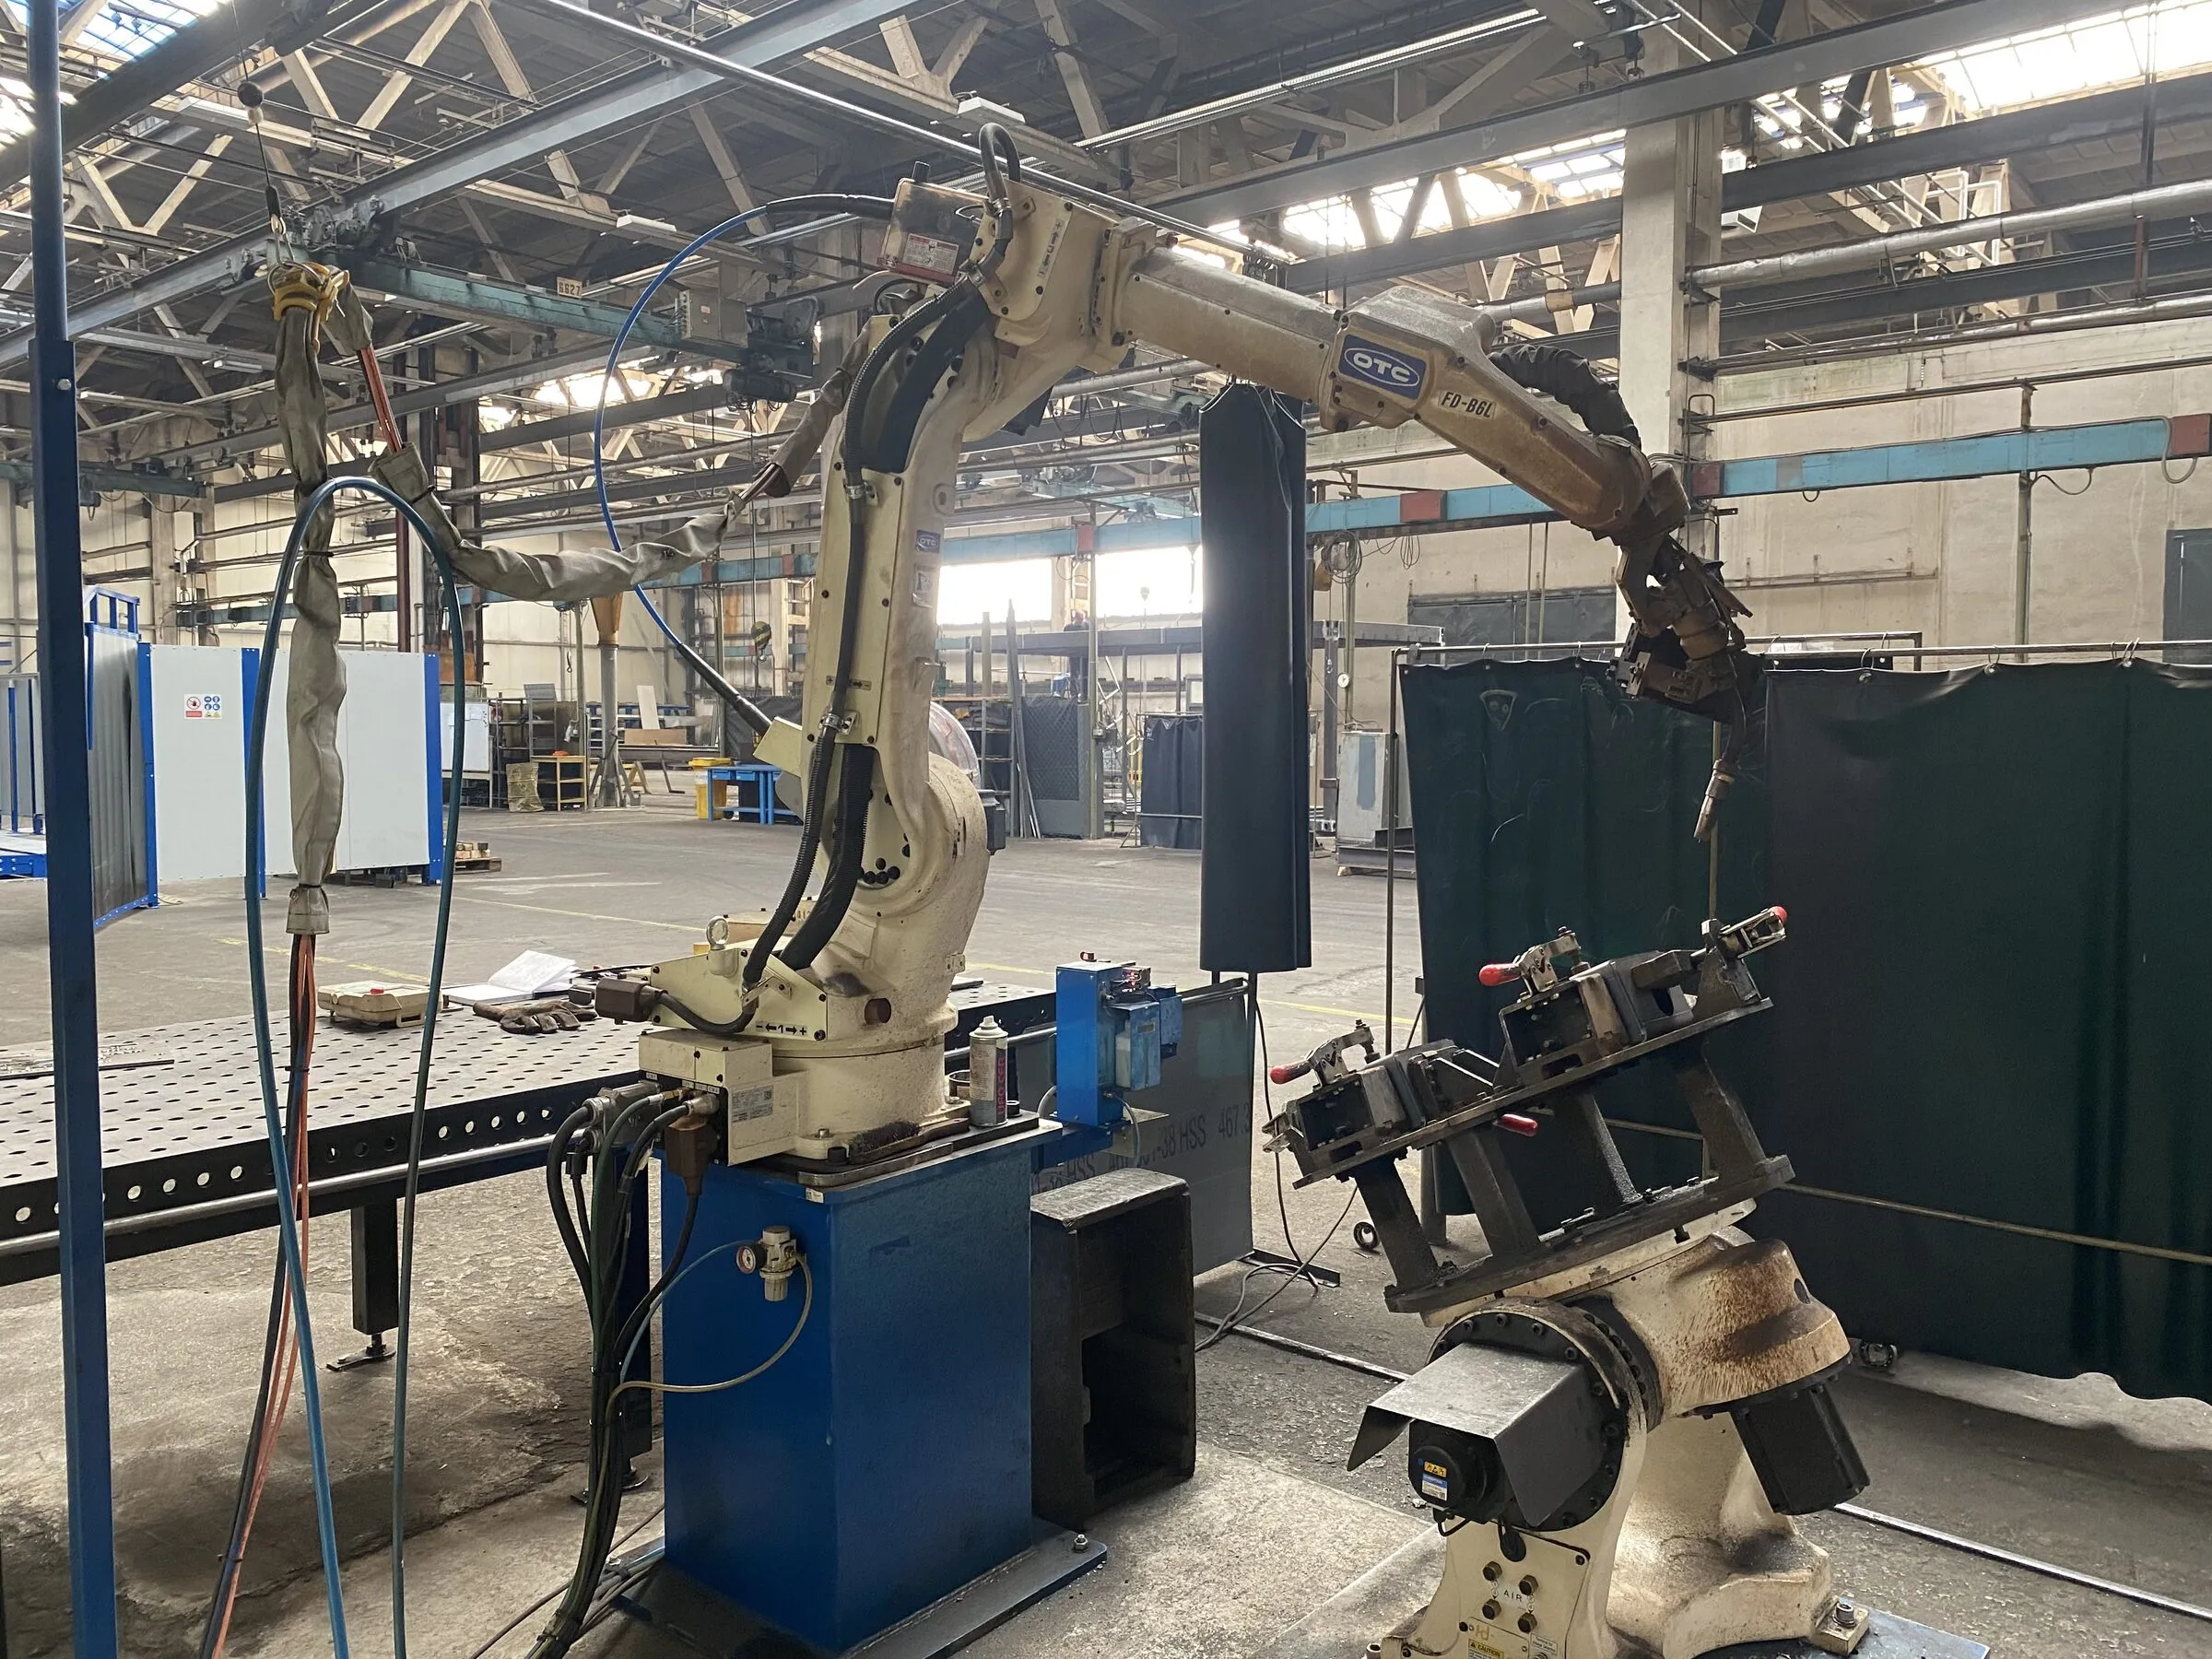
- robotic welding on a 14 m track
Robotic welding cell on its track, production hall
Before Tanax made containers it made steel for other people's machines, and it still does. Conveyor frames, machine bases, chassis and subframes, brackets, welded assemblies, staircases, platforms and racking, designed for manufacturability, welded to EN ISO 3834-2, machined, blasted, painted and delivered. Around a third of the factory's hours go to European machinery OEMs on repeat frame agreements.
Specification
Site
- Production area
- 31,486 m²
- Headcount
- ~80
- Engineering tradition
- machine building on this site since 1951
Cutting
- Laser
- 2,000 × 4,000 mm, 3.2 kW, to 20 mm
- Plasma
- 3-15 mm, 4,000 × 1,500 mm
- Shears
- to 25 mm × 3,150 mm
- Sawing
- frame, band and circular to Ø400 mm
Forming
- Press brake
- 400 t, 6,050 mm table
- Plate bending
- CNC to 20 mm × 4,000 mm
Welding
- Robotic
- 2 × 6-axis on a 14 m track, plus a 6-axis cell, R = 2,008 mm
- Qualification
- EN ISO 3834-2, welders to EN ISO 9606, structures to EN 1090-1 EXC2
Machining
- Horizontal boring, large
- 6,200 × 3,000 × 1,600 mm, rotary 1,800 × 2,500 mm, 16,000 kg, Ø160 mm
- Horizontal boring, second
- 3,500 × 2,500 × 1,600 mm, 12,000 kg, Ø130 mm
- Boring / milling
- 8,000 × 3,000 × 1,500 mm
- CNC turning
- Ø550 mm over bed, Ø350 over cross slide, 1,590 mm
- Rotary table CNC
- chuck Ø800 mm, workpiece to Ø1,100 mm, 765 mm high, 2,500 kg
- Gear cutting
- wheel to Ø600 mm, module 2-13, 5-120 teeth, face width to 110 mm
- Grinding
- cylindrical to Ø400 × 2,000 mm; surface 200 × 1,200 mm
- Planing / slotting
- to 1,200 × 5,000 mm; grooves to 15 mm × 120 mm
Finishing
- Shot blasting
- 8,000 × 5,000 × 3,000 mm to Sa 2.5, rail-linked to paint
- Paint
- 7,900 × 5,000 × 4,890 mm booth, drying 75-80 °C
Inspection
- 3D
- 6-axis measuring arm
How it is built
The decisions behind the numbers
Design for manufacture is part of the quote.
Tanax's engineers review a part for how it will actually be cut, formed, jigged and welded, and propose changes that take cost out without changing function. On repeat parts that also means designing and building the welding jigs, which is what makes a hand-welded assembly repeatable.
Robotic welding is applied where it pays, and only there.
The candidate list is built from the products themselves: parts common to more than one product, and parts with intermittent welds. On a recent programme fourteen parts were shortlisted from two OEM product families and the first four weldments went to fixture design. That is the method: map the parts, then build the fixtures.
Blast and paint are on the same rail.
The blasting chamber and the paint booth are rail-connected, so a large weldment moves from Sa 2.5 straight to primer without a re-handle and without flash rust between the two.
One roof, one owner of the tolerance stack.
Cut, form, weld, machine, blast, paint, measure and pack in one building means one supplier owns the tolerance stack instead of four suppliers blaming each other.
Configurations
What gets built here

Belt conveyor frame in the production hall Conveyor systems and frames
- belt conveyor frames, discharge and collecting conveyors
- galvanised, assembled
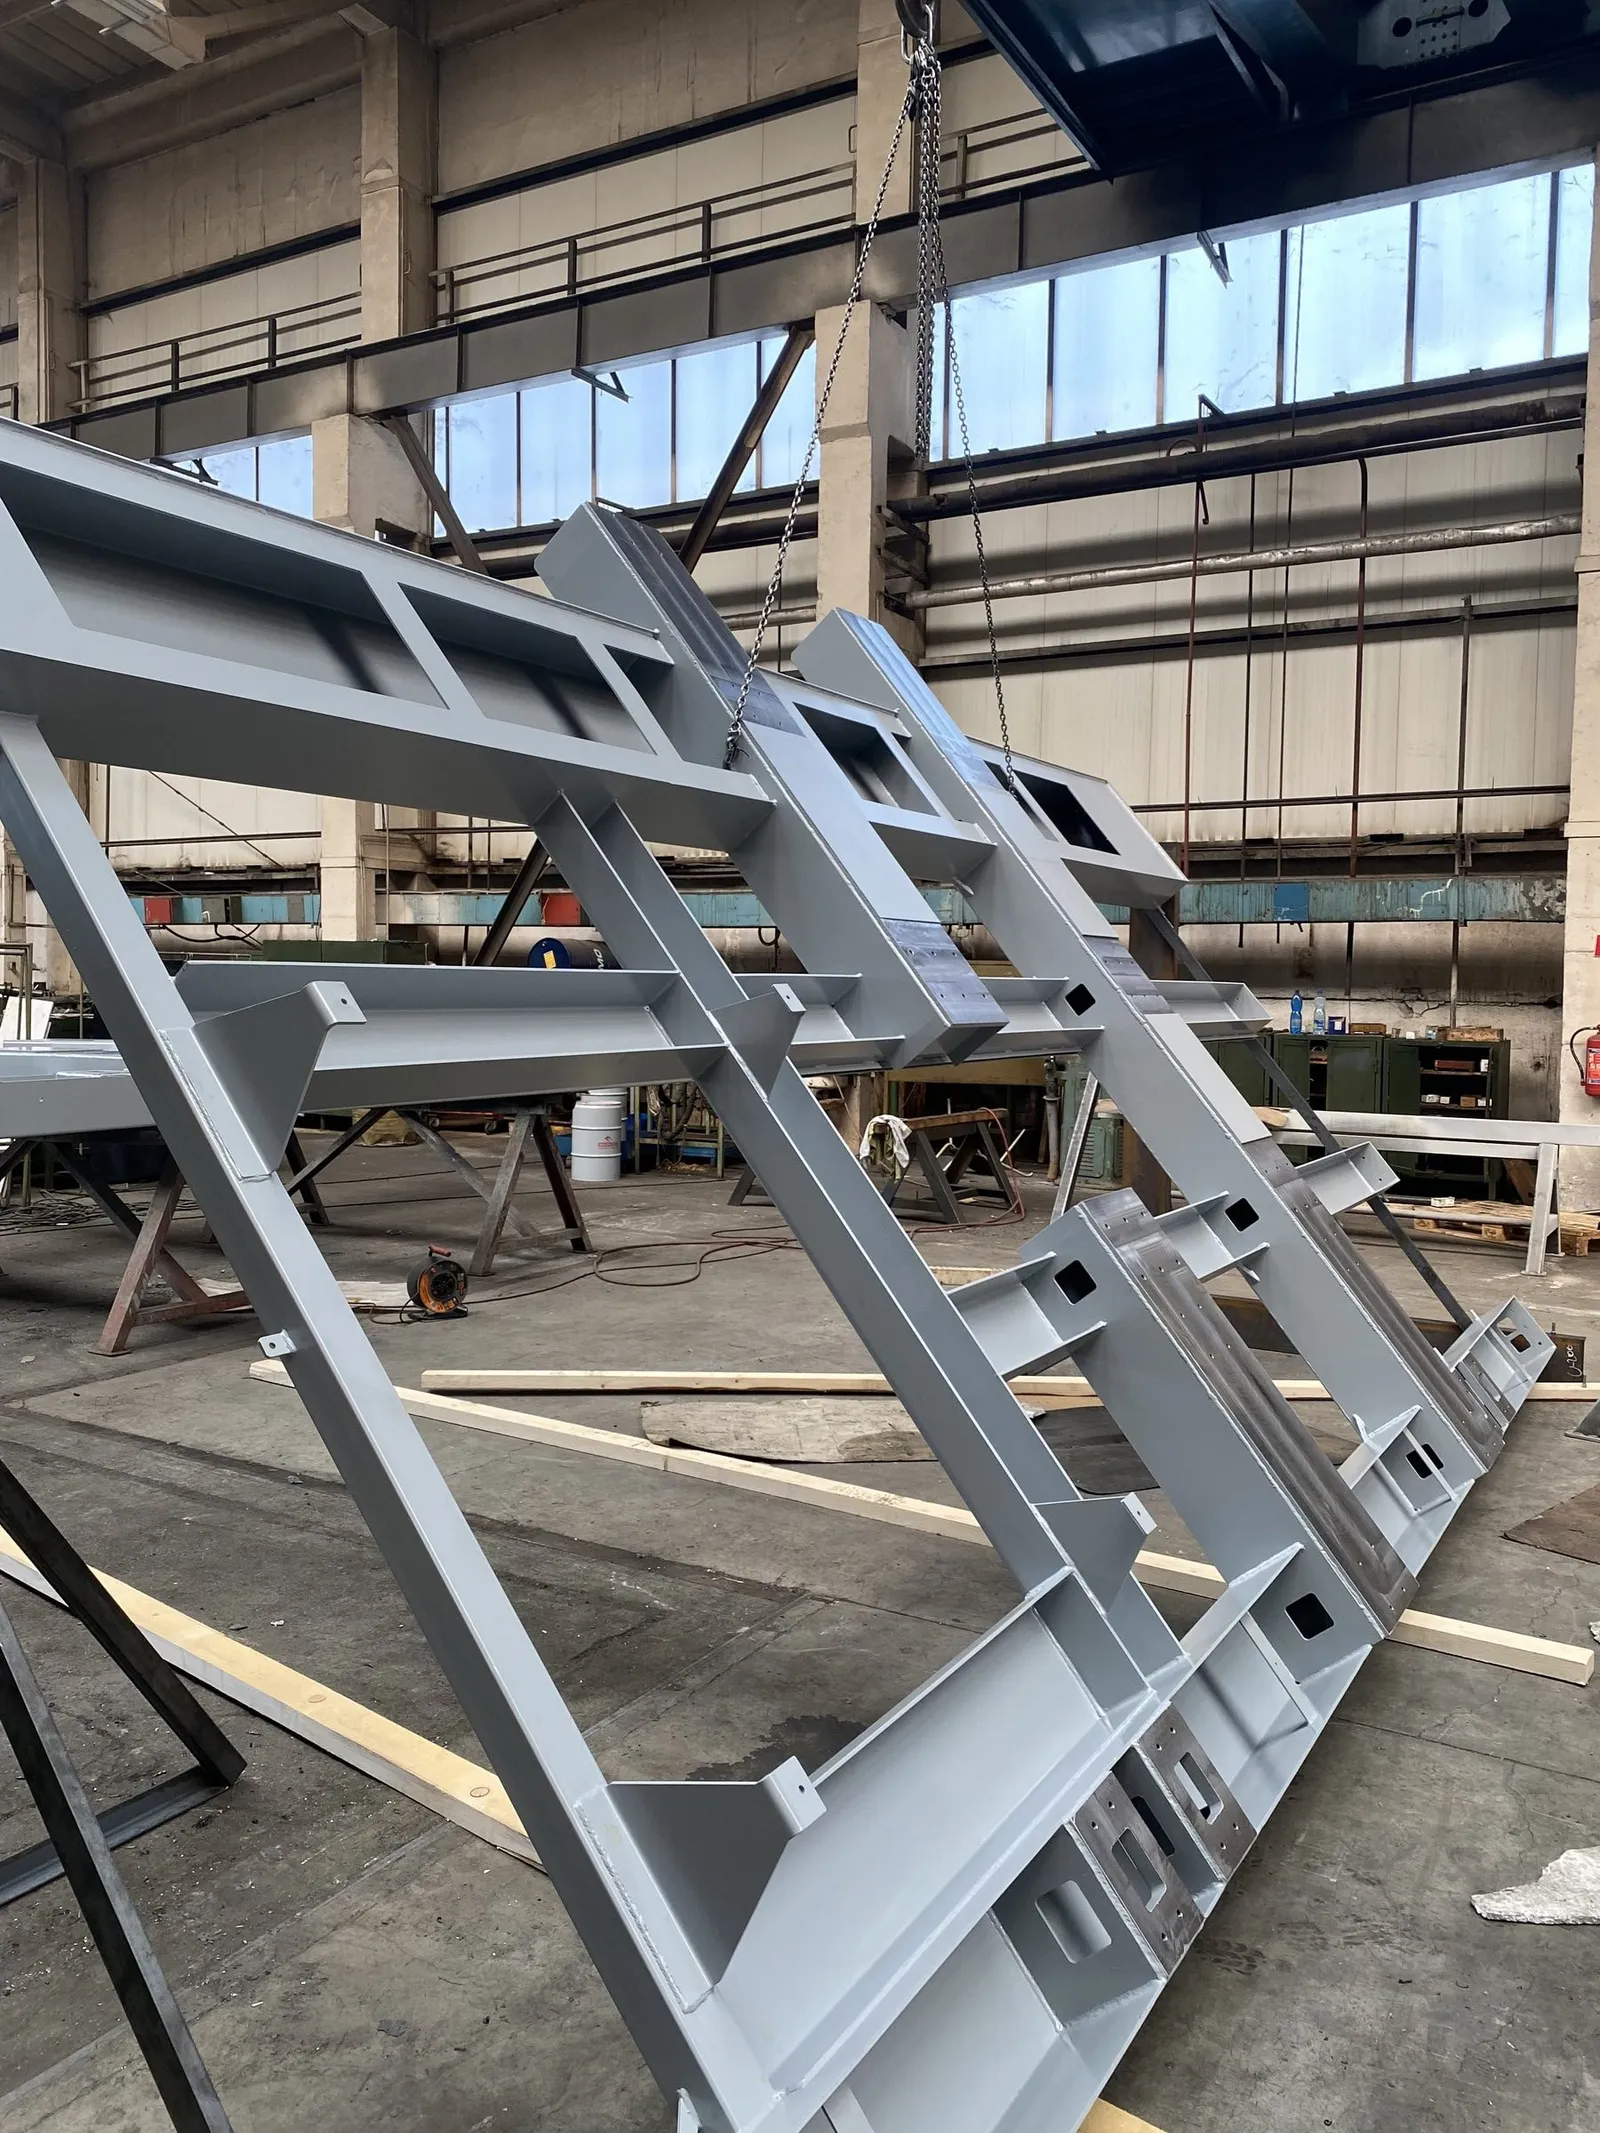
Welded machine frame in the production hall Machine frames and bases
- precision machine frames, welded and machined to final tolerance
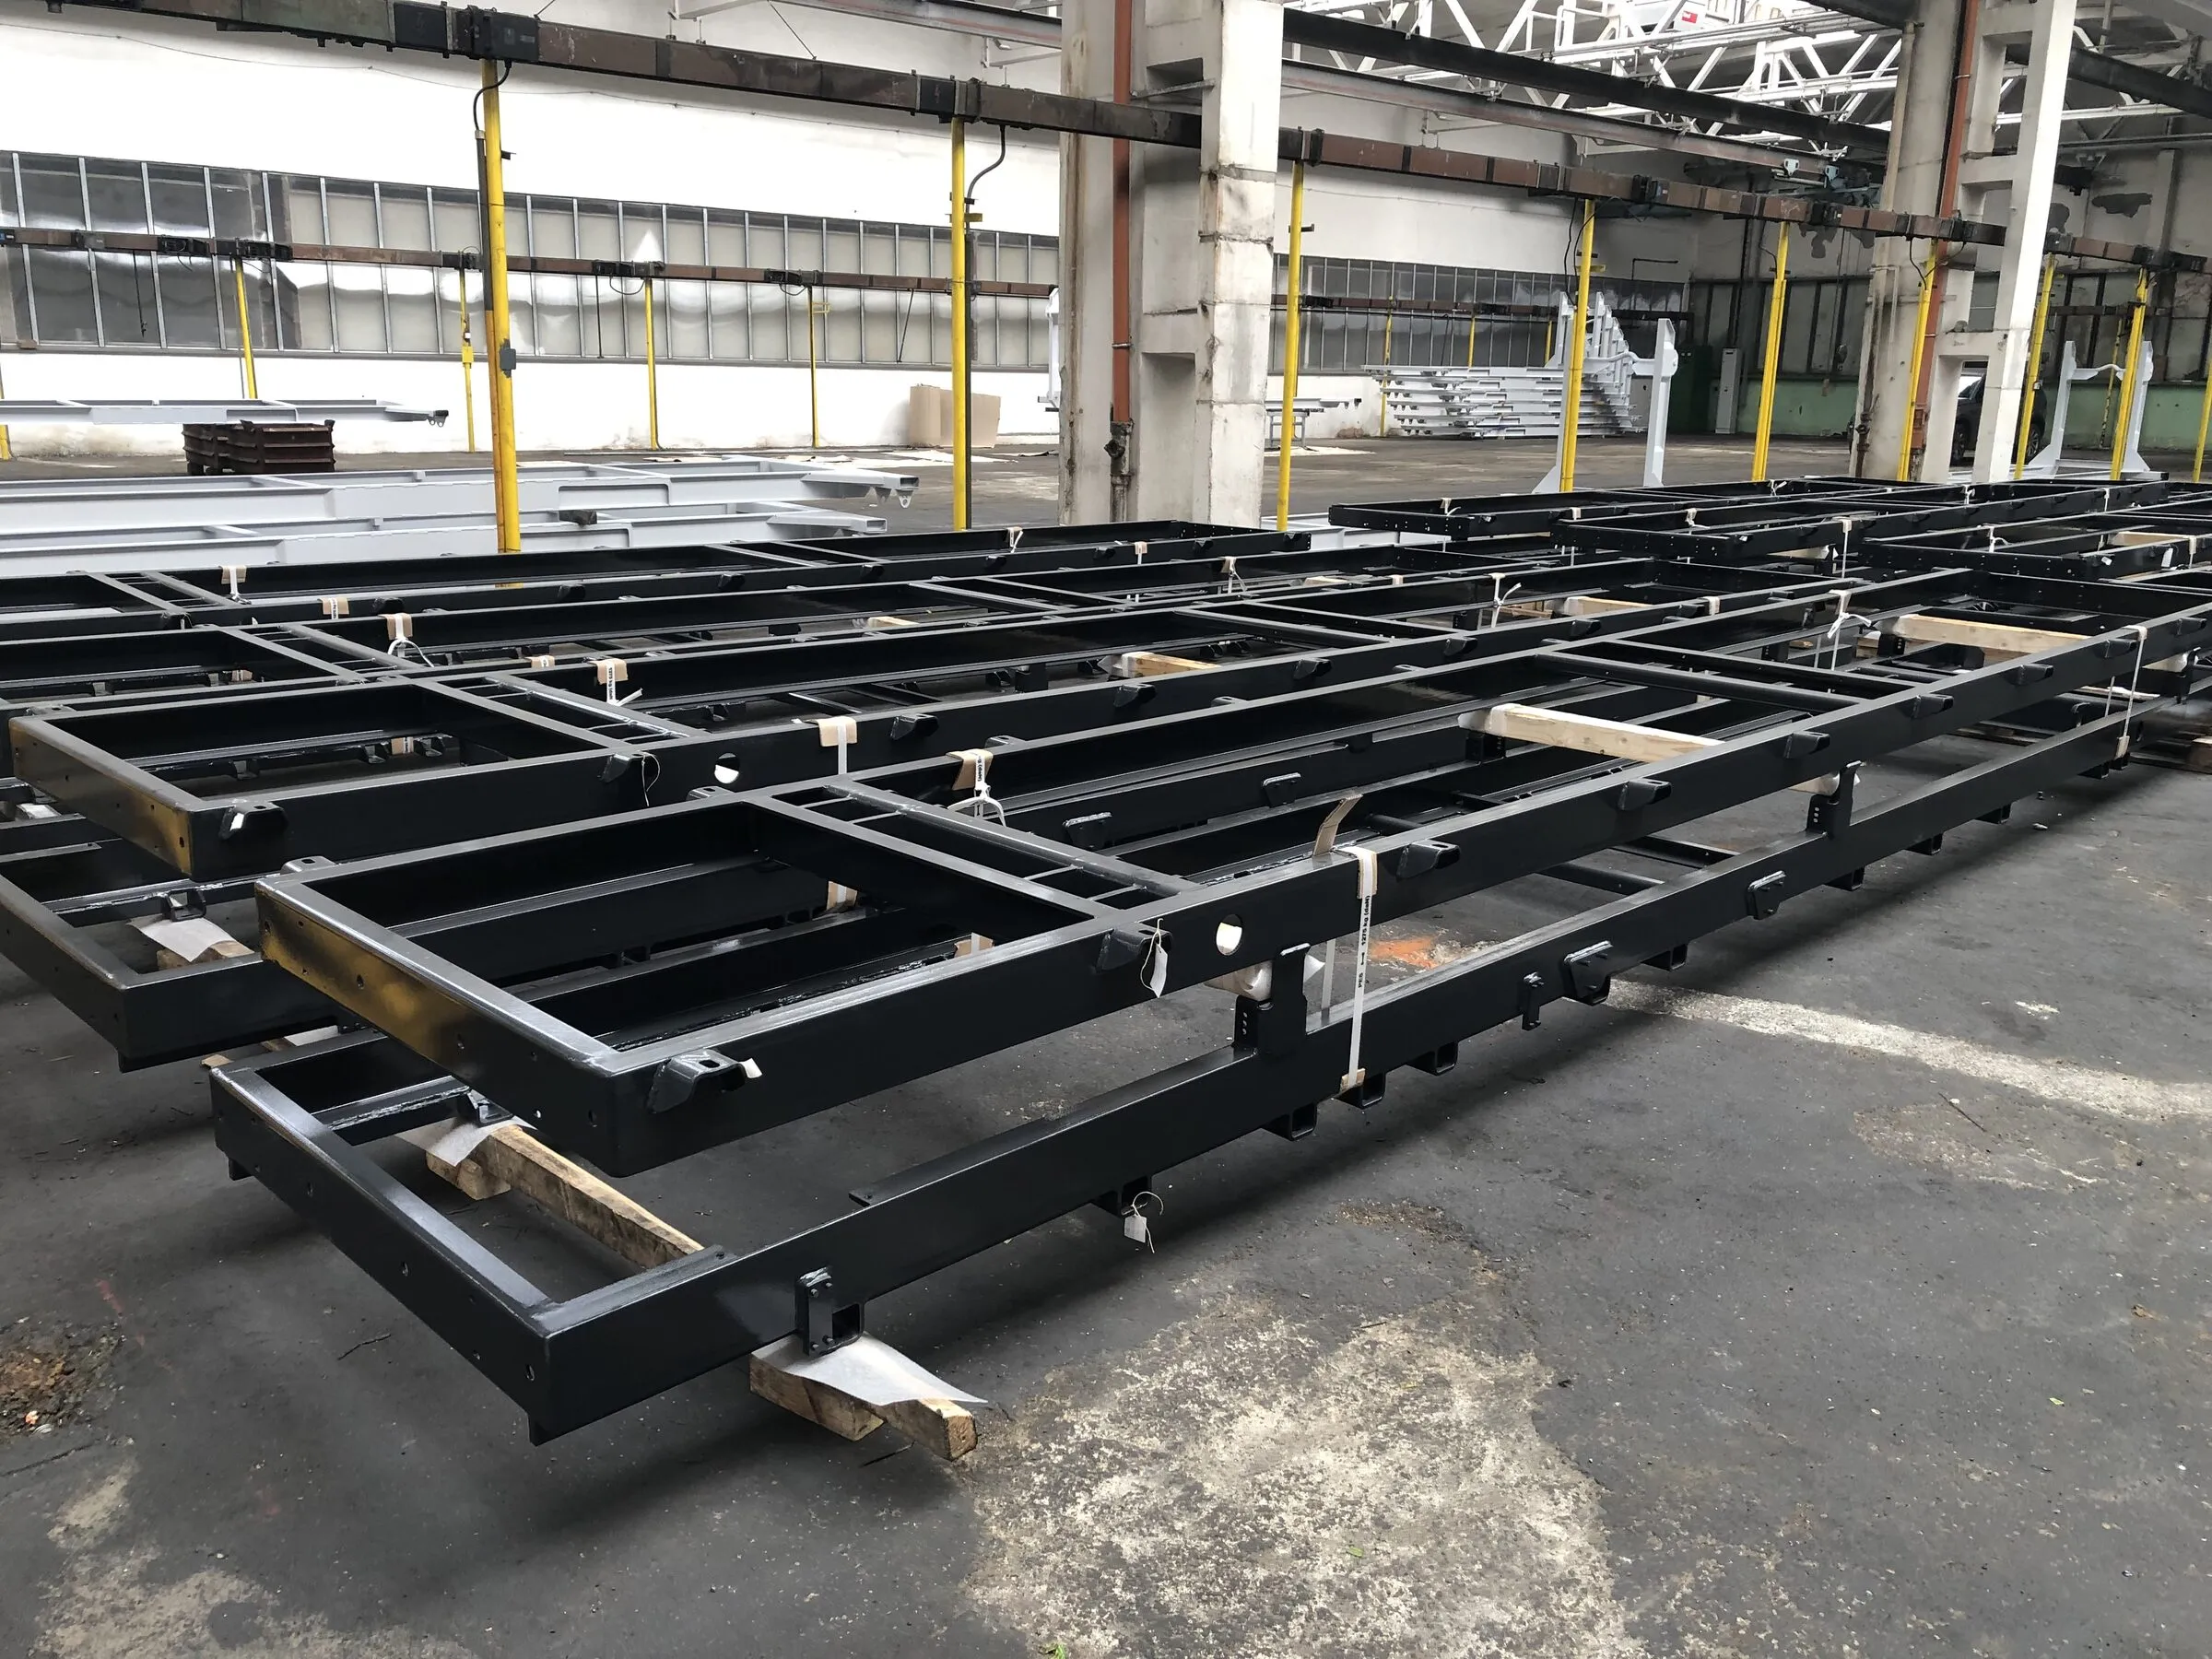
Loader chassis under fabrication Chassis and subframes
- loader chassis, vehicle subframes, brackets, mounting structures
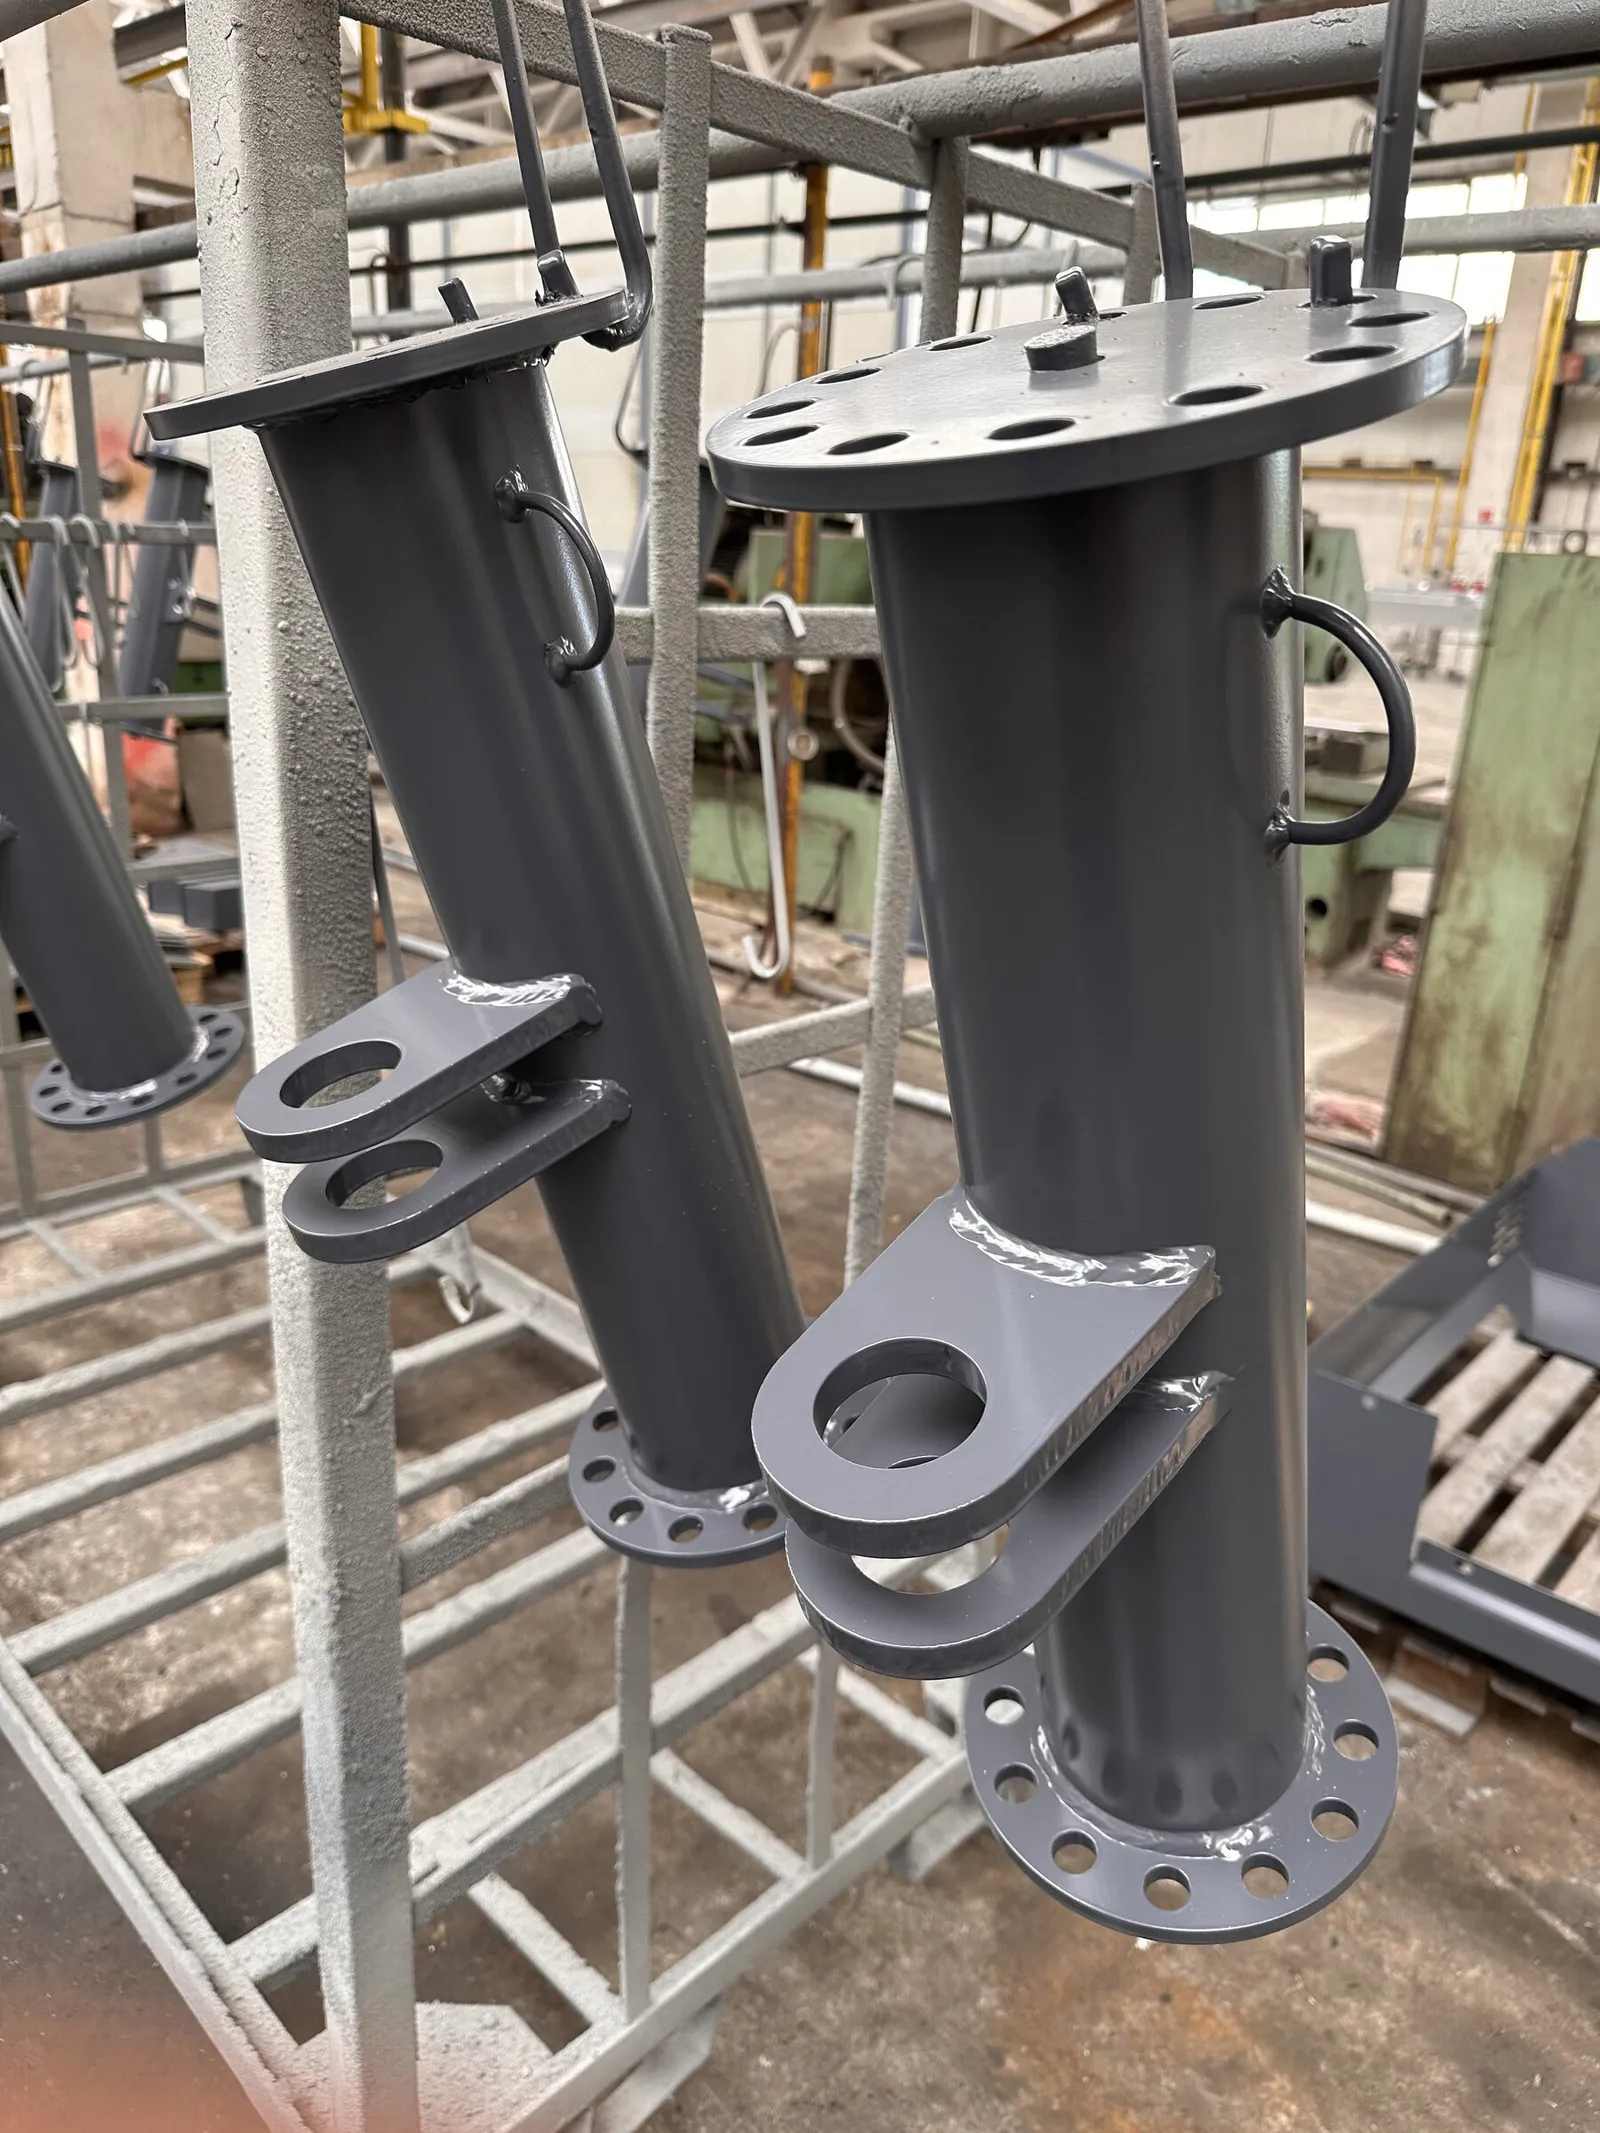
Machined pipe weldments with flanges Welded assemblies
- medium and heavy weldments to EXC2
- robotic and manual
- No photograph yet
Staircases, platforms, walkways
- EN 1090 EXC2
- galvanised or painted
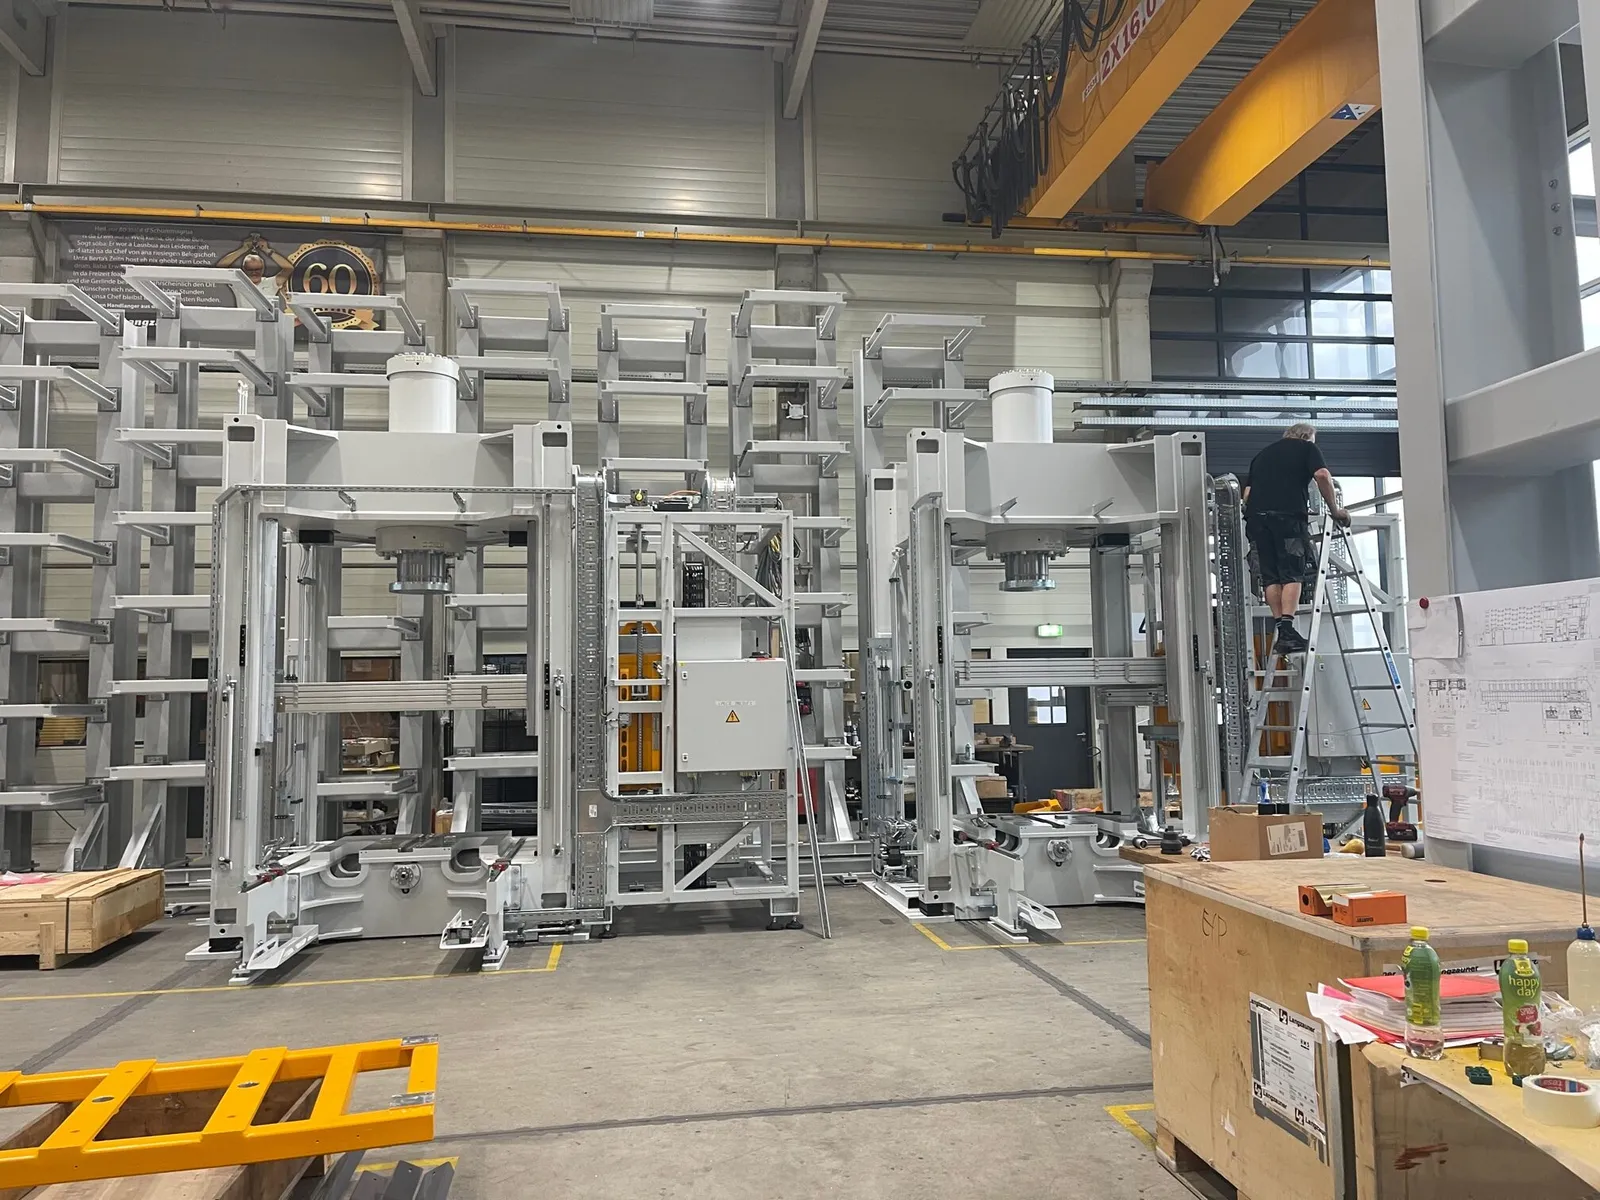
Racking structure in the production hall Racking and storage structures
- specialised racking systems
- No photograph yet
Silos and hoppers
- galvanised steel, assembled
- prototype and serial
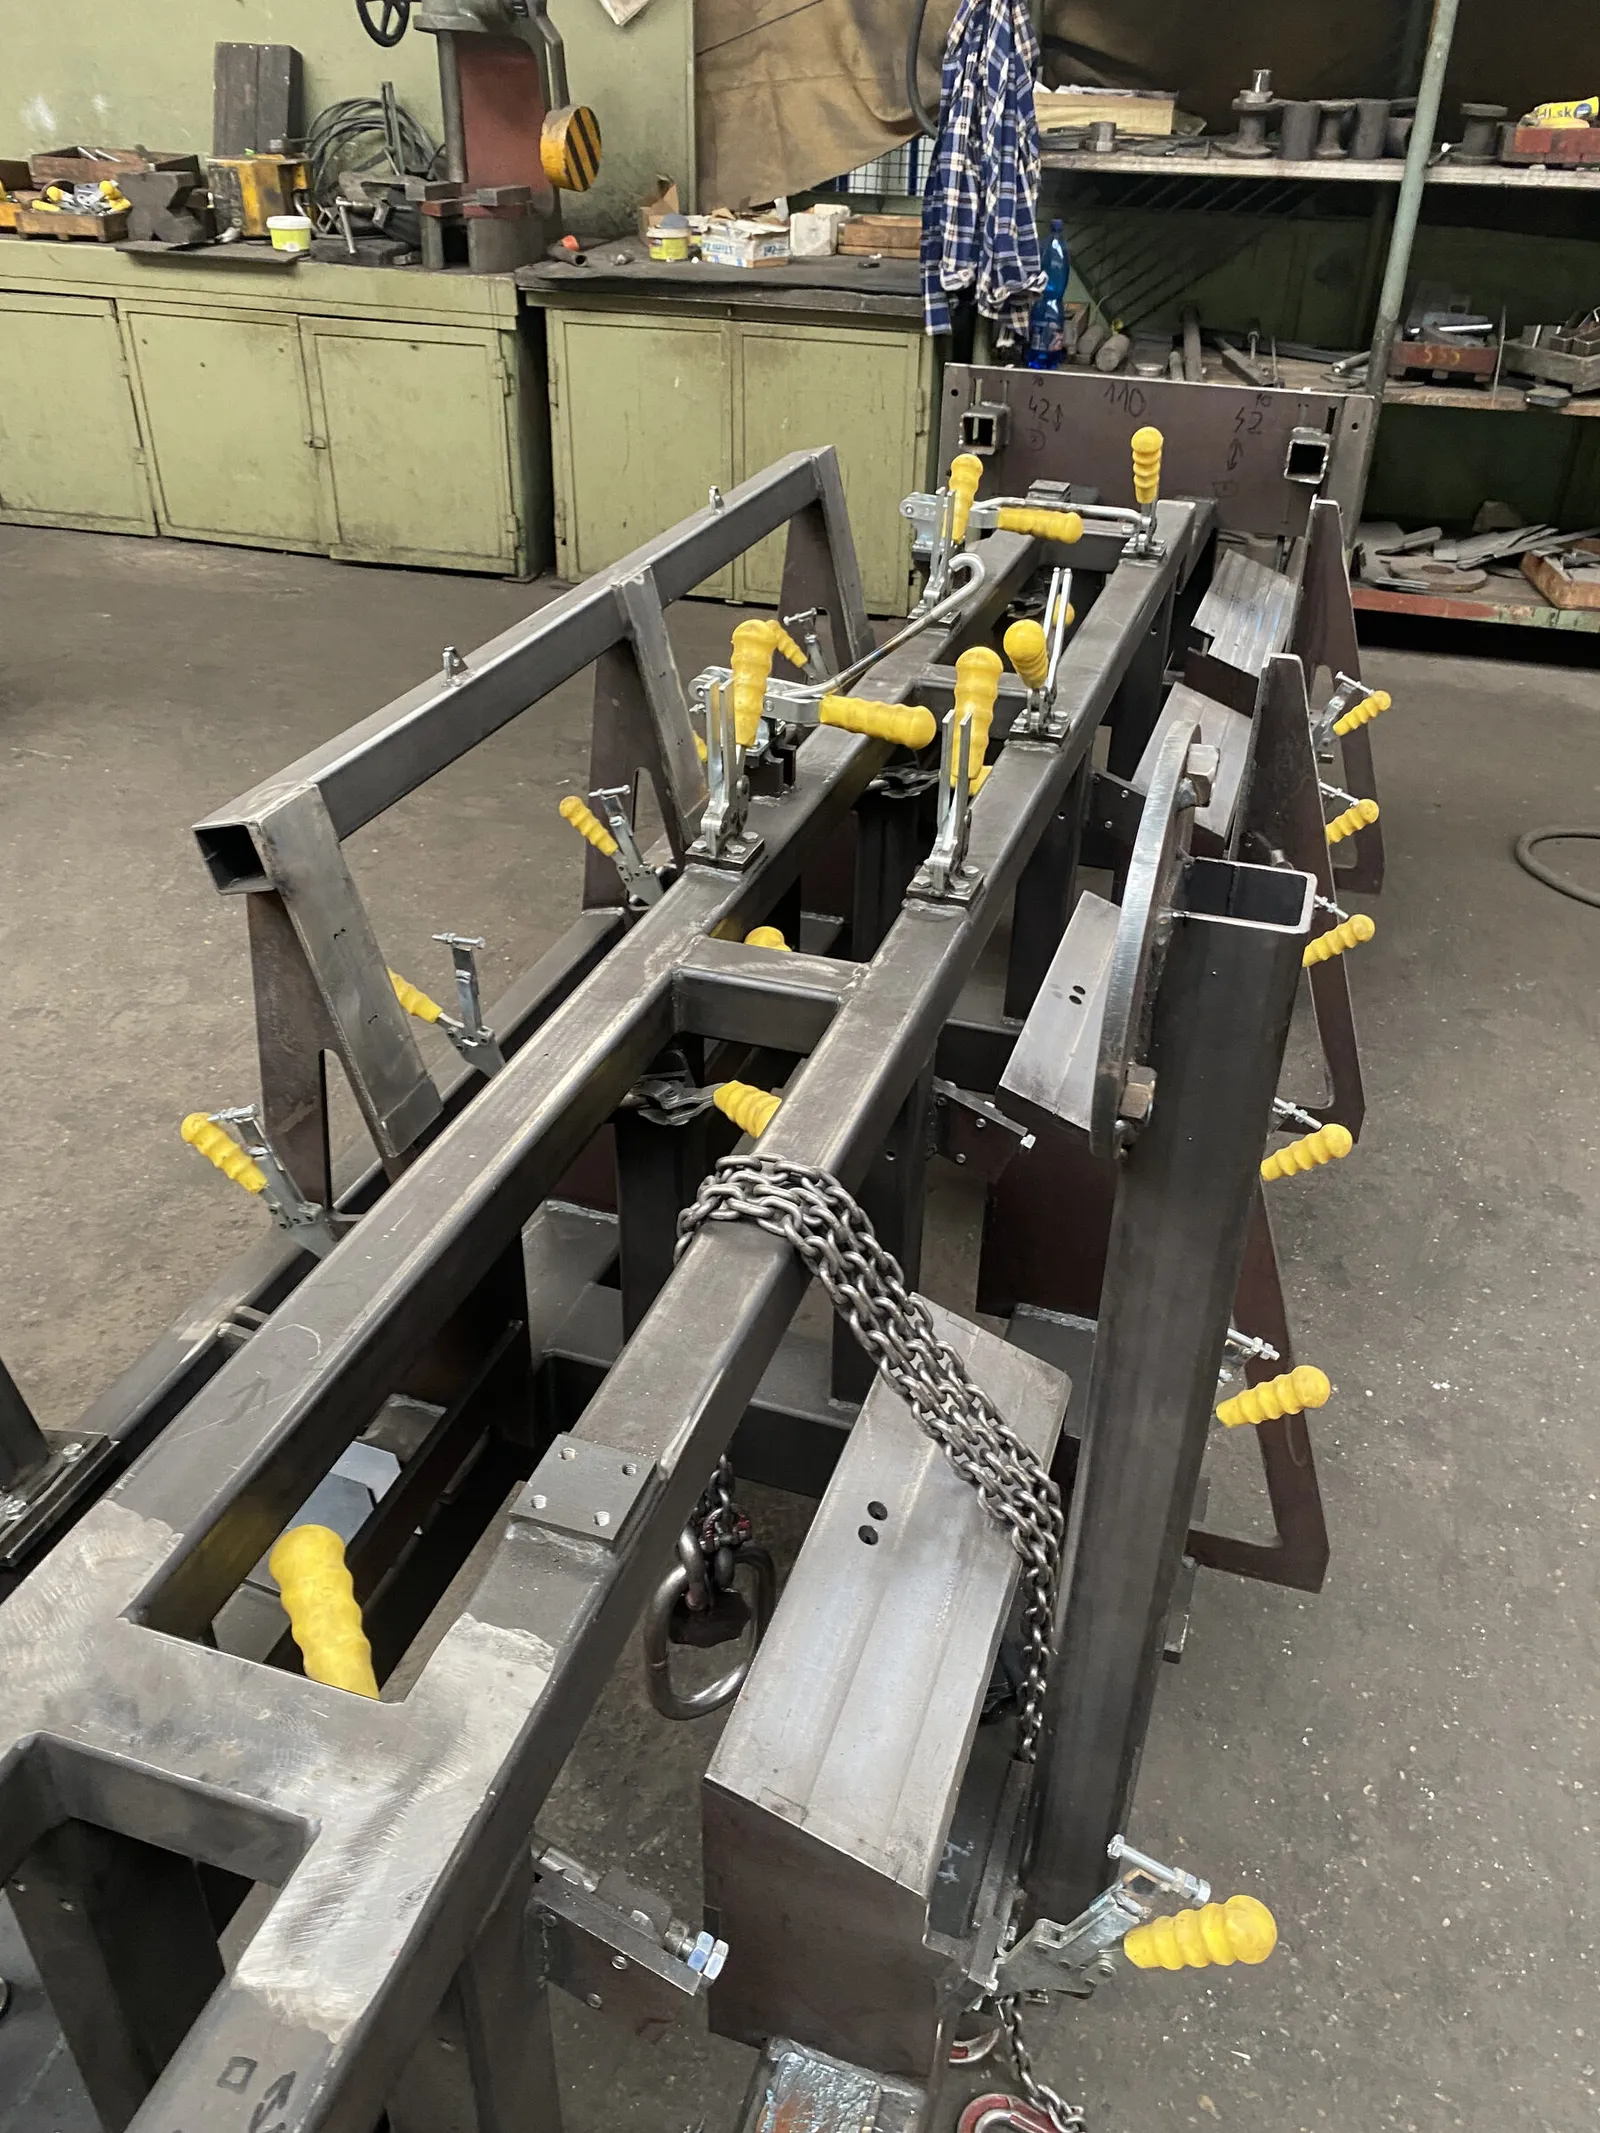
Welding jig with a frame clamped Welding jigs and fixtures
- designed and built for the customer's own production
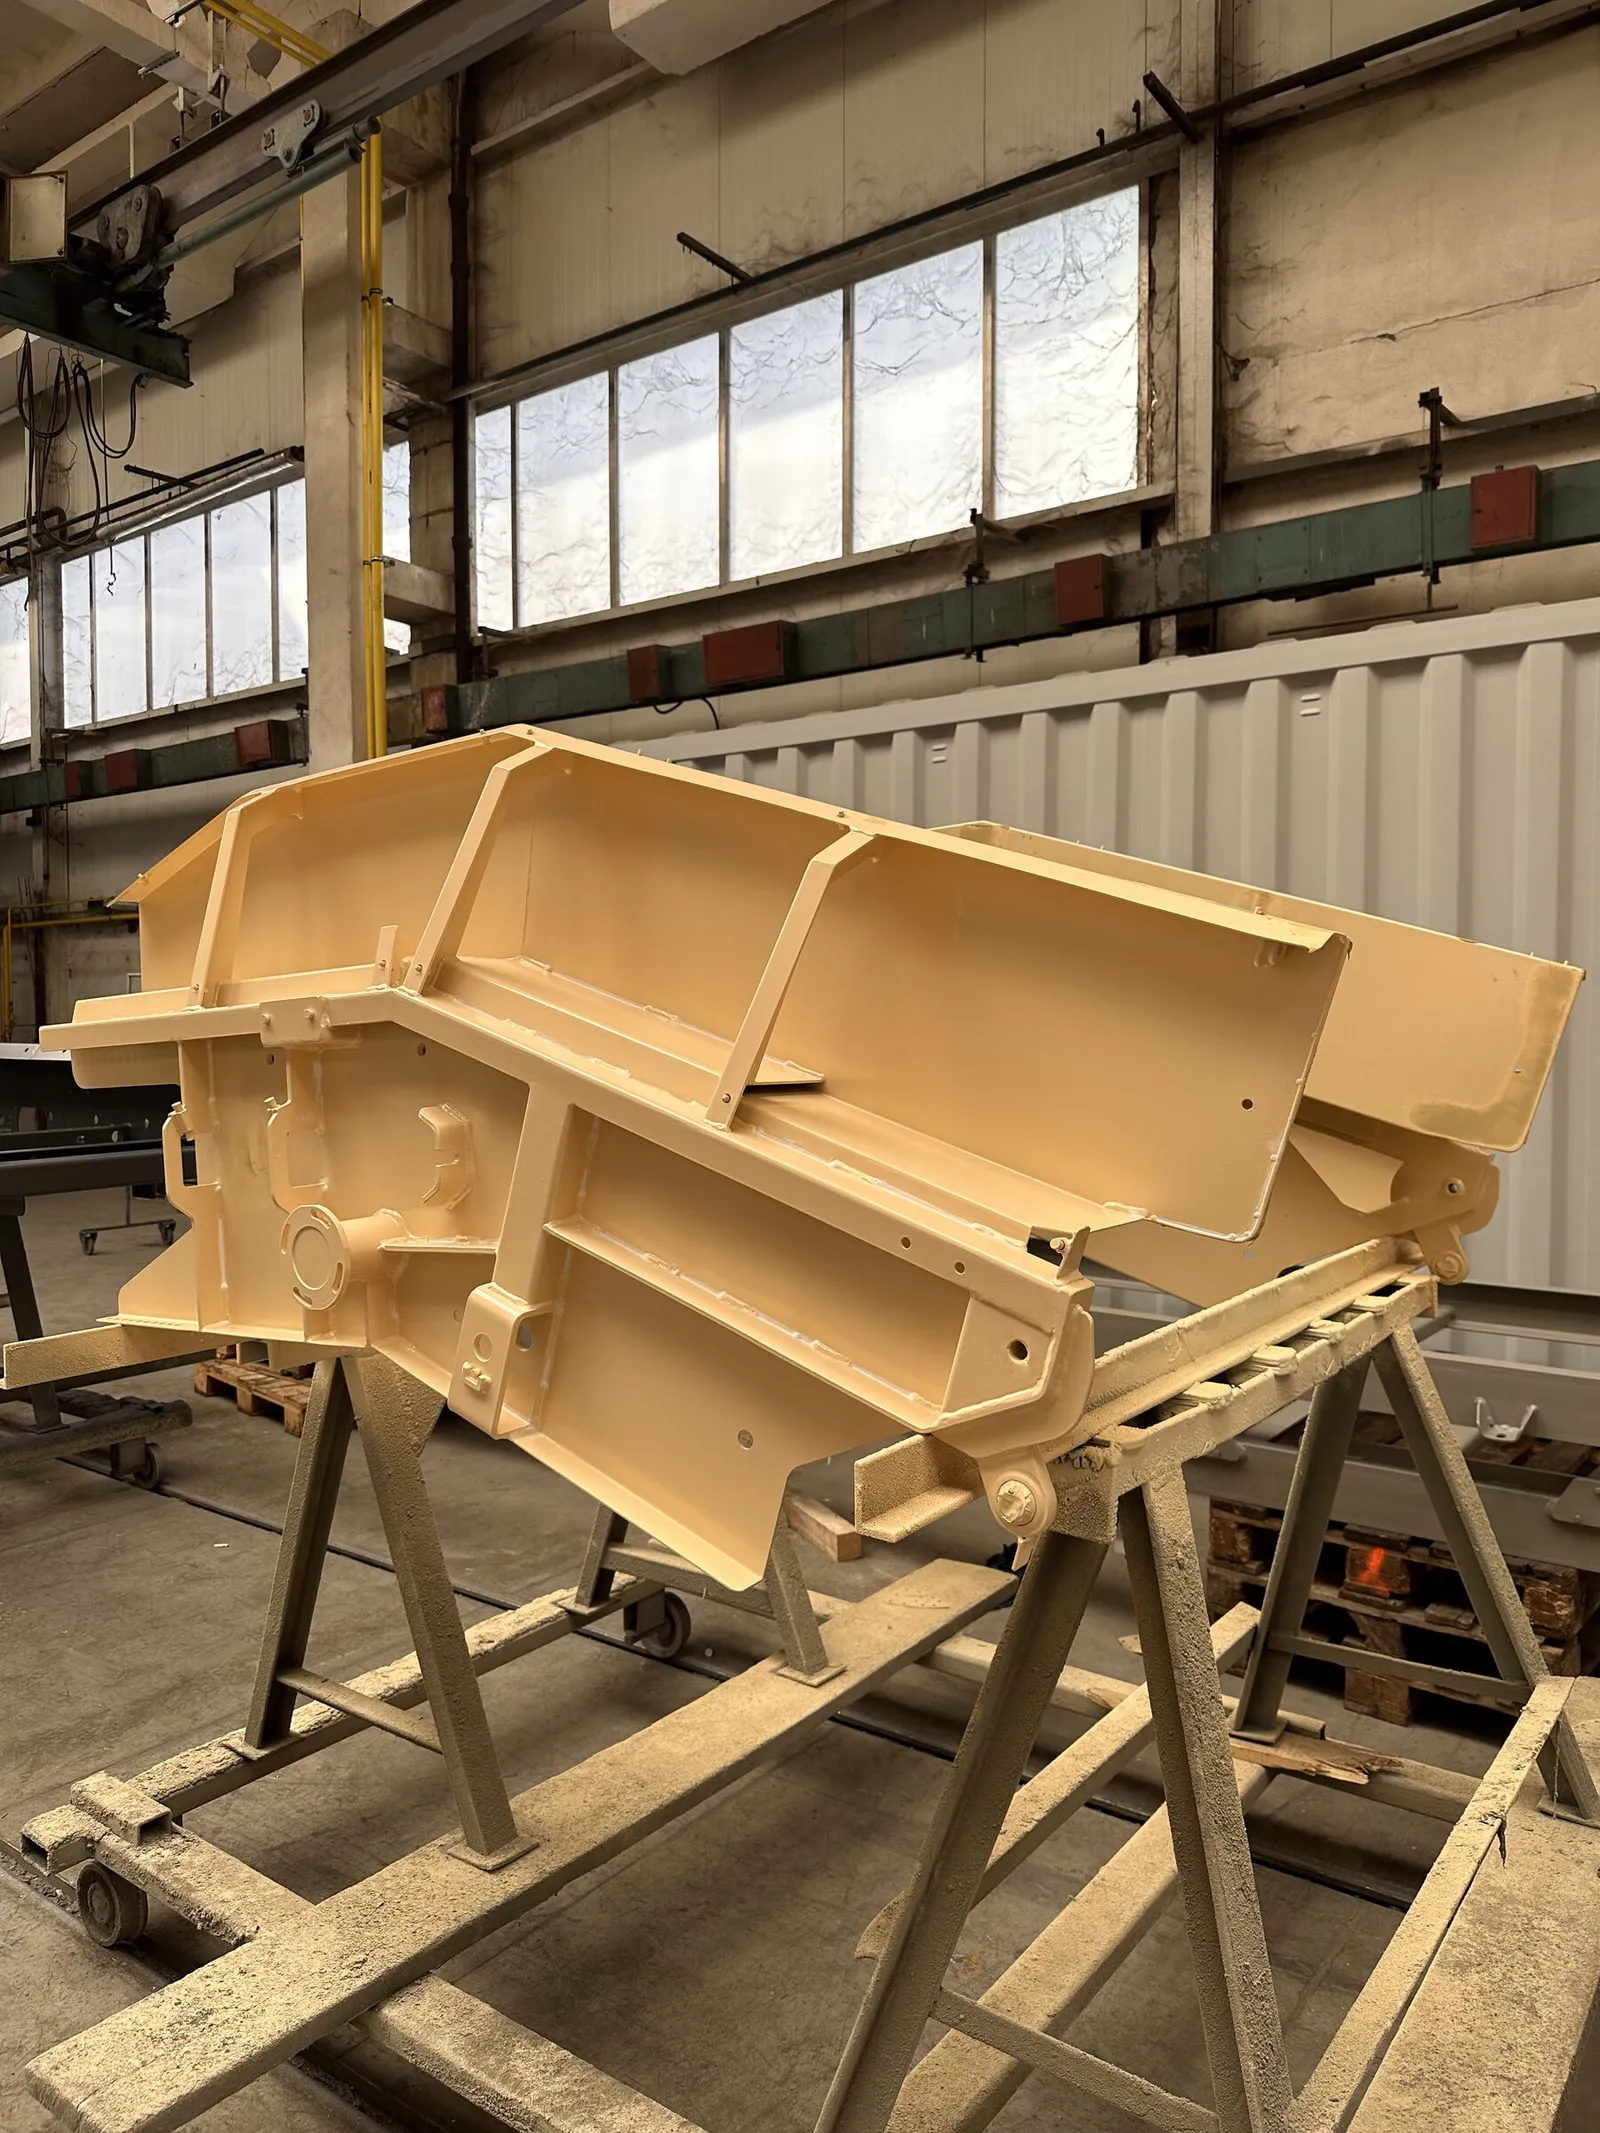
Welded part for an agricultural machinery OEM Agricultural and harvesting machinery parts
- frames and fabricated components on repeat frame agreements
Build detail
What the detail photography shows
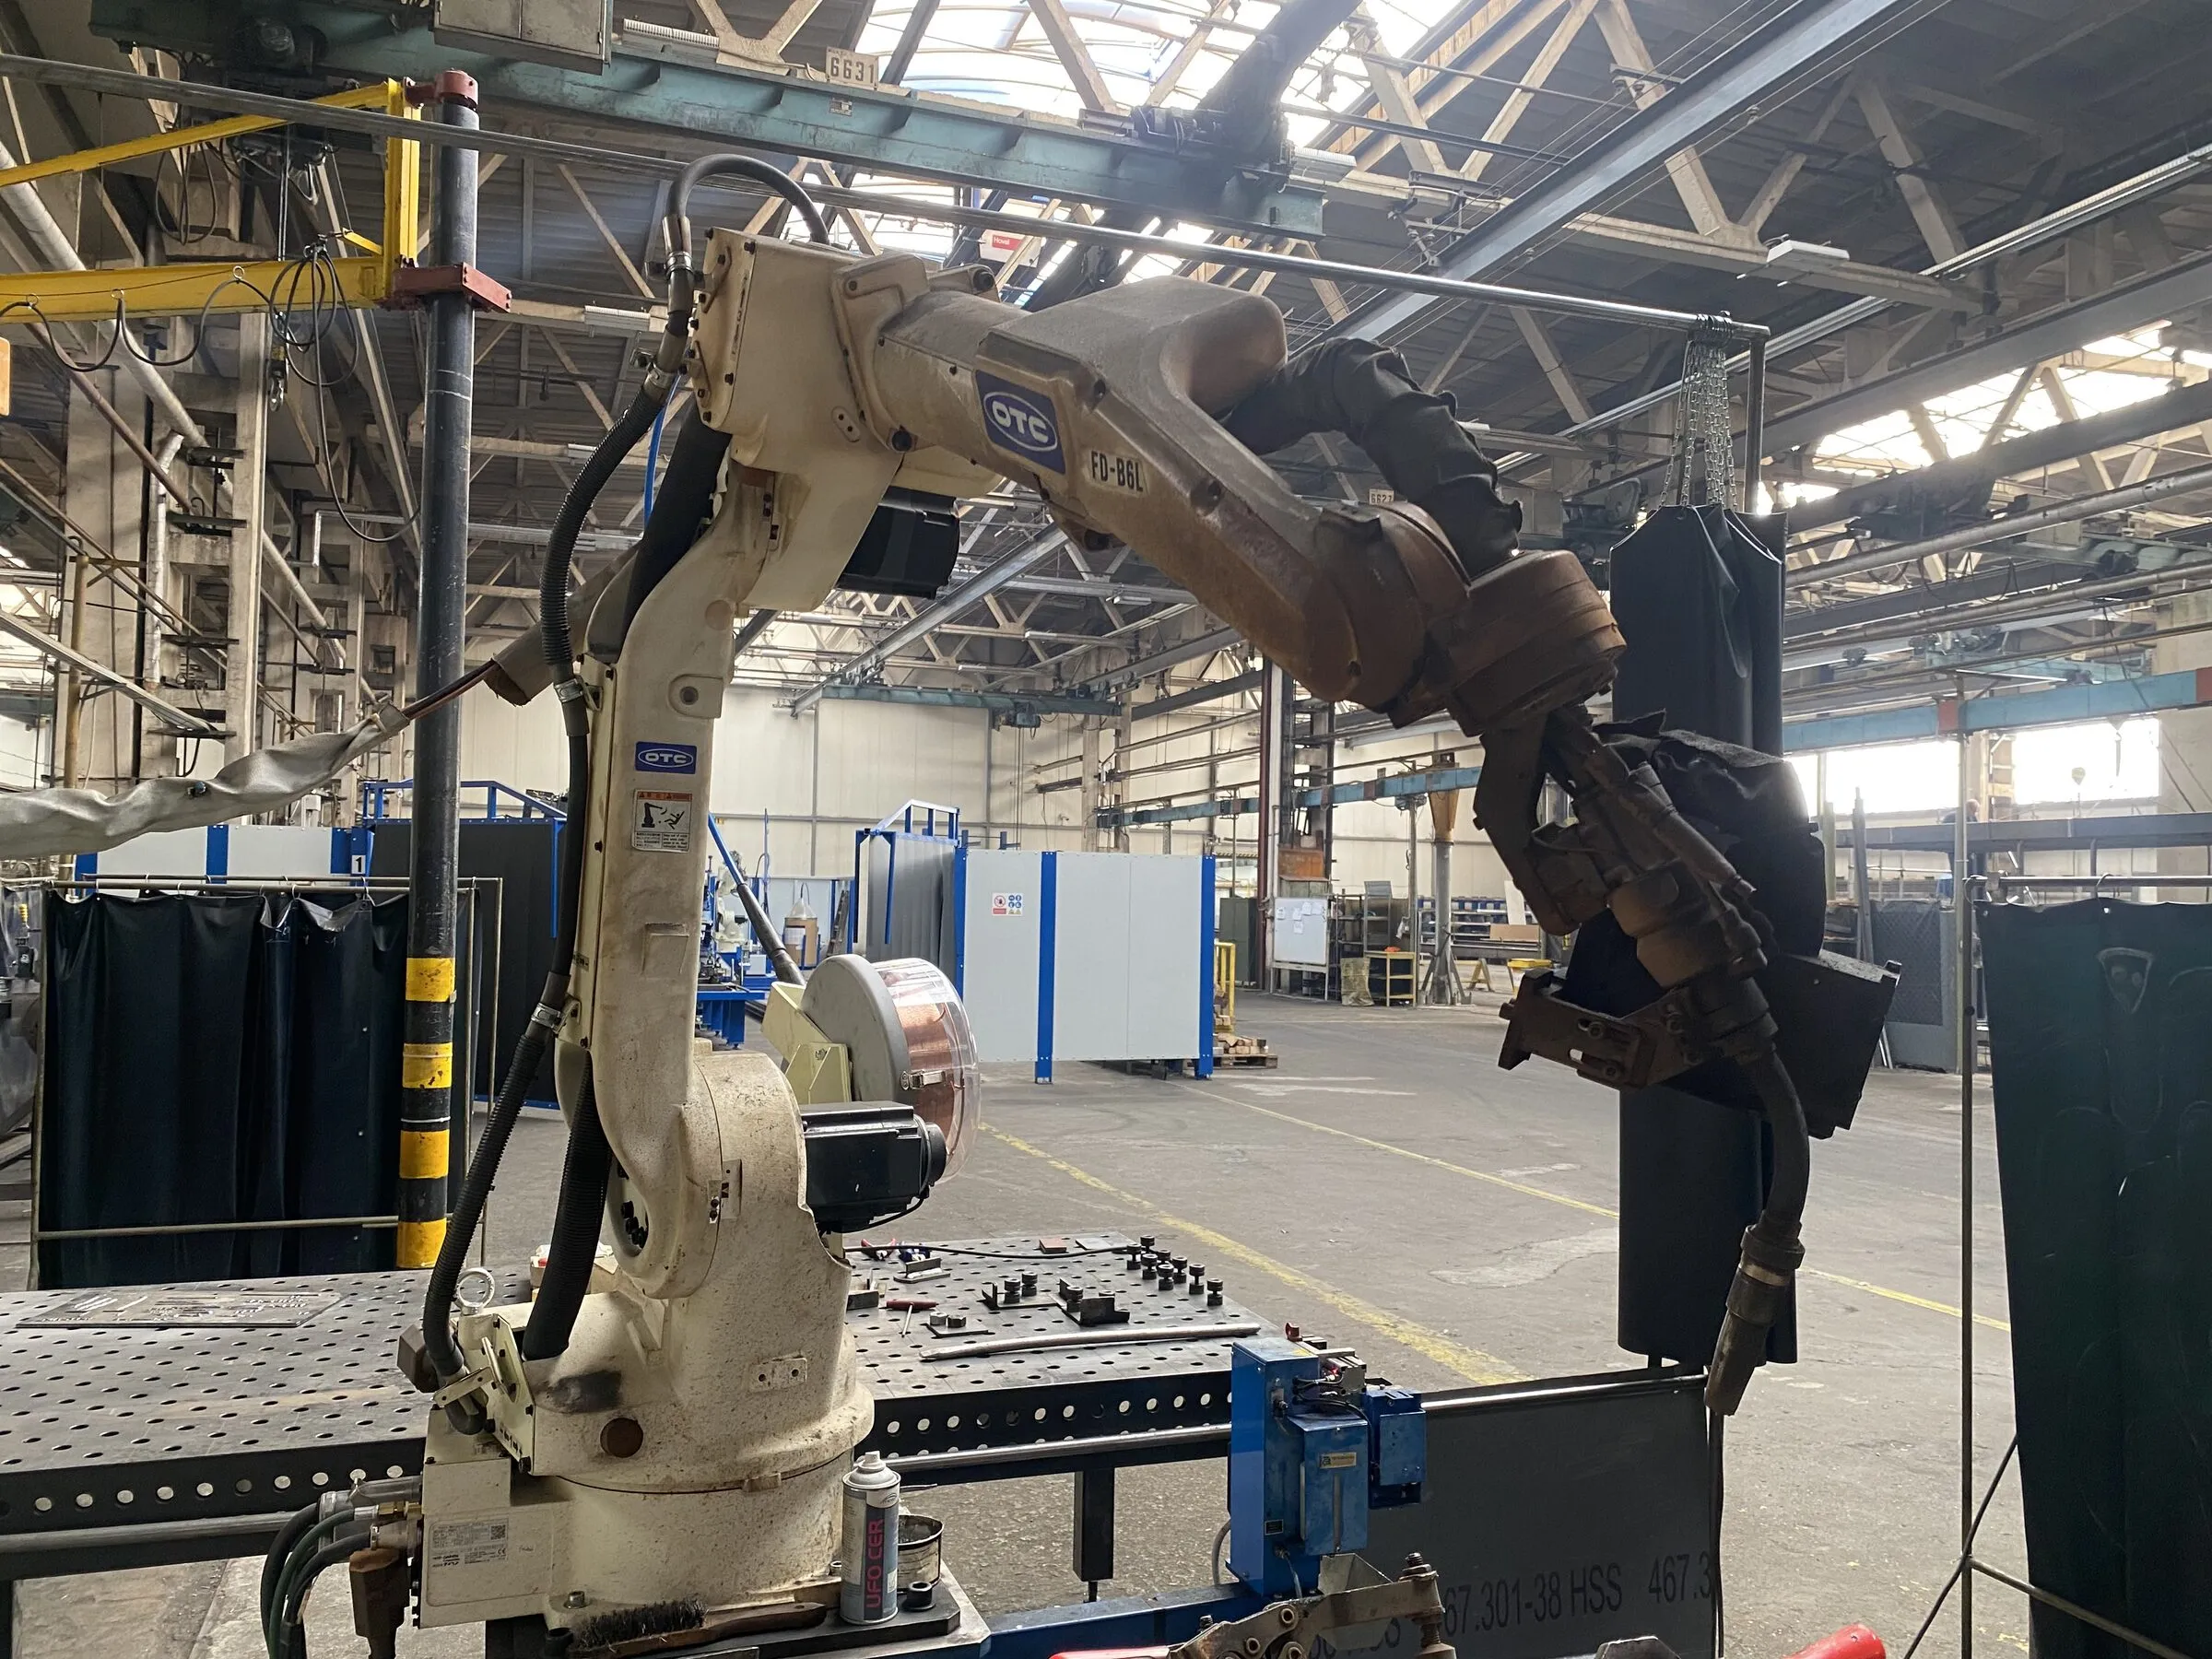
Robotic welding cell on the 14 m track 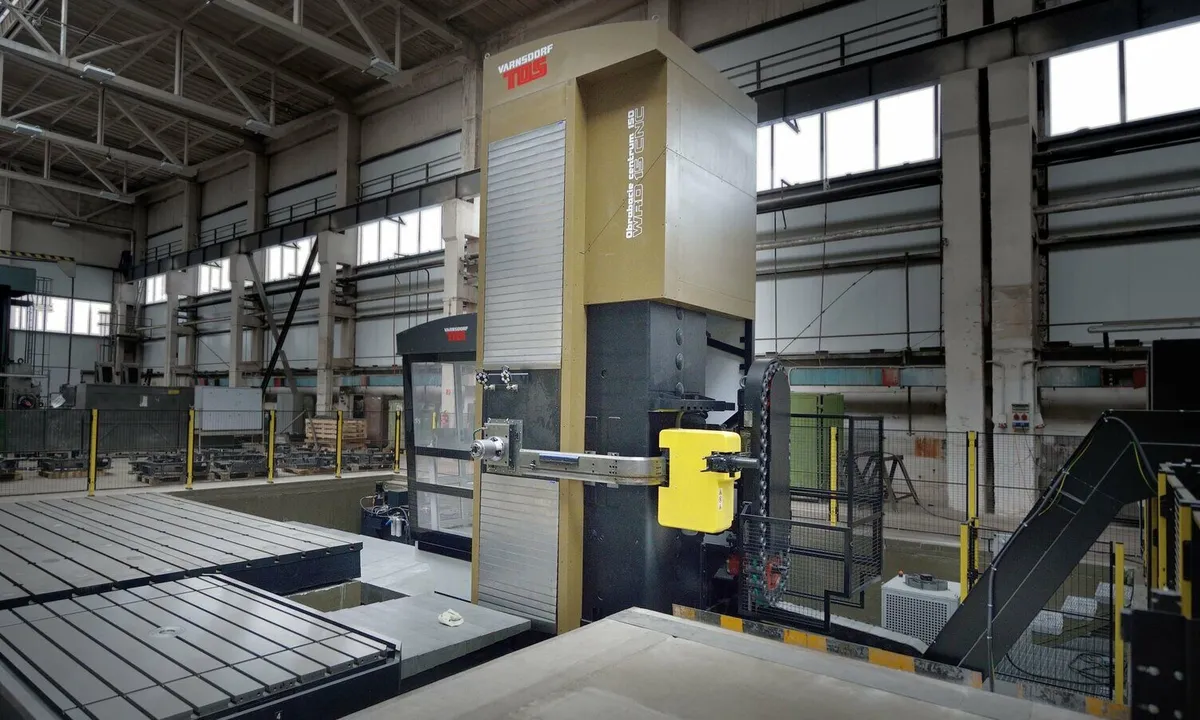
Machine shop, large horizontal boring machine 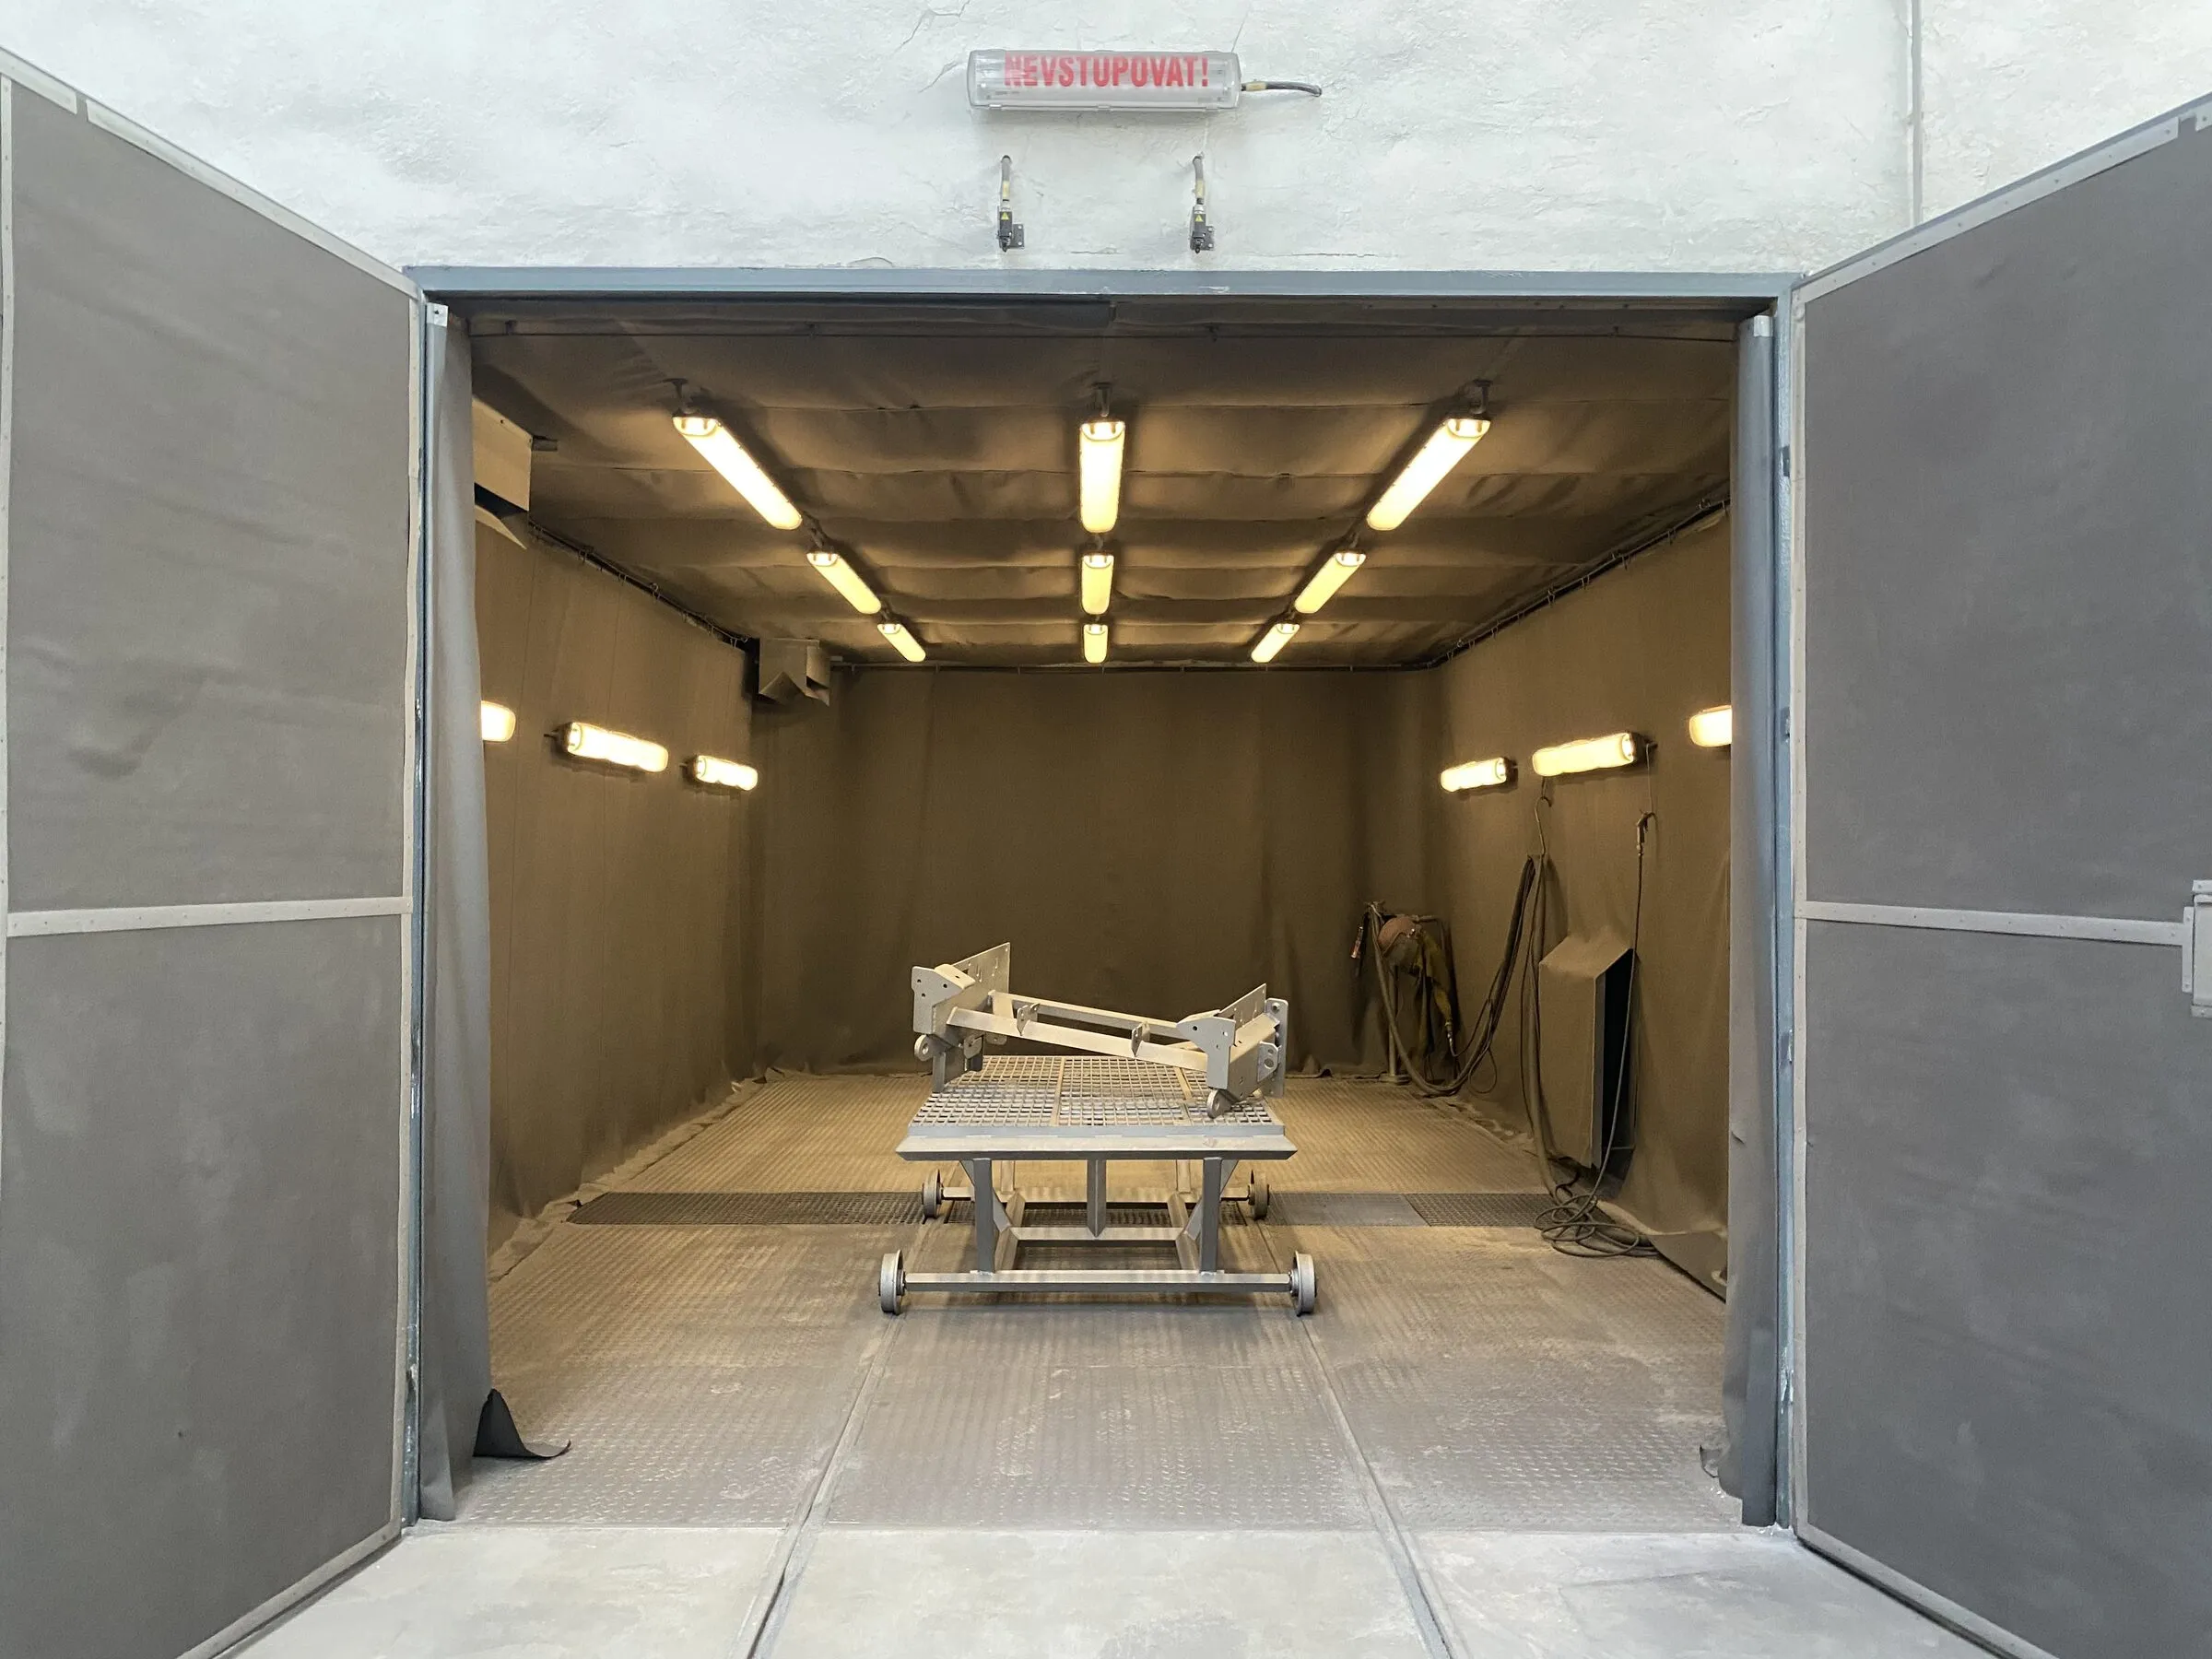
Shot blasting to Sa 2.5, rail-linked to the paint booth 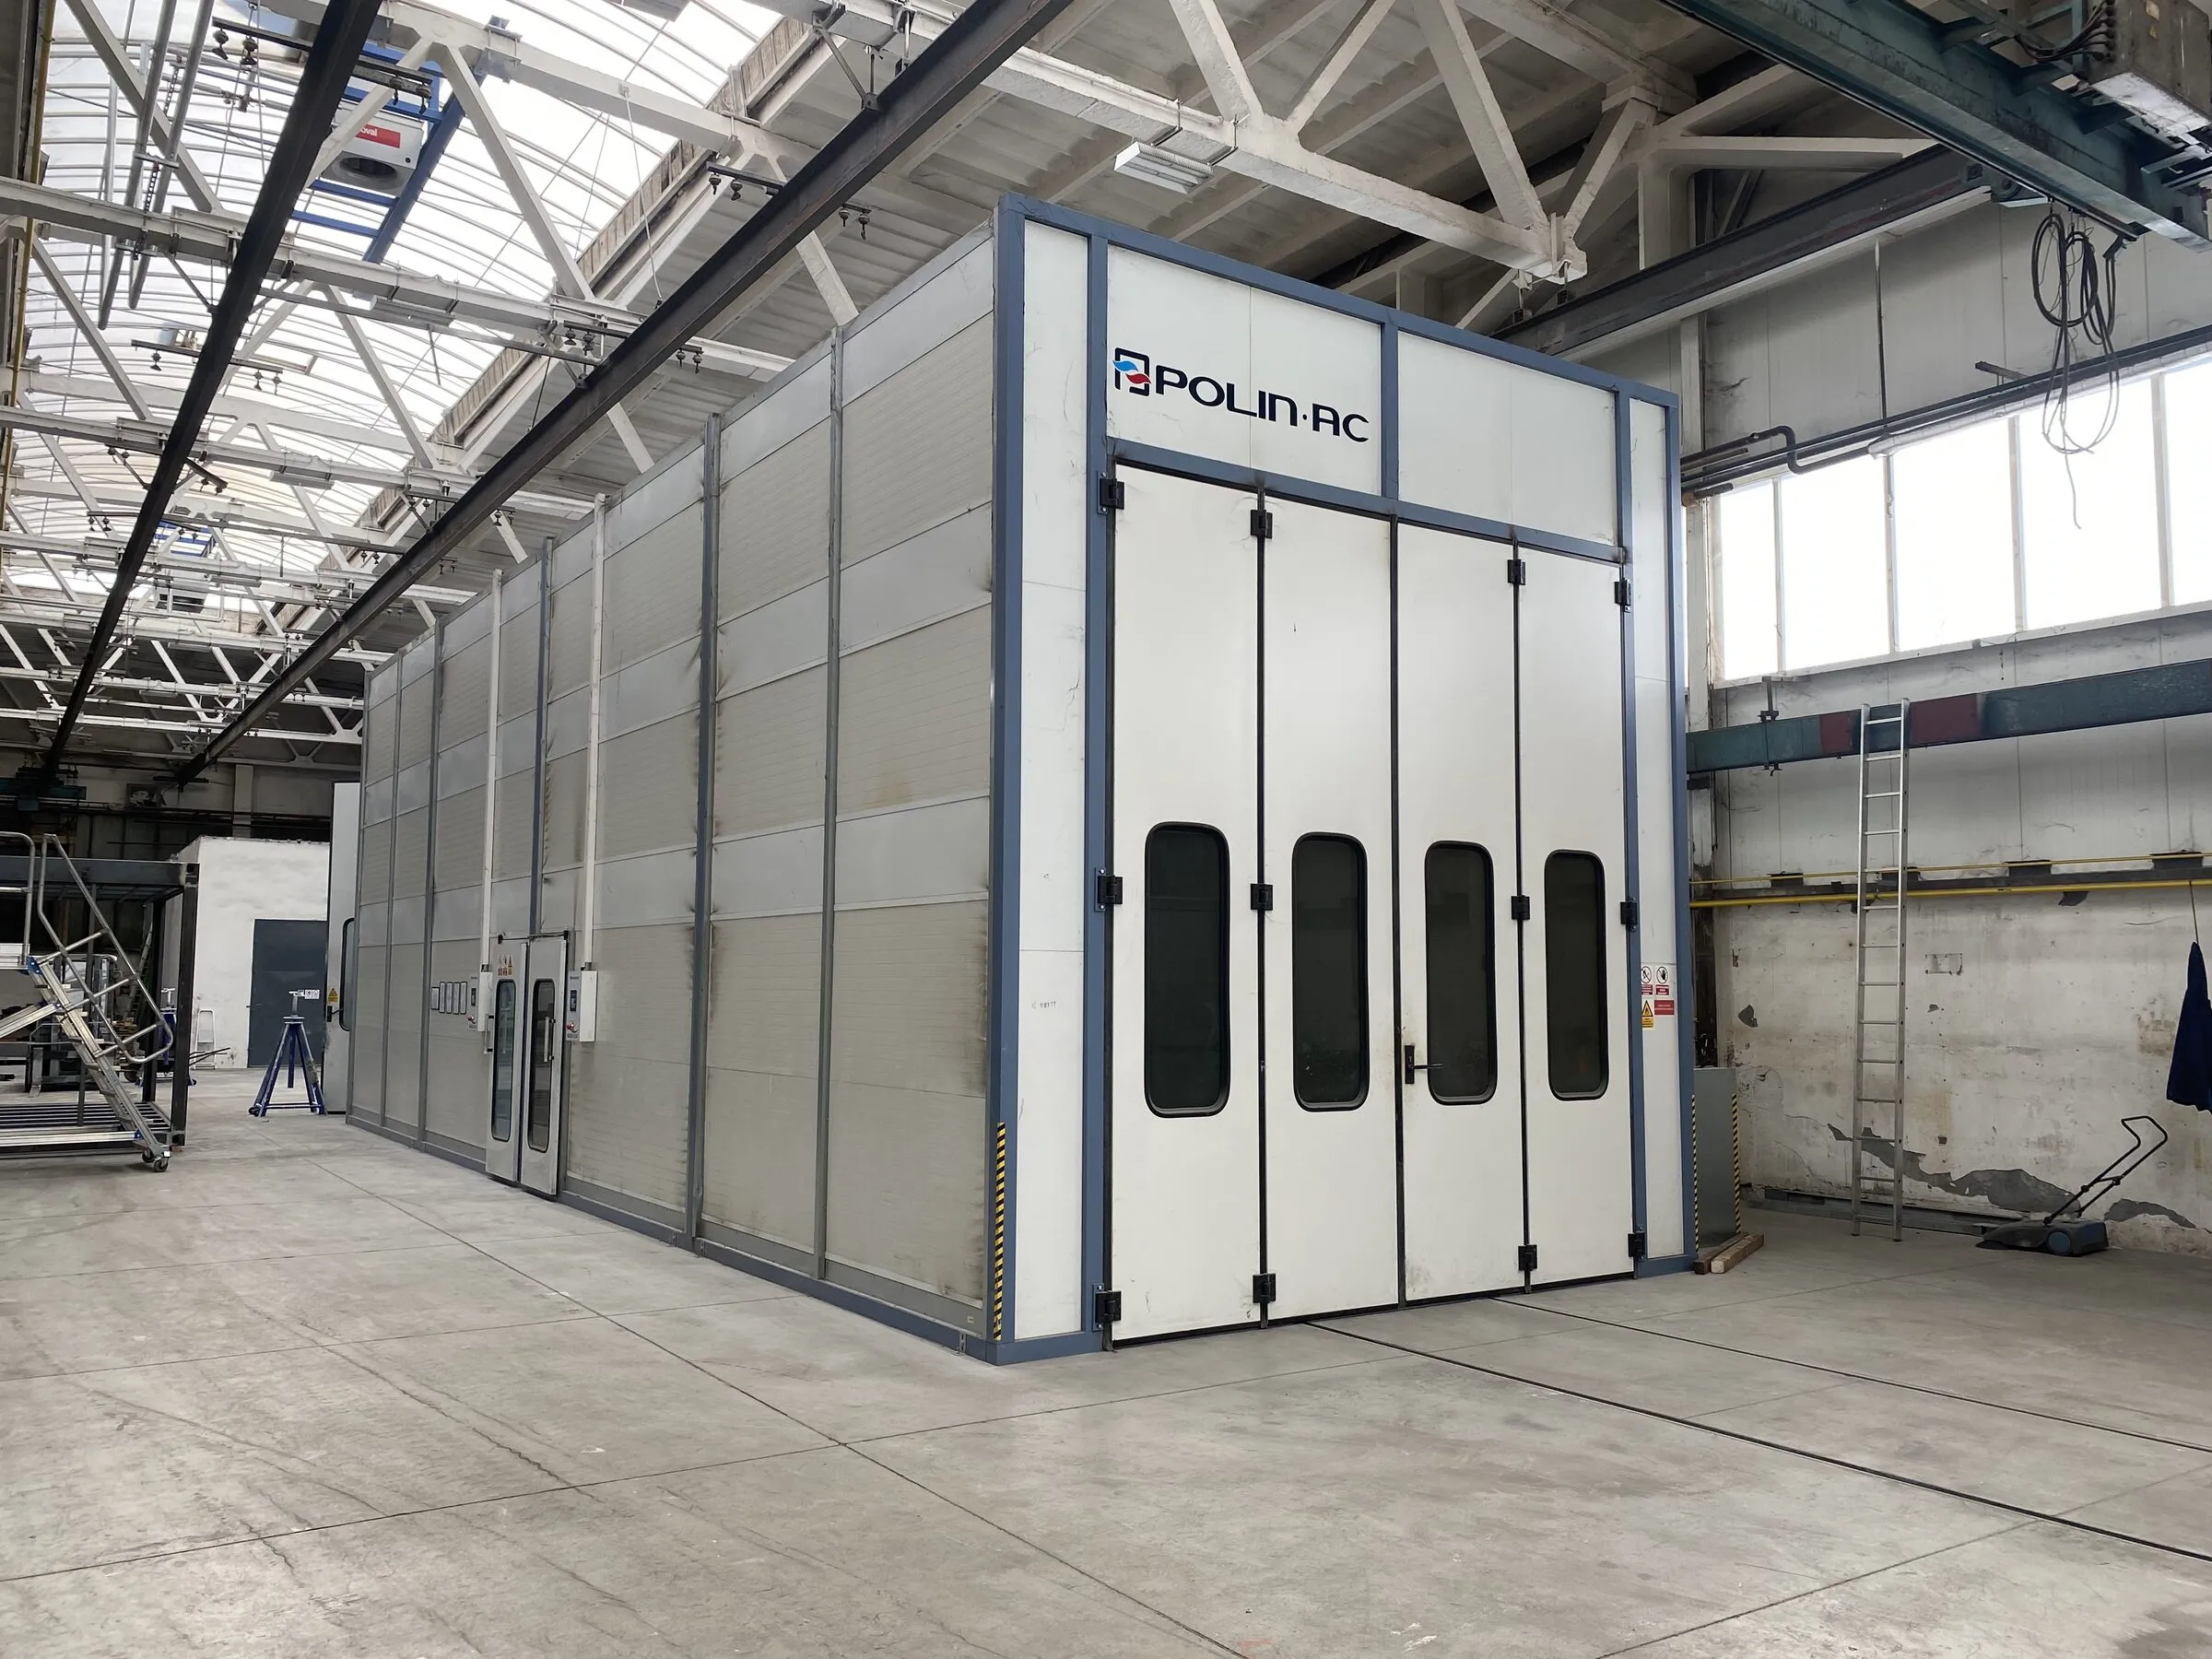
Paint booth, 7.9 m long 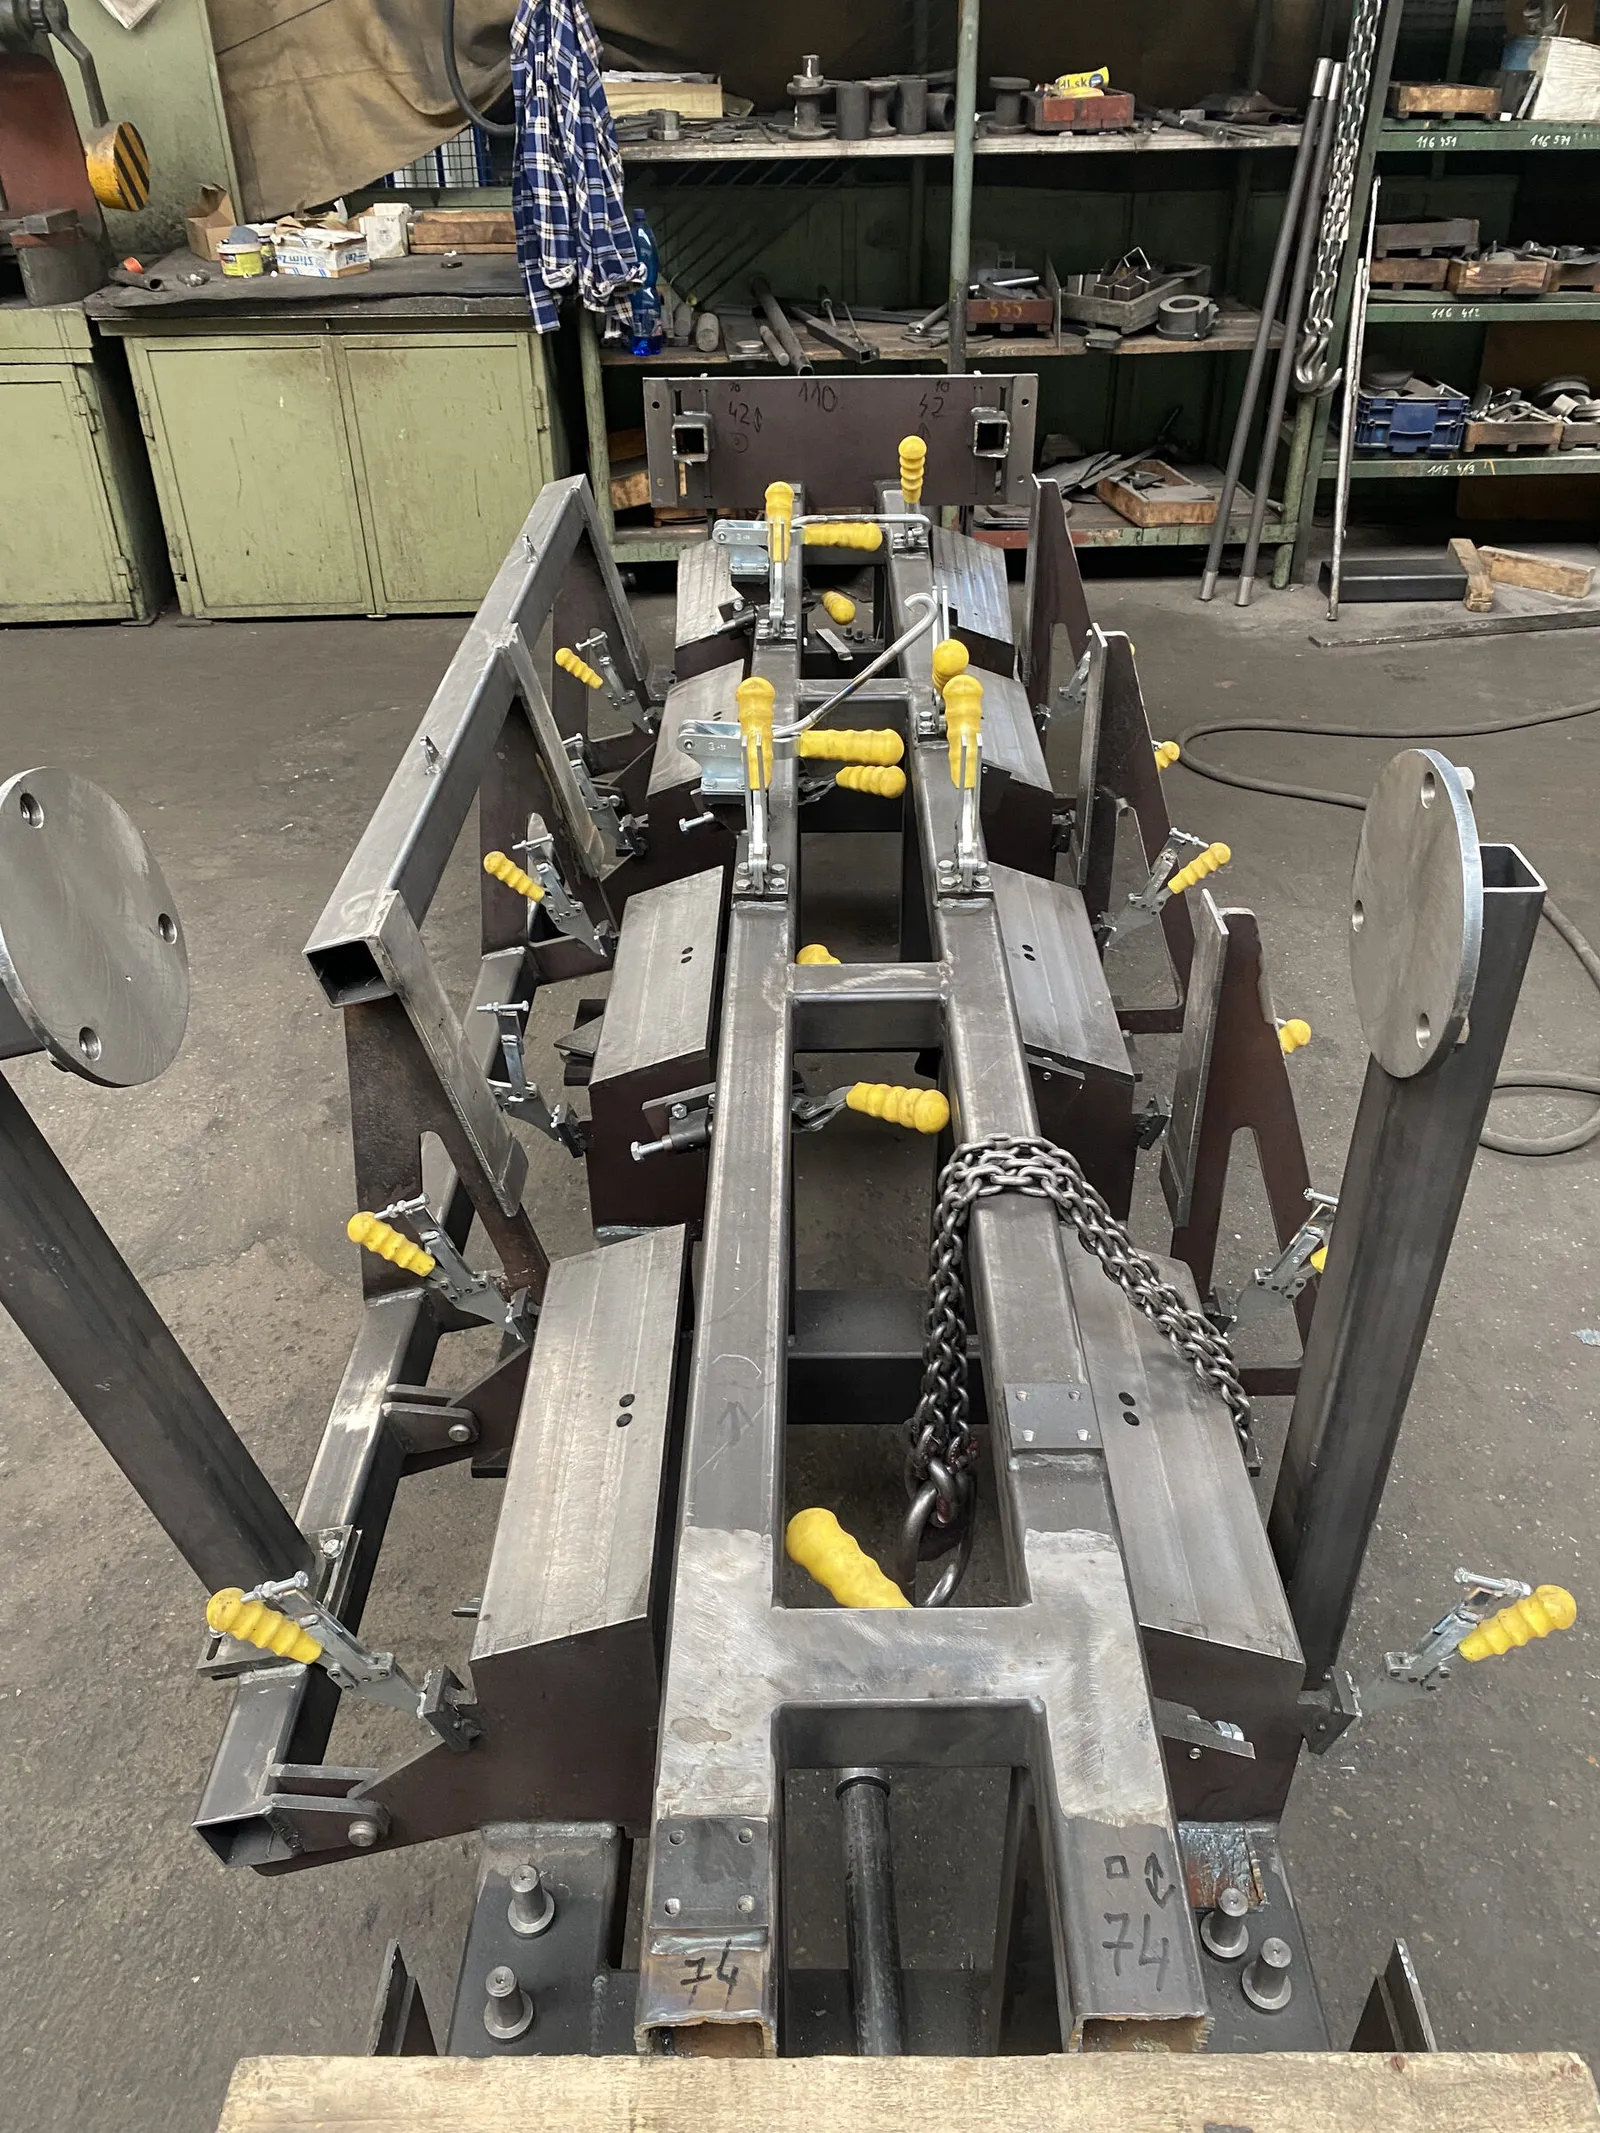
Welding jig with a part clamped 
Weldment after machining
The hall
Photographs from the workshop, by capability
Robotic welding cell
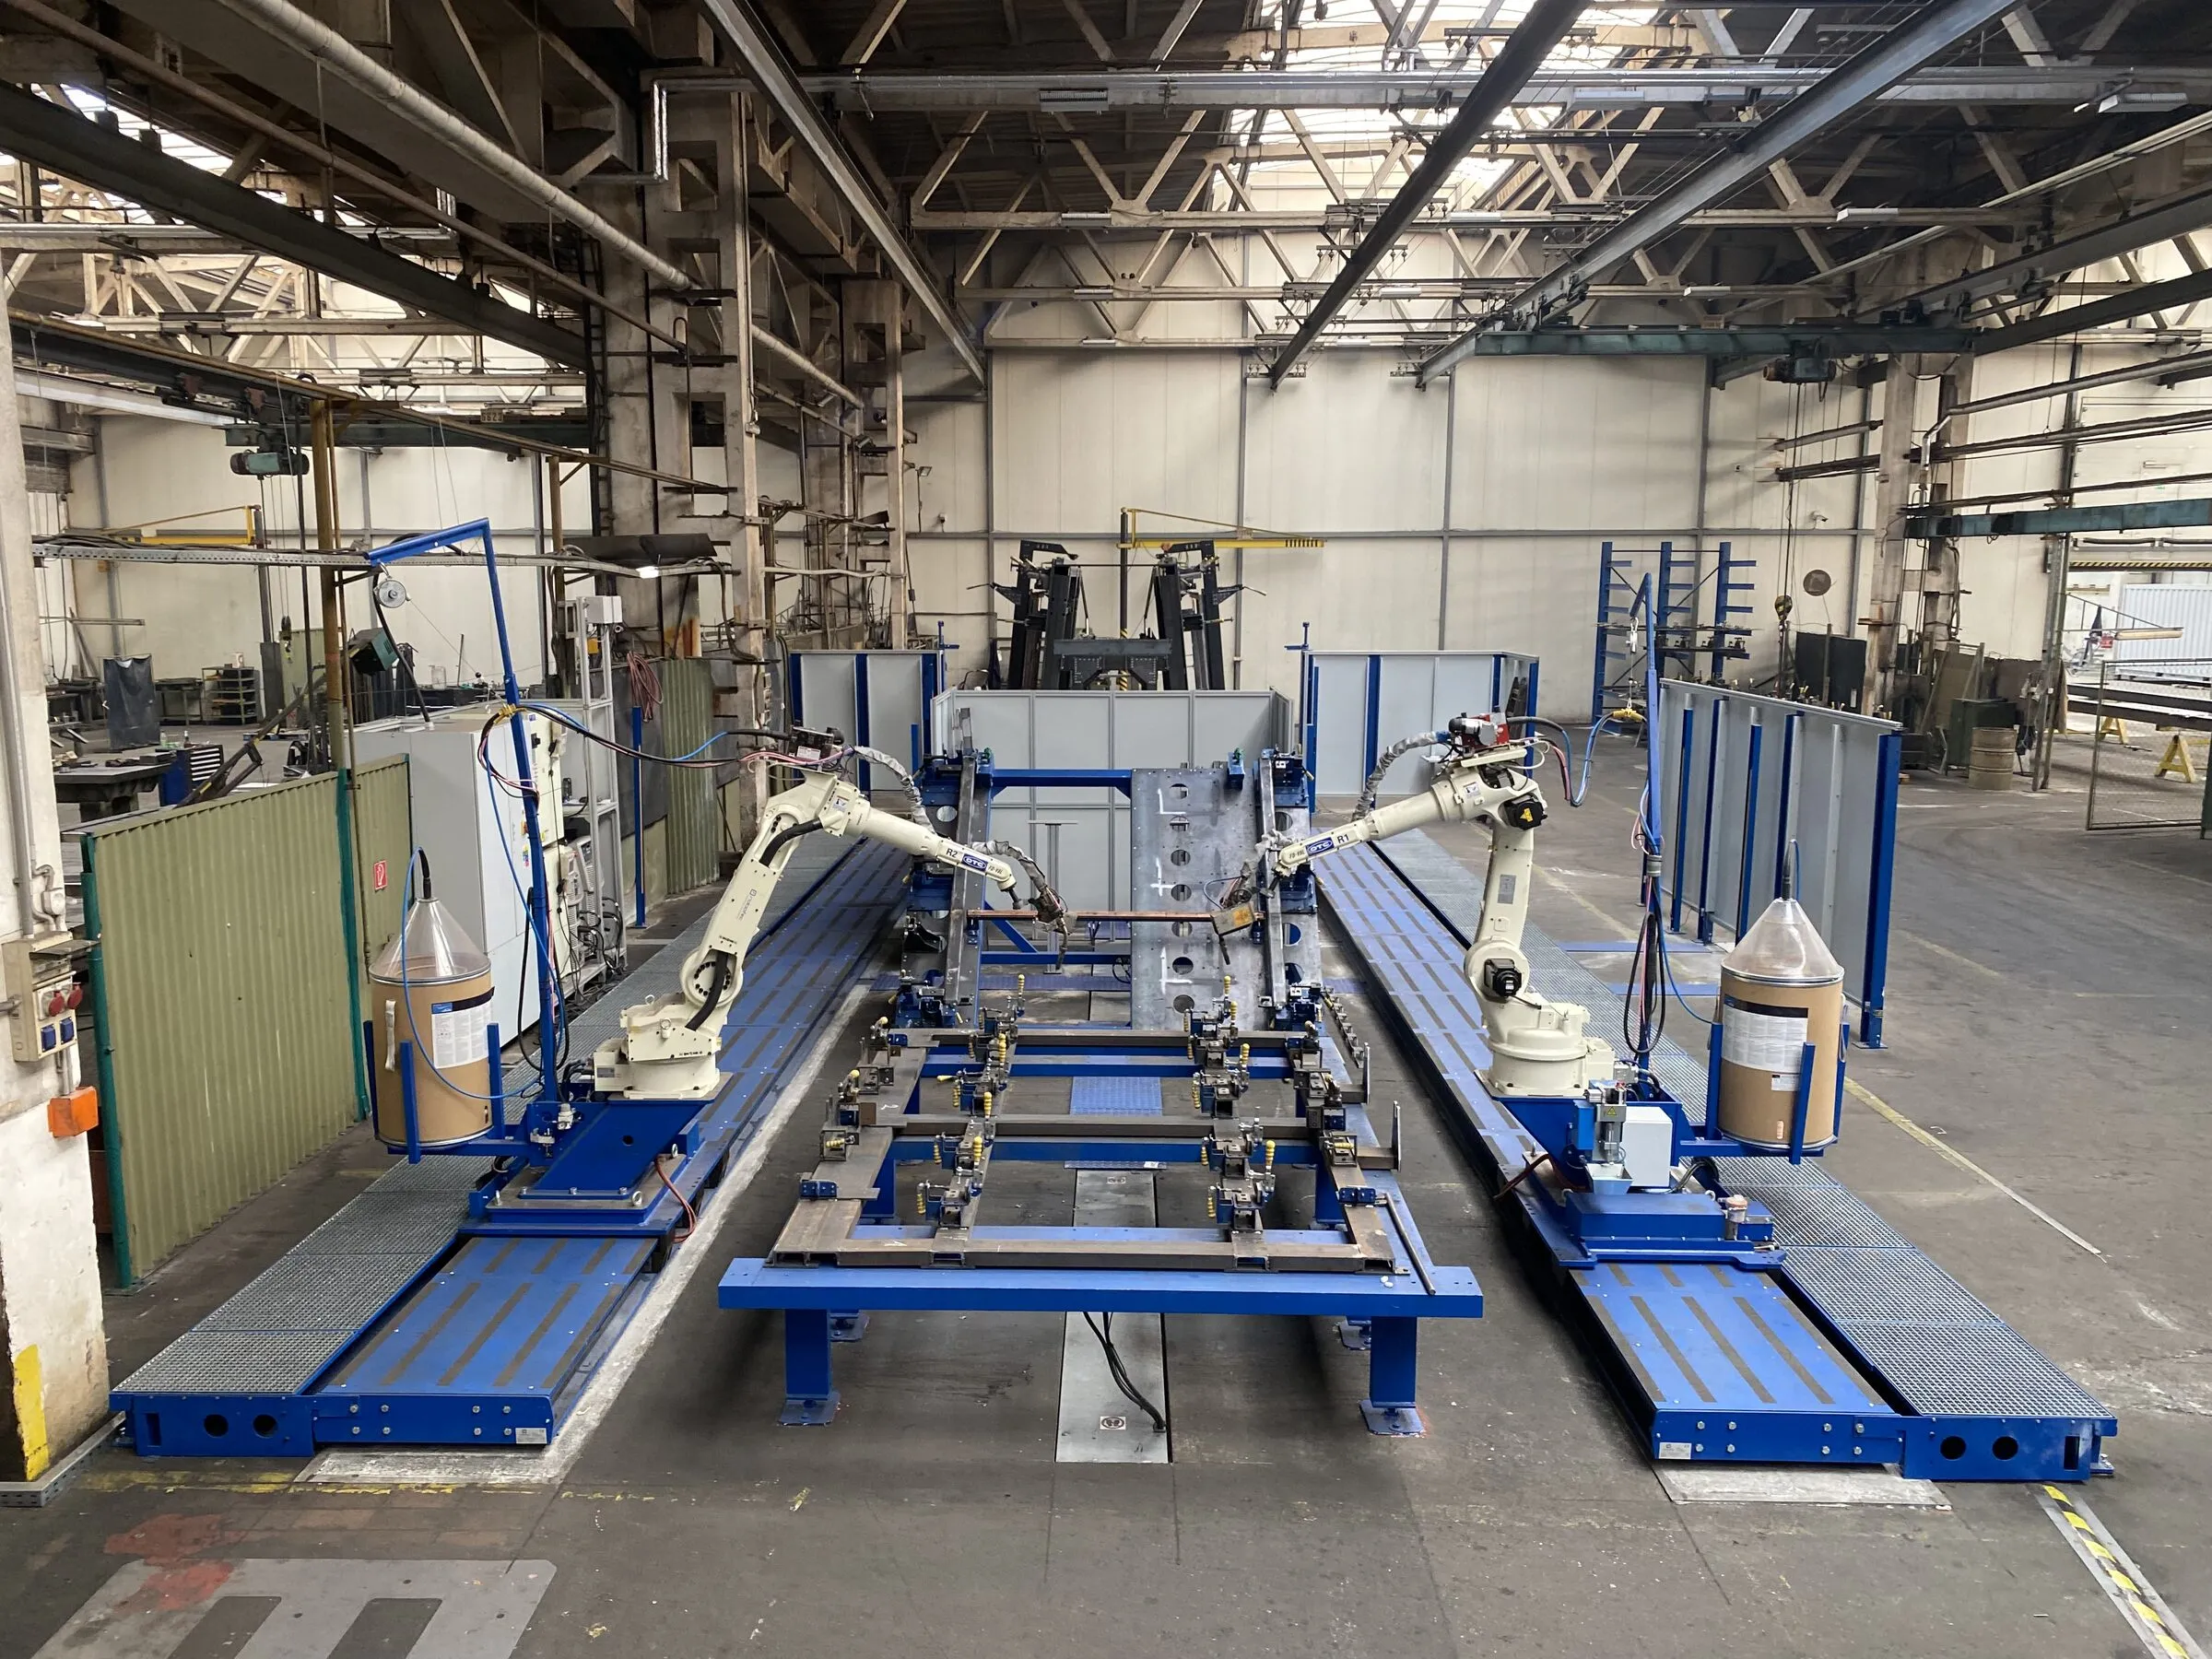
Two welding robots on the track over a long fixture, wide view of the cell 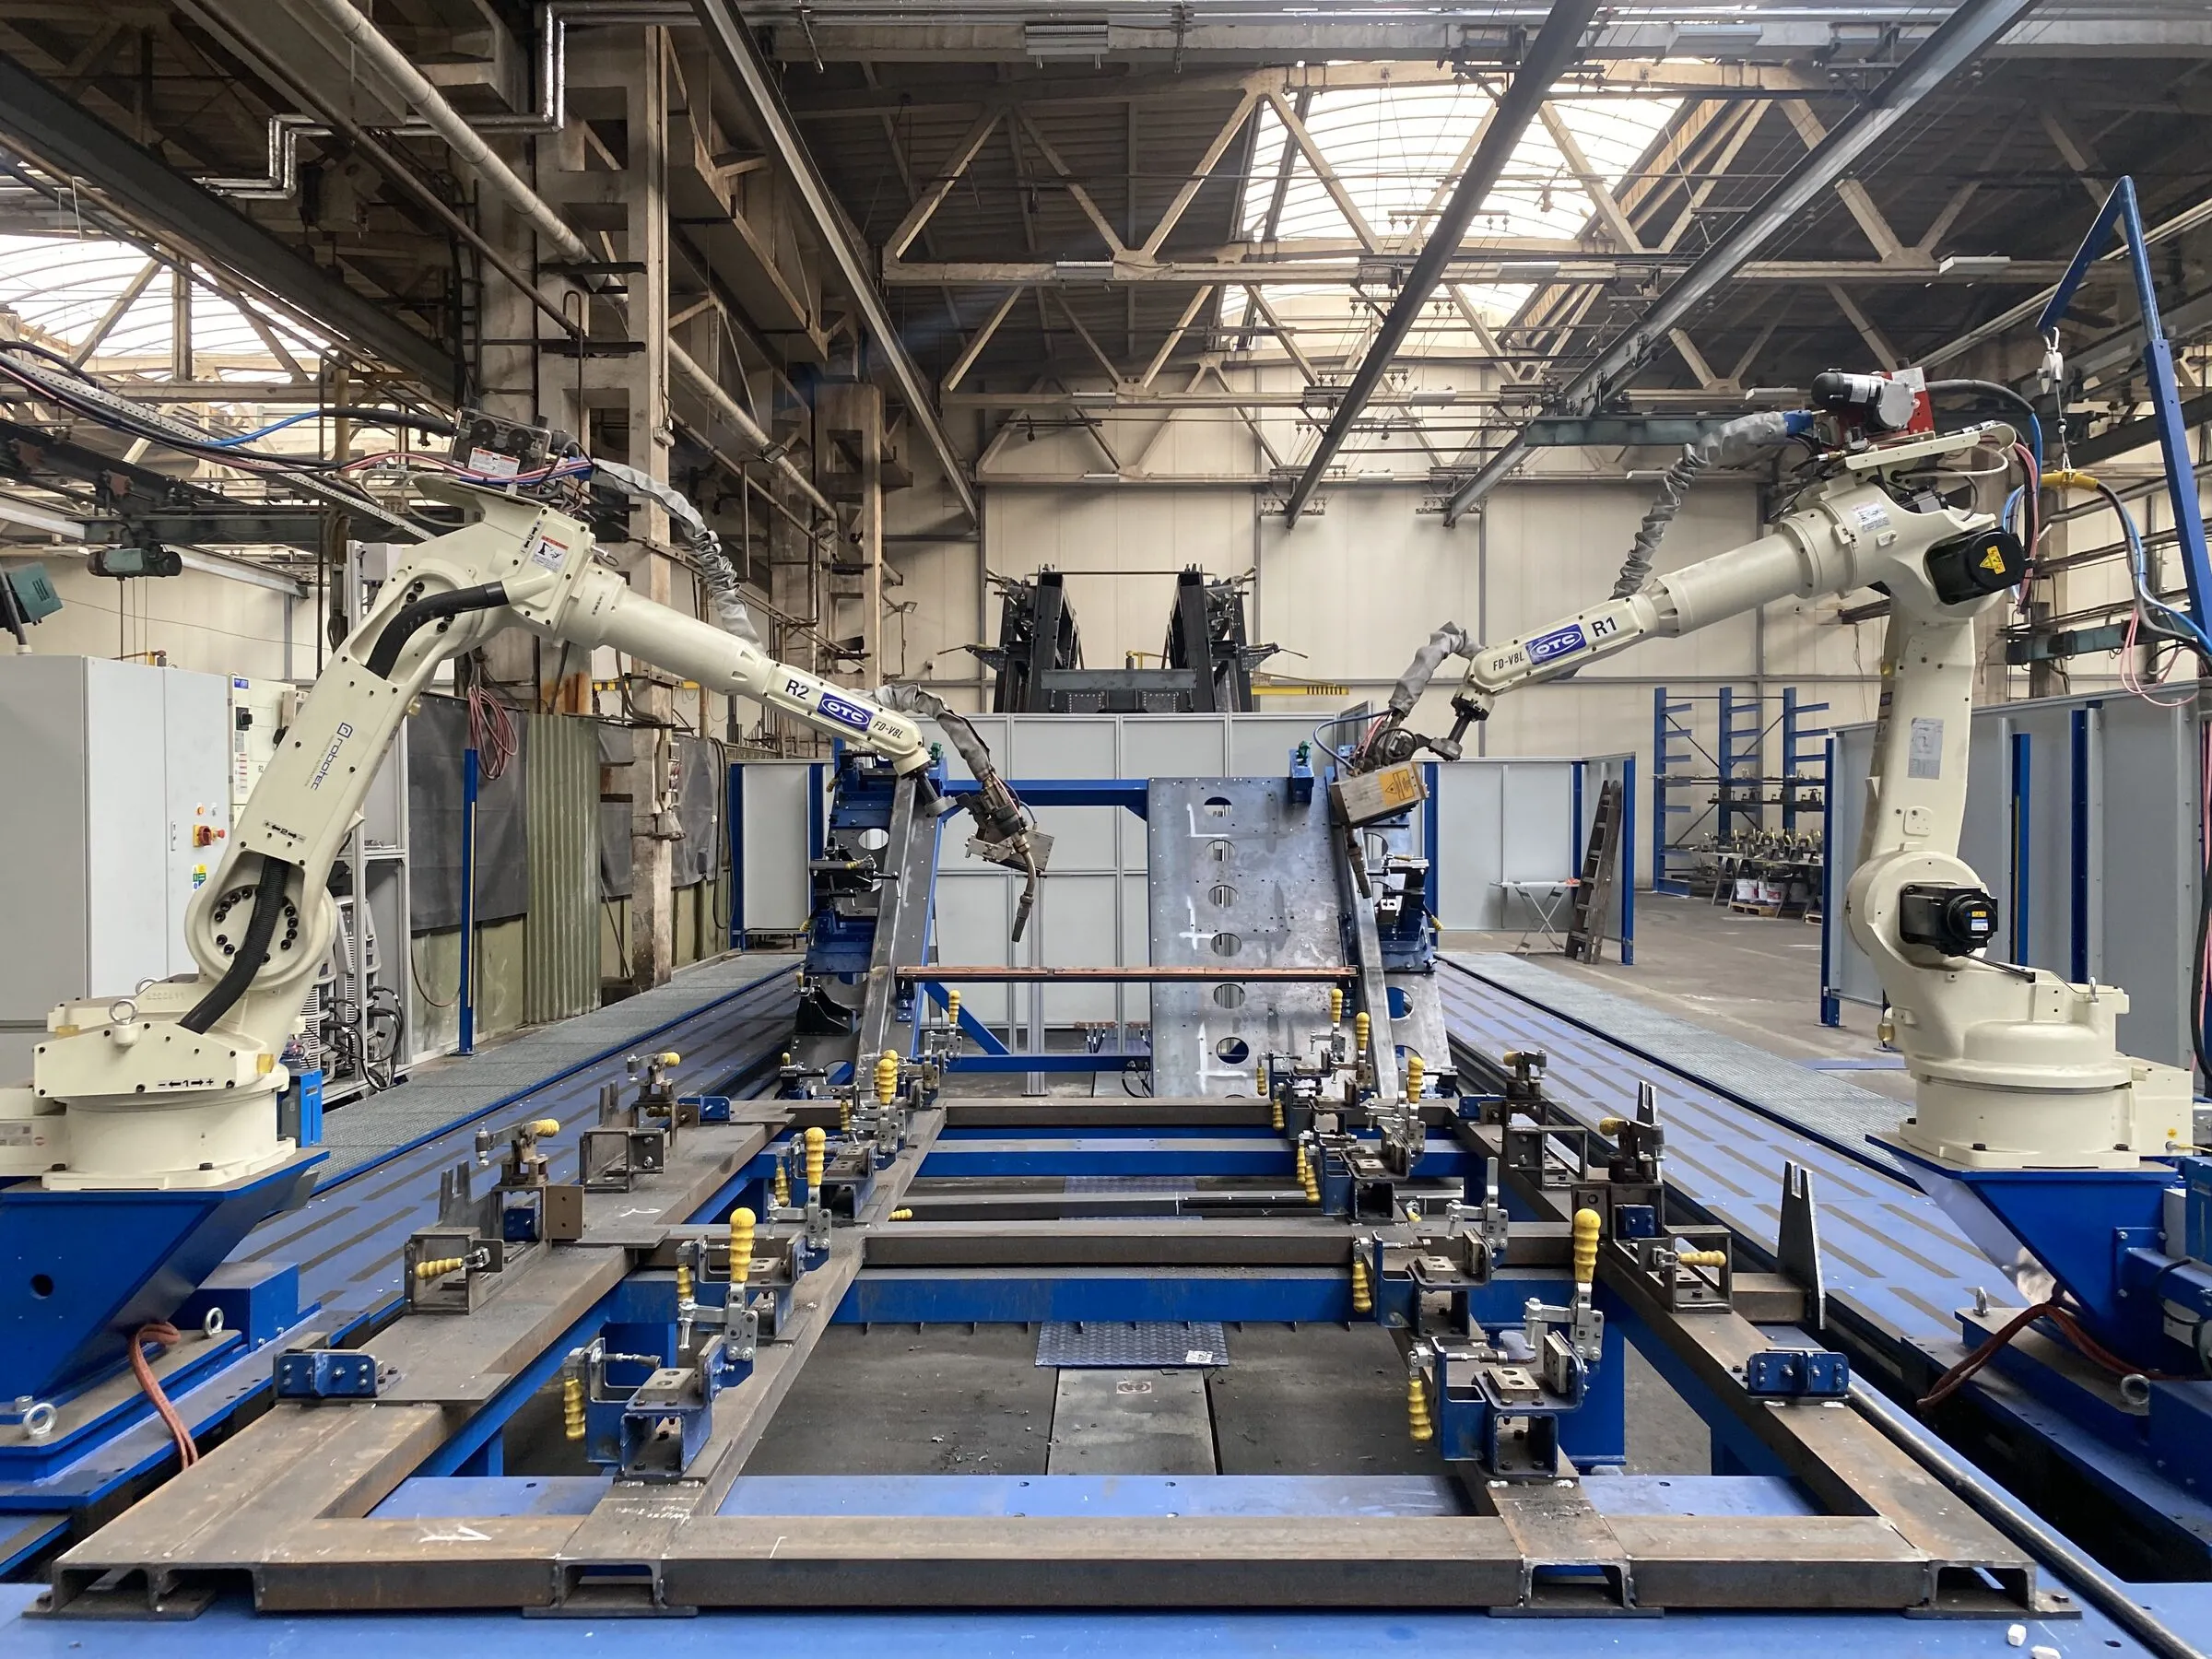
Robots and fixture table seen from the side 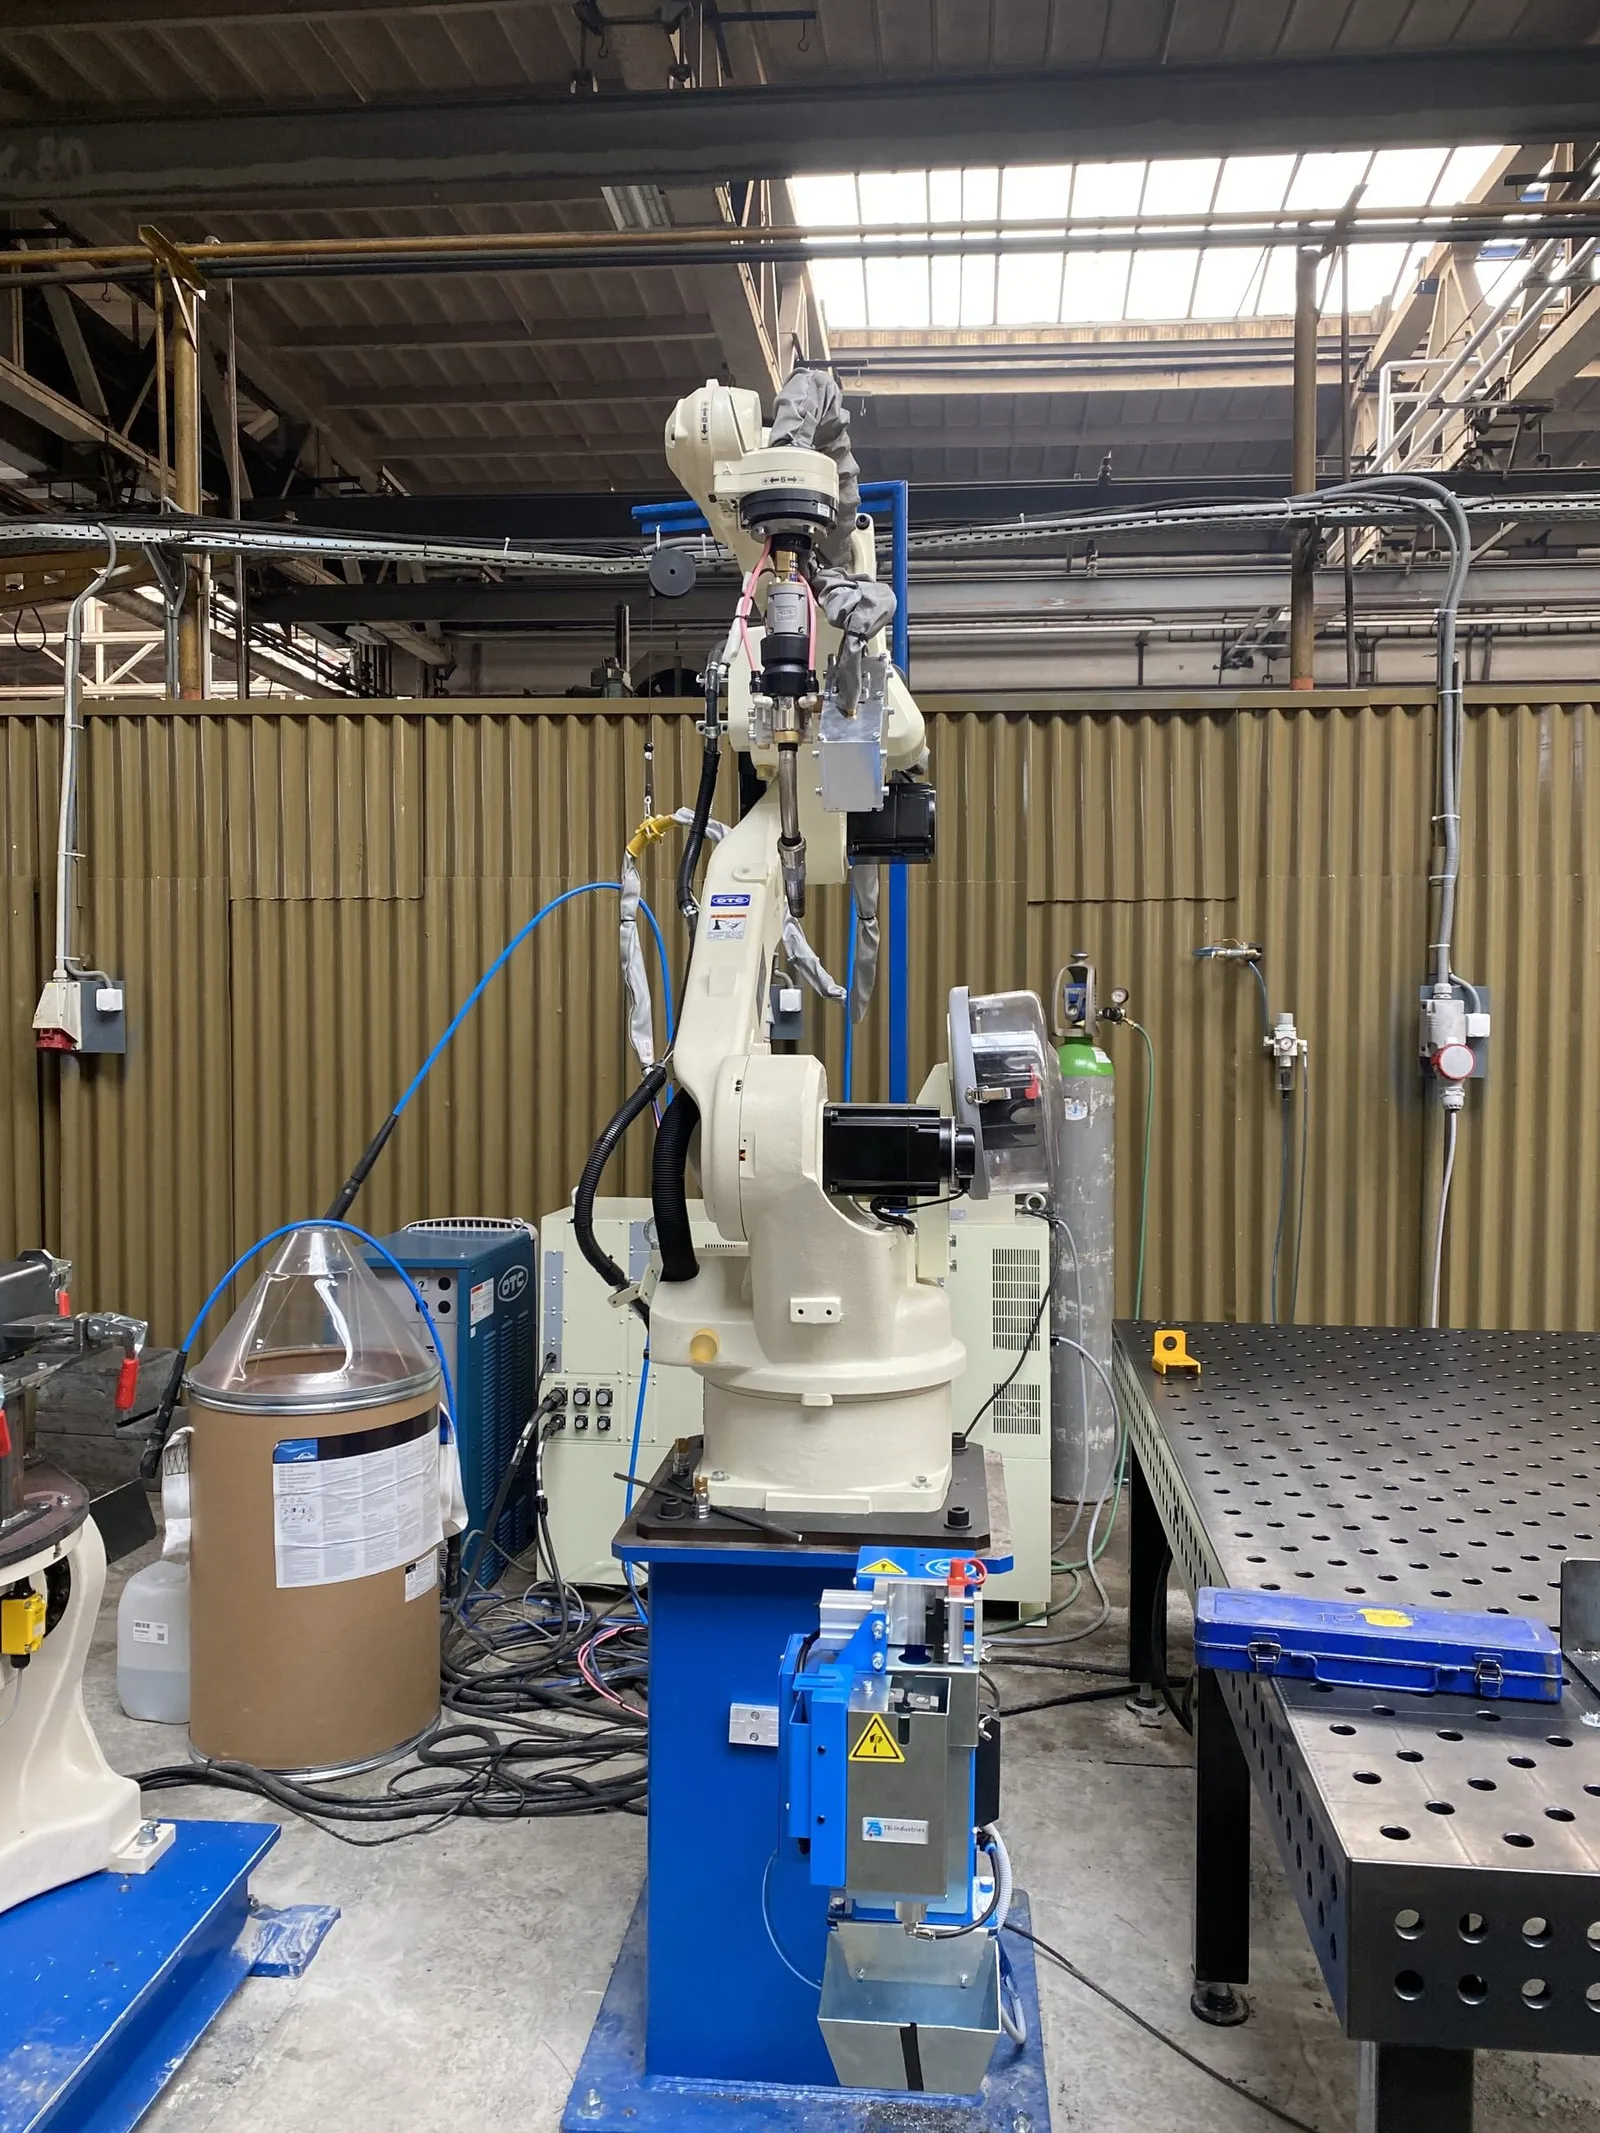
Six-axis welding robot on a blue base, torch pointing down 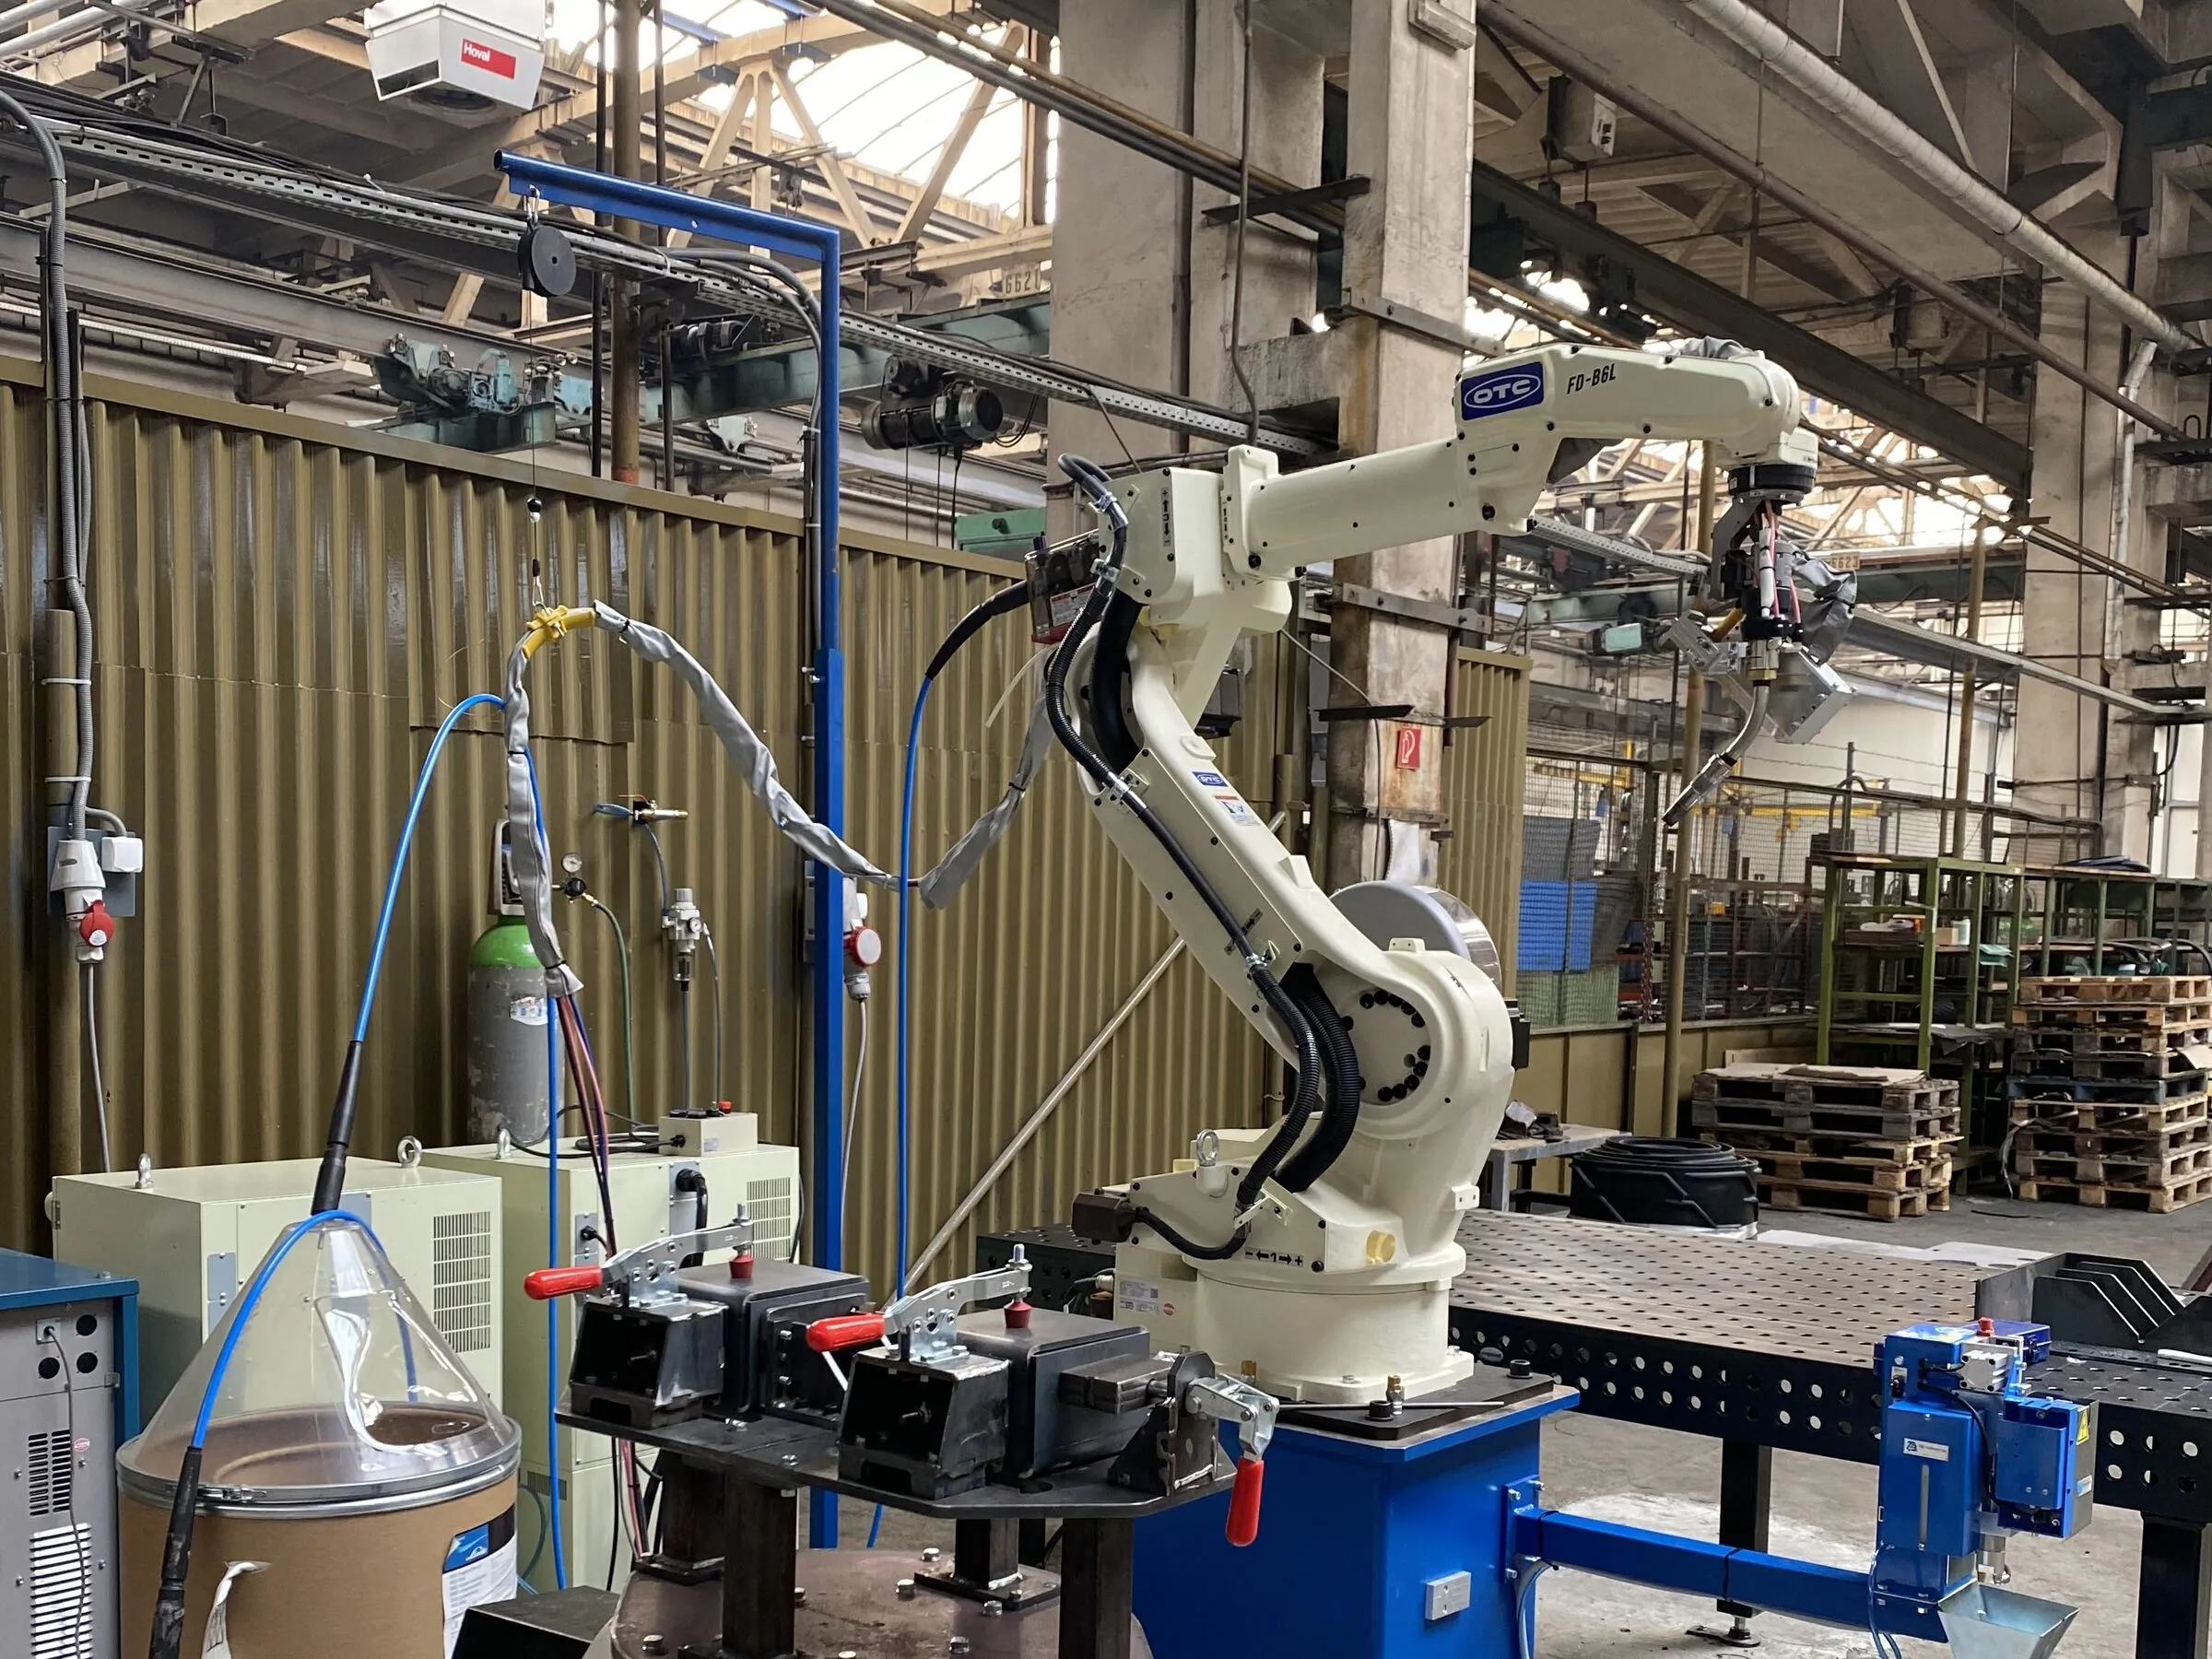
Robot arm with torch over the welding table, ochre screens 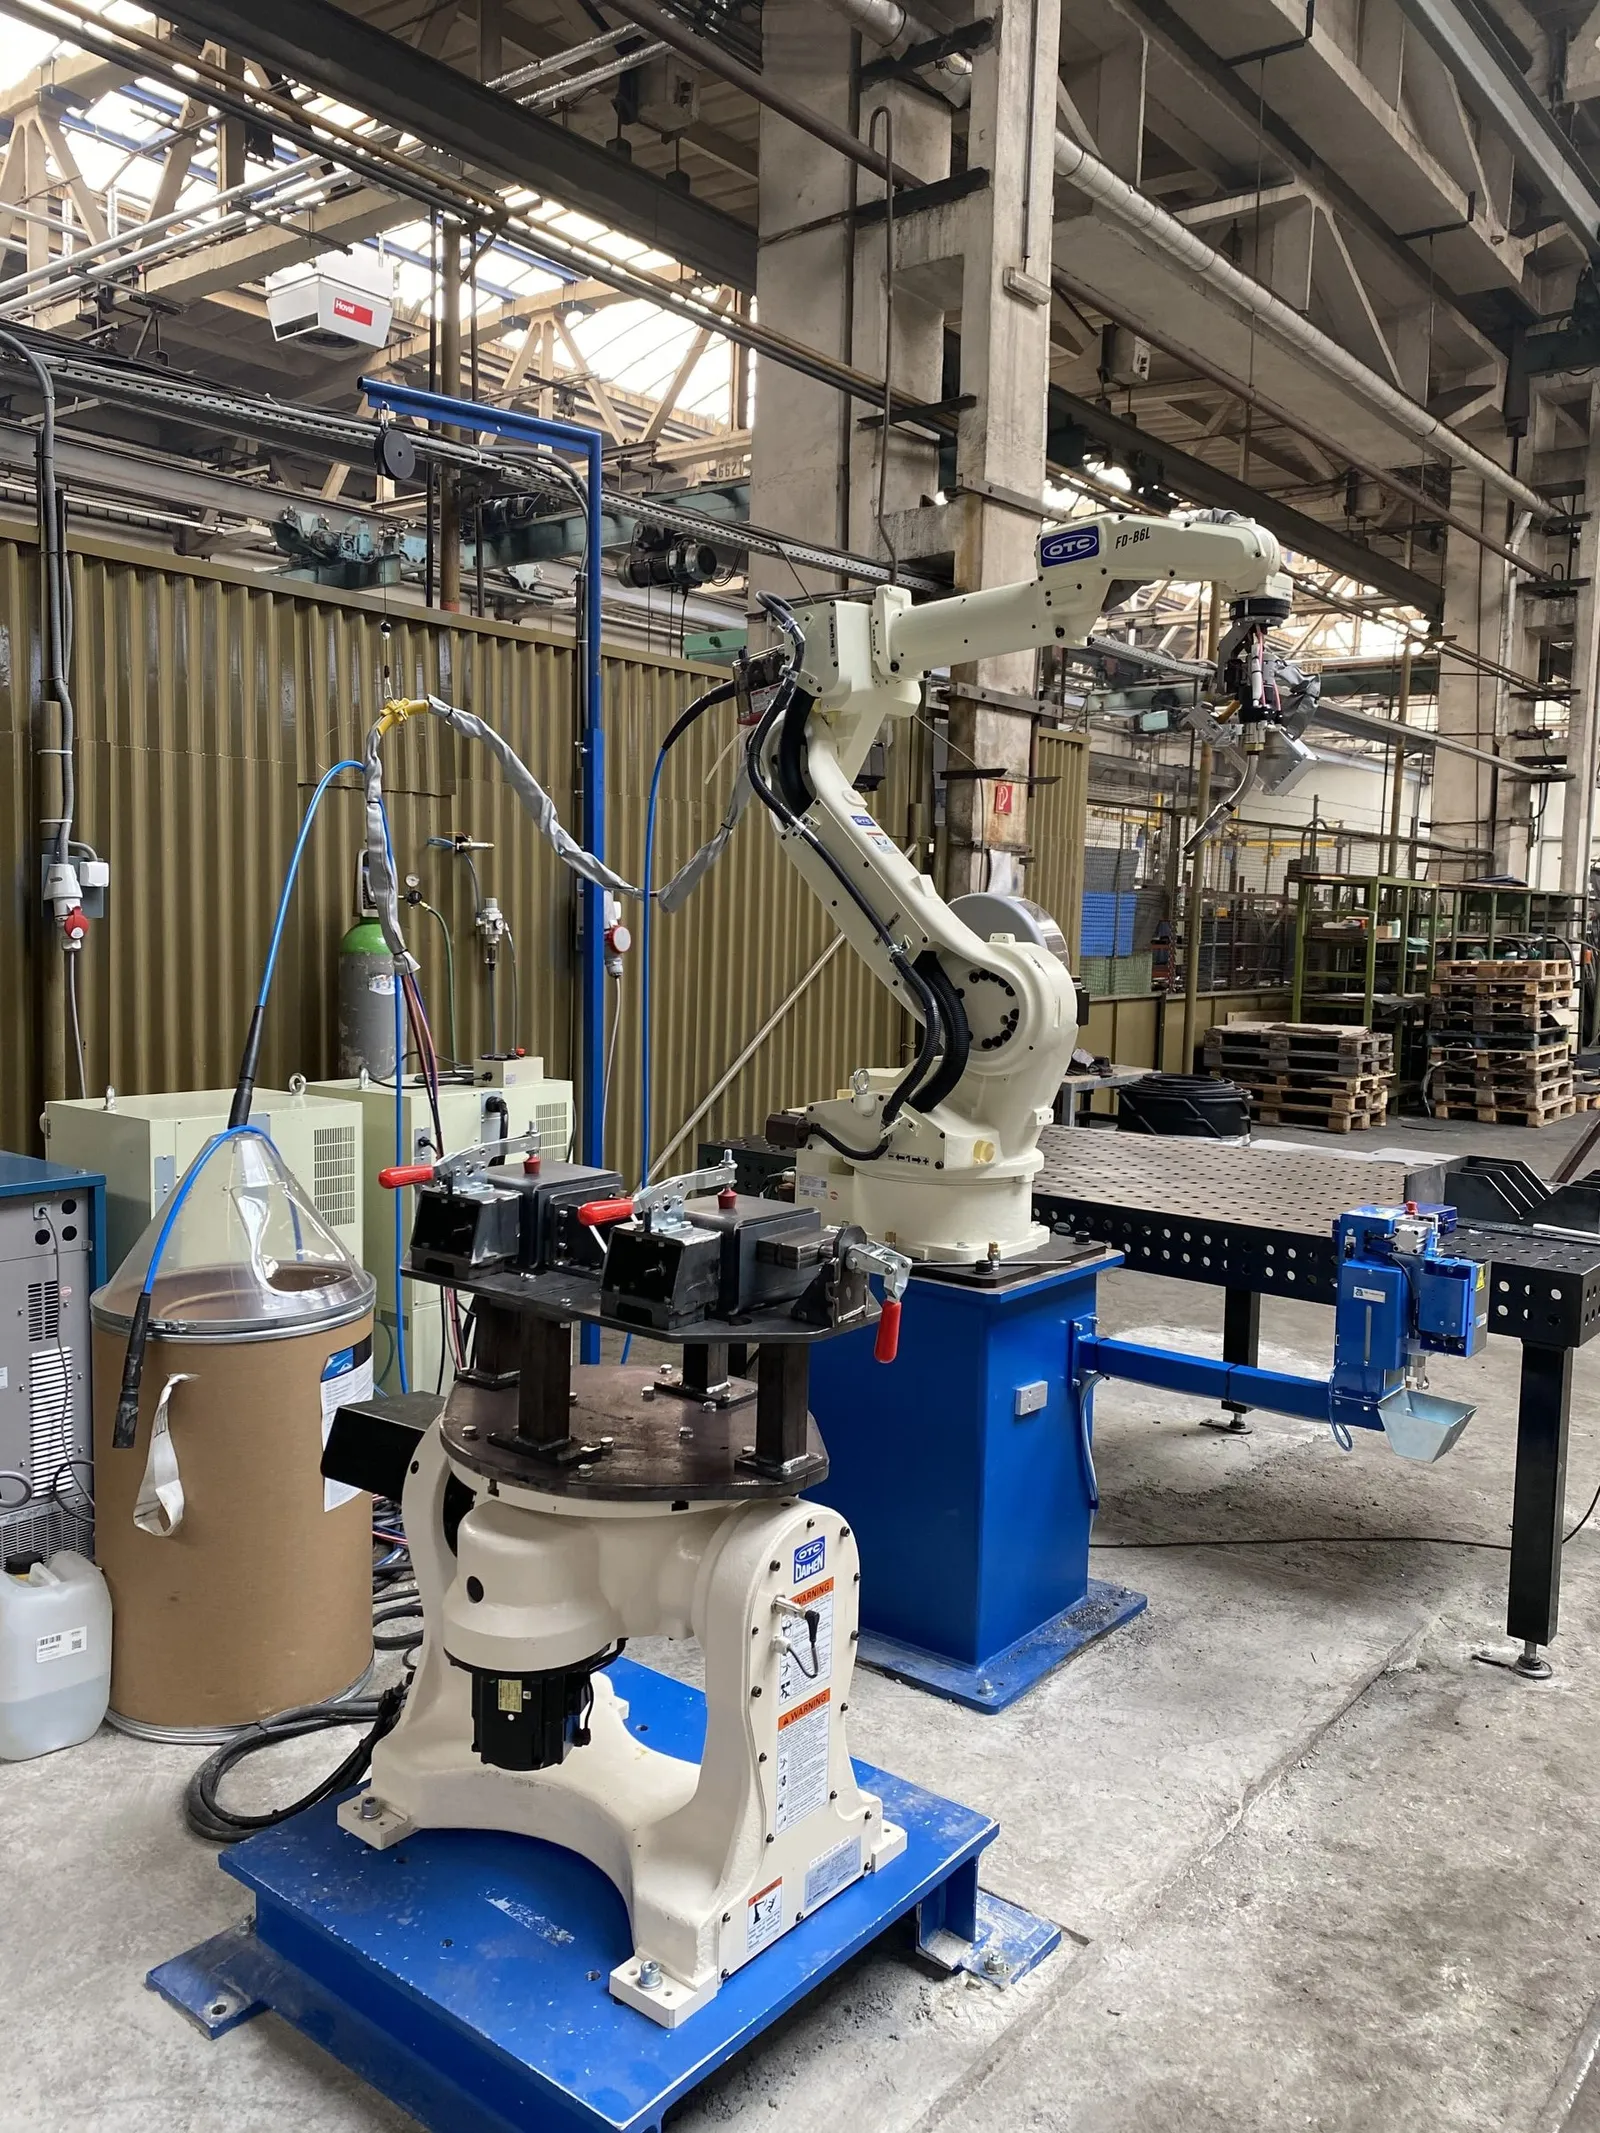
Welding robot with wire feeder and torch, blue base 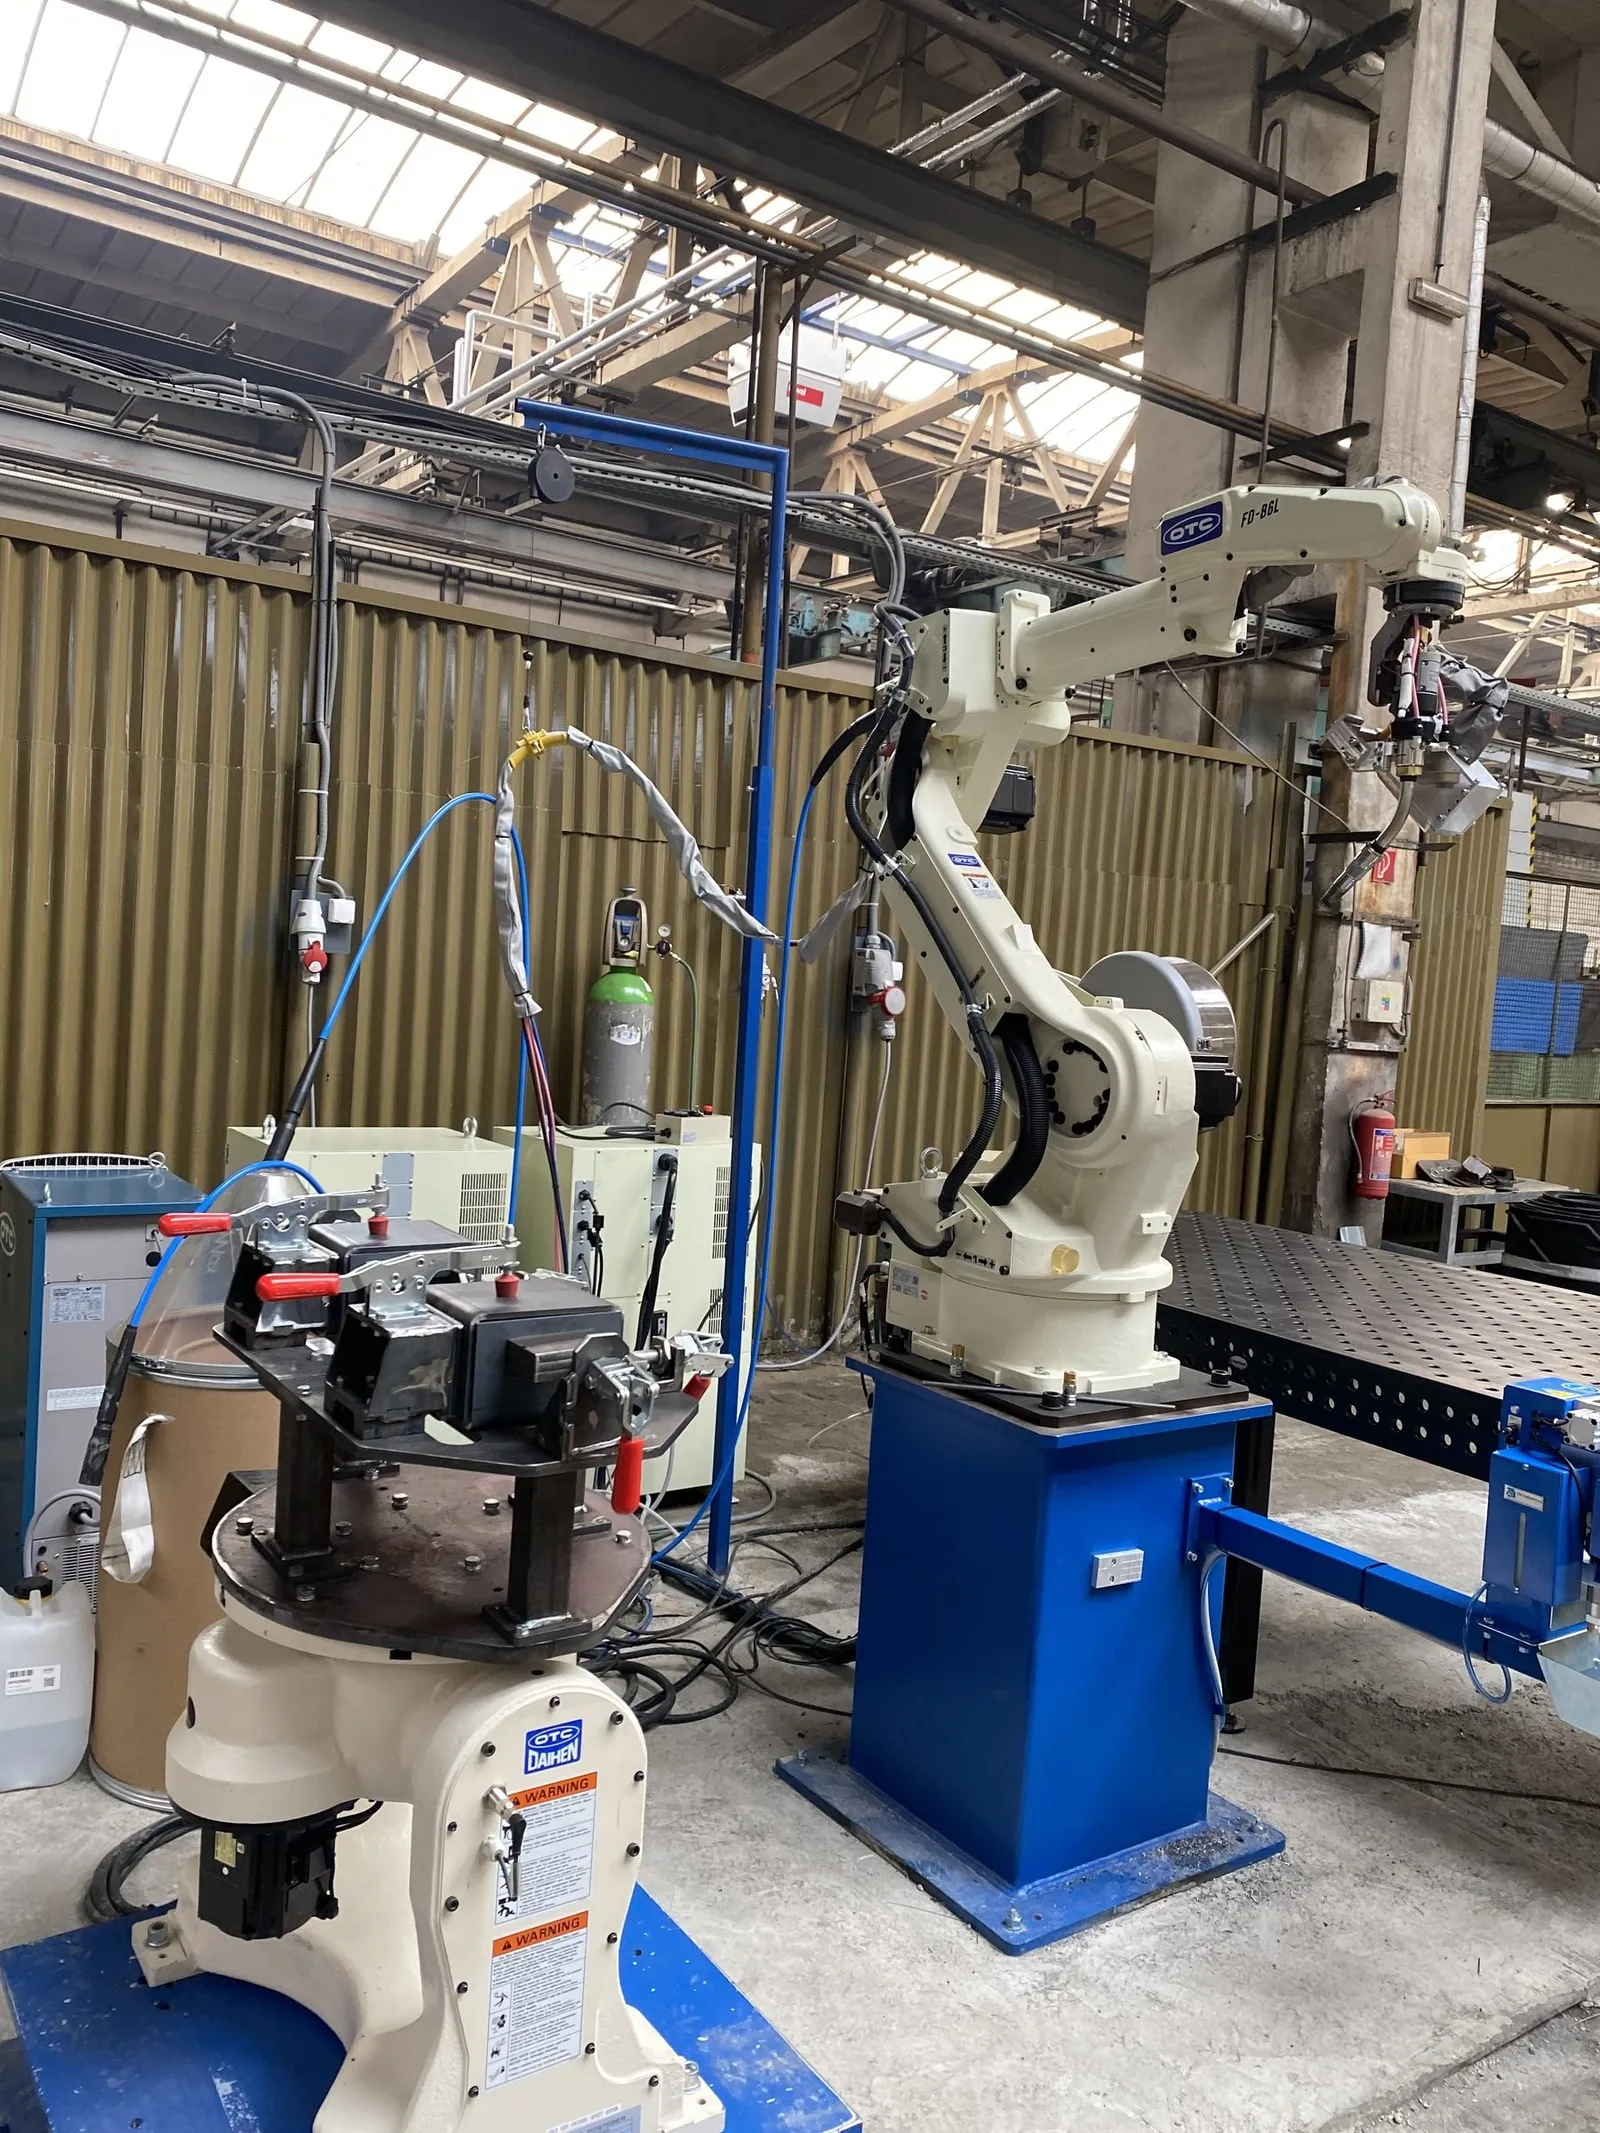
Robot at the fixture with protective screens around it
Machine shop
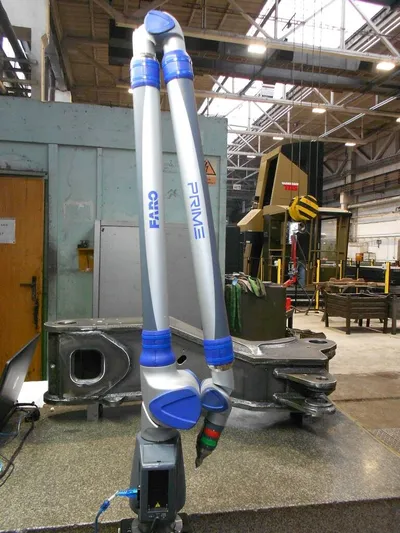
Six-axis 3D measuring arm in the hall 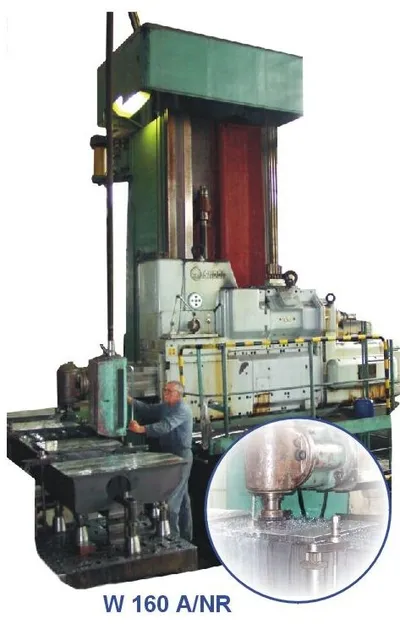
Horizontal boring machine W 160 A/NR, catalogue view 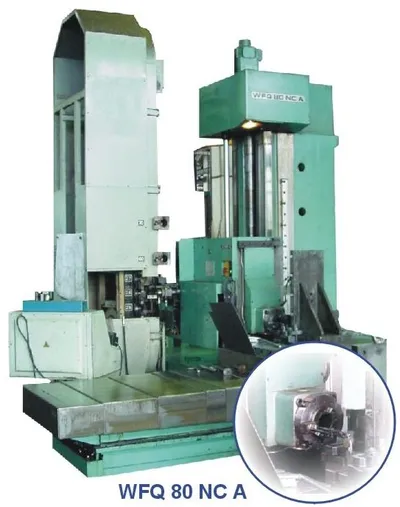
Horizontal boring and milling machine WFQ 80 NC A, catalogue view 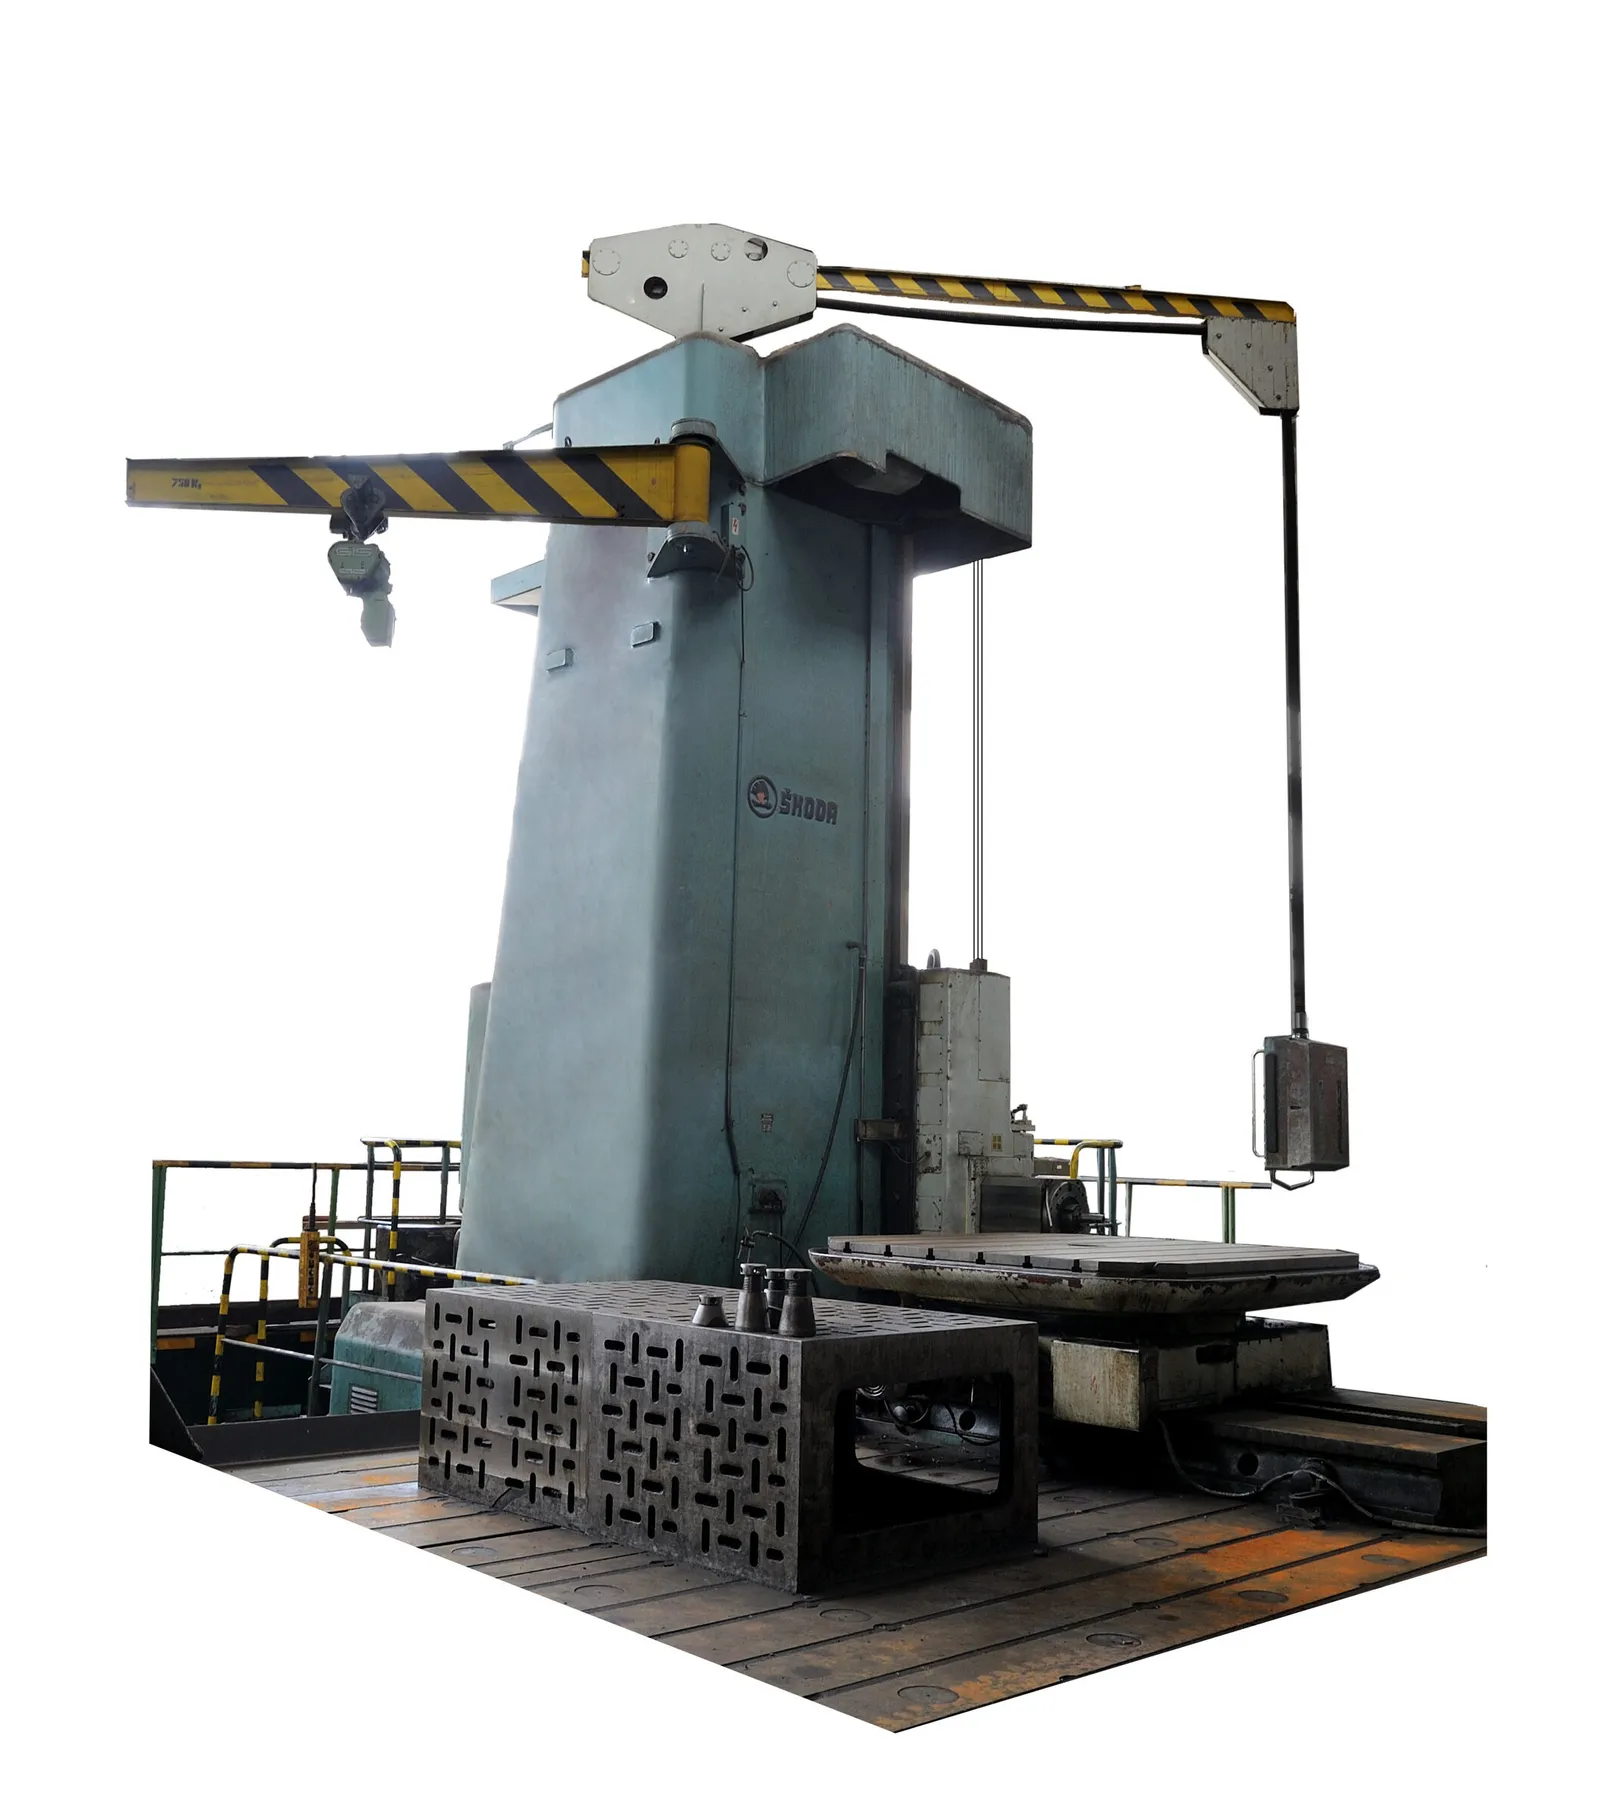
Large horizontal boring machine with rotary table and a jib crane 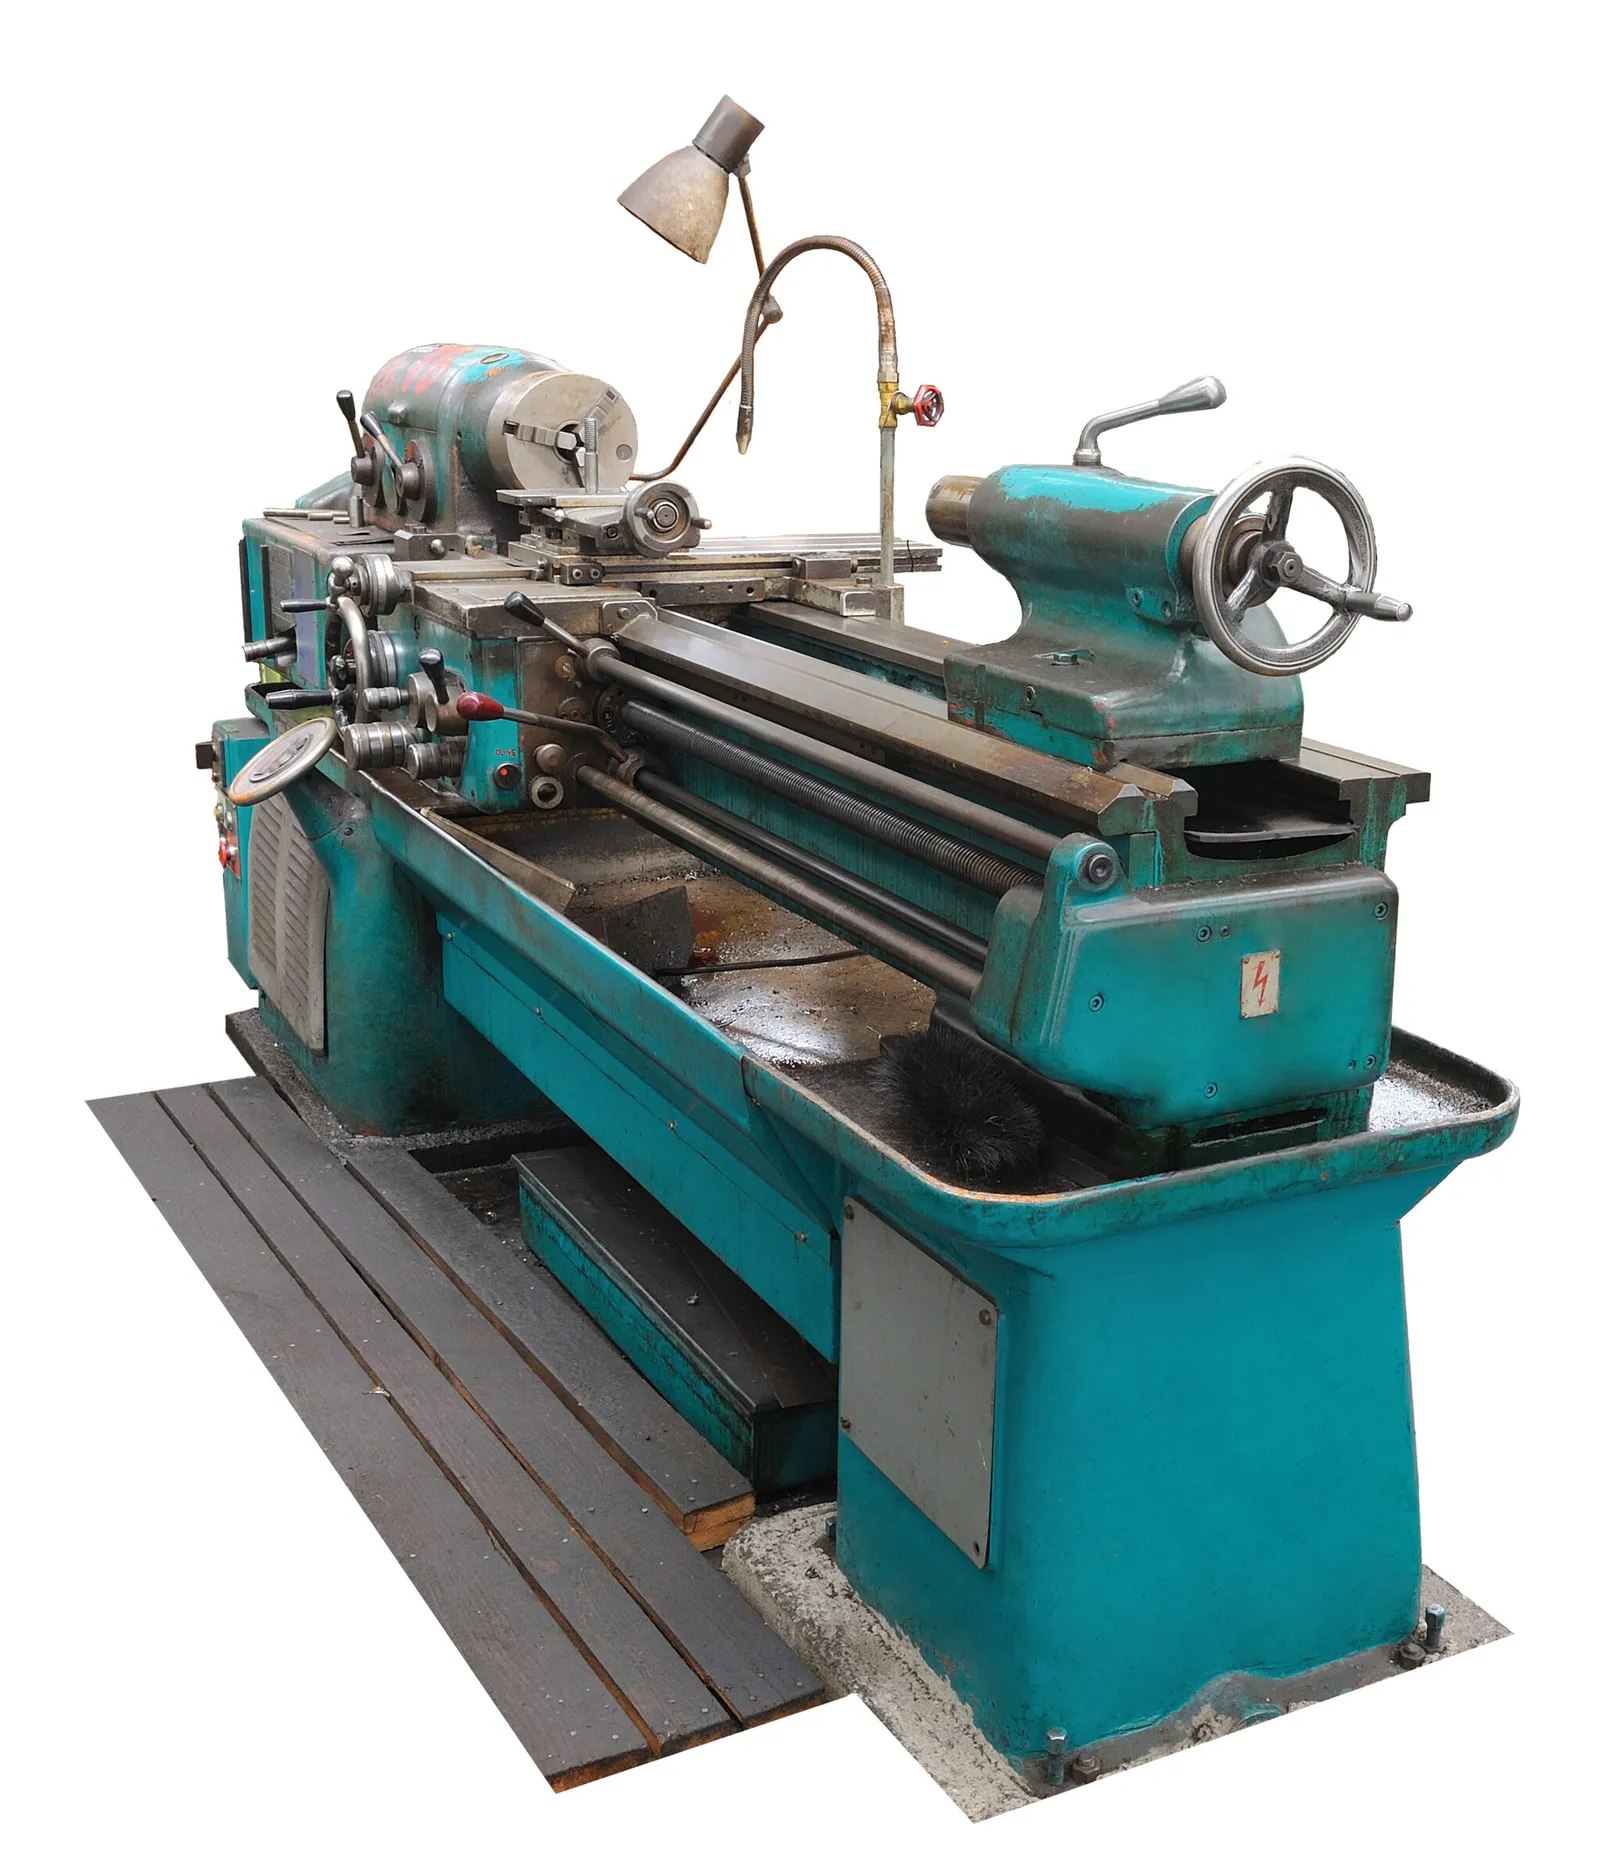
Centre lathe with chuck and carriage 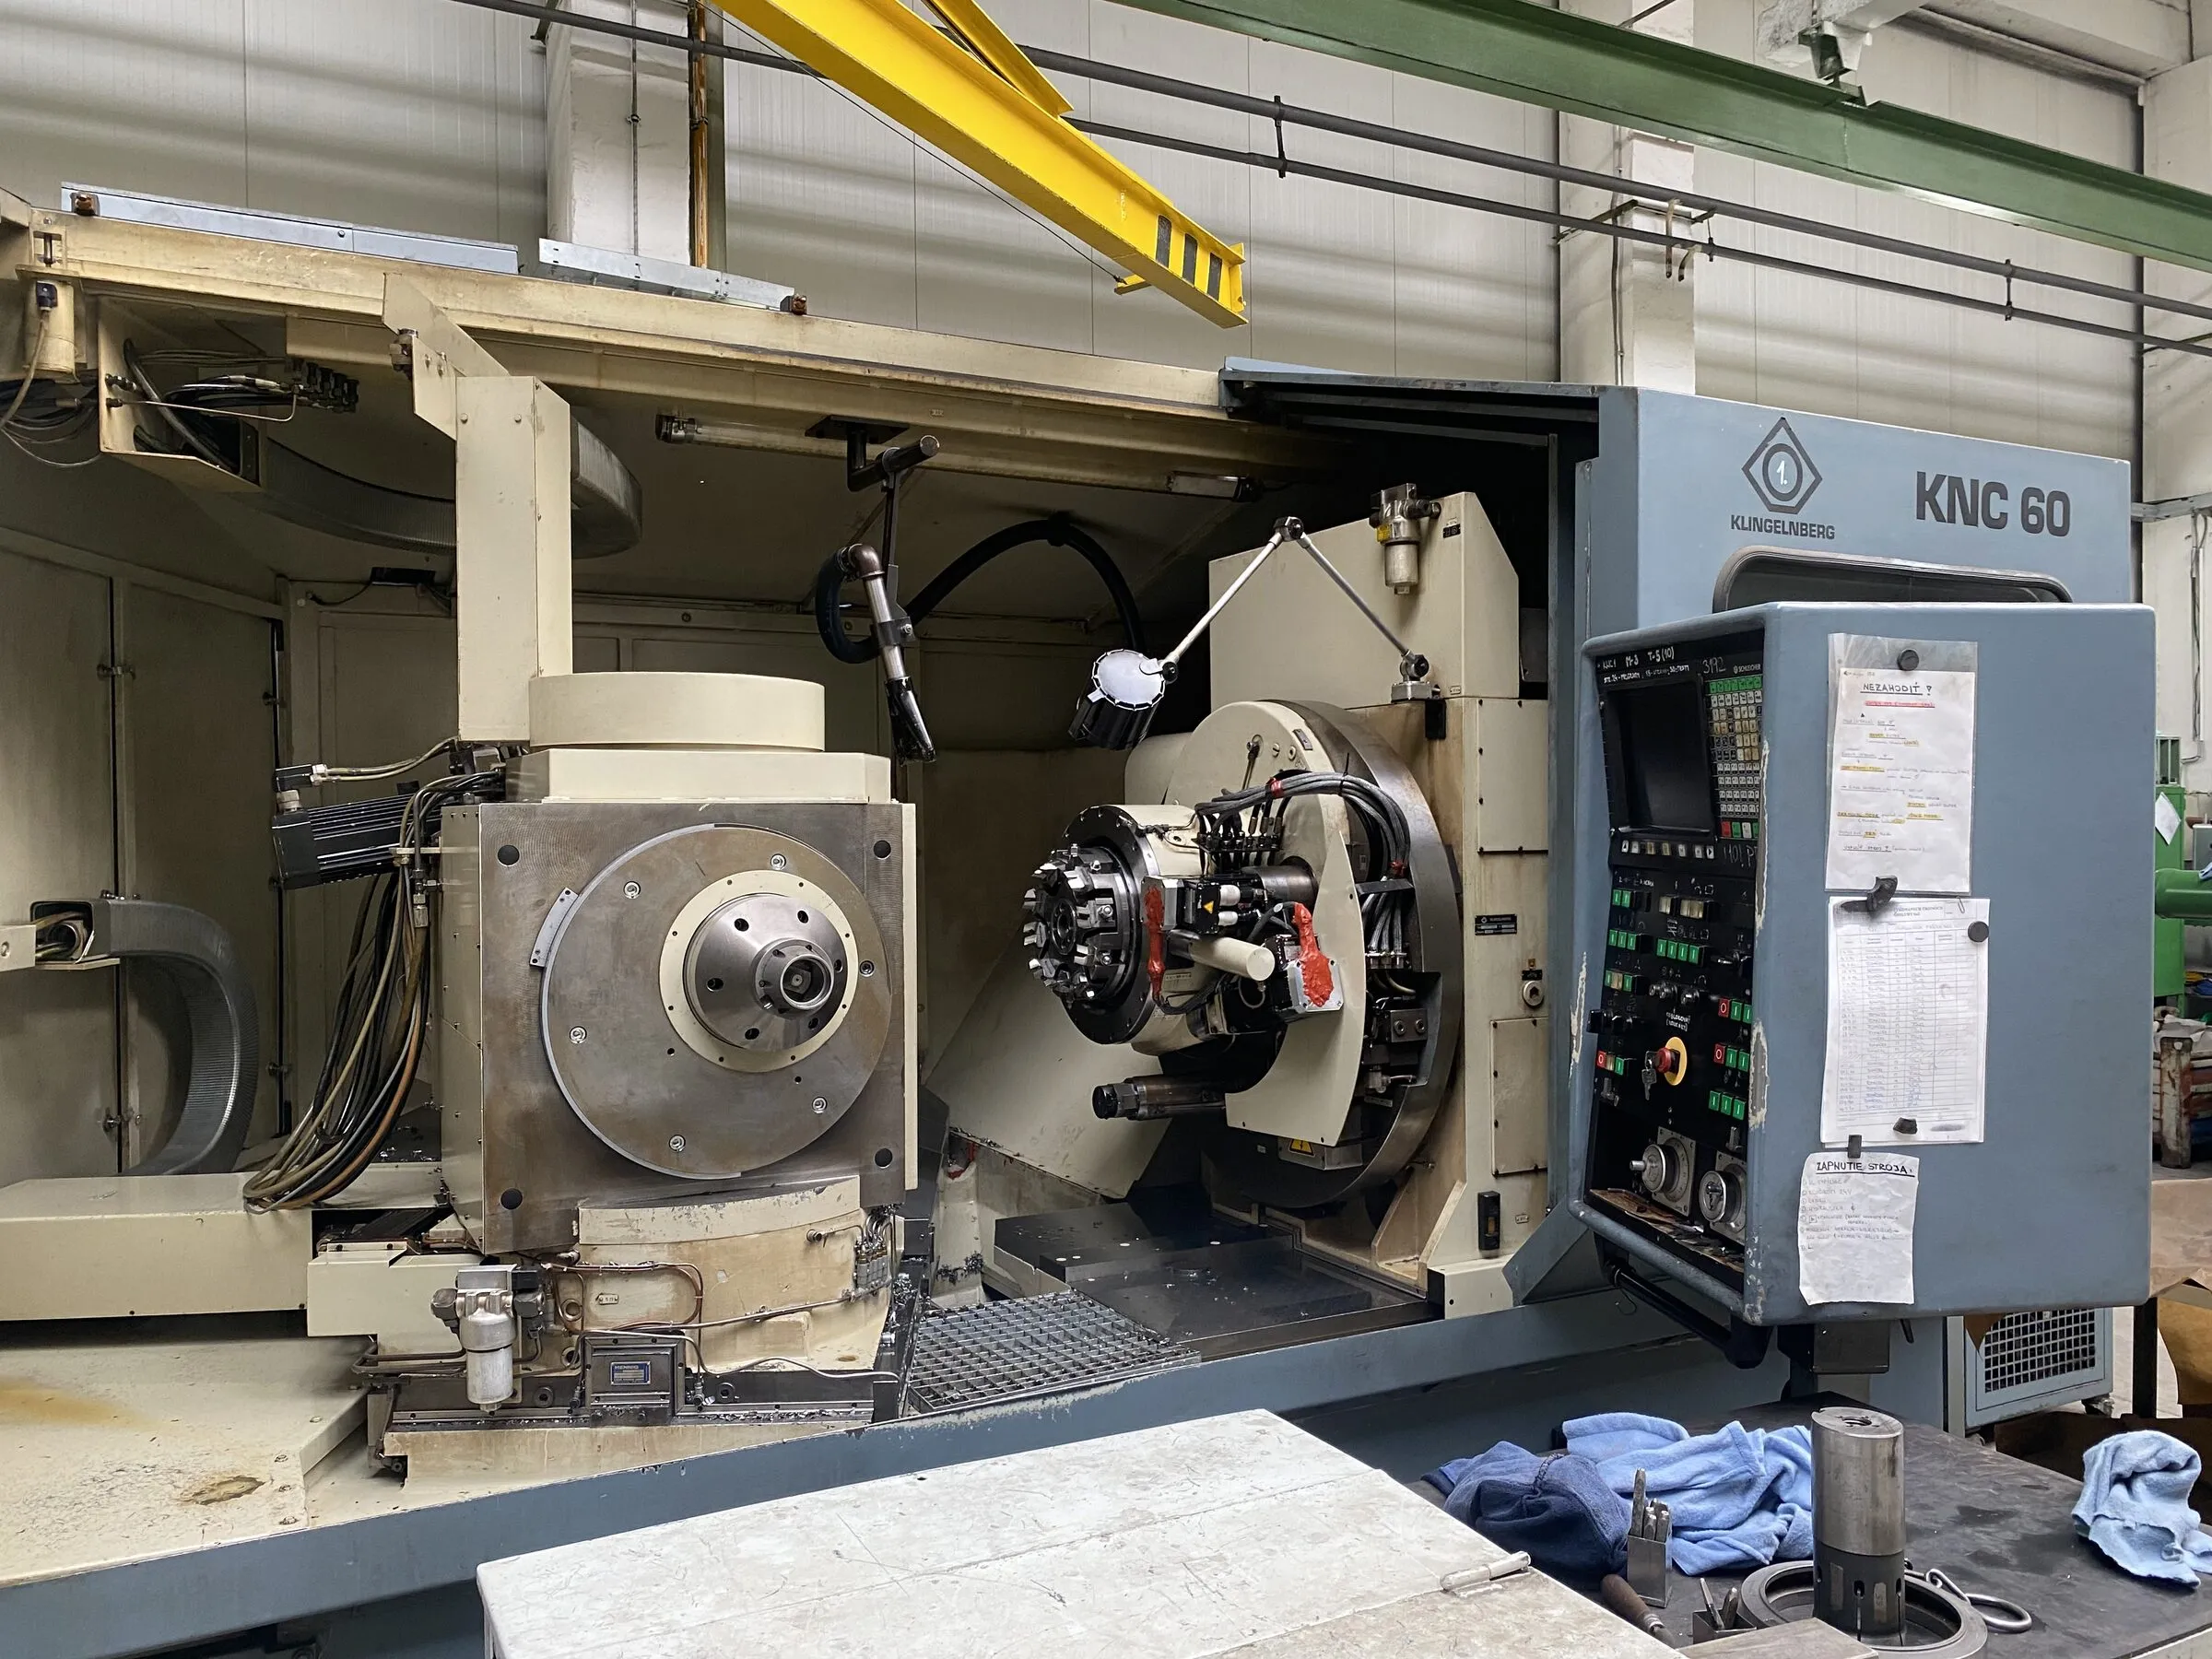
CNC lathe work area, chuck and turret 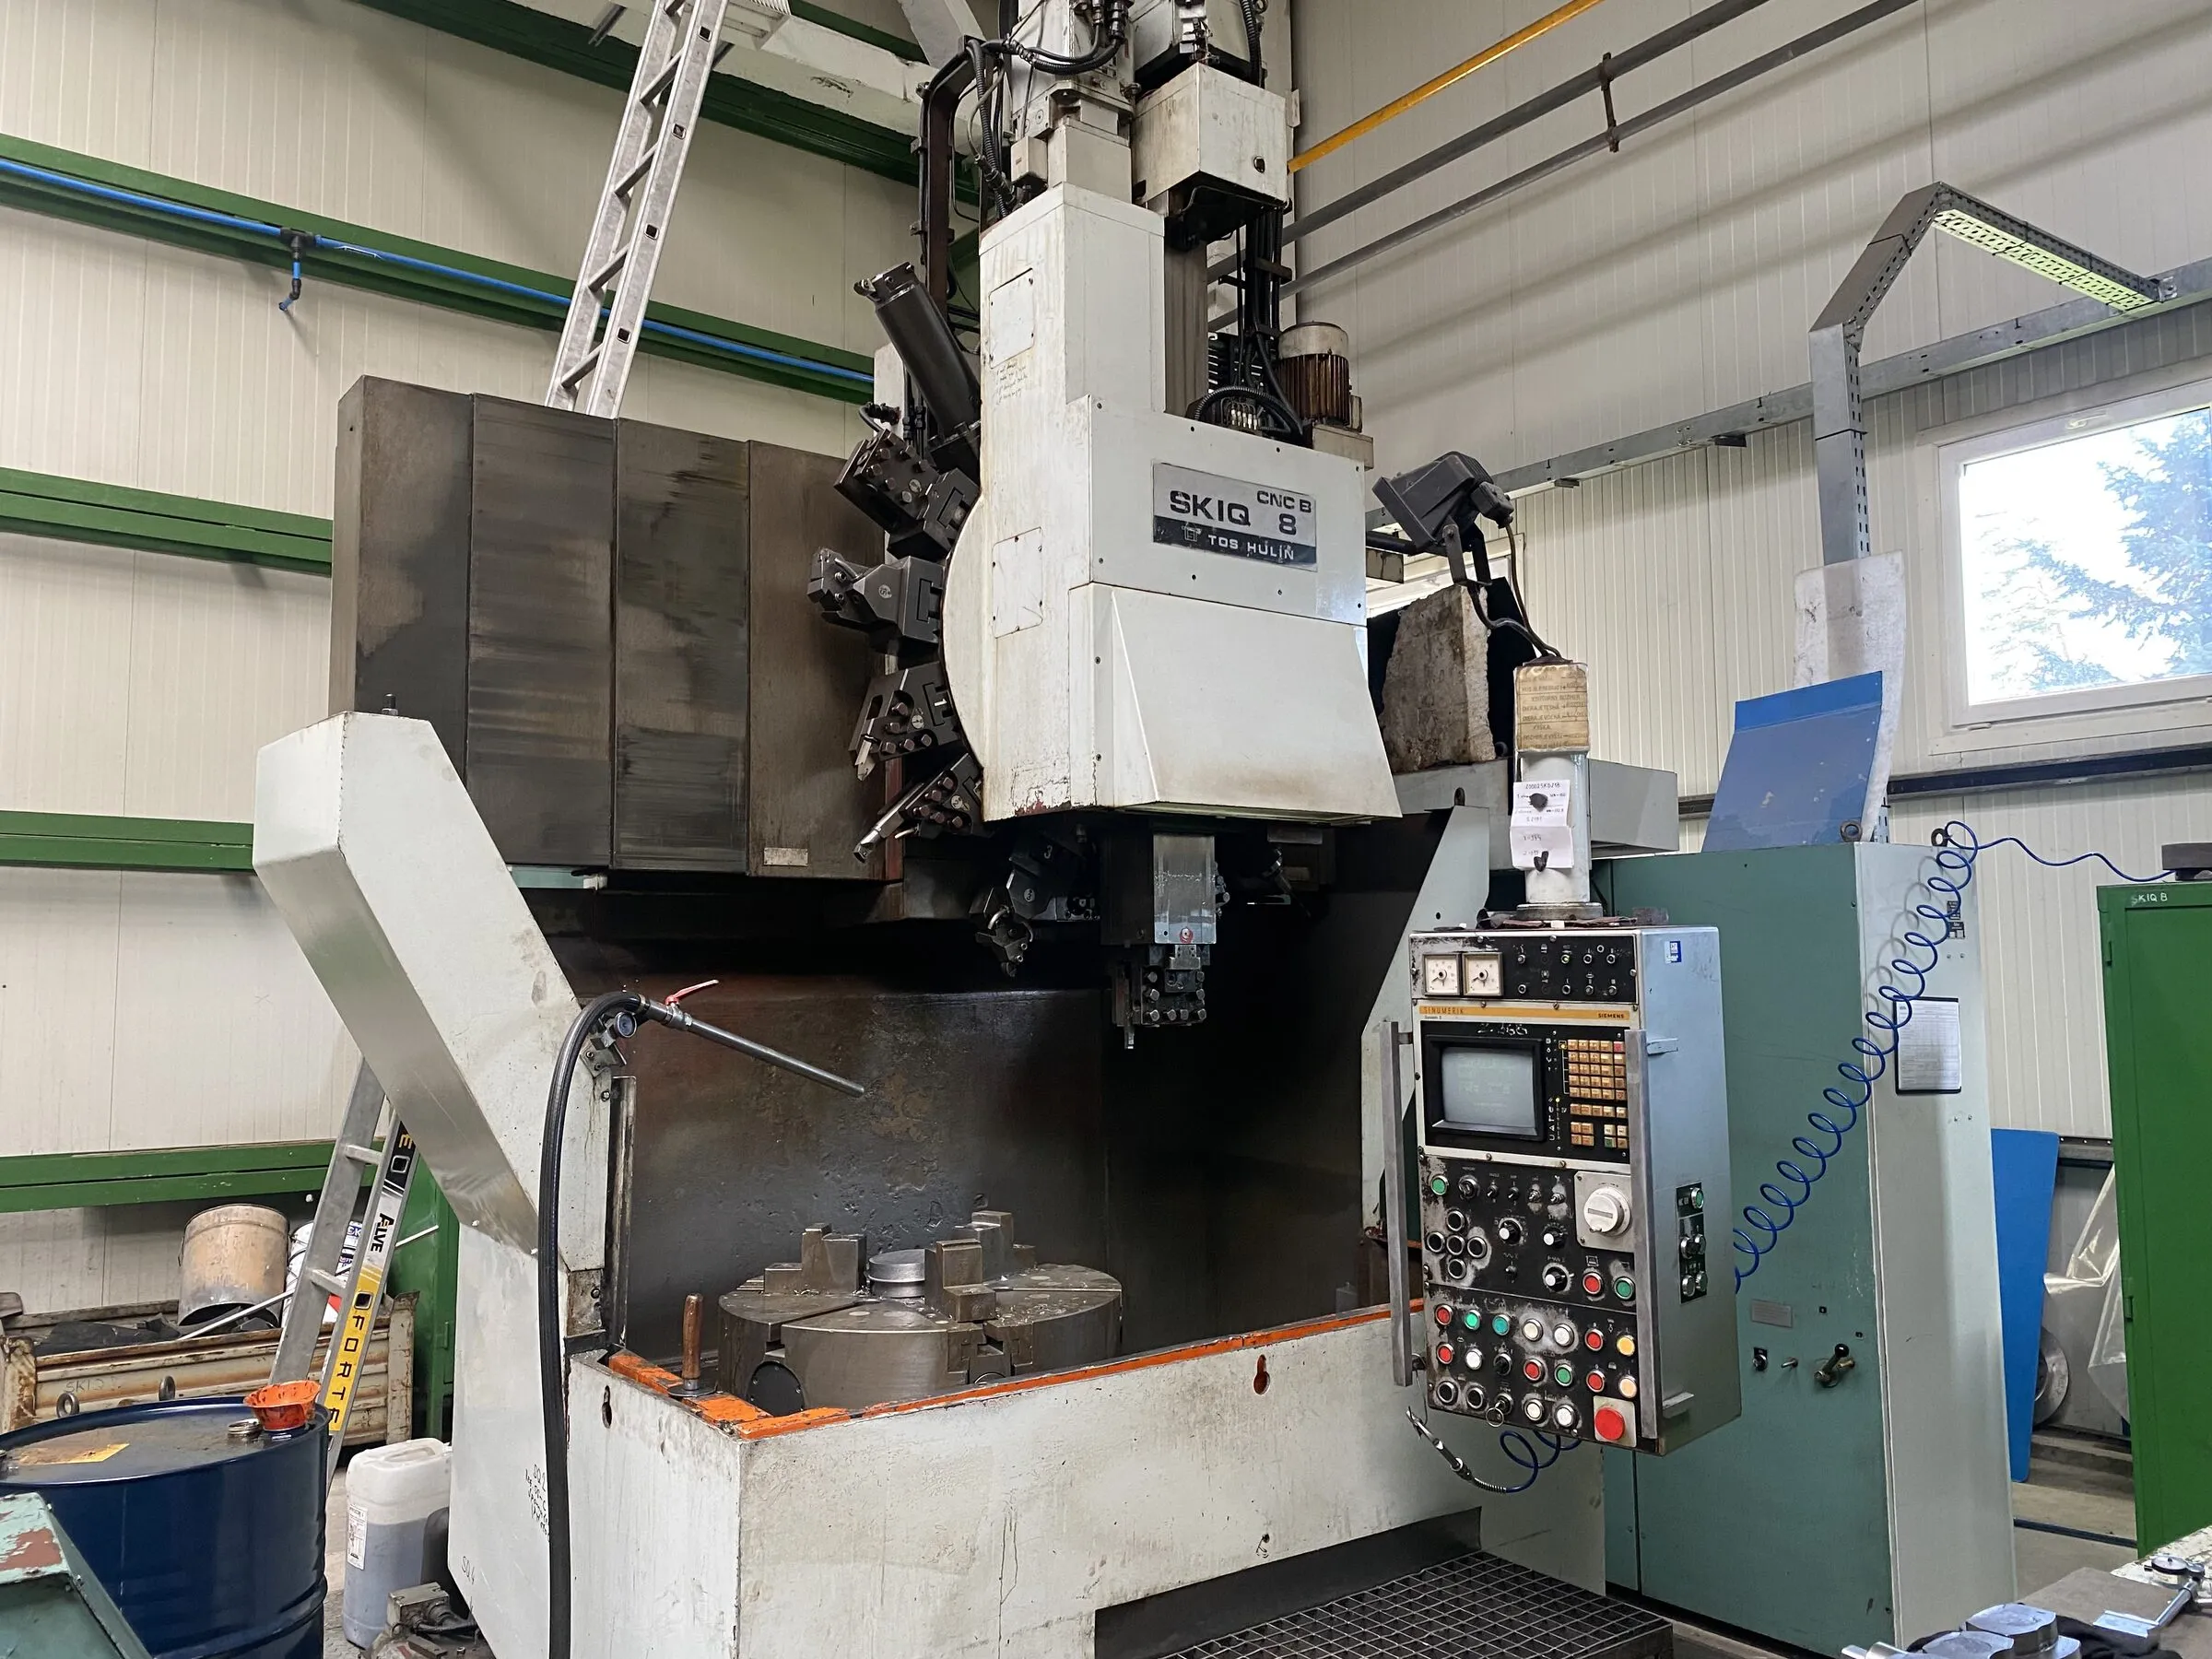
CNC machining centre with a gantry, view into the work area 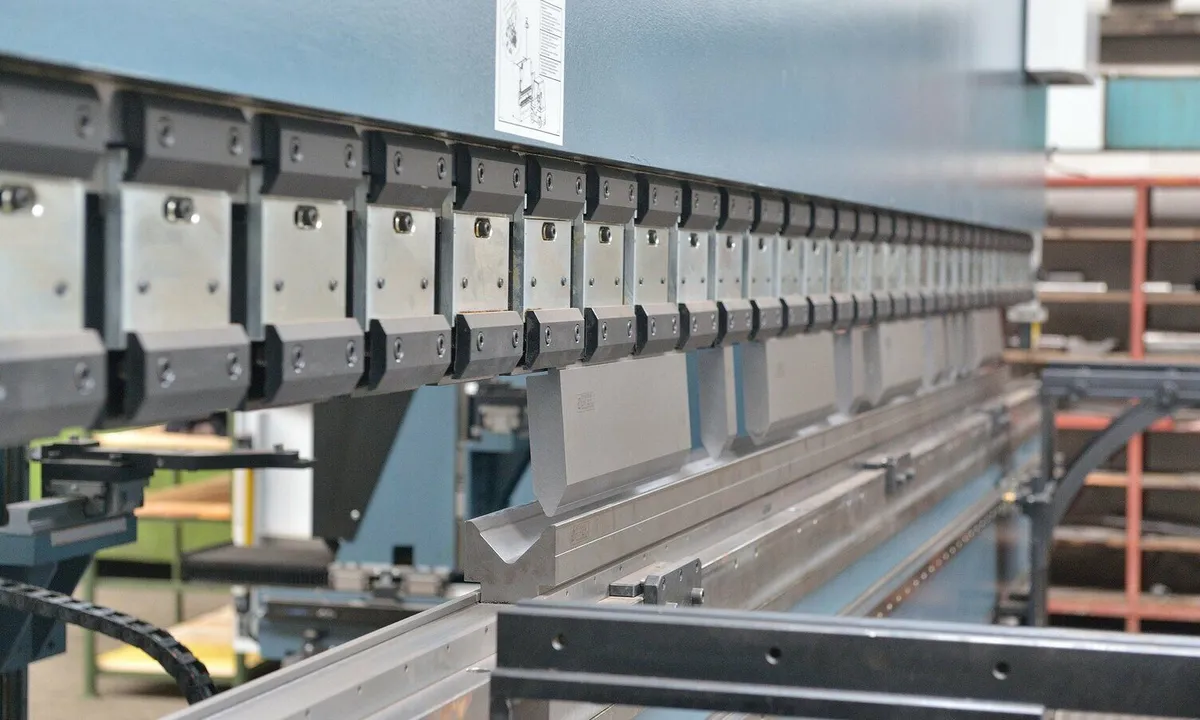
Press brake tooling along the long table
Conveyor systems
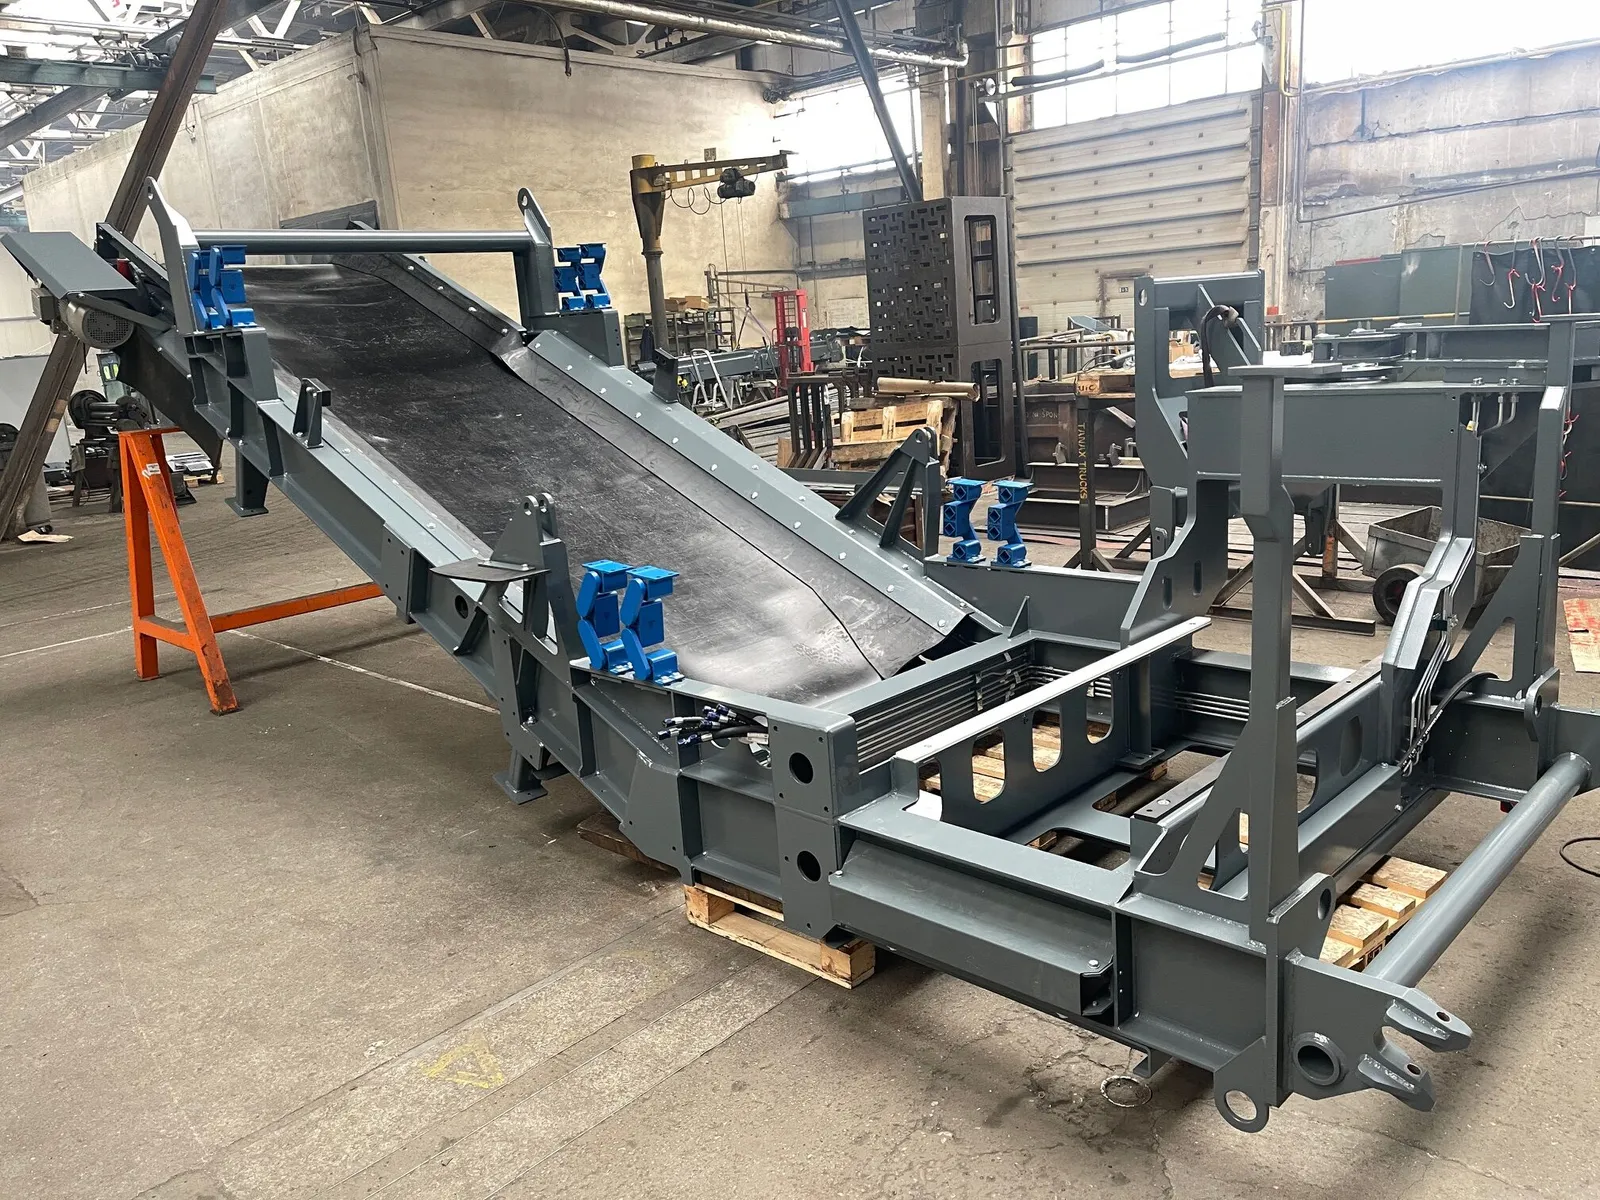
Belt conveyor with frame and belt assembled in the hall, wide view 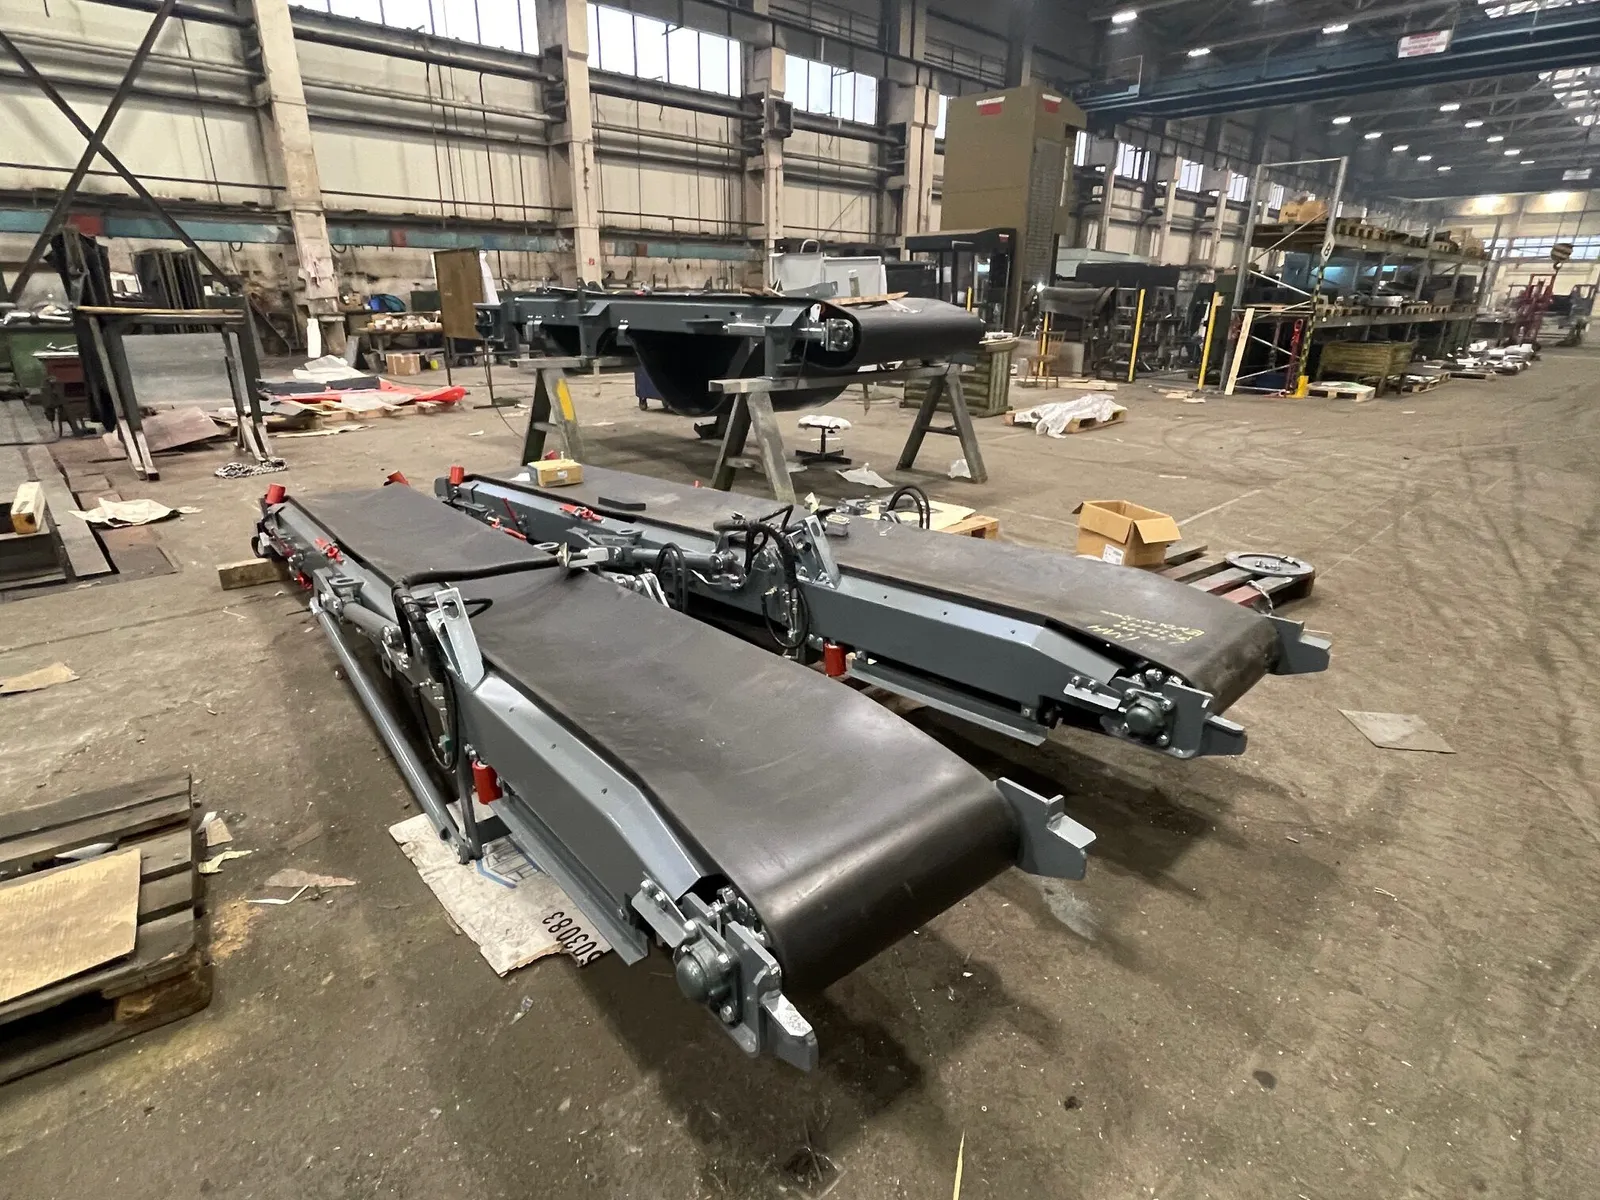
Assembled belt conveyor, side view 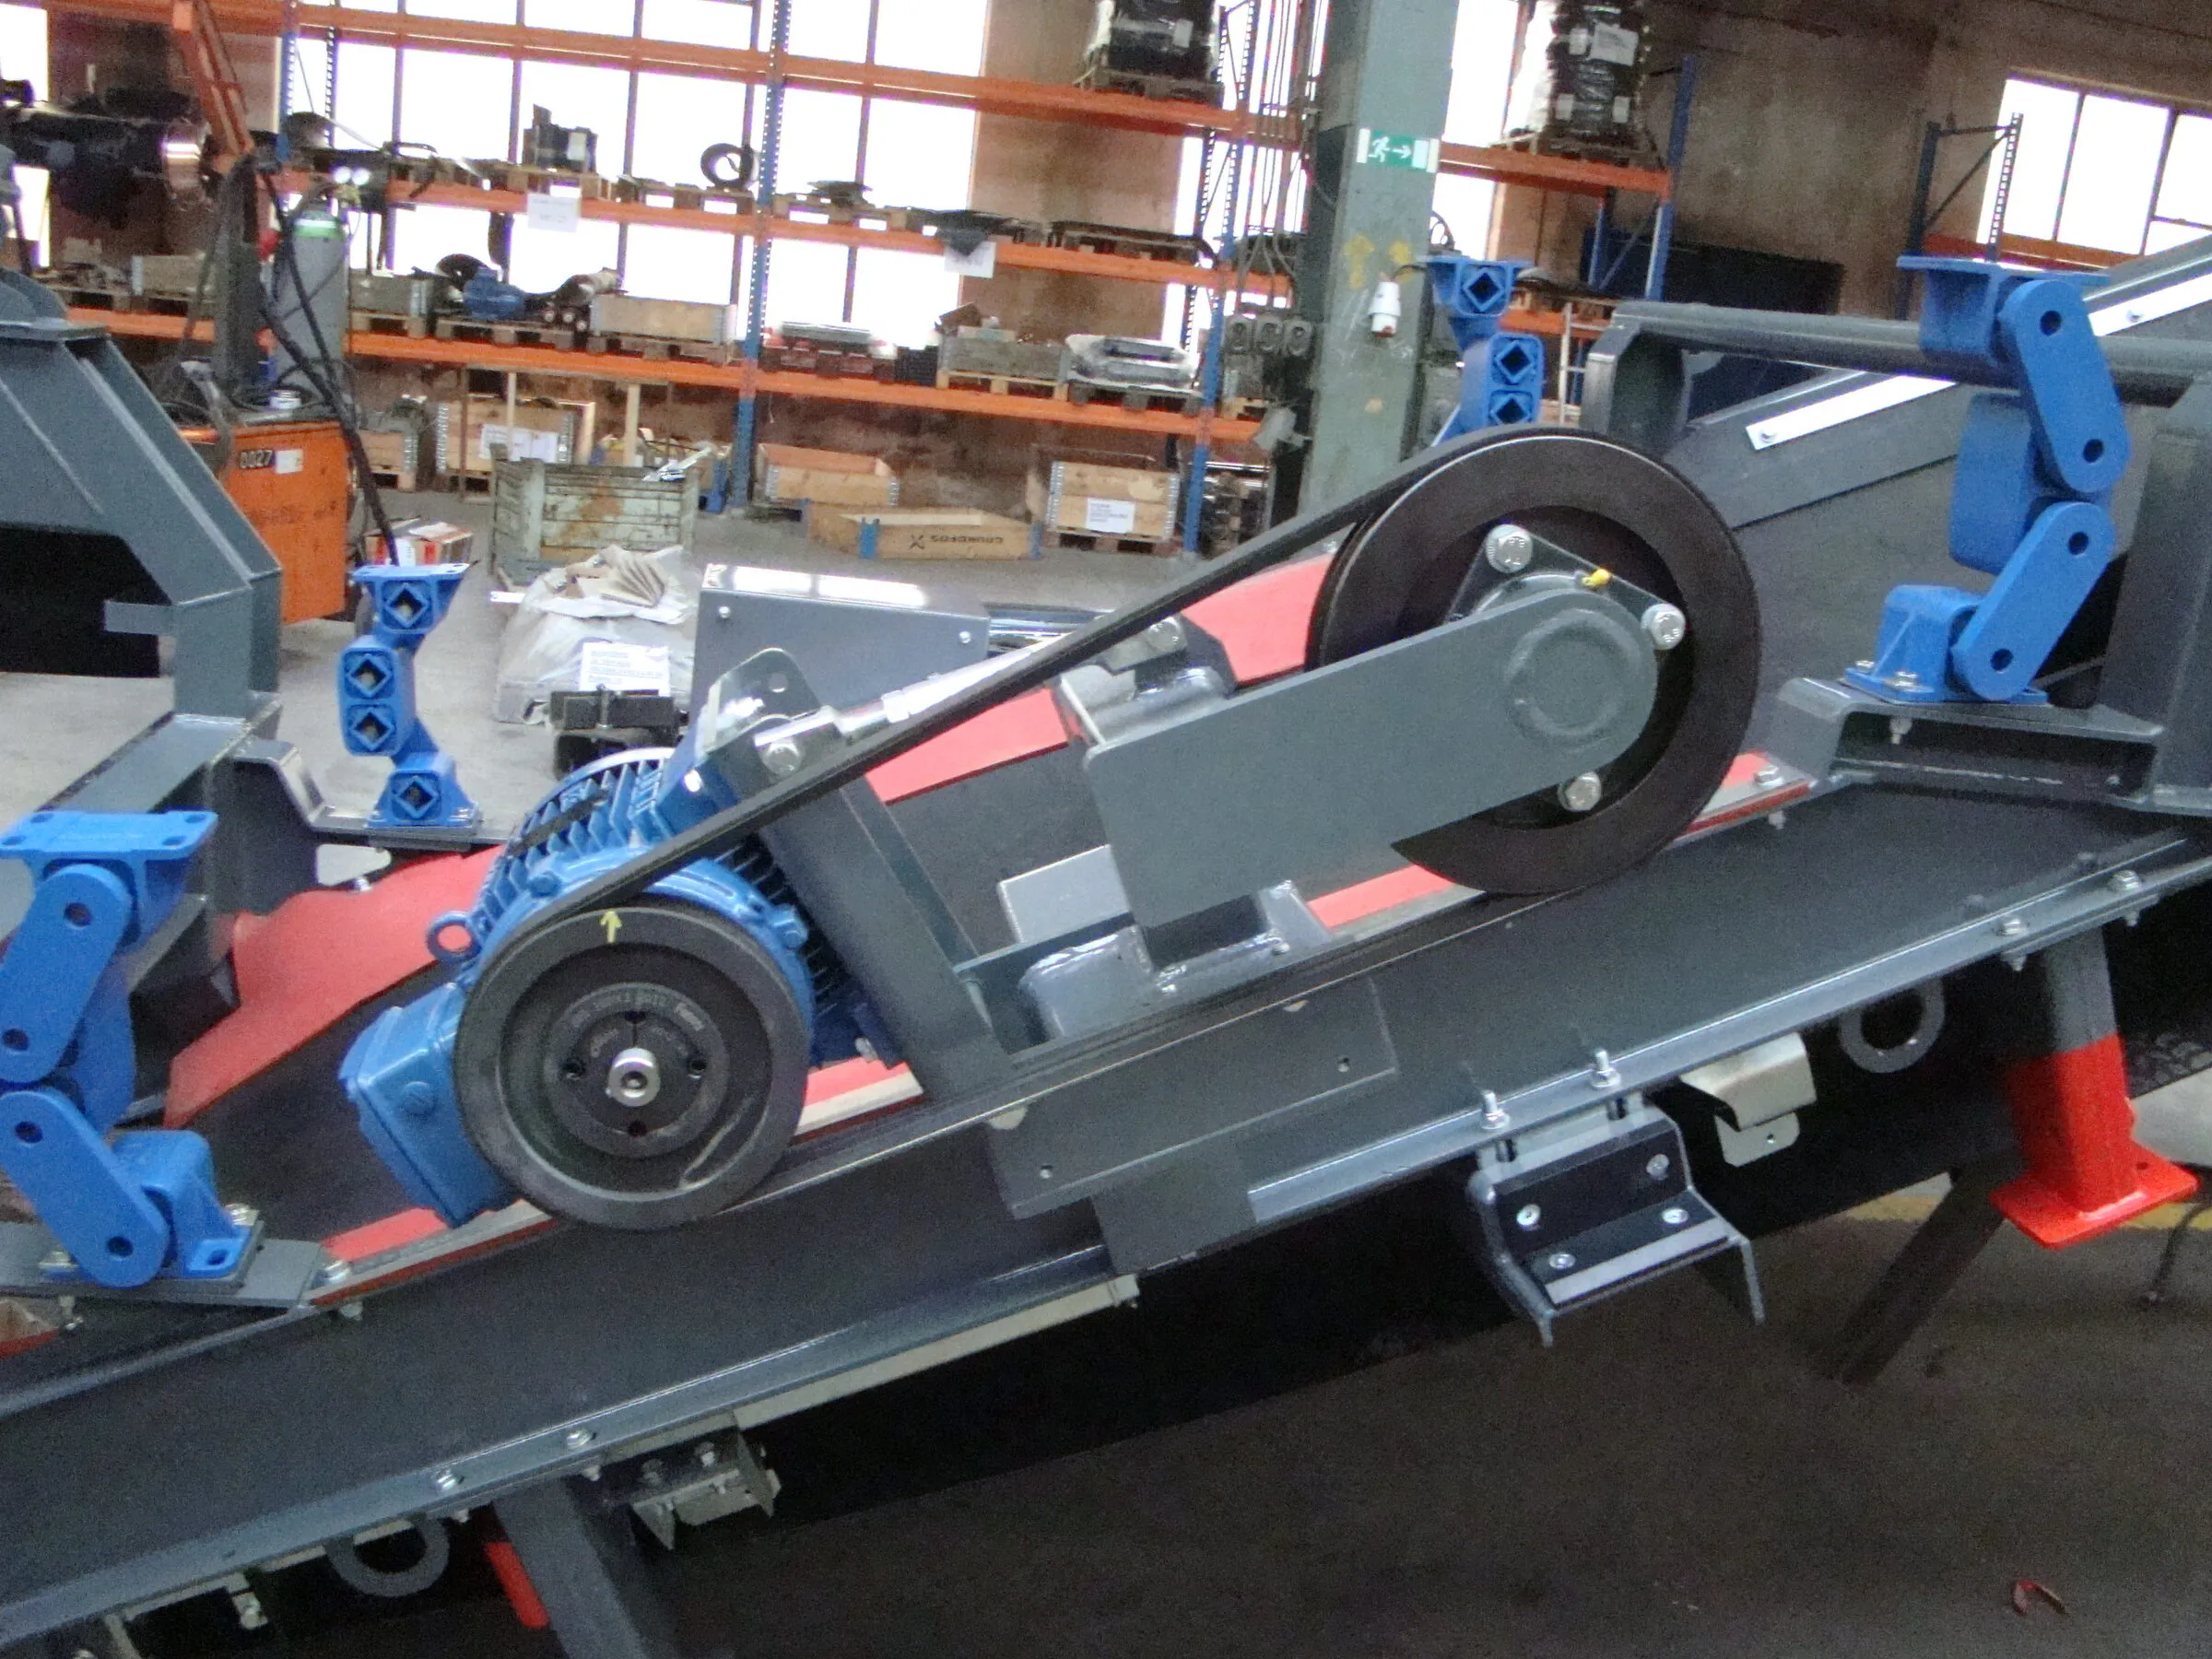
Conveyor drive: pulley, bearing and blue mounts 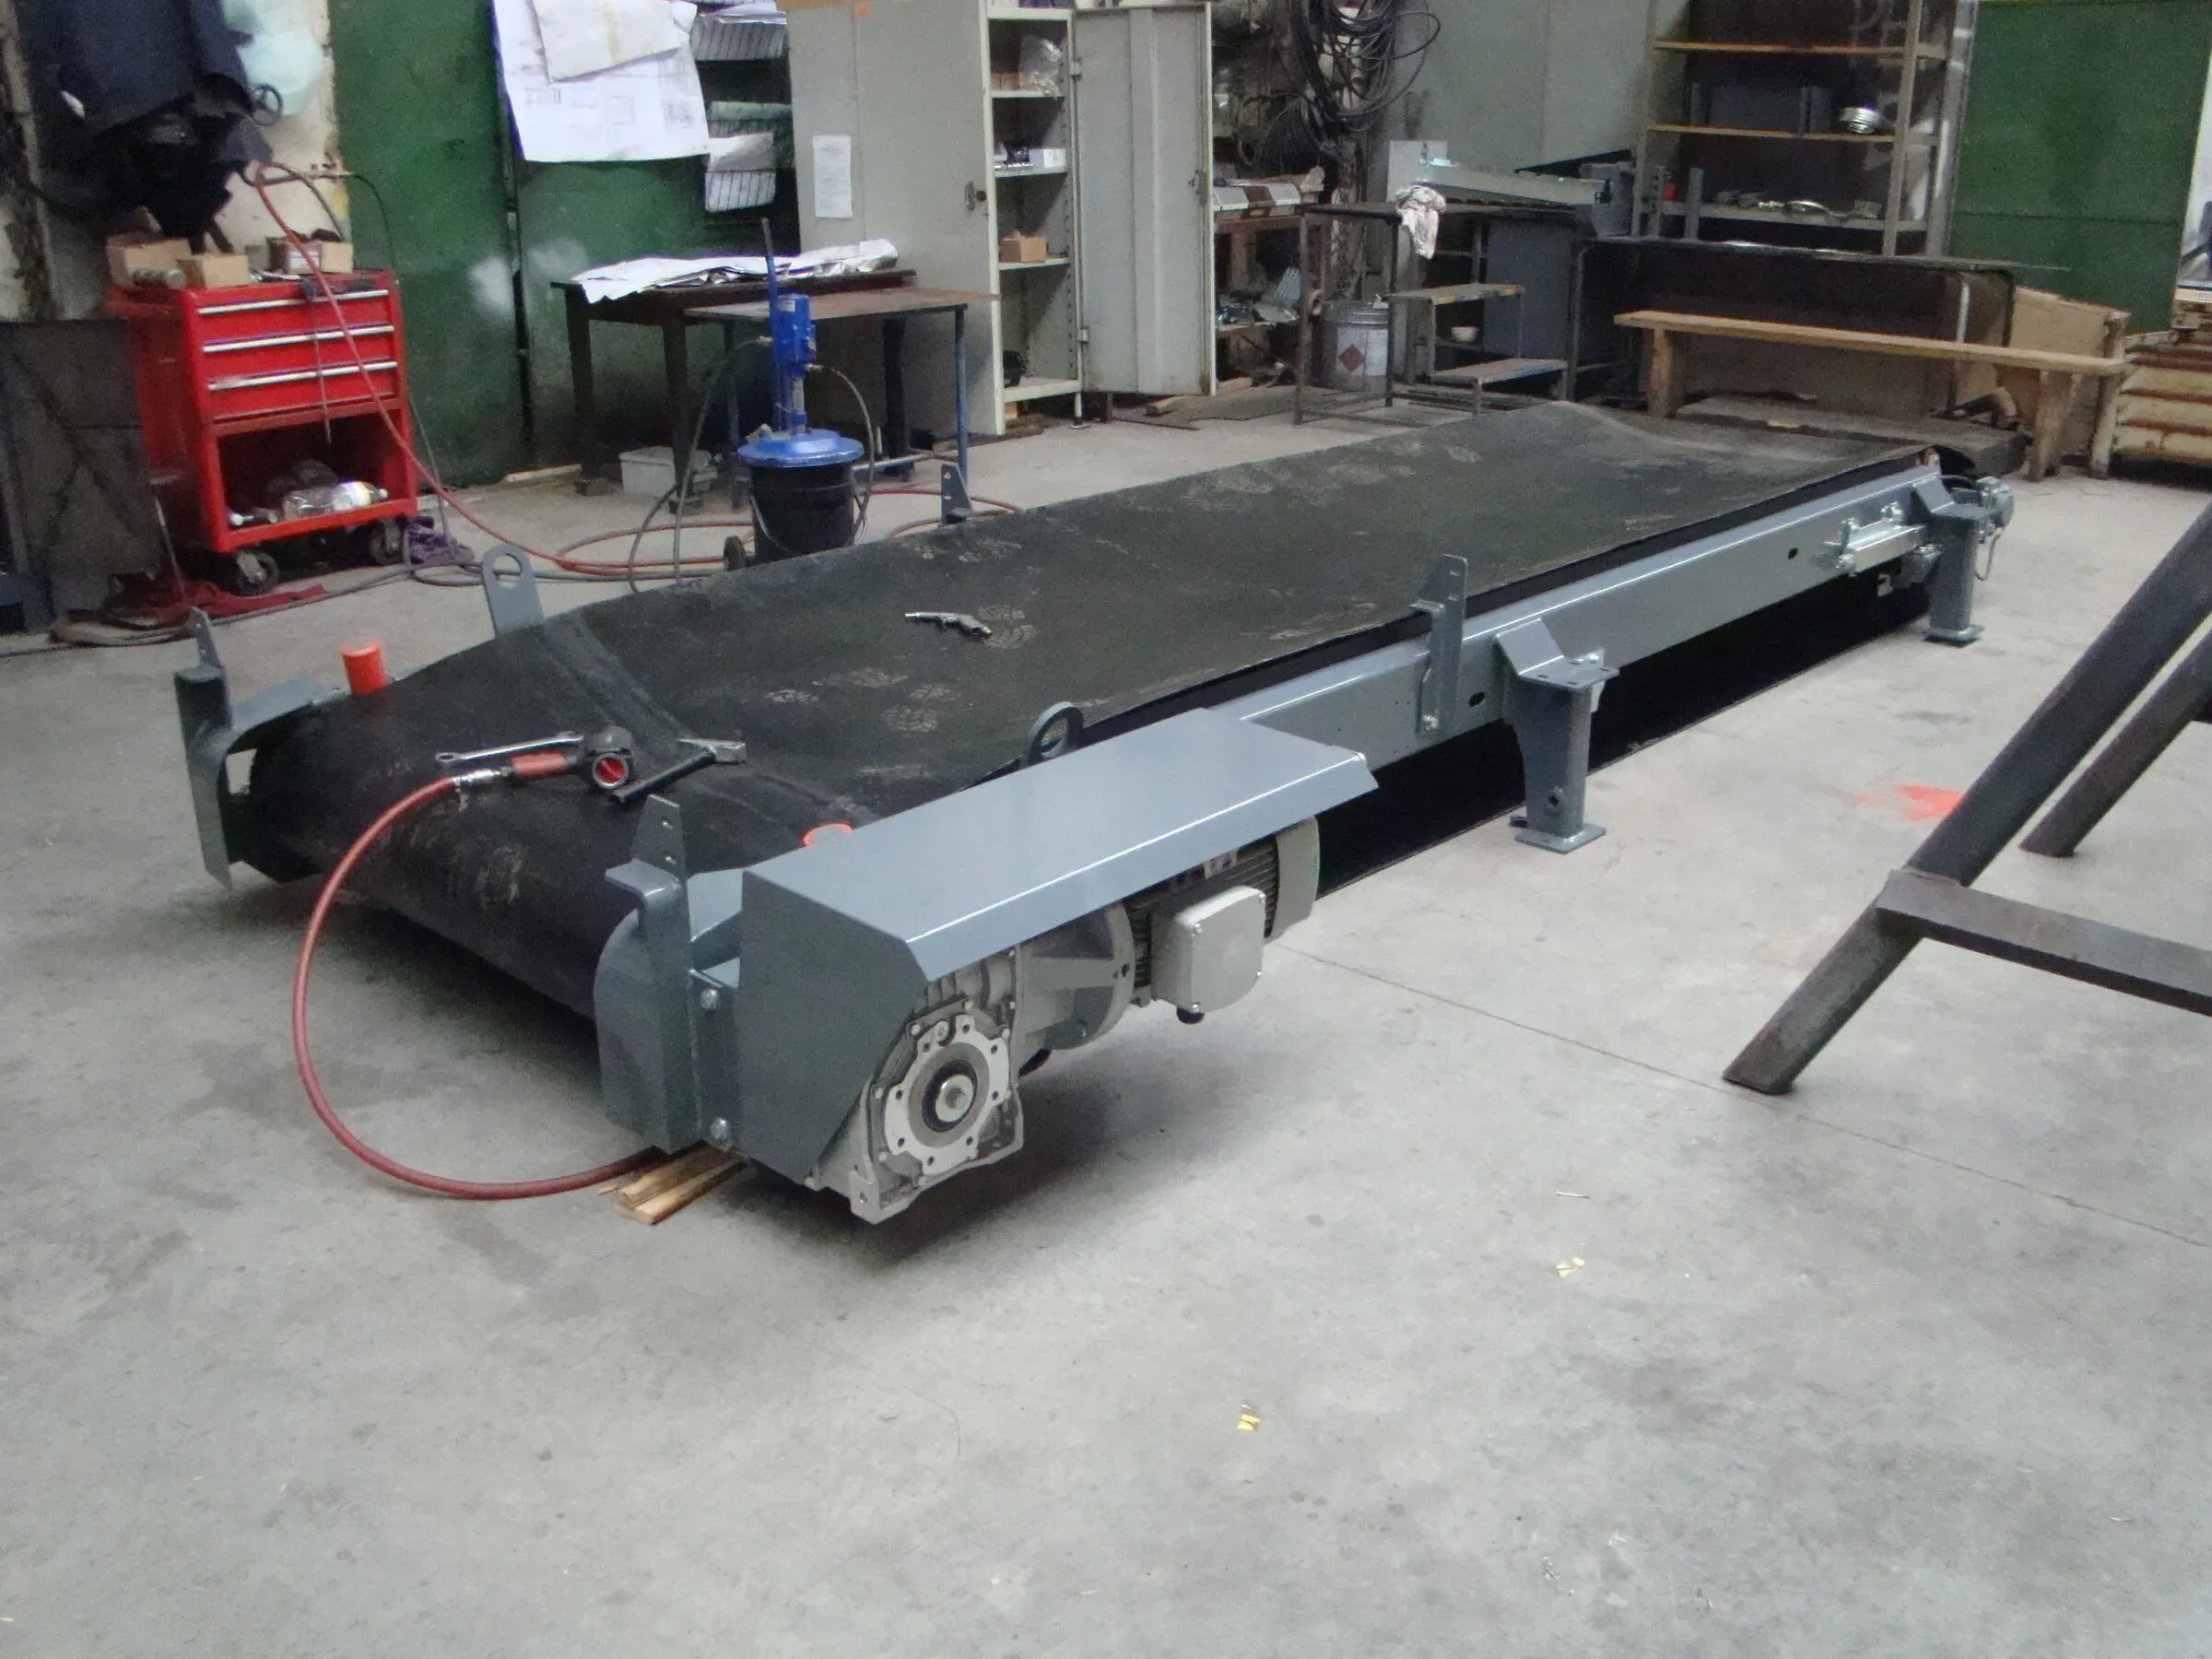
Conveyor with belt lying on the hall floor 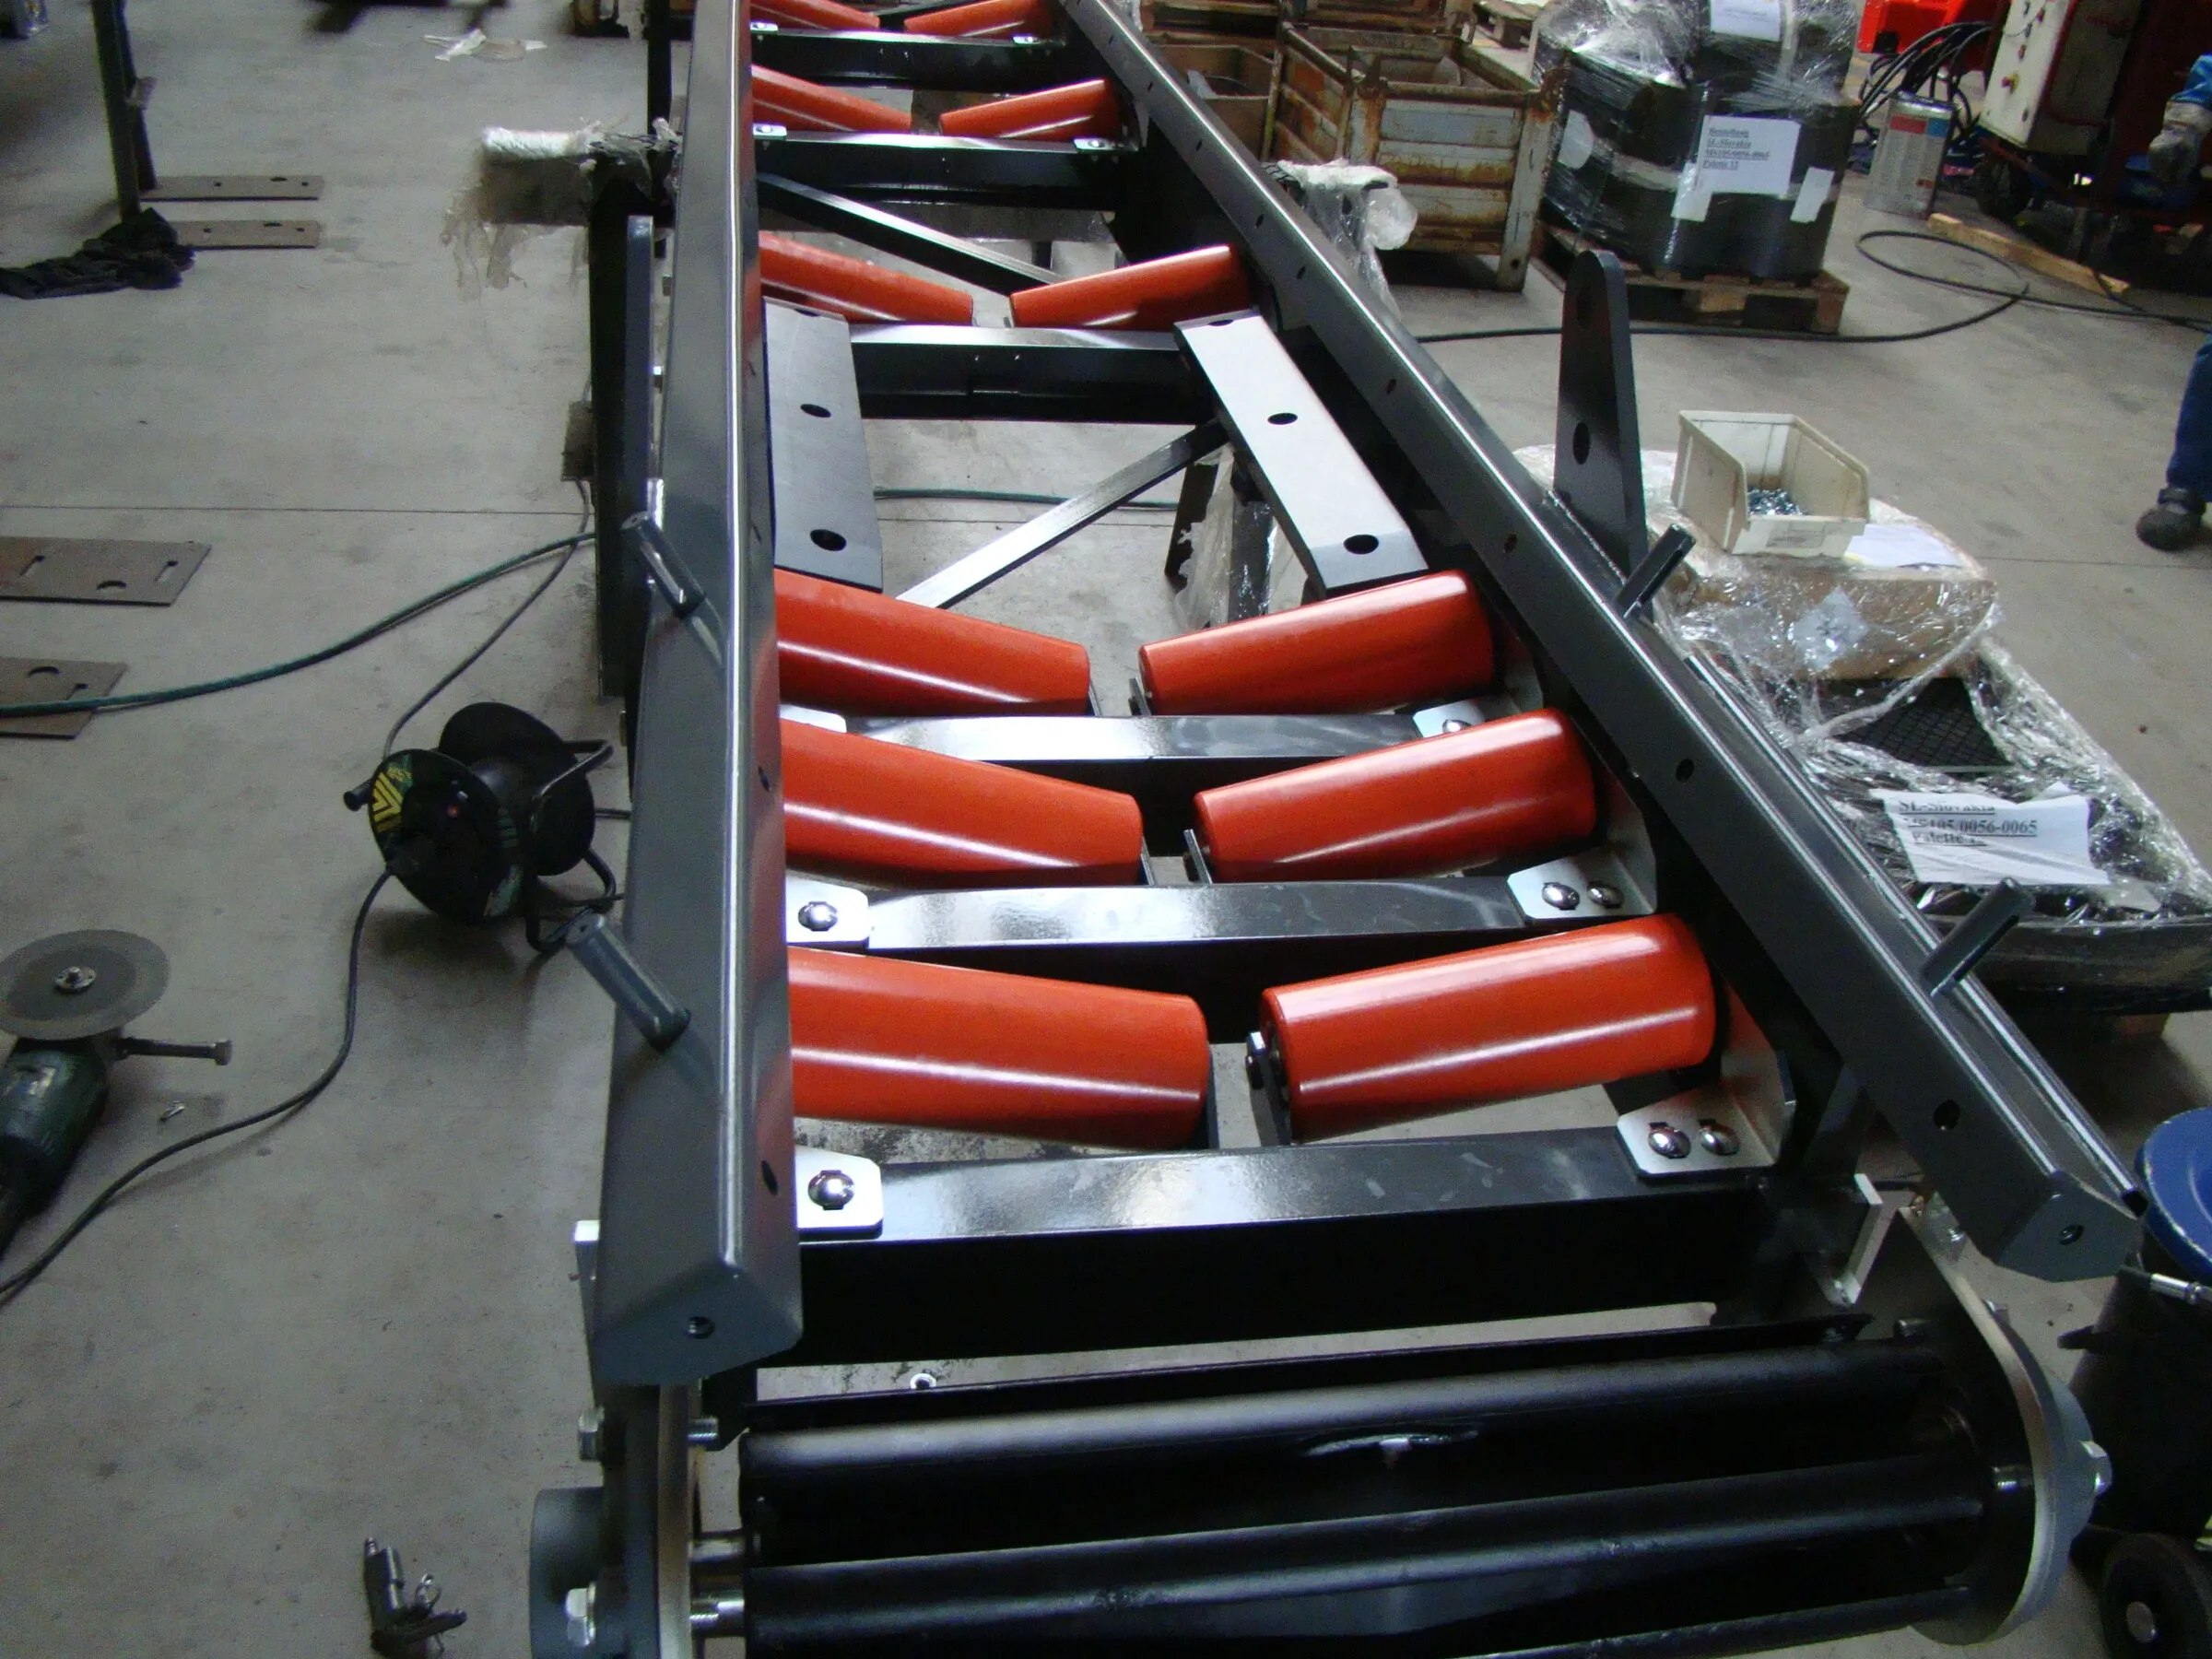
Red idler rollers on a conveyor frame, close-up 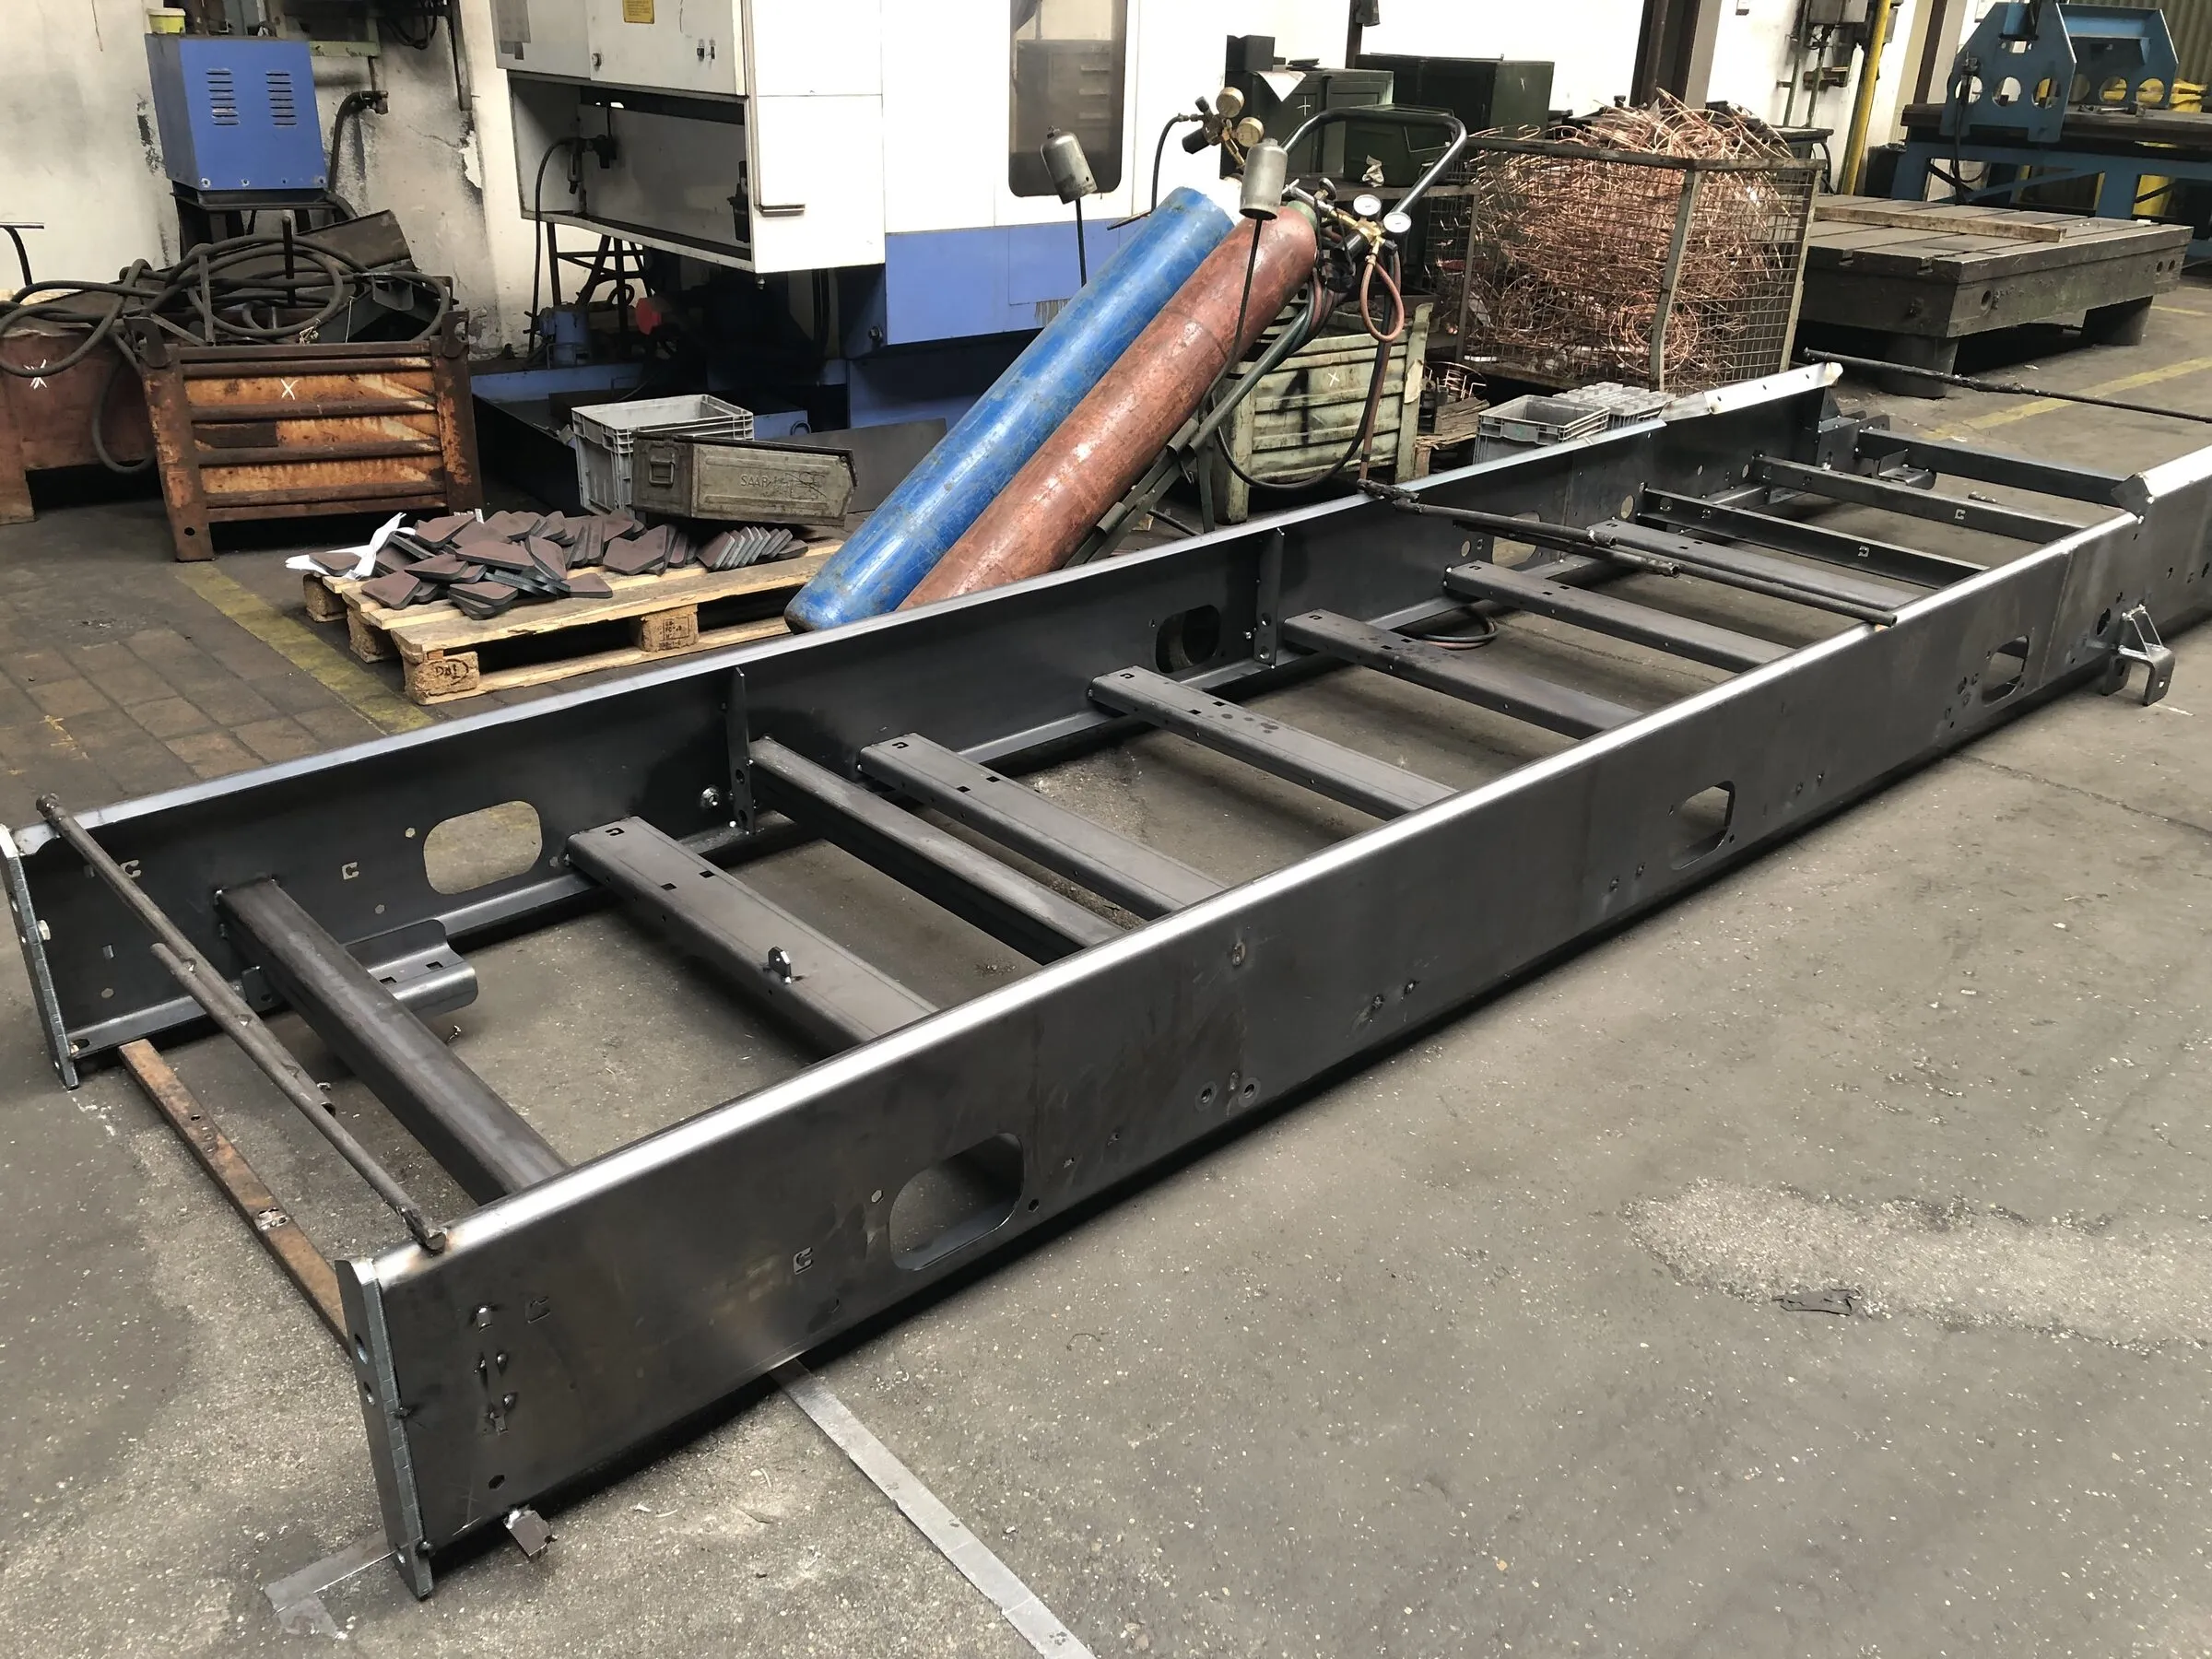
Long conveyor frame with drum, before the belt goes on 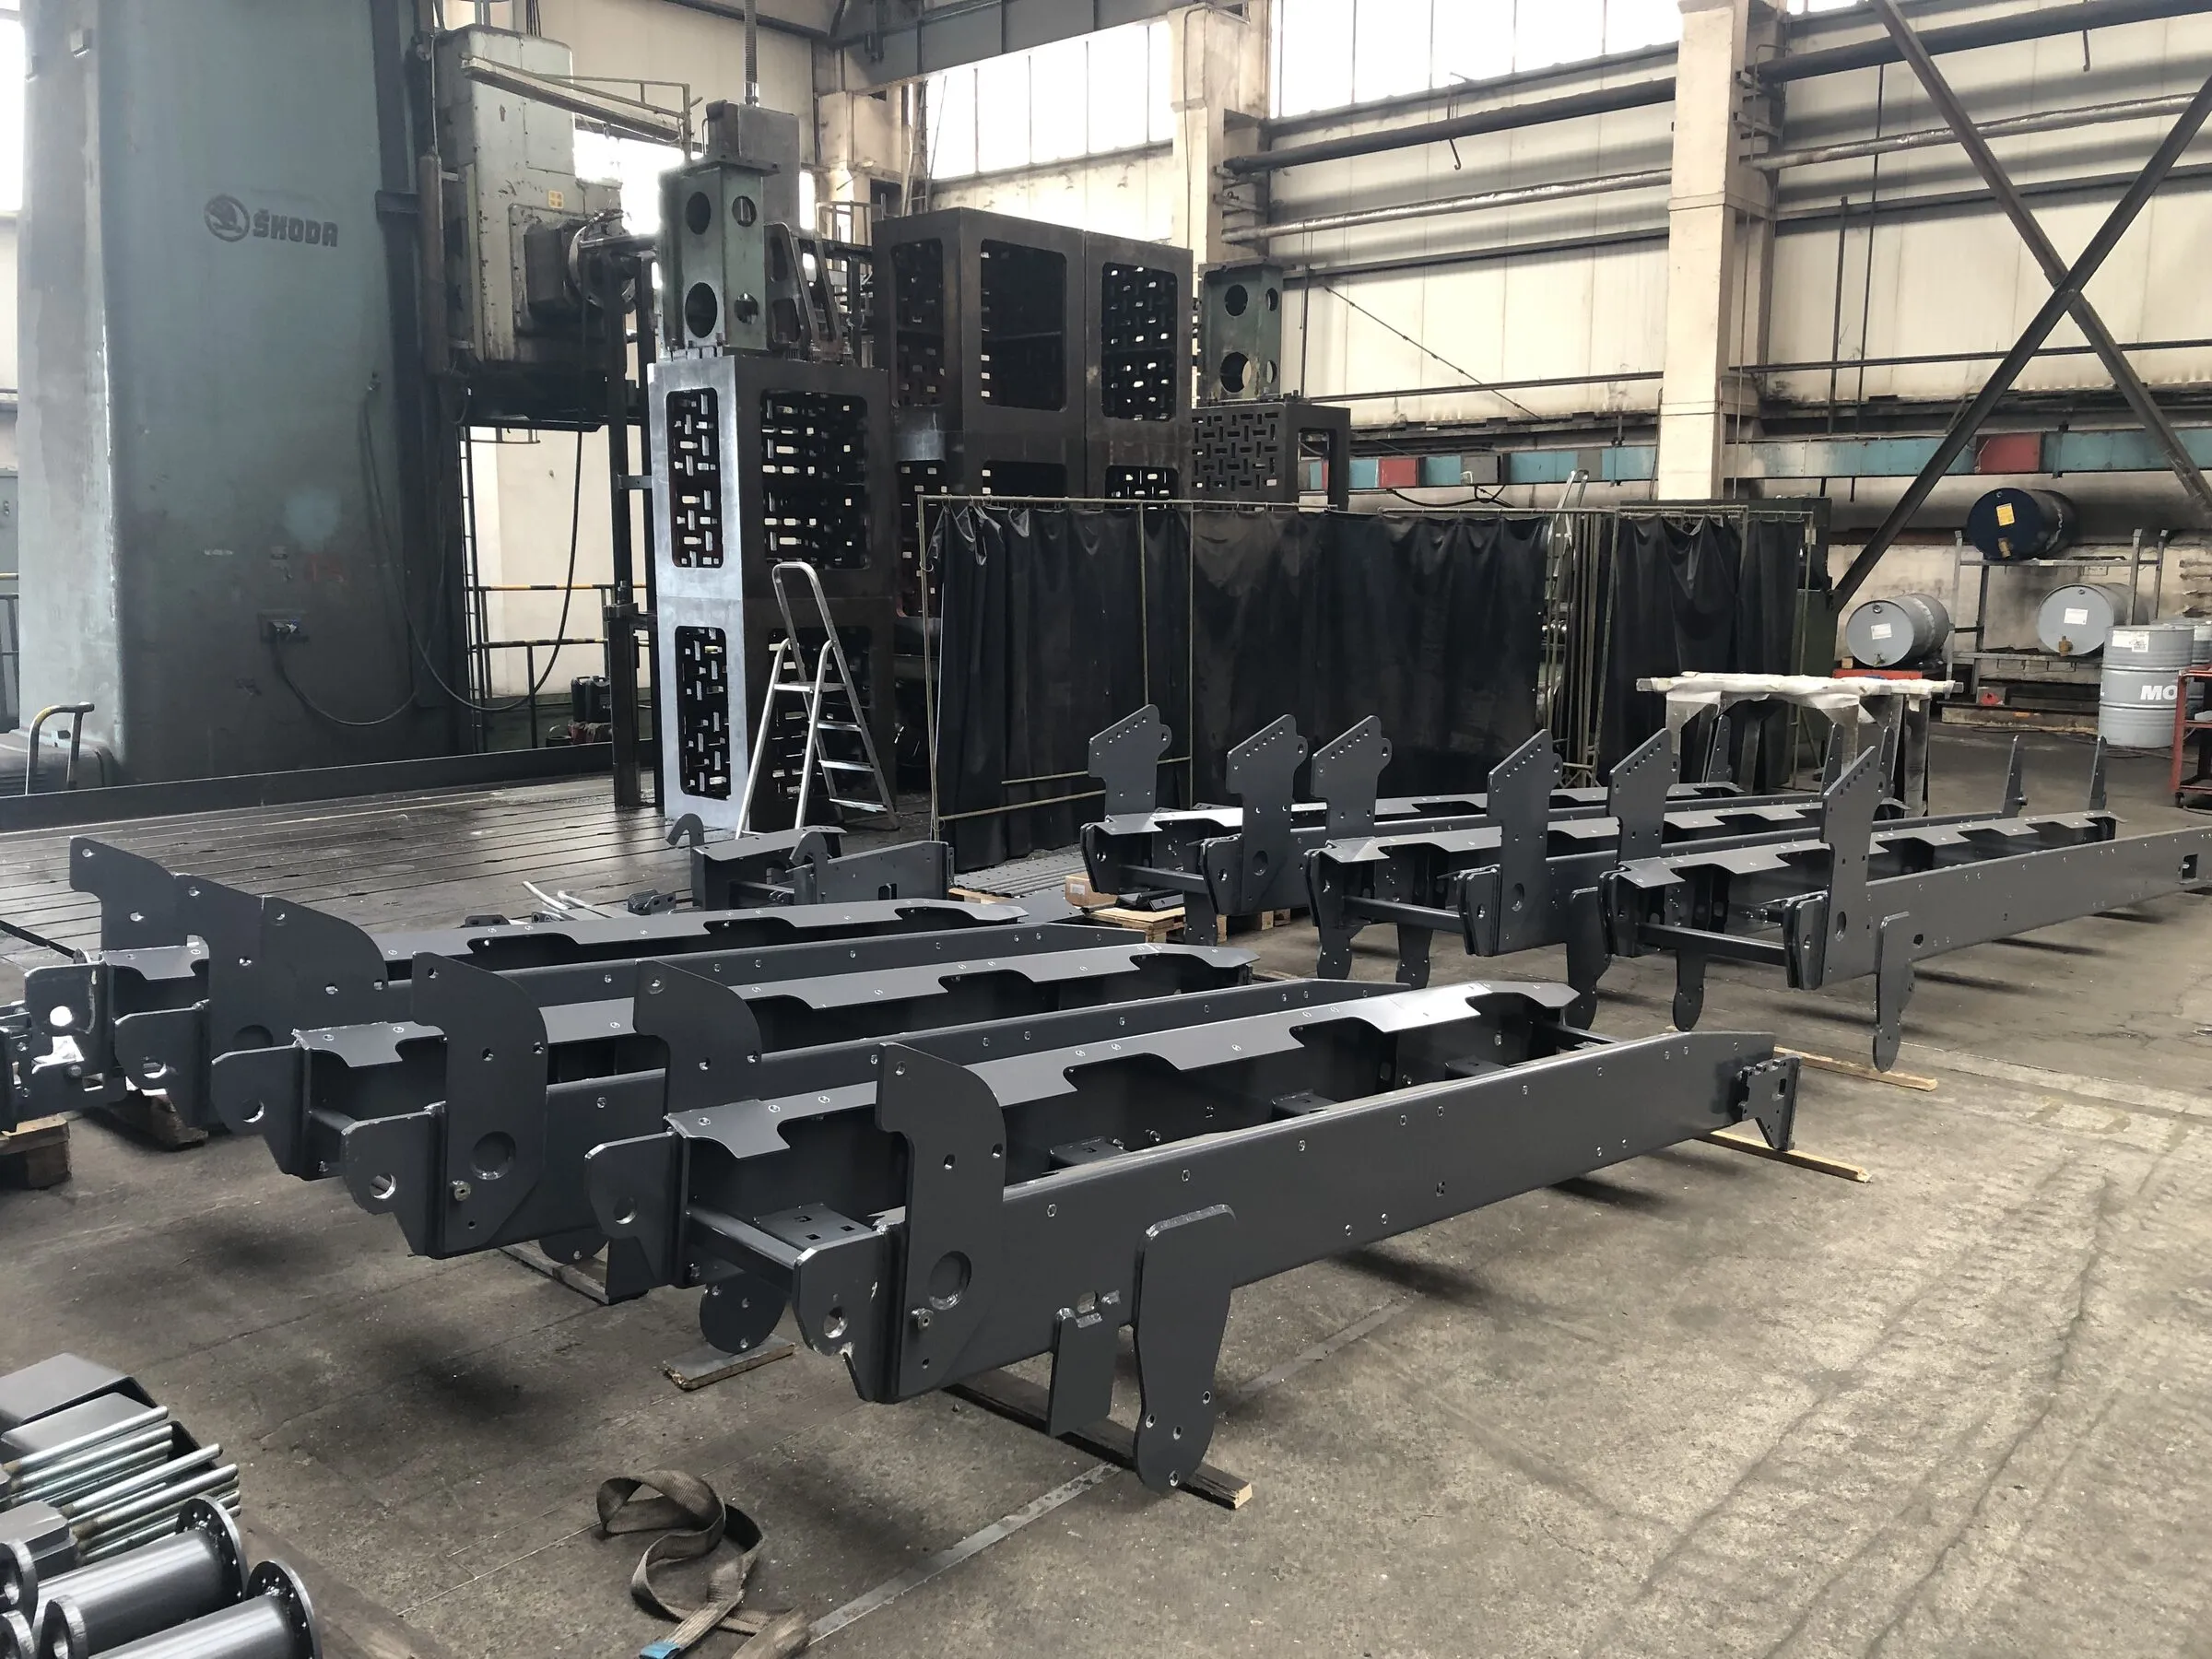
Black welded conveyor support frames staged on the hall floor
Machined weldments
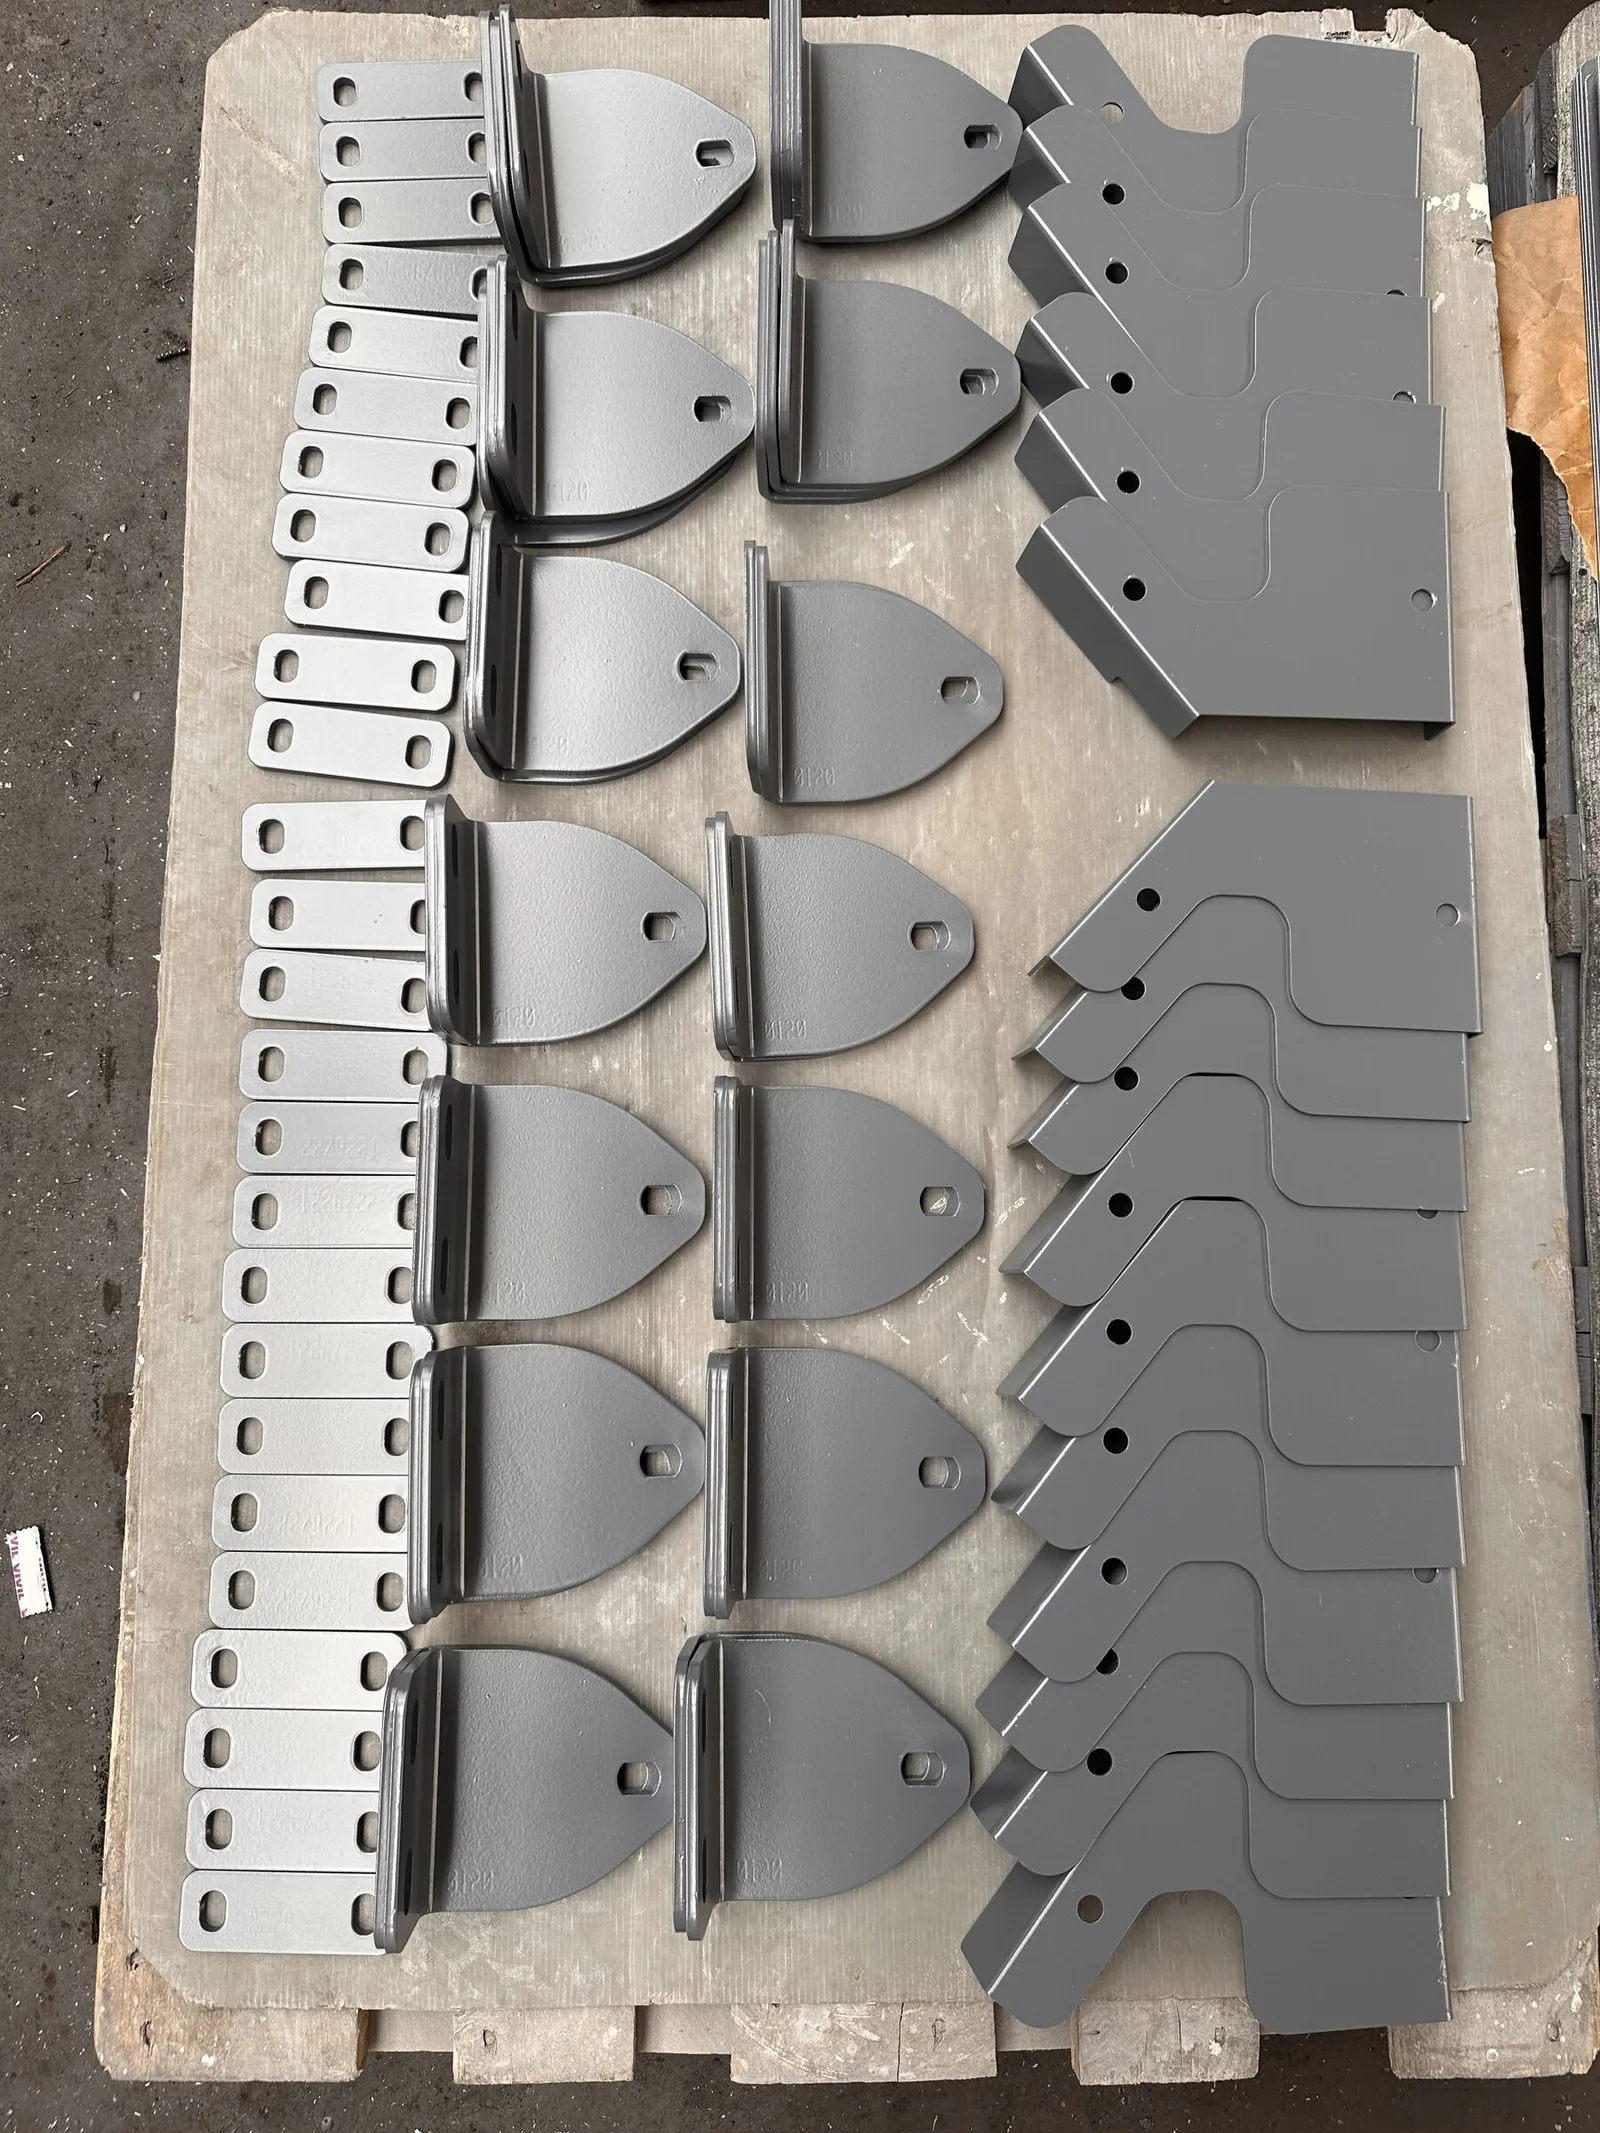
Cut and painted brackets and plates on a pallet 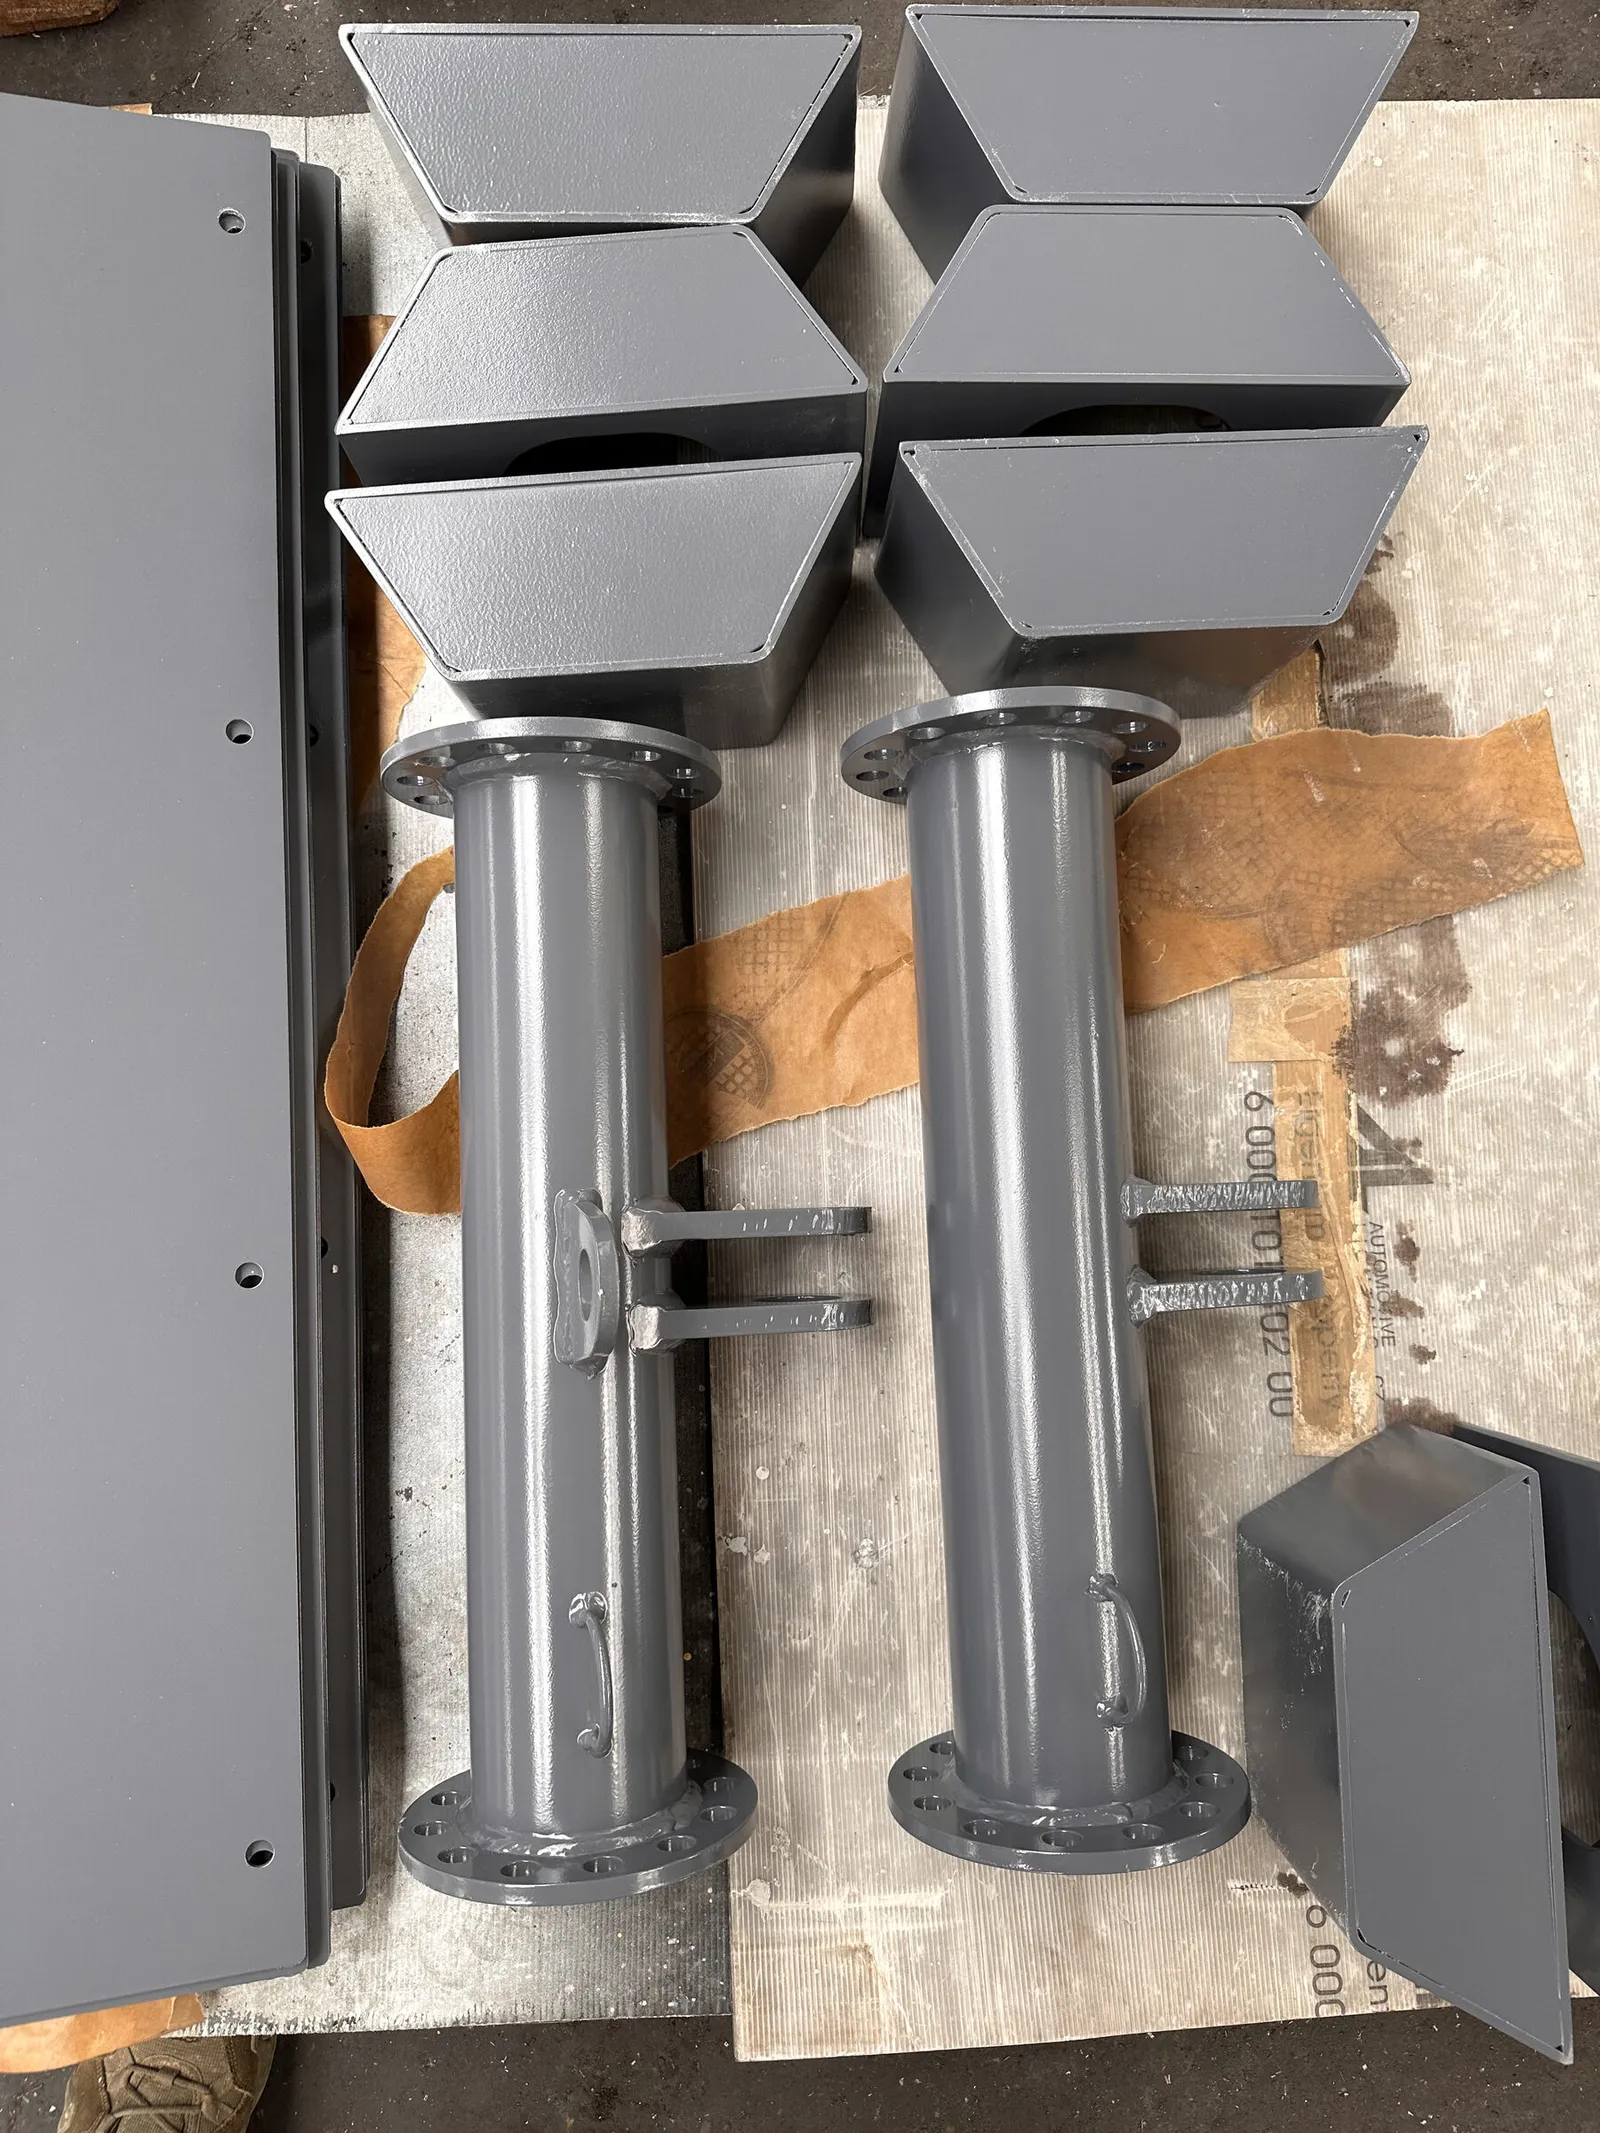
Two painted tube weldments with flanges and brackets 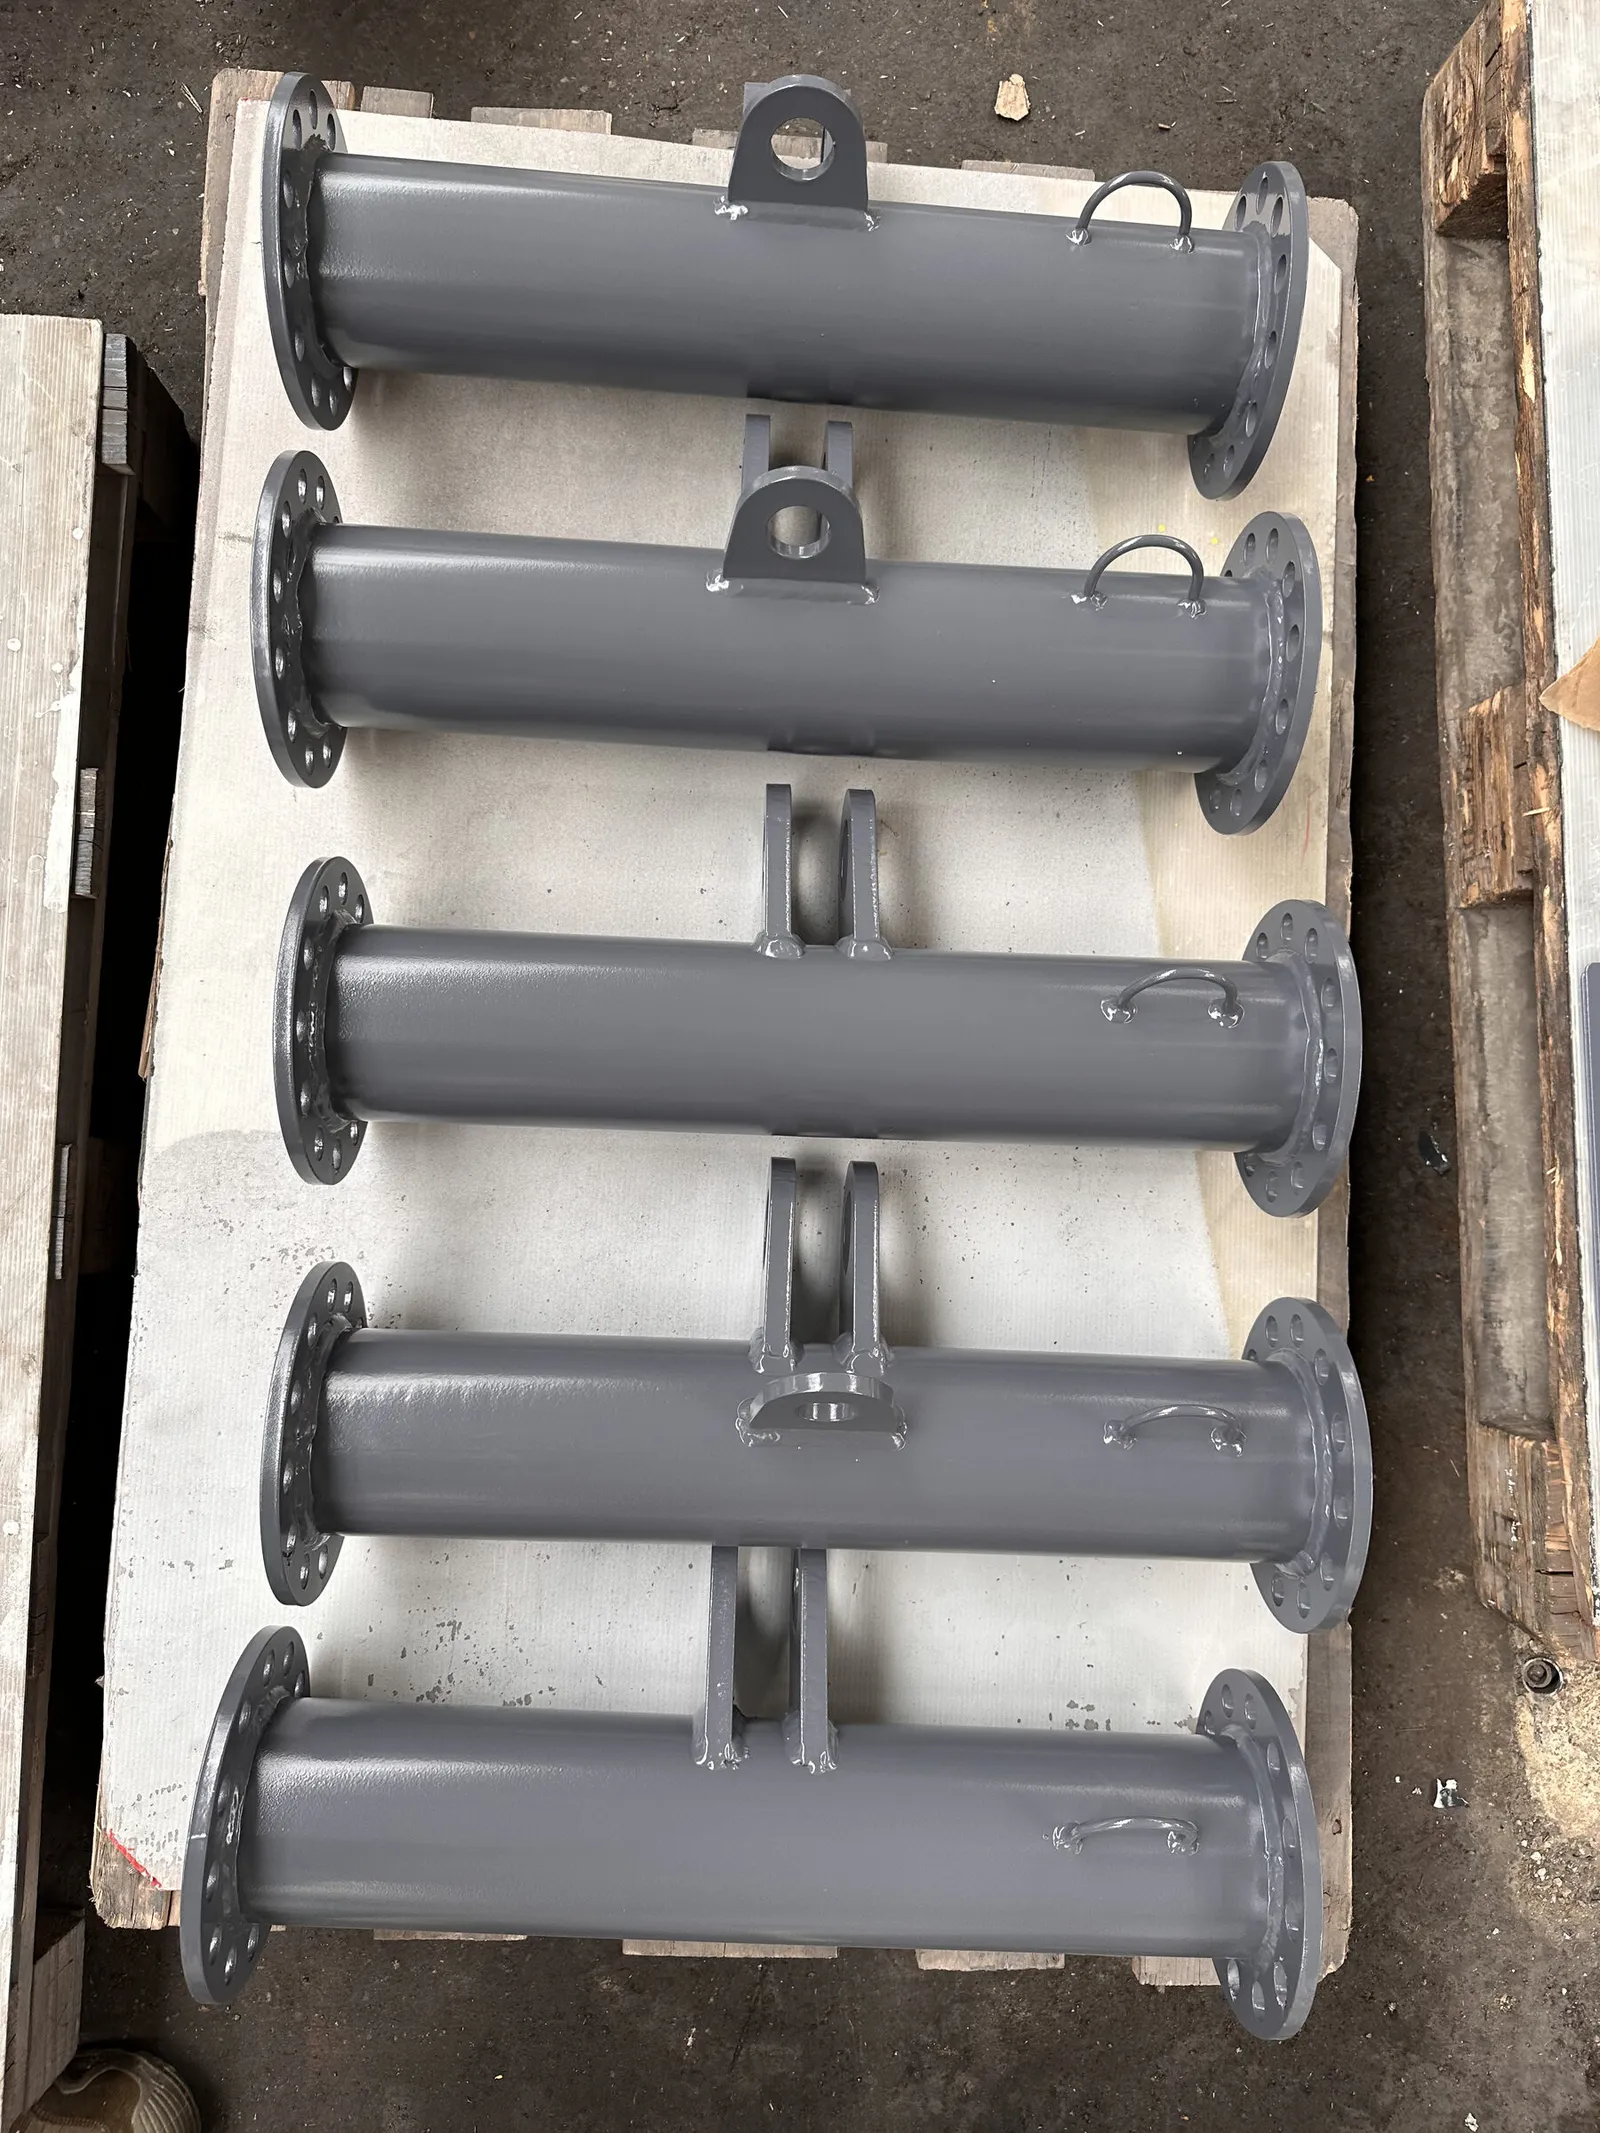
Five painted tube assemblies with end flanges on a pallet 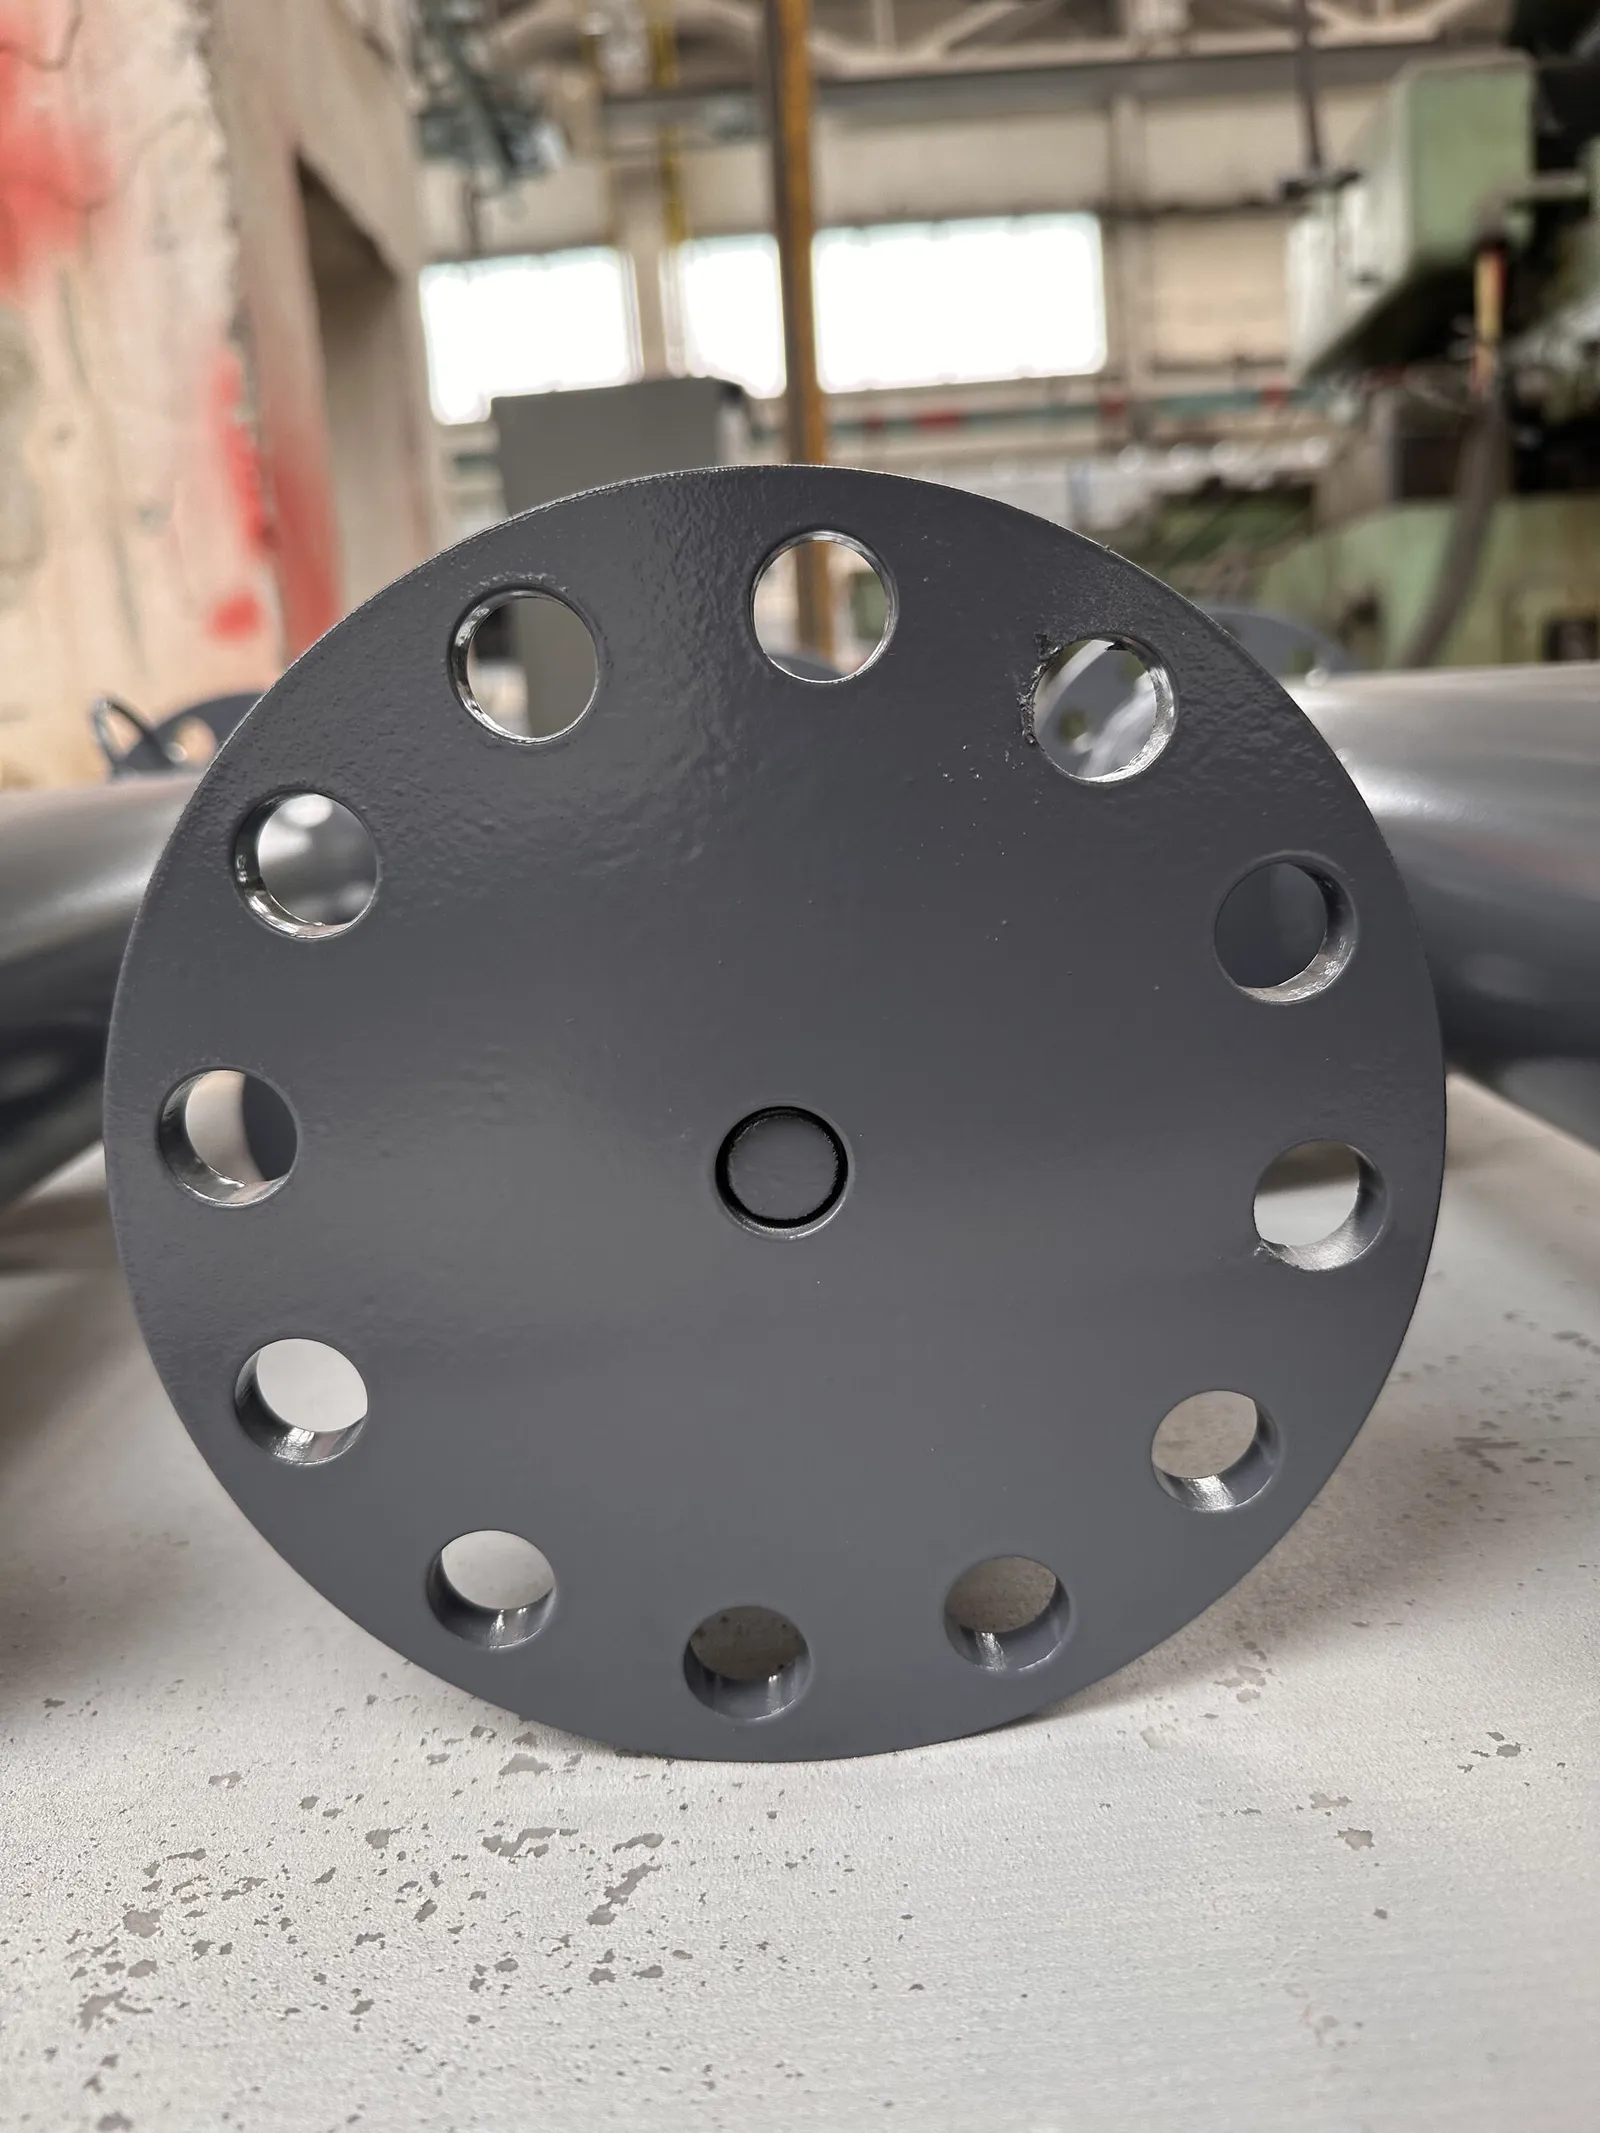
Dark grey round flange plate with bolt holes 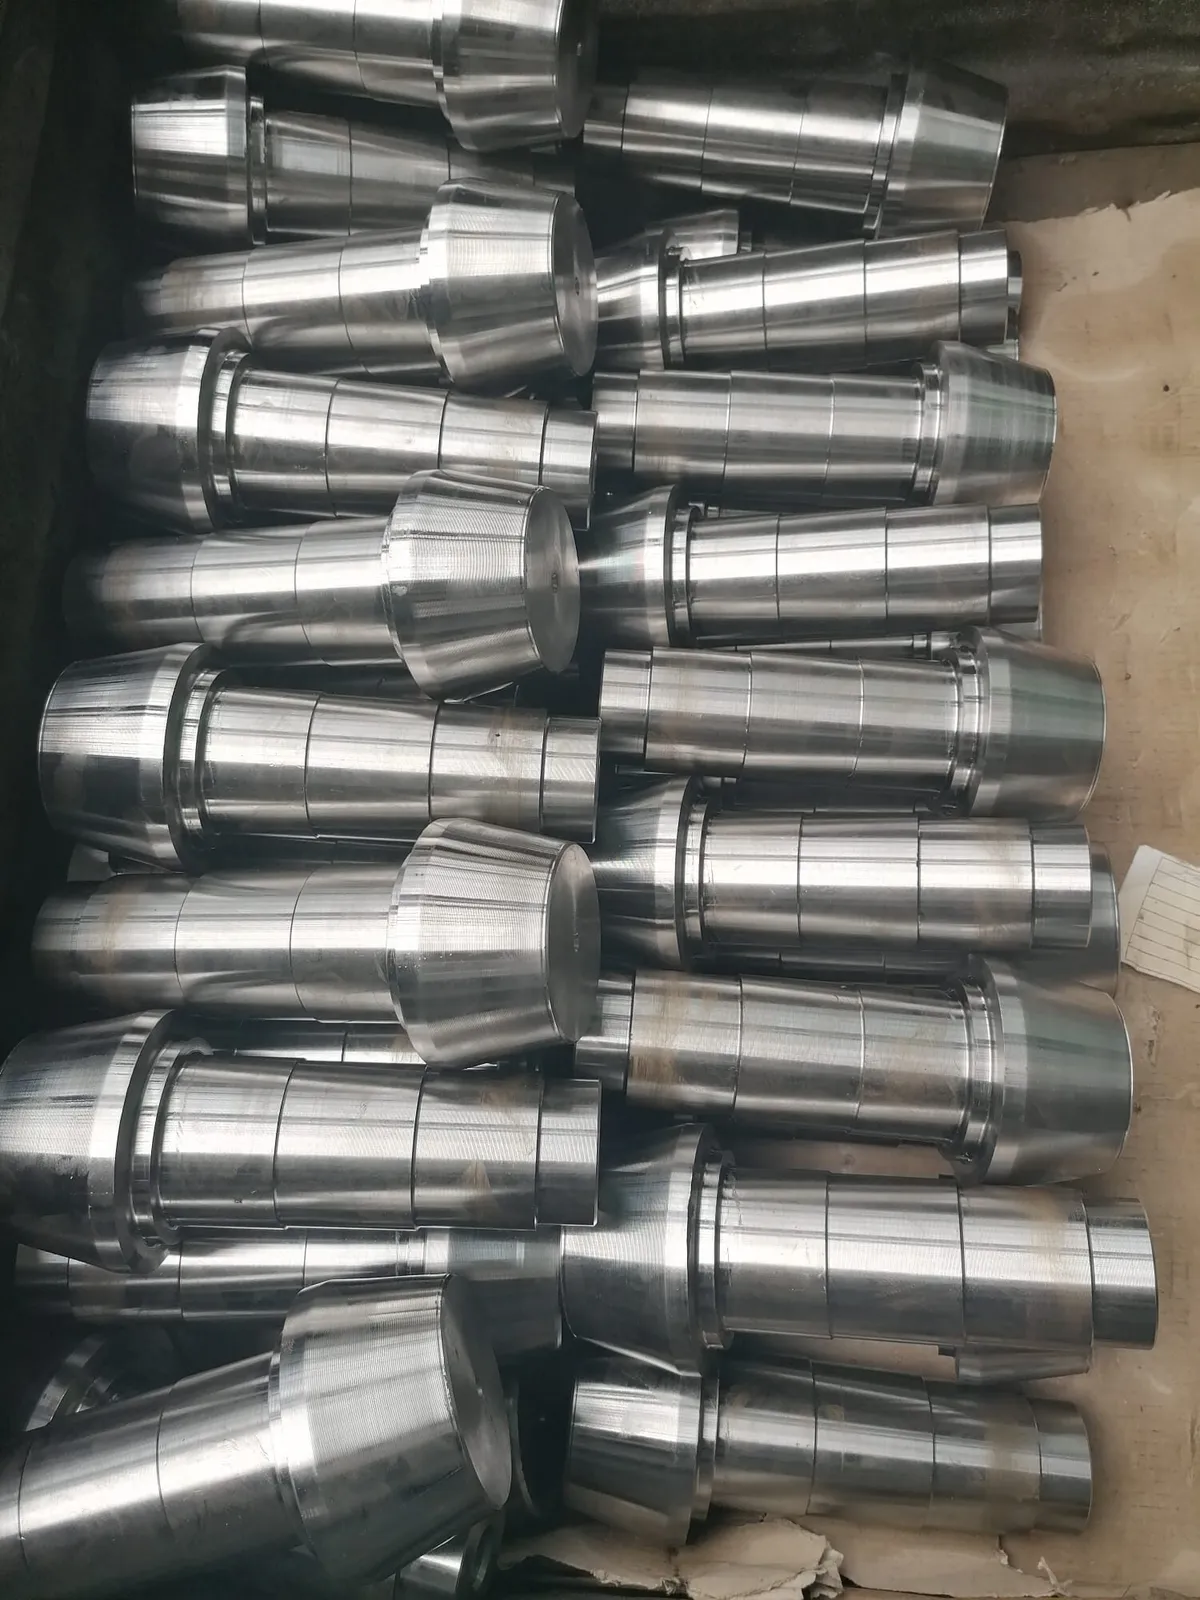
Rack of machined steel shafts 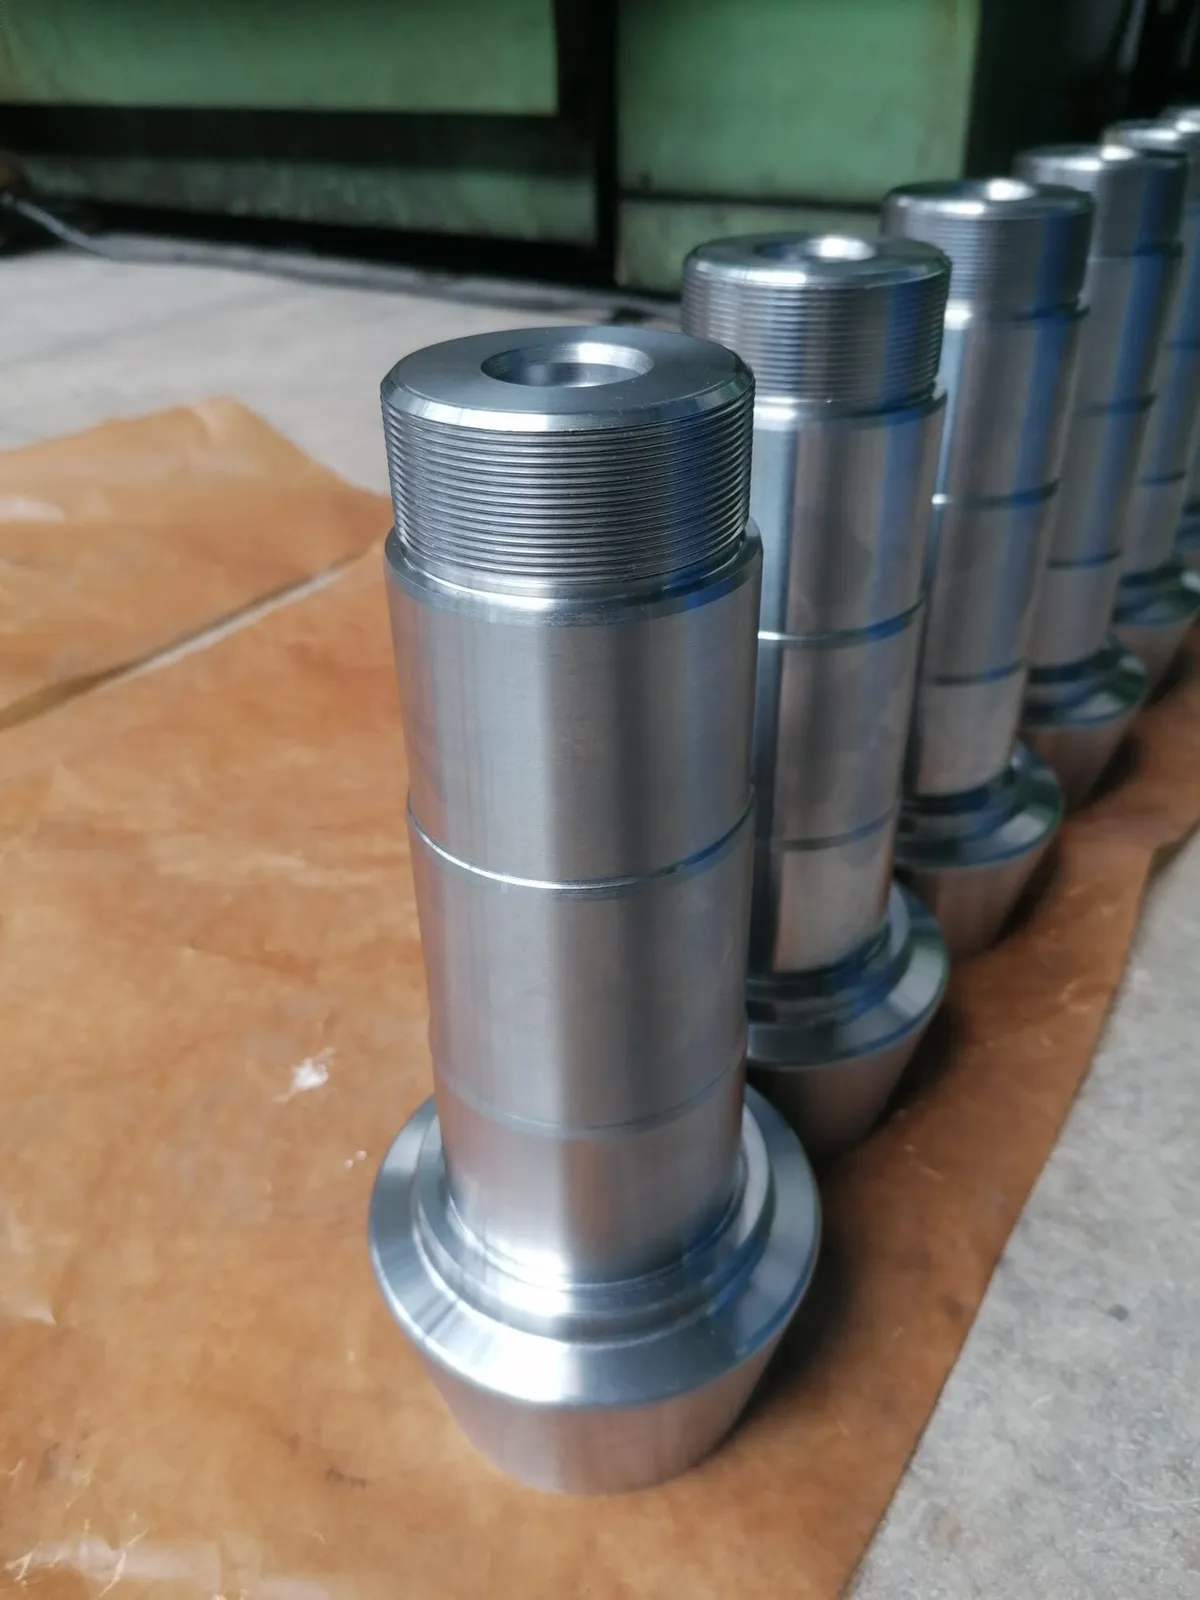
Turned shafts of larger diameter, close-up 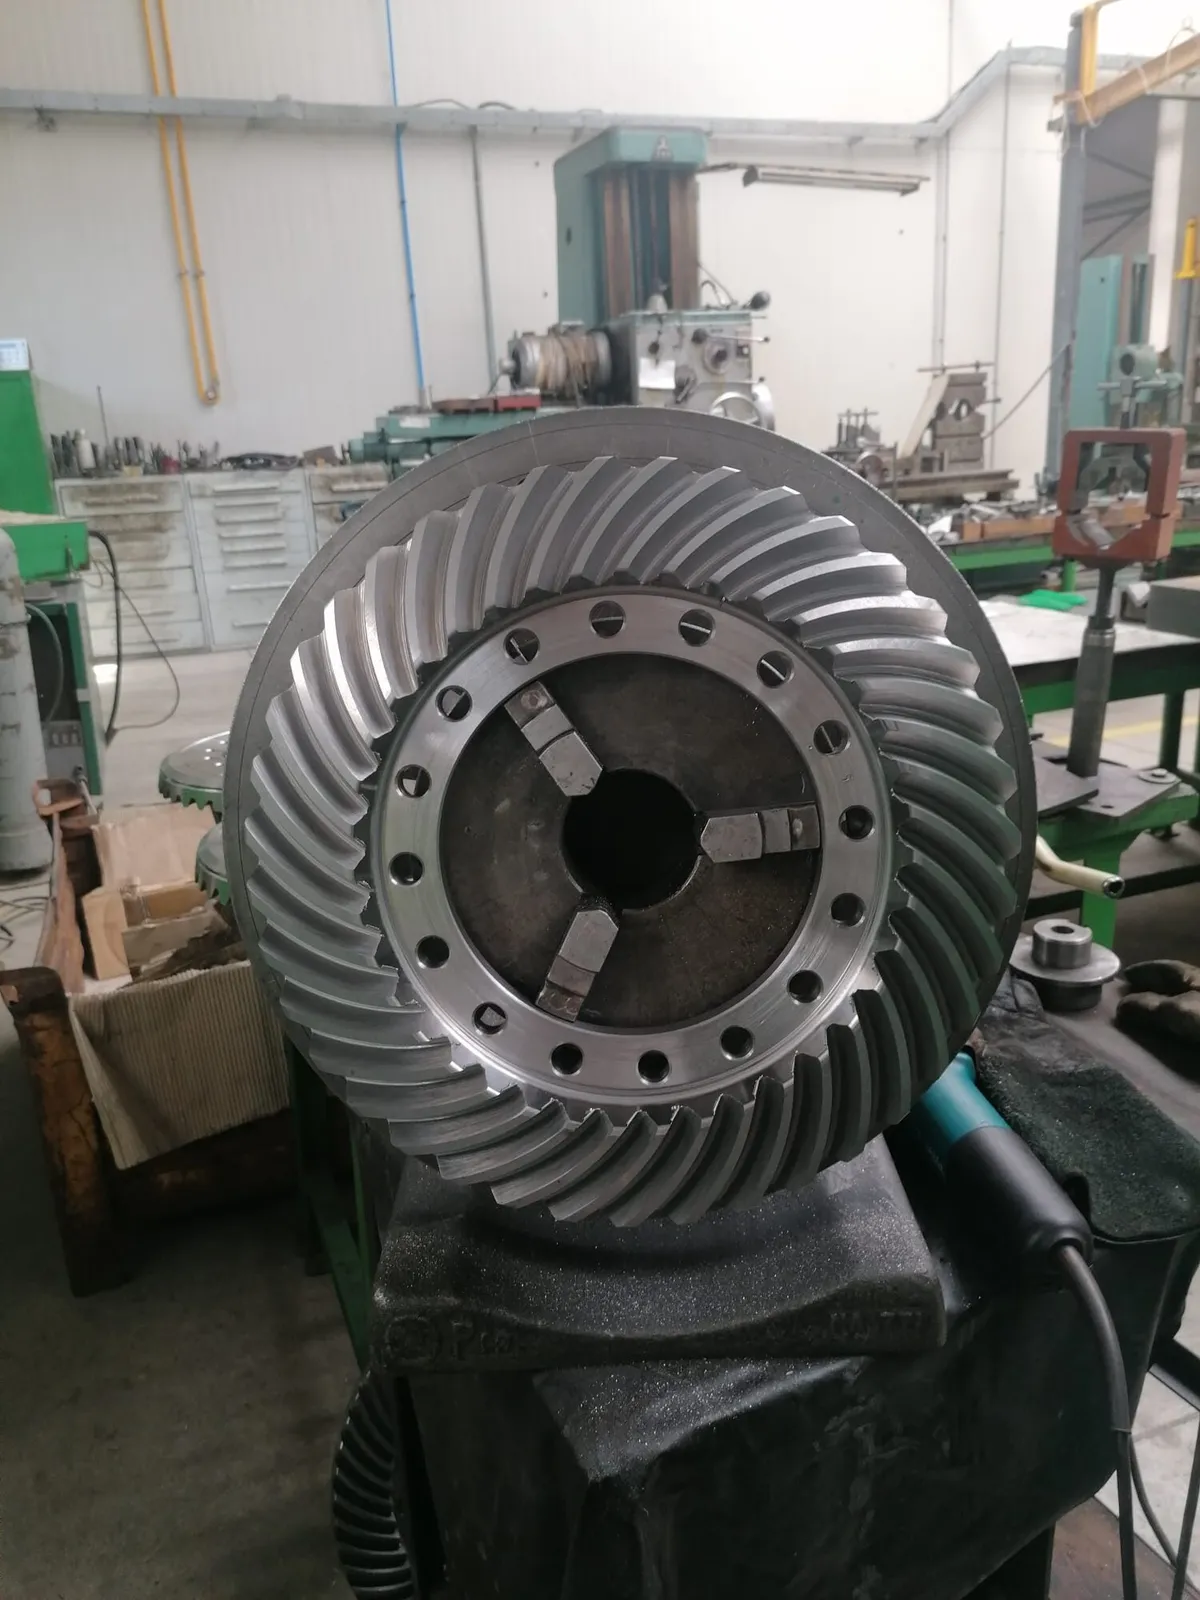
Spiral bevel gear after gear cutting 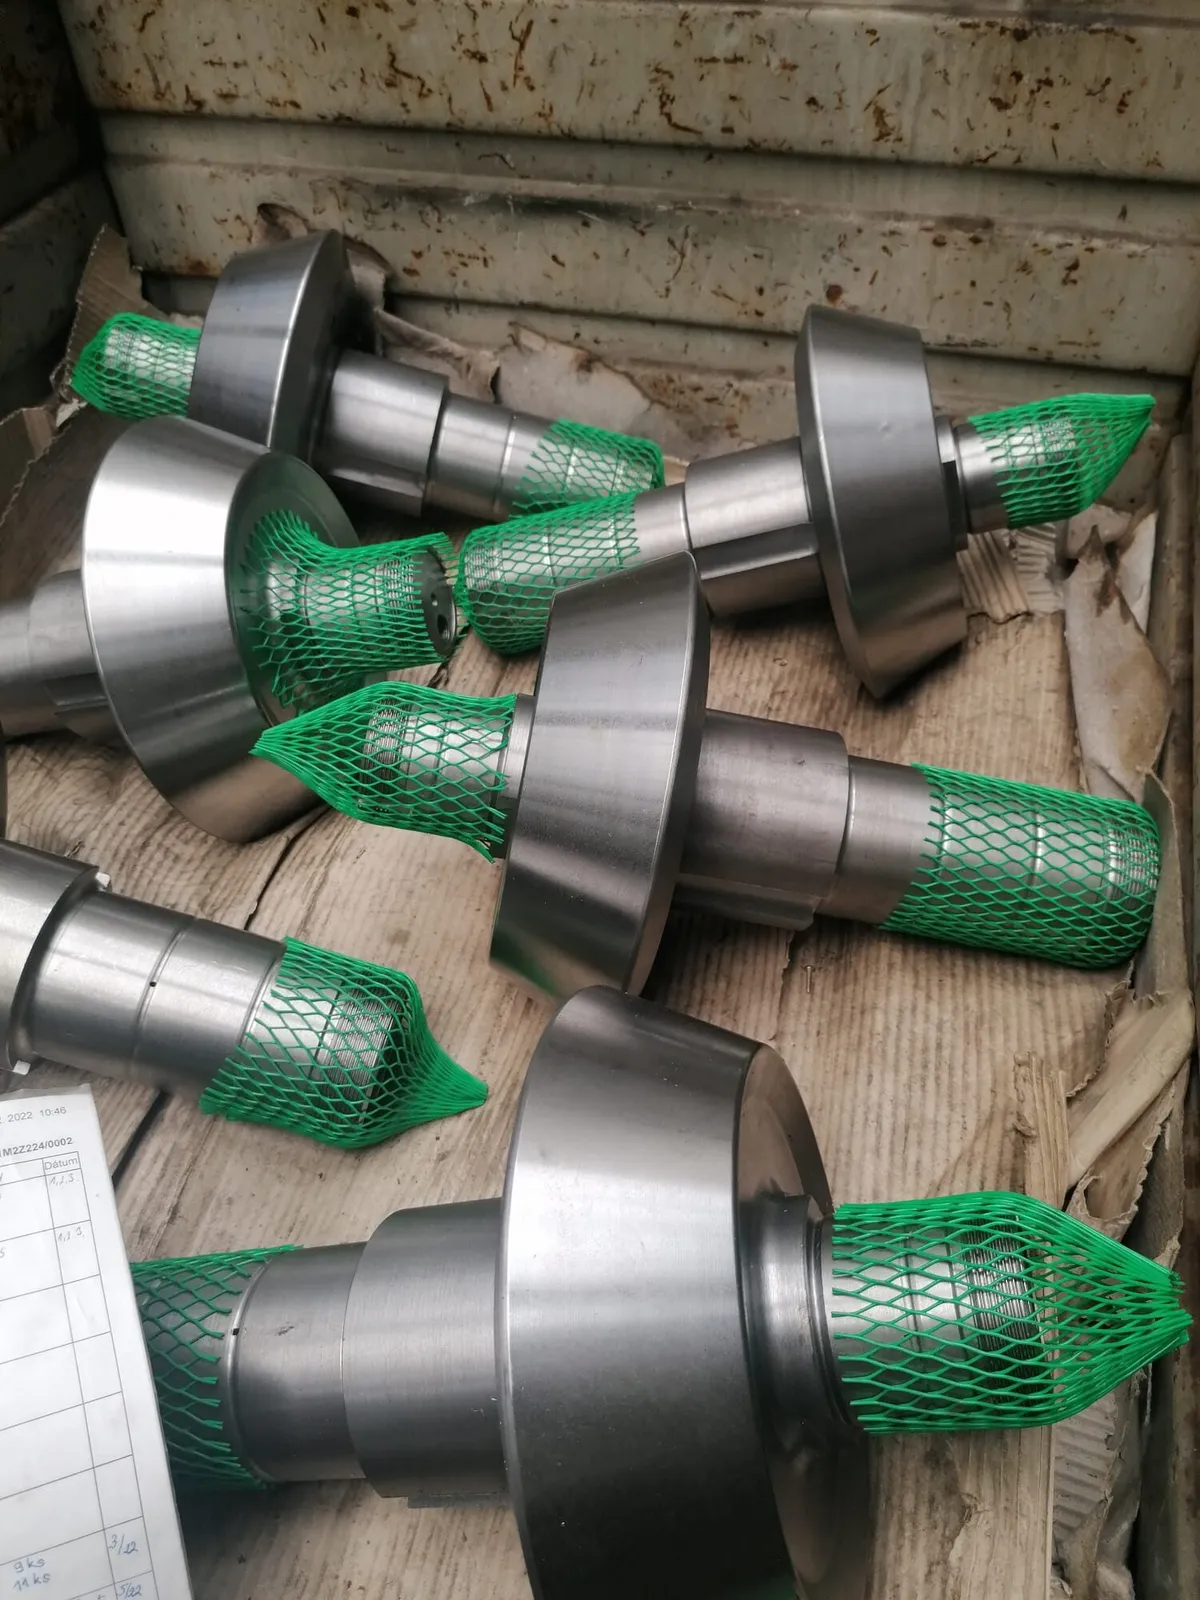
Turned shafts with protective mesh sleeves on the ends
Welding jigs and fixtures
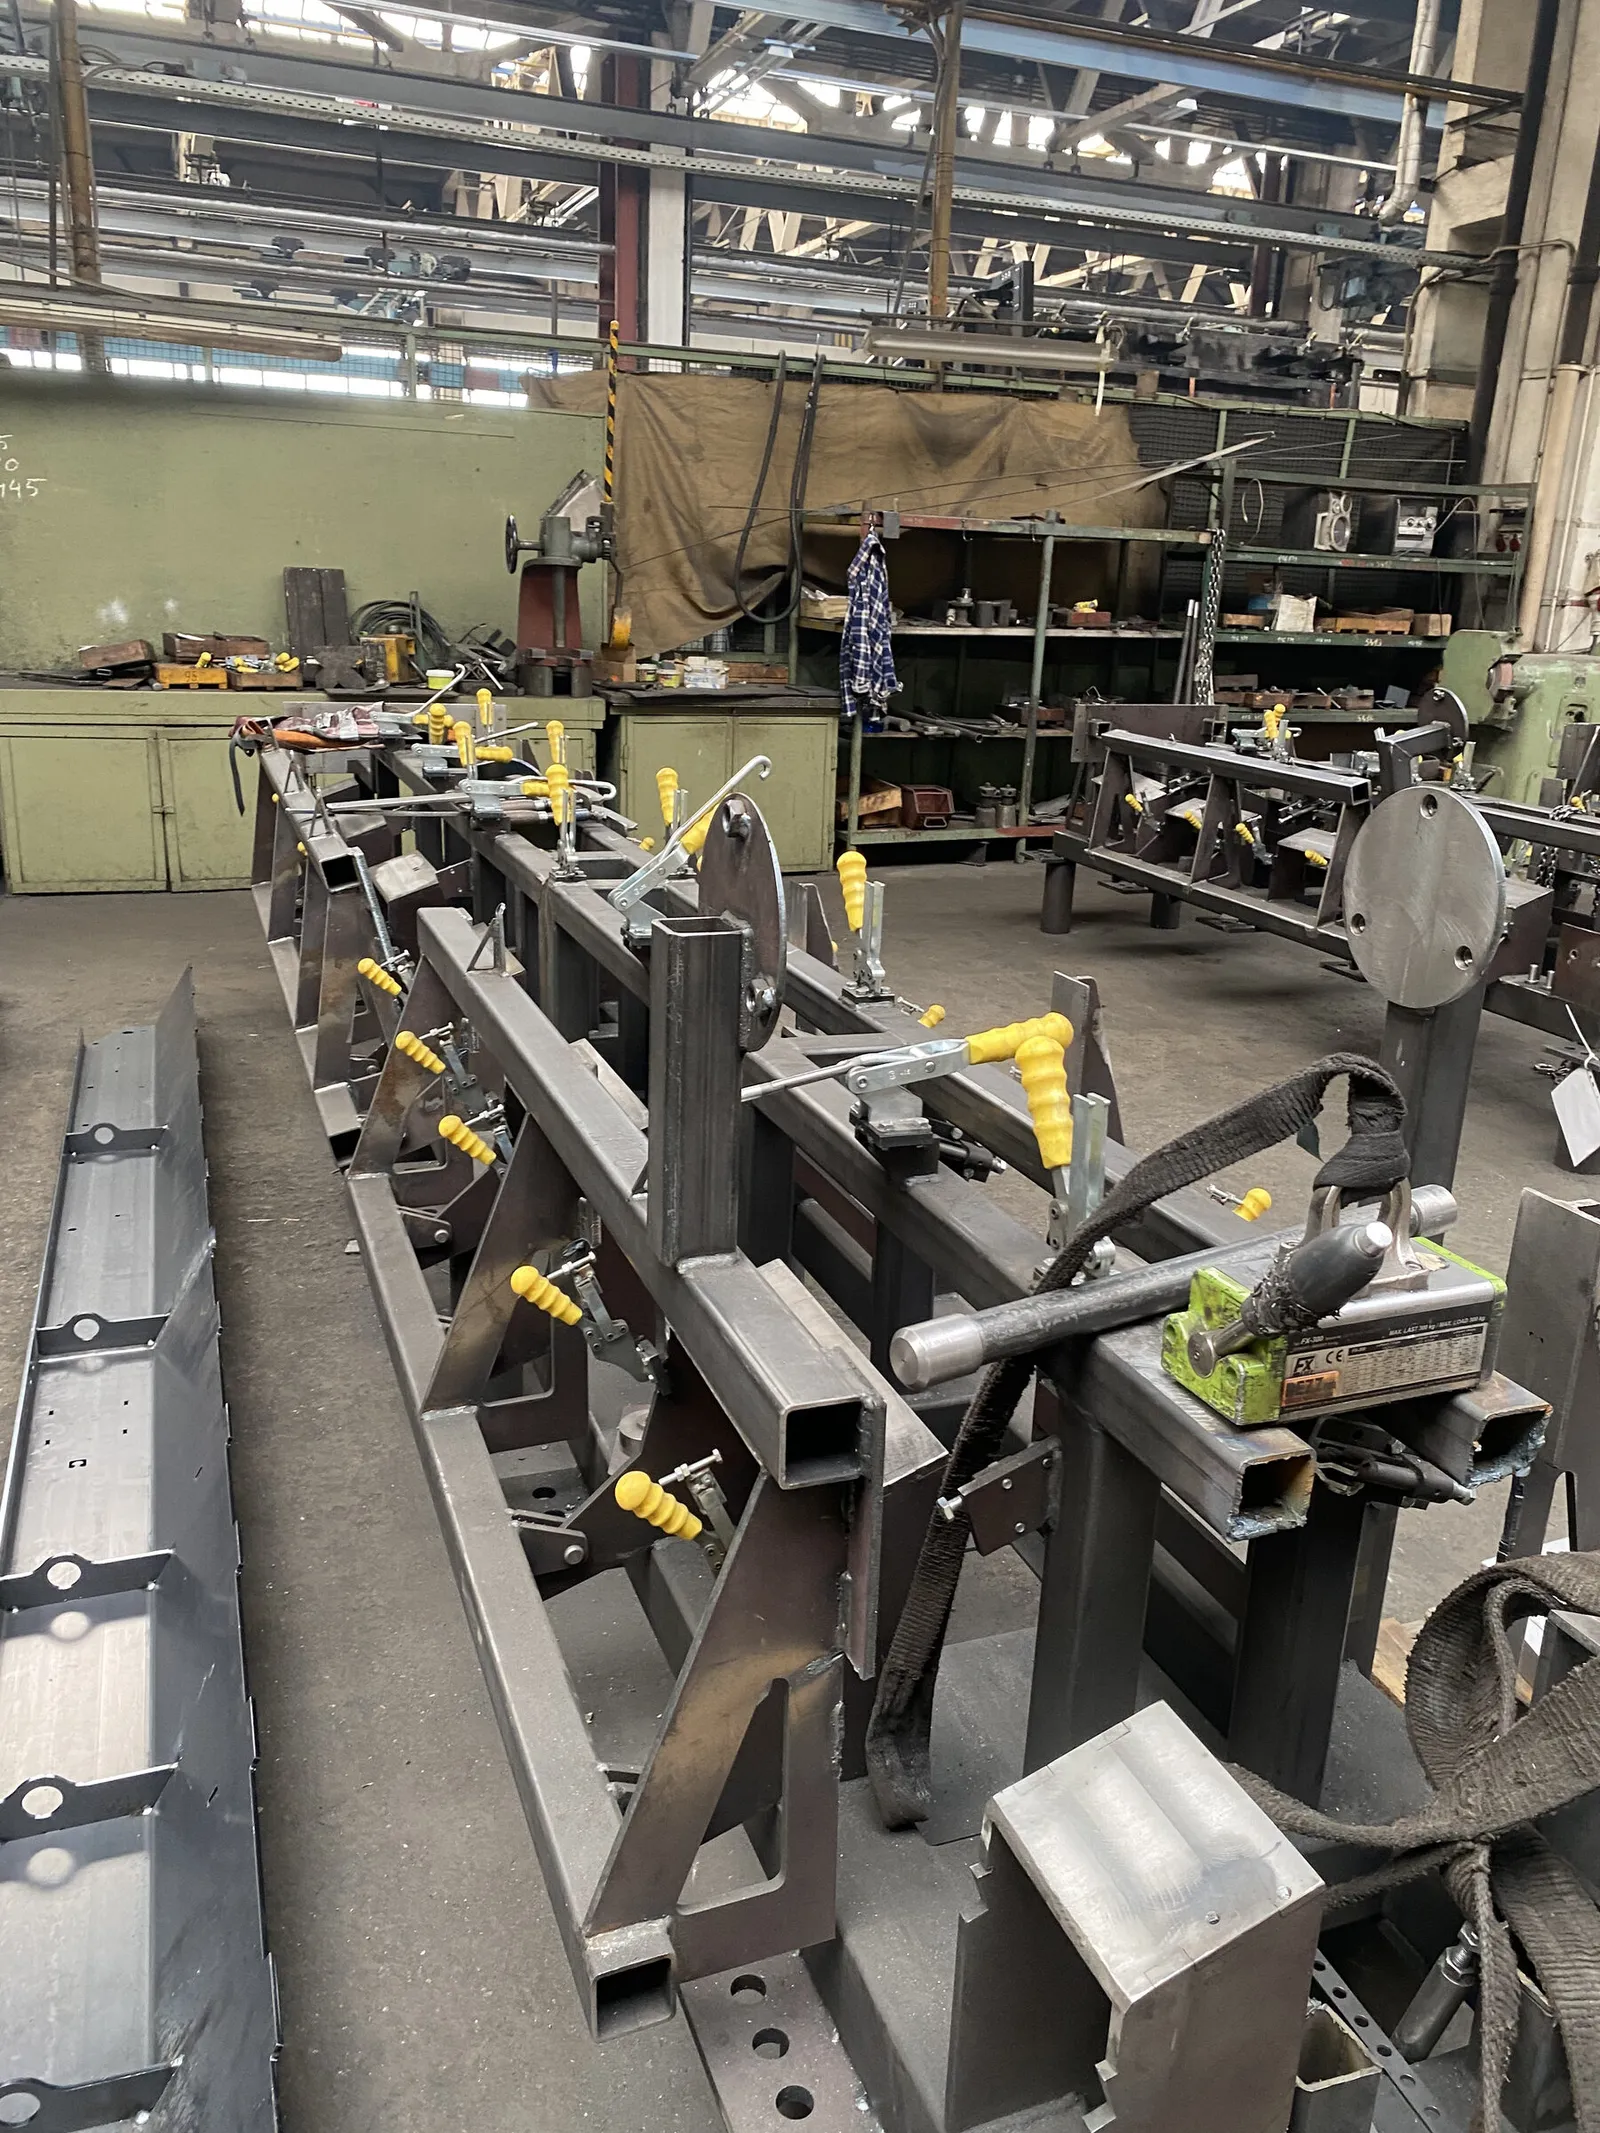
Long frame clamped in a welding jig 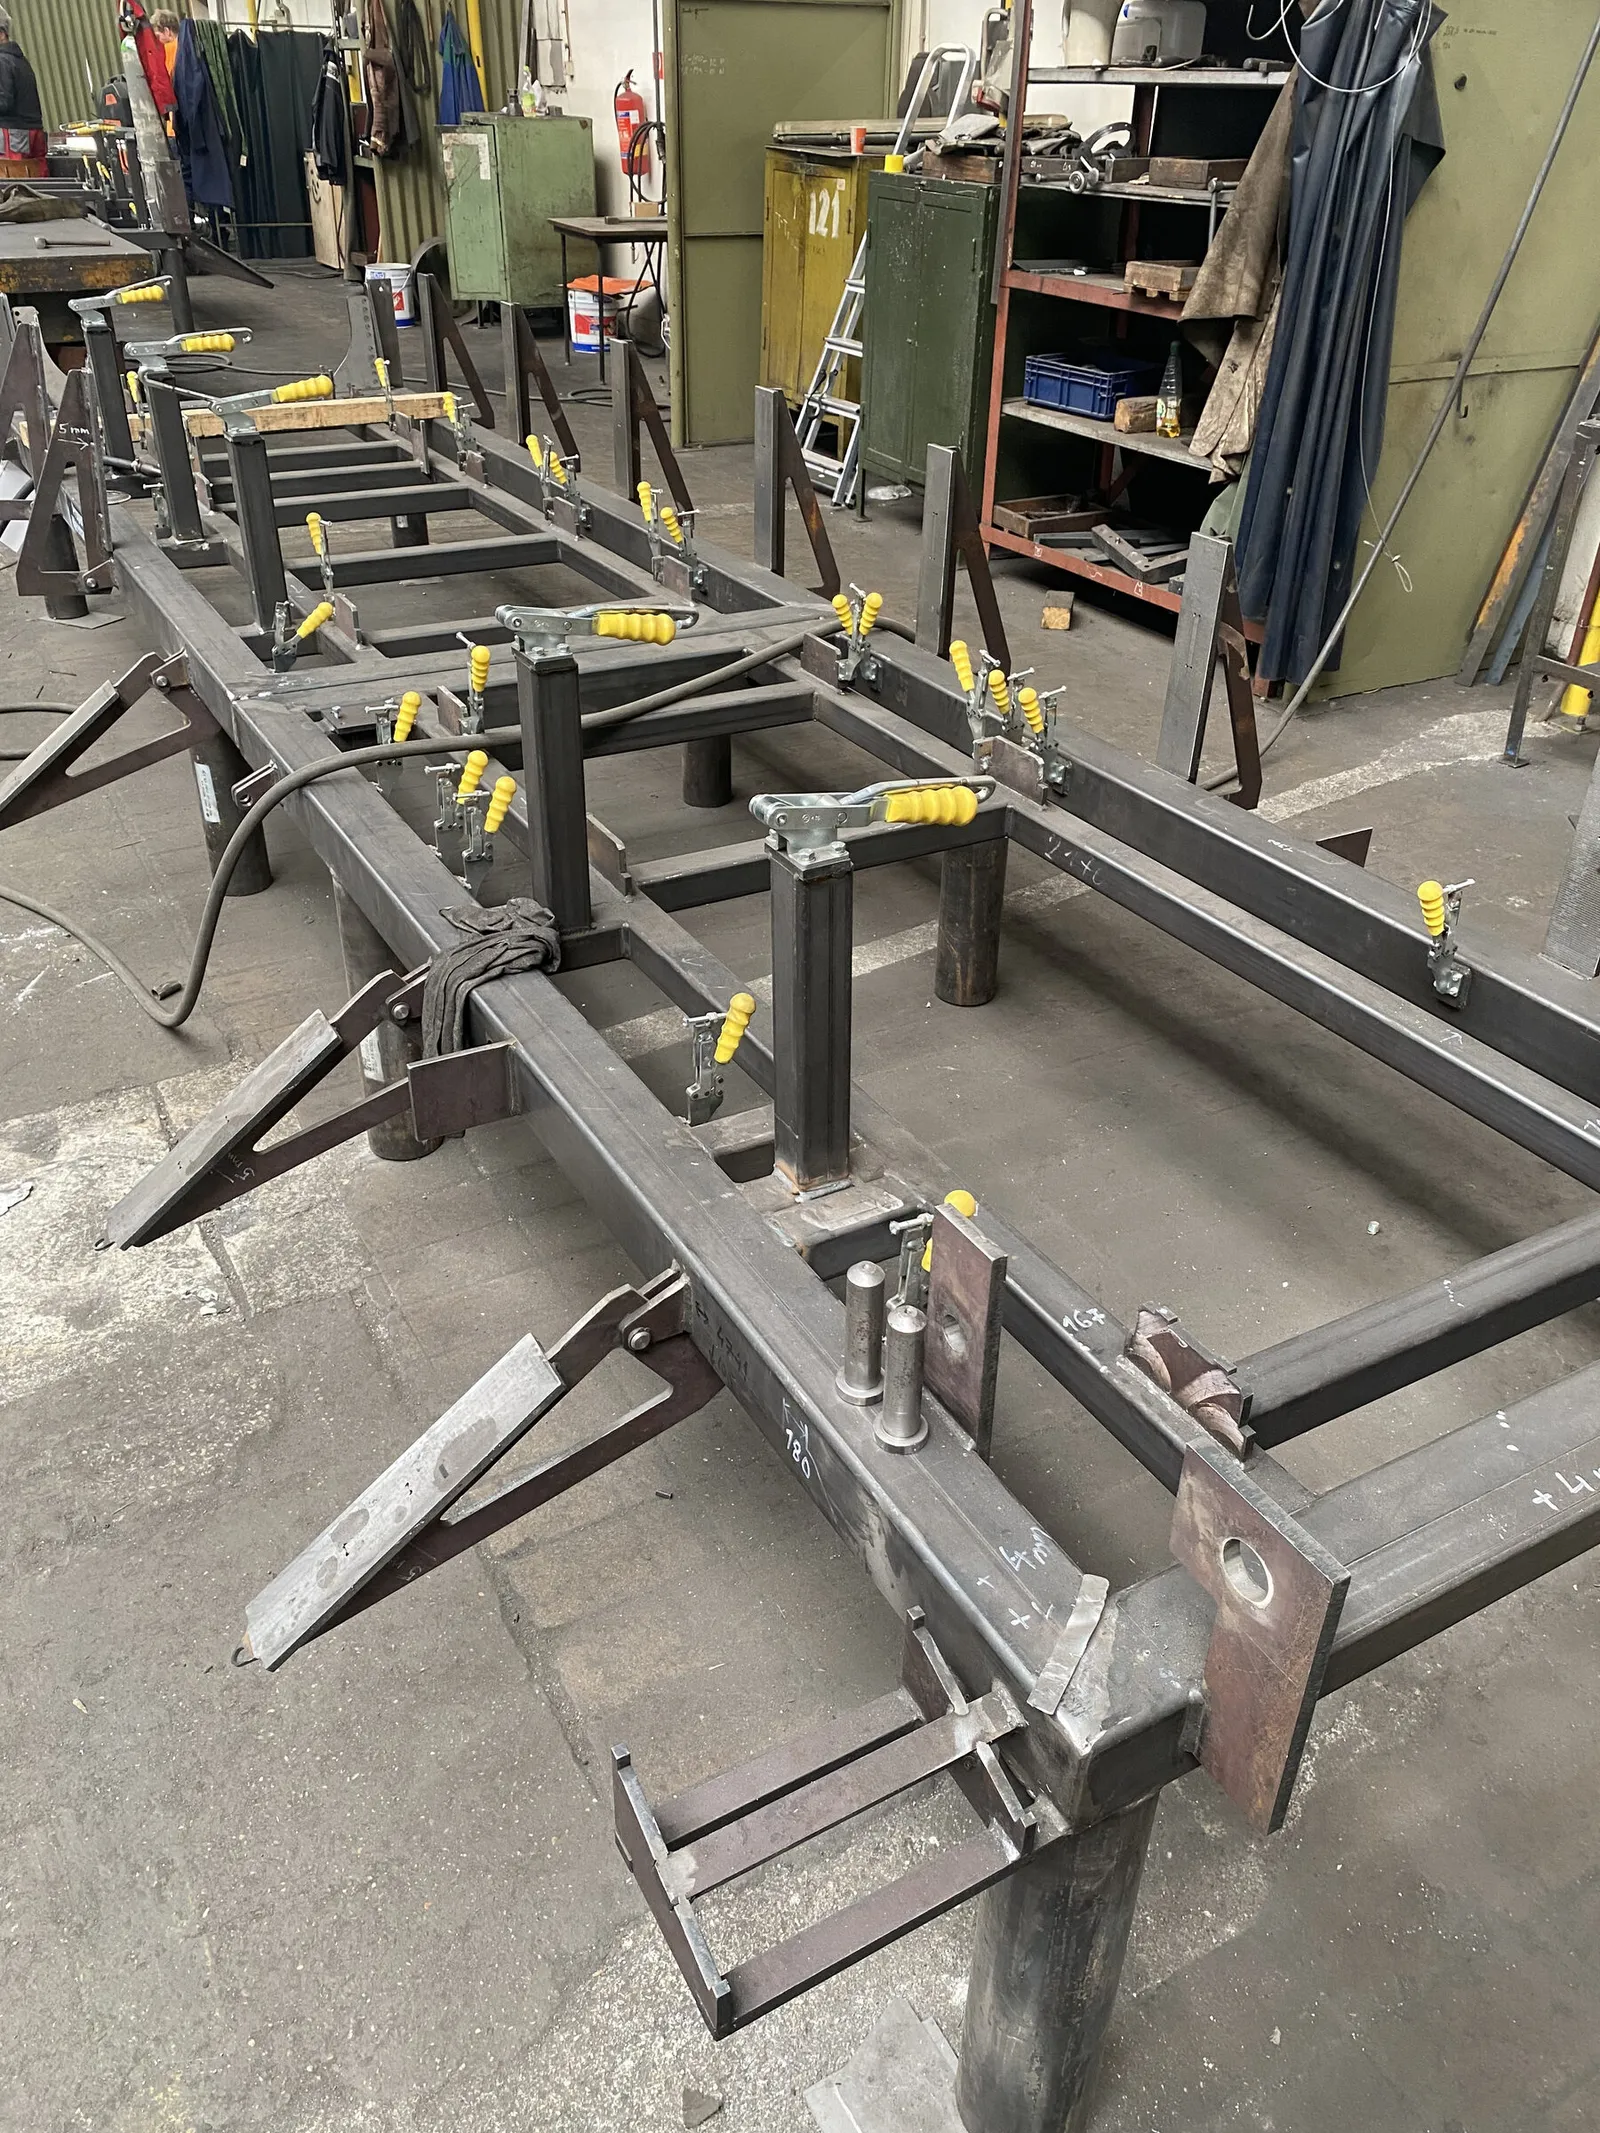
Frame in the welding jig, seen from the end 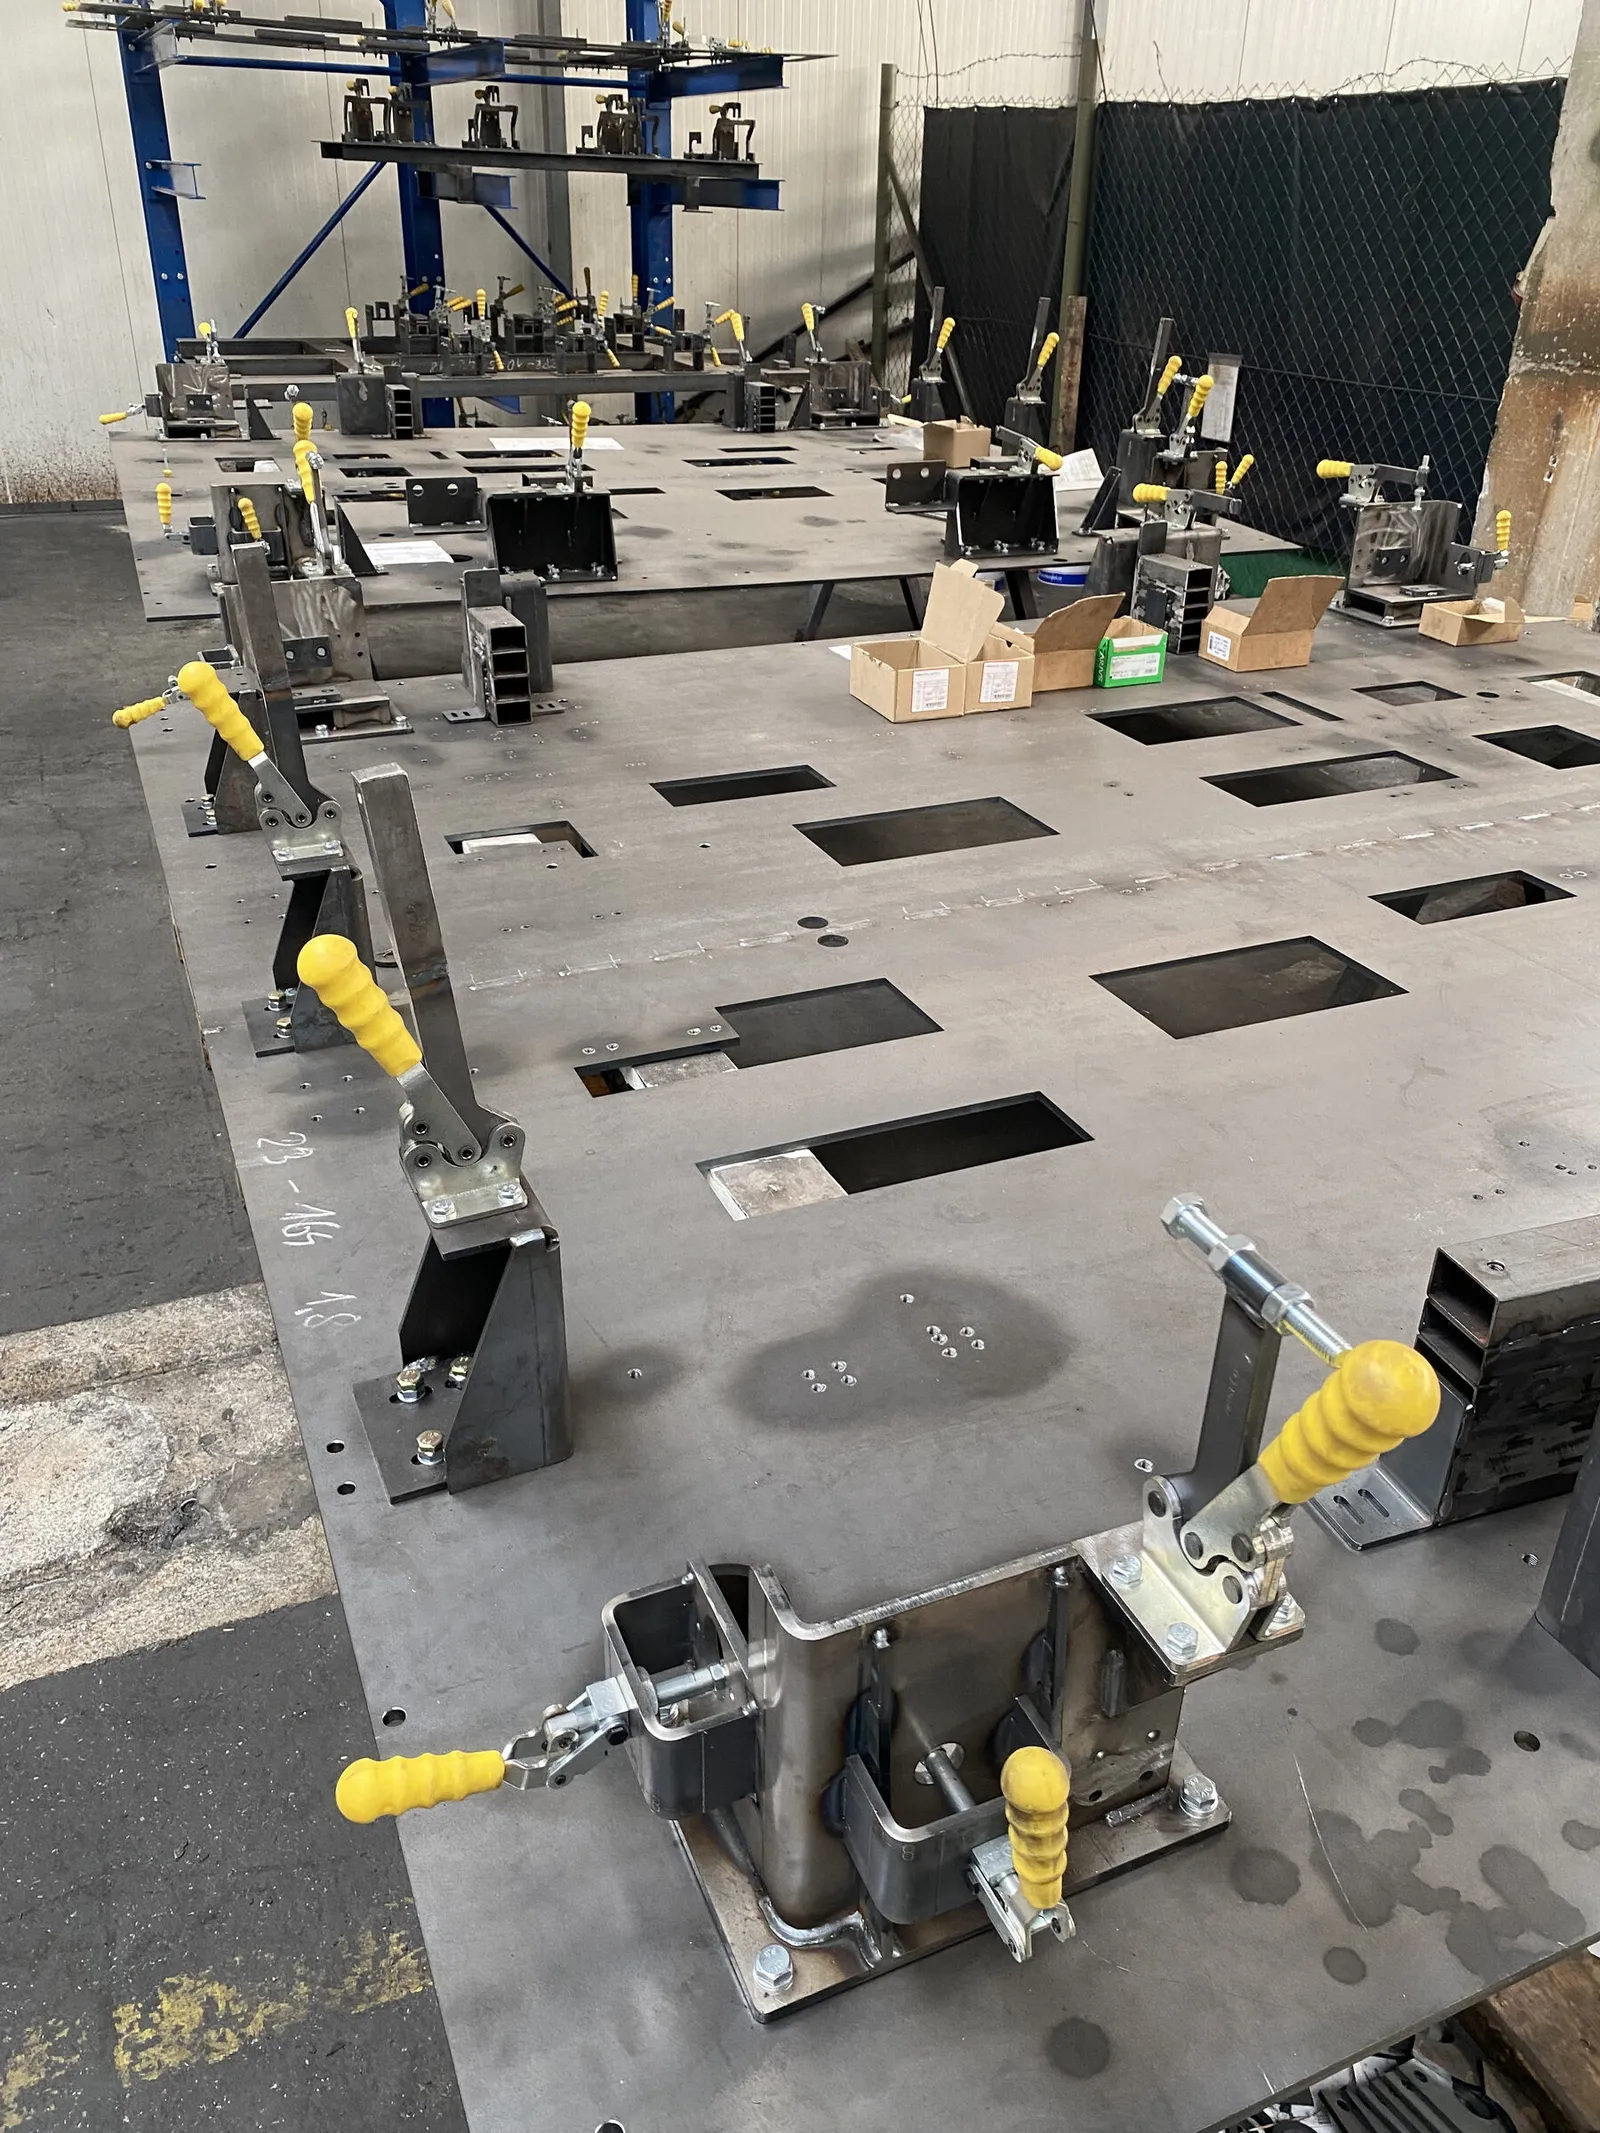
Perforated jig table with clamps with yellow handles 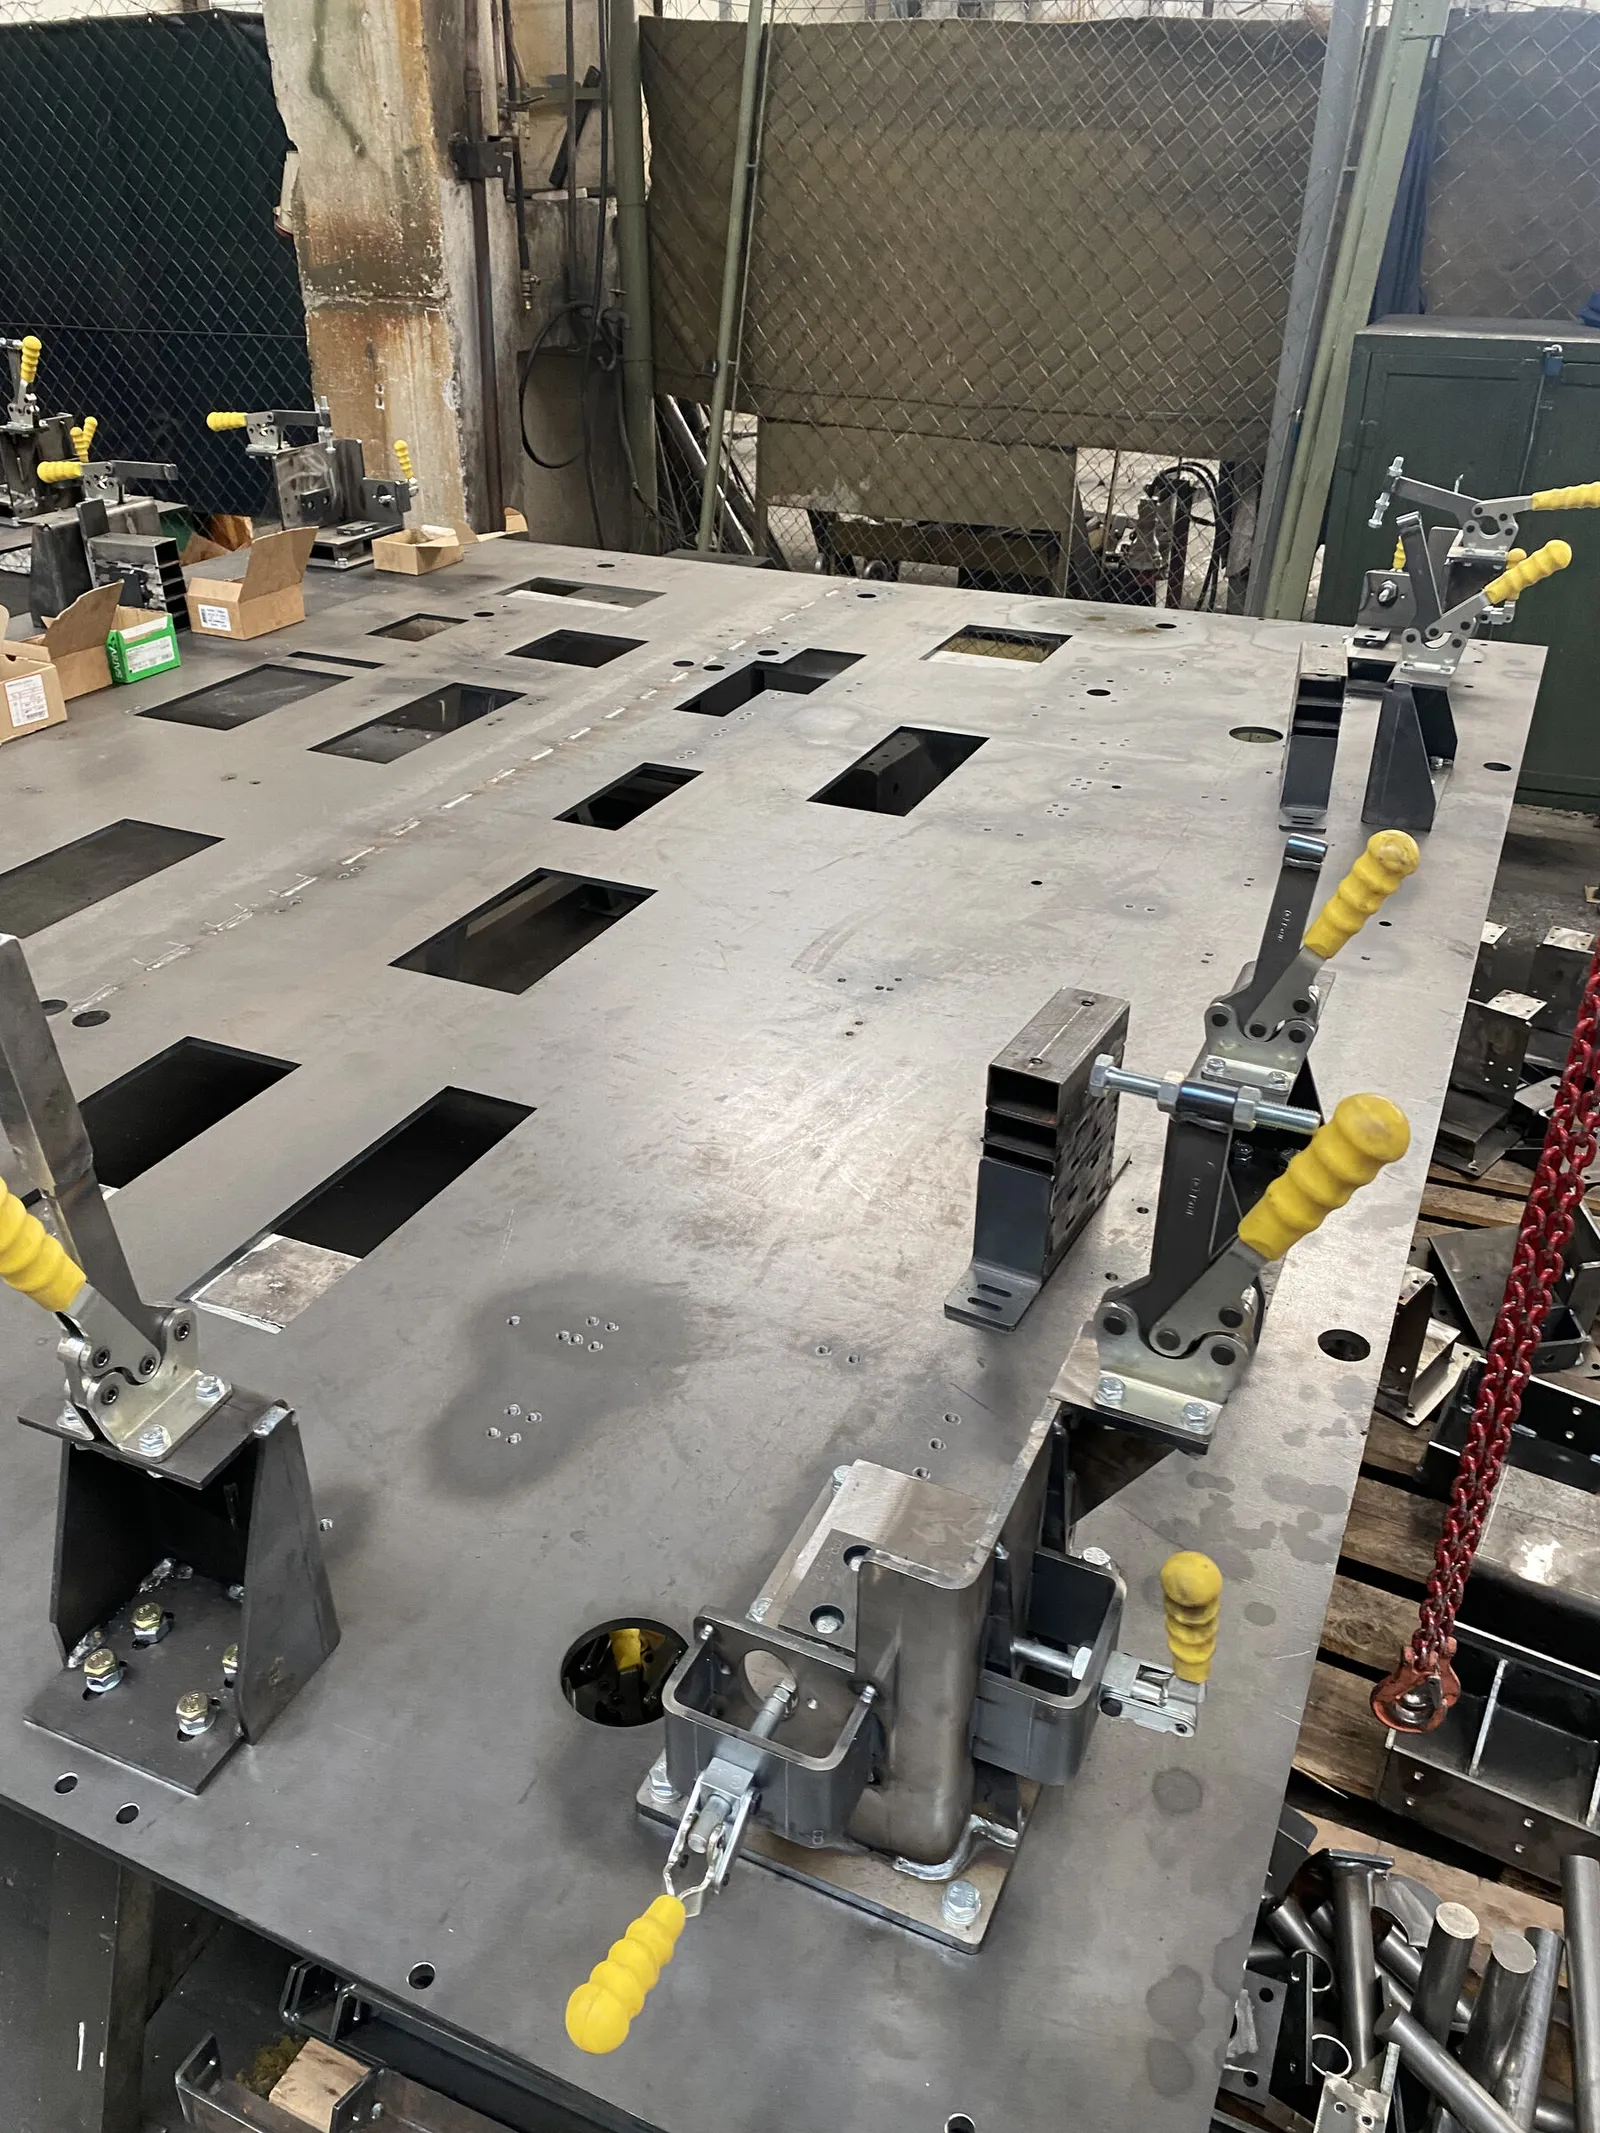
Jig table with stops and fixtures 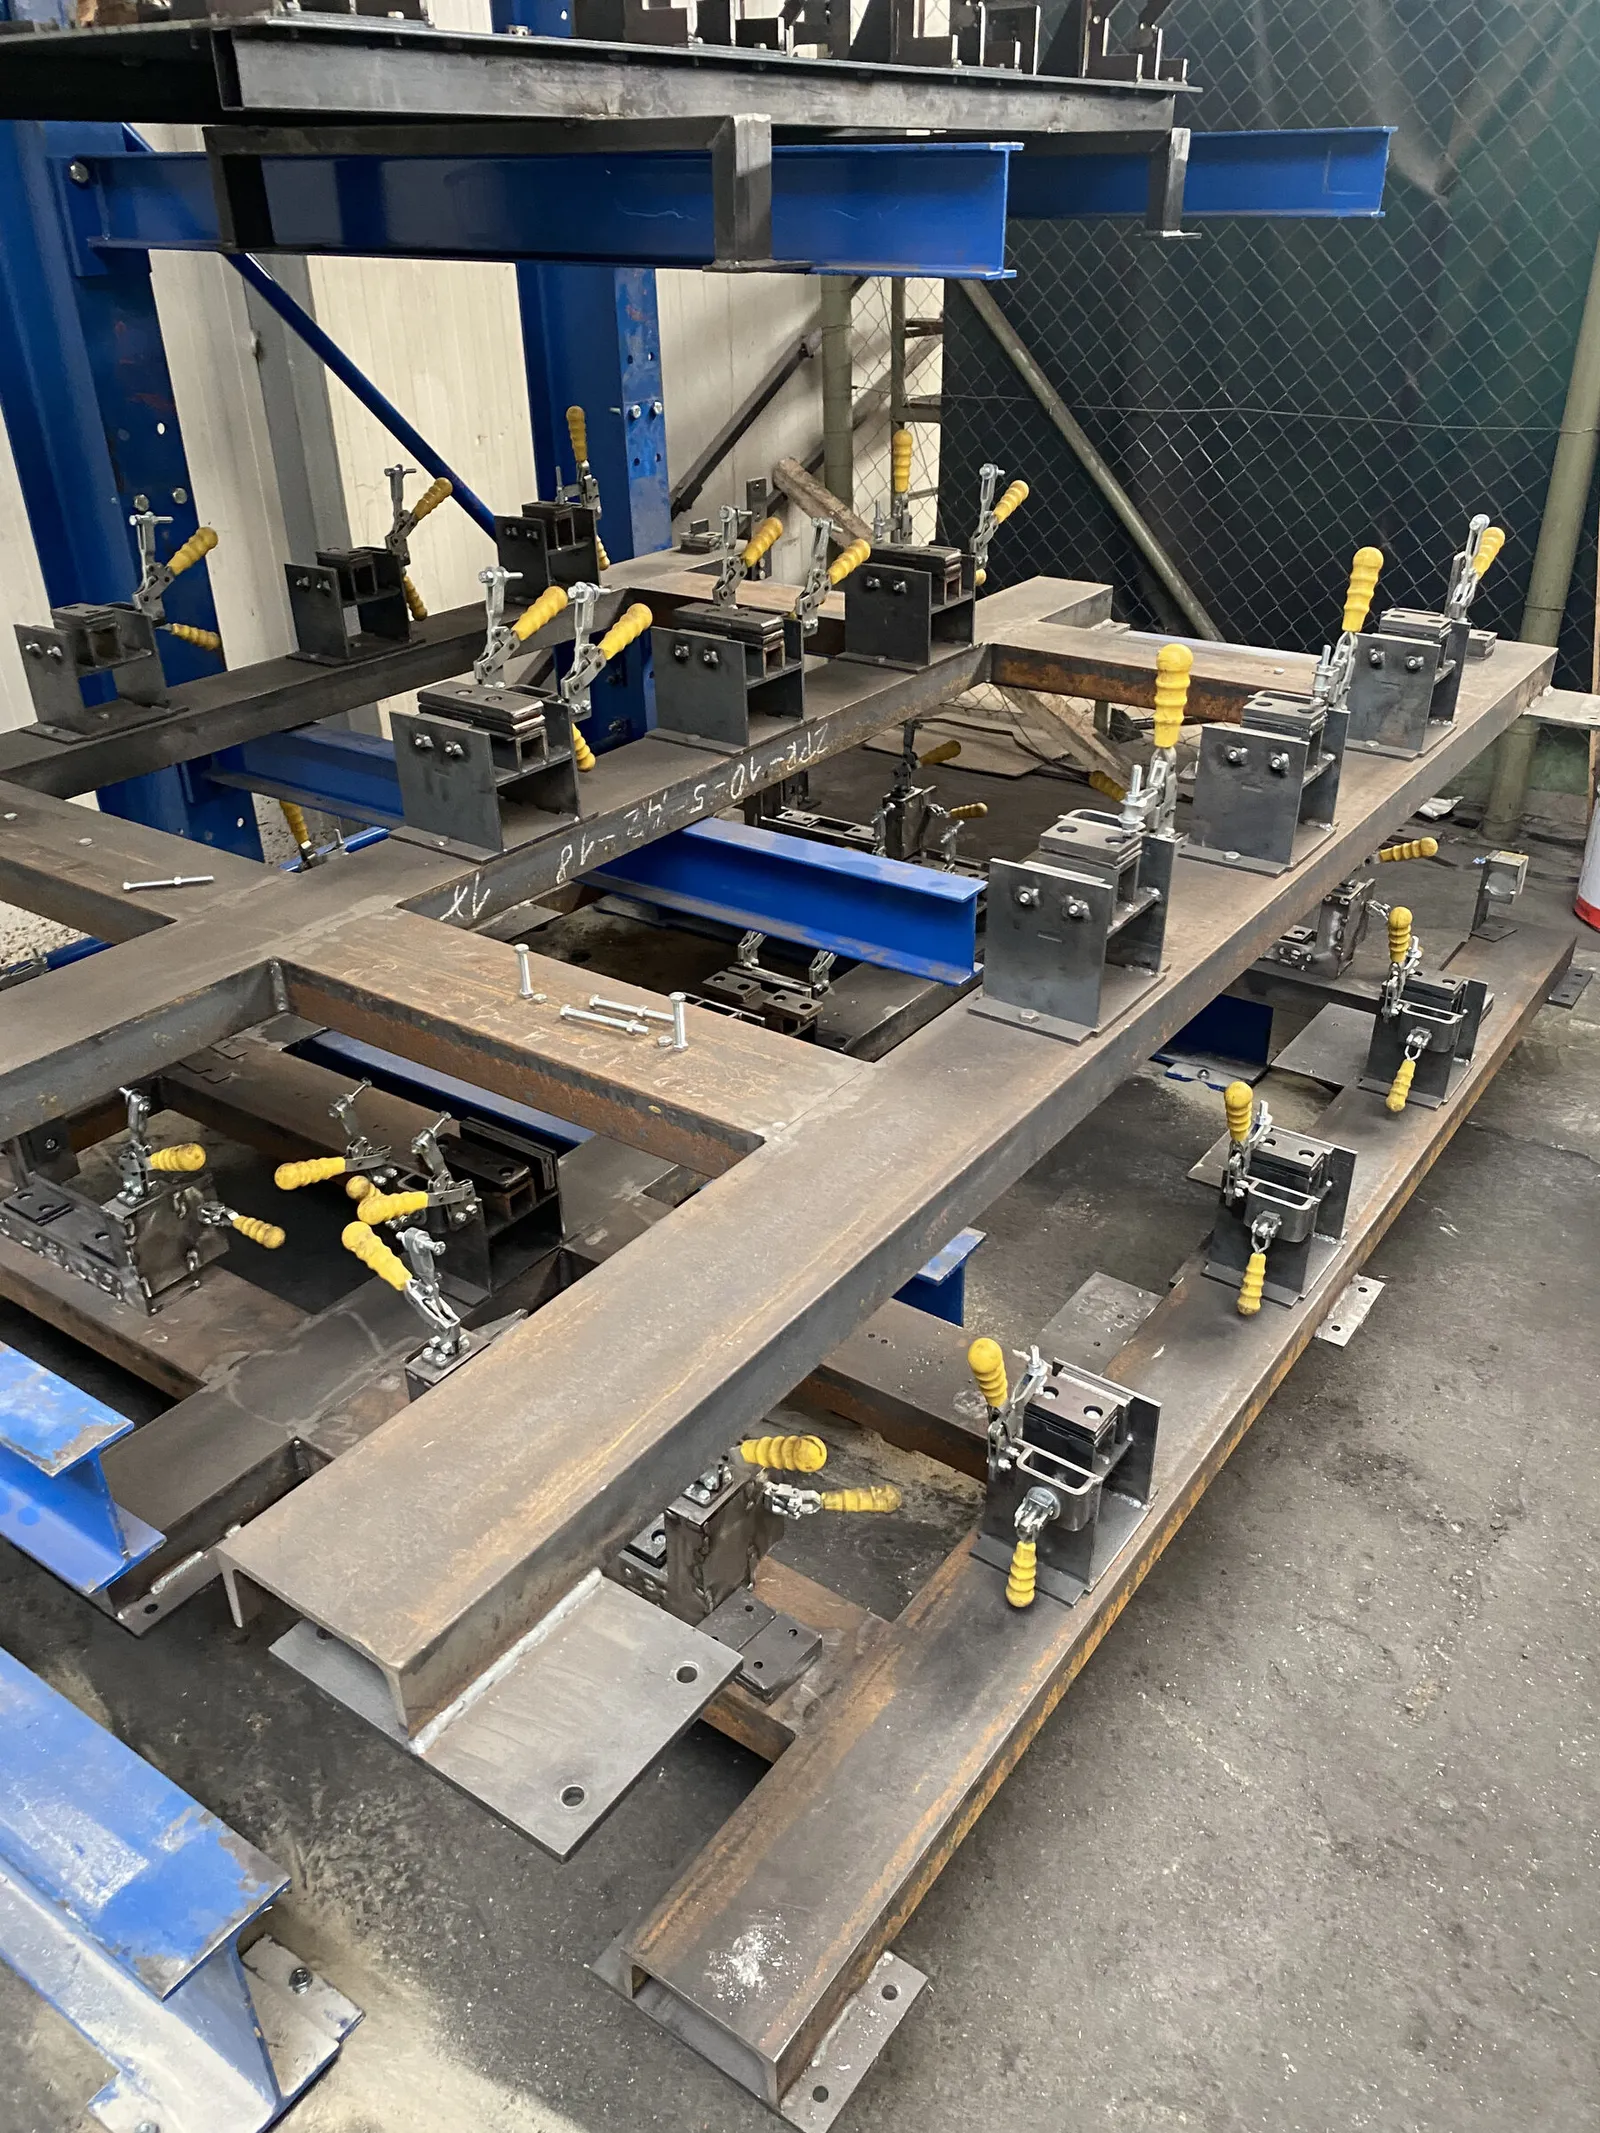
Fixture on blue stands with clamps 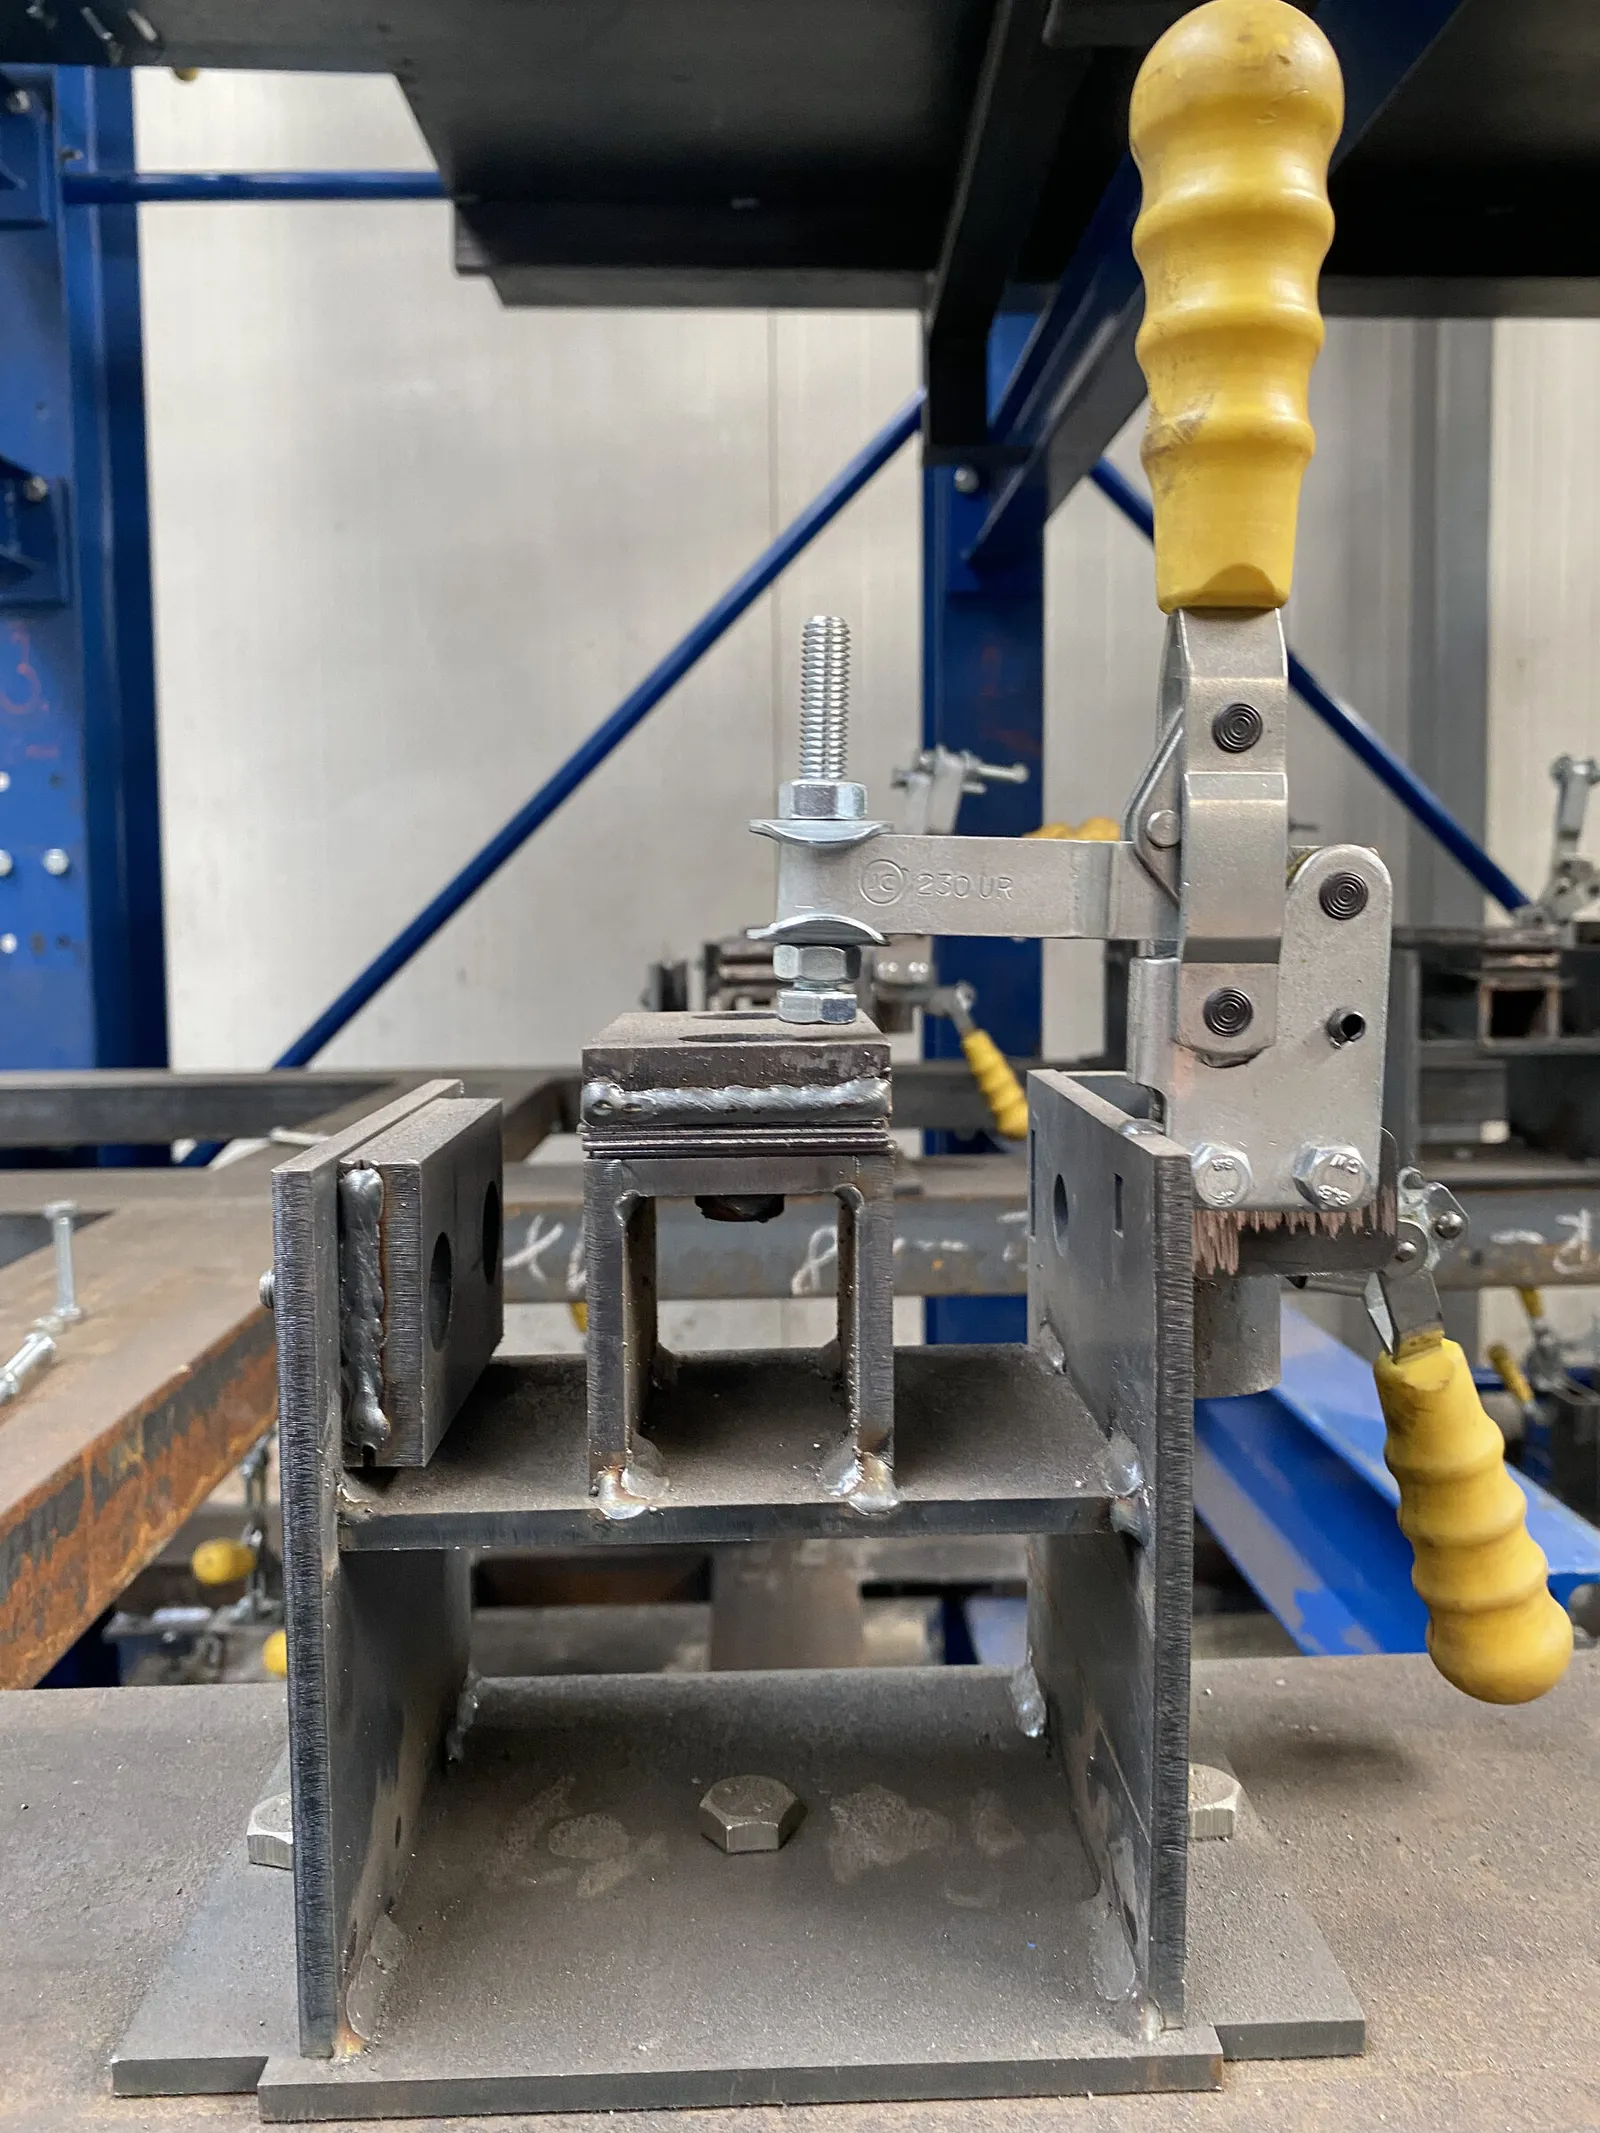
Toggle clamp on a fixture, close-up
Machine frames
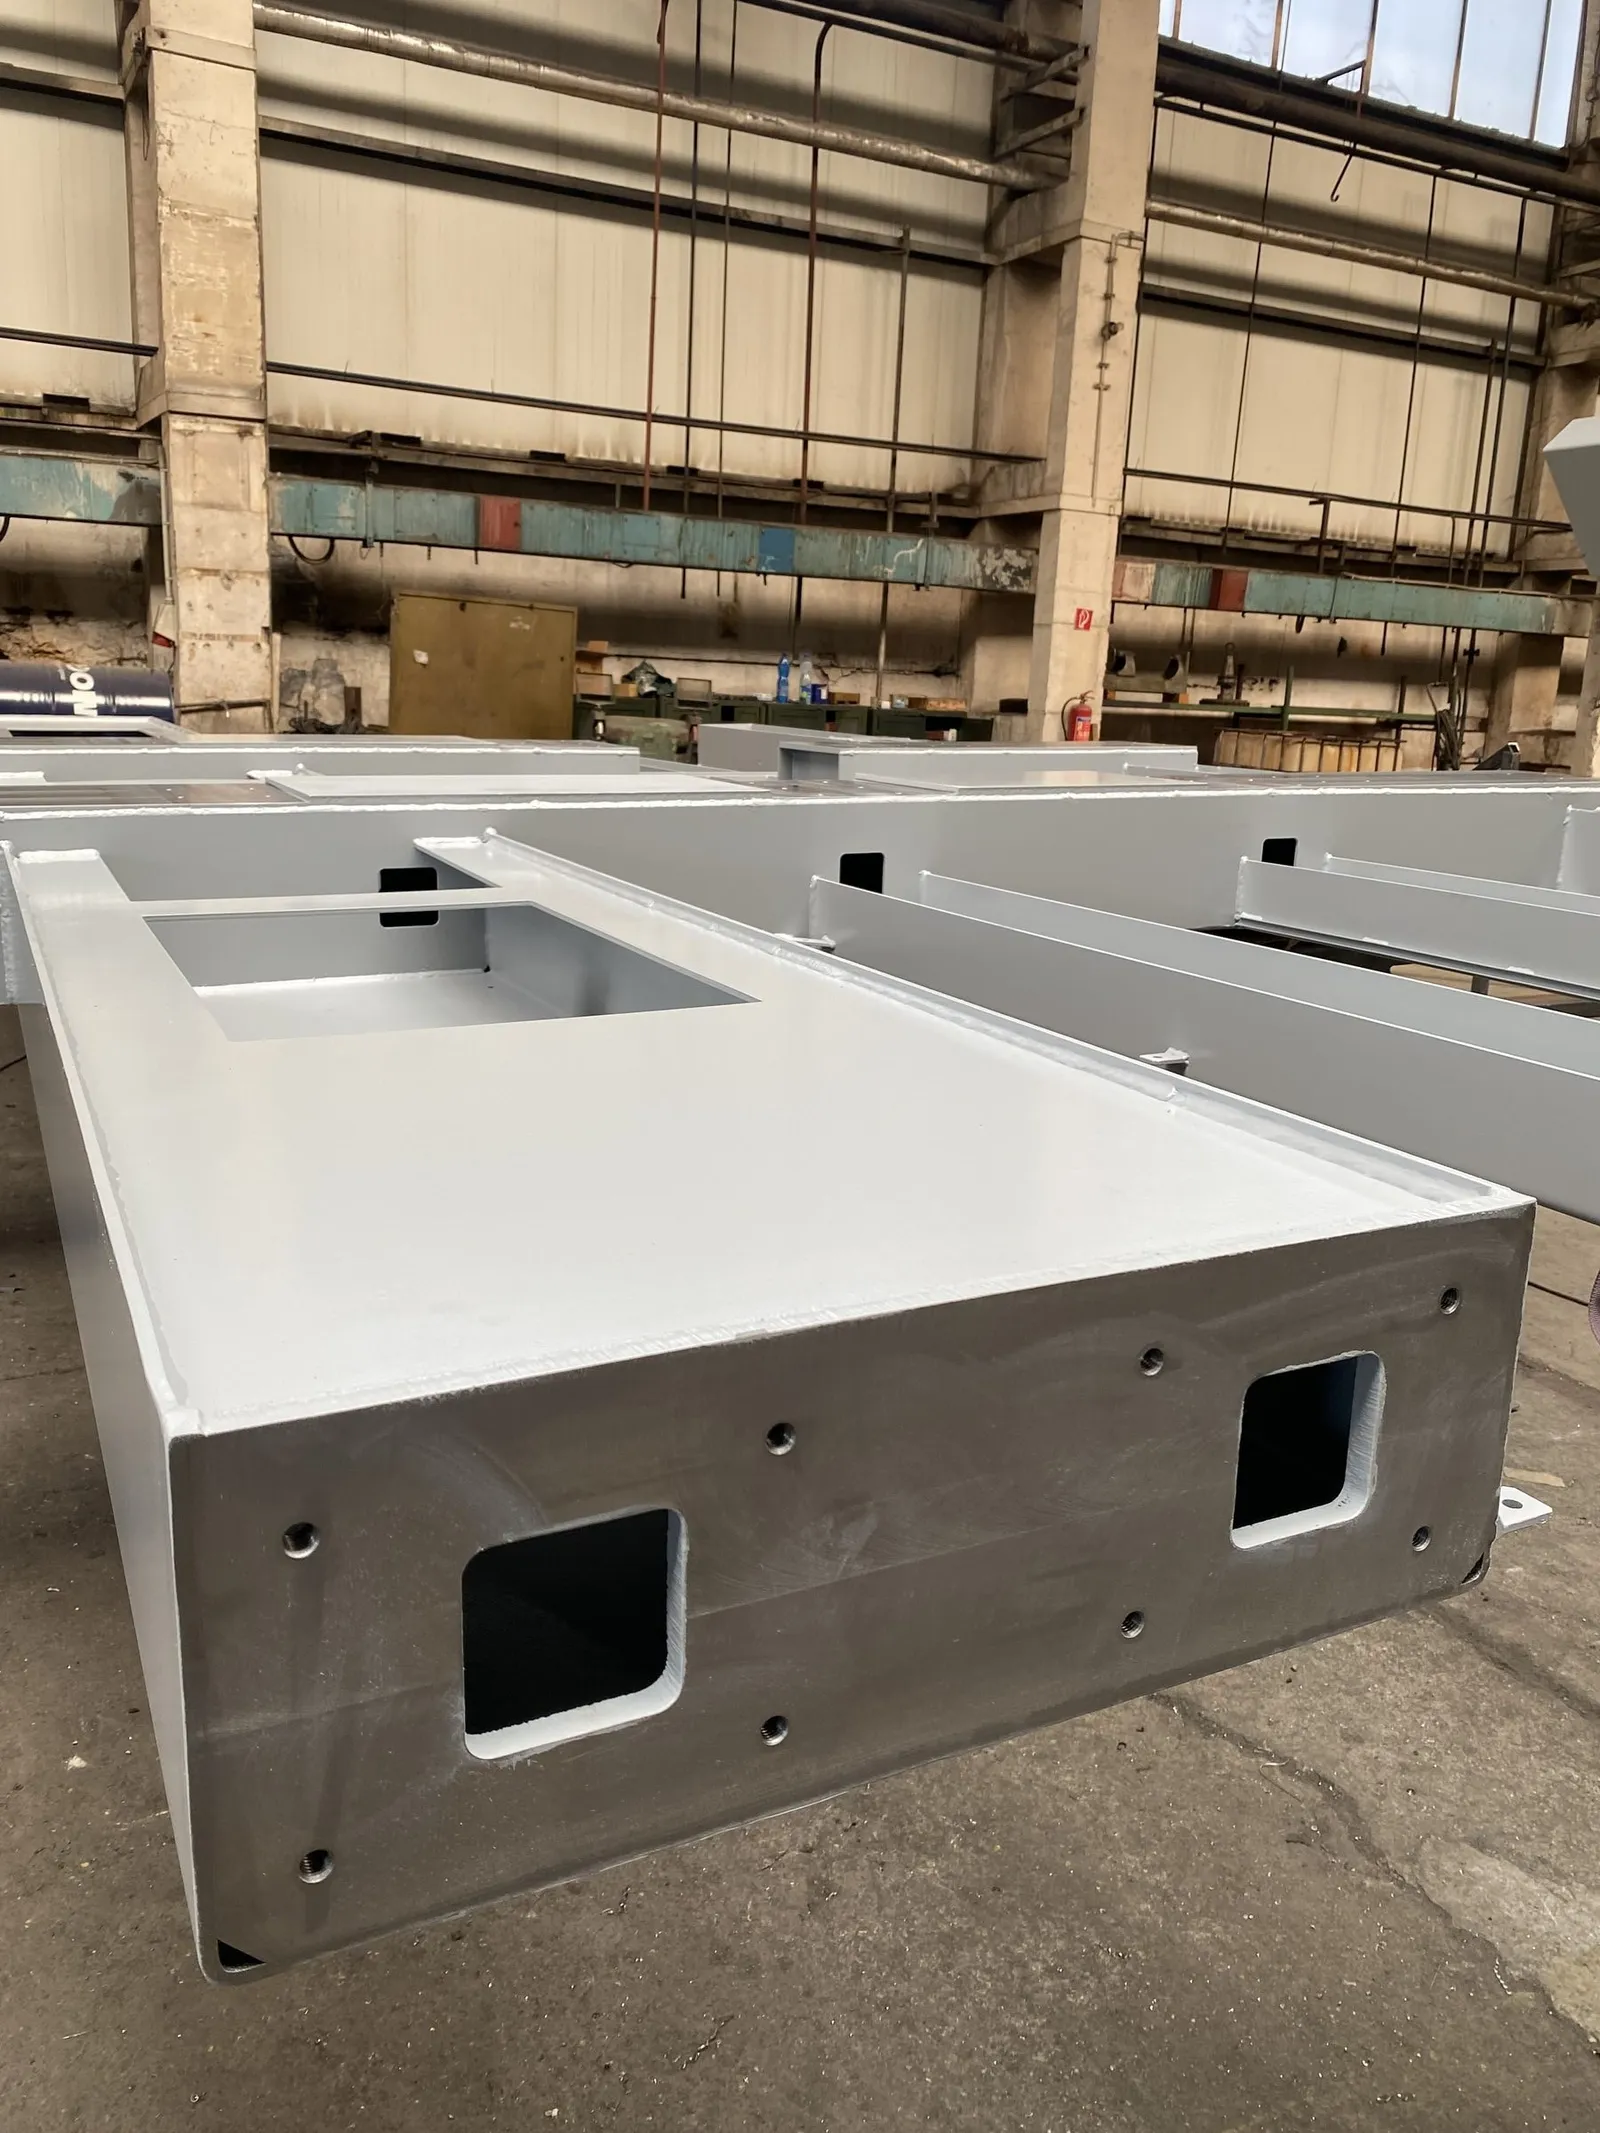
Machine frame base with machined faces 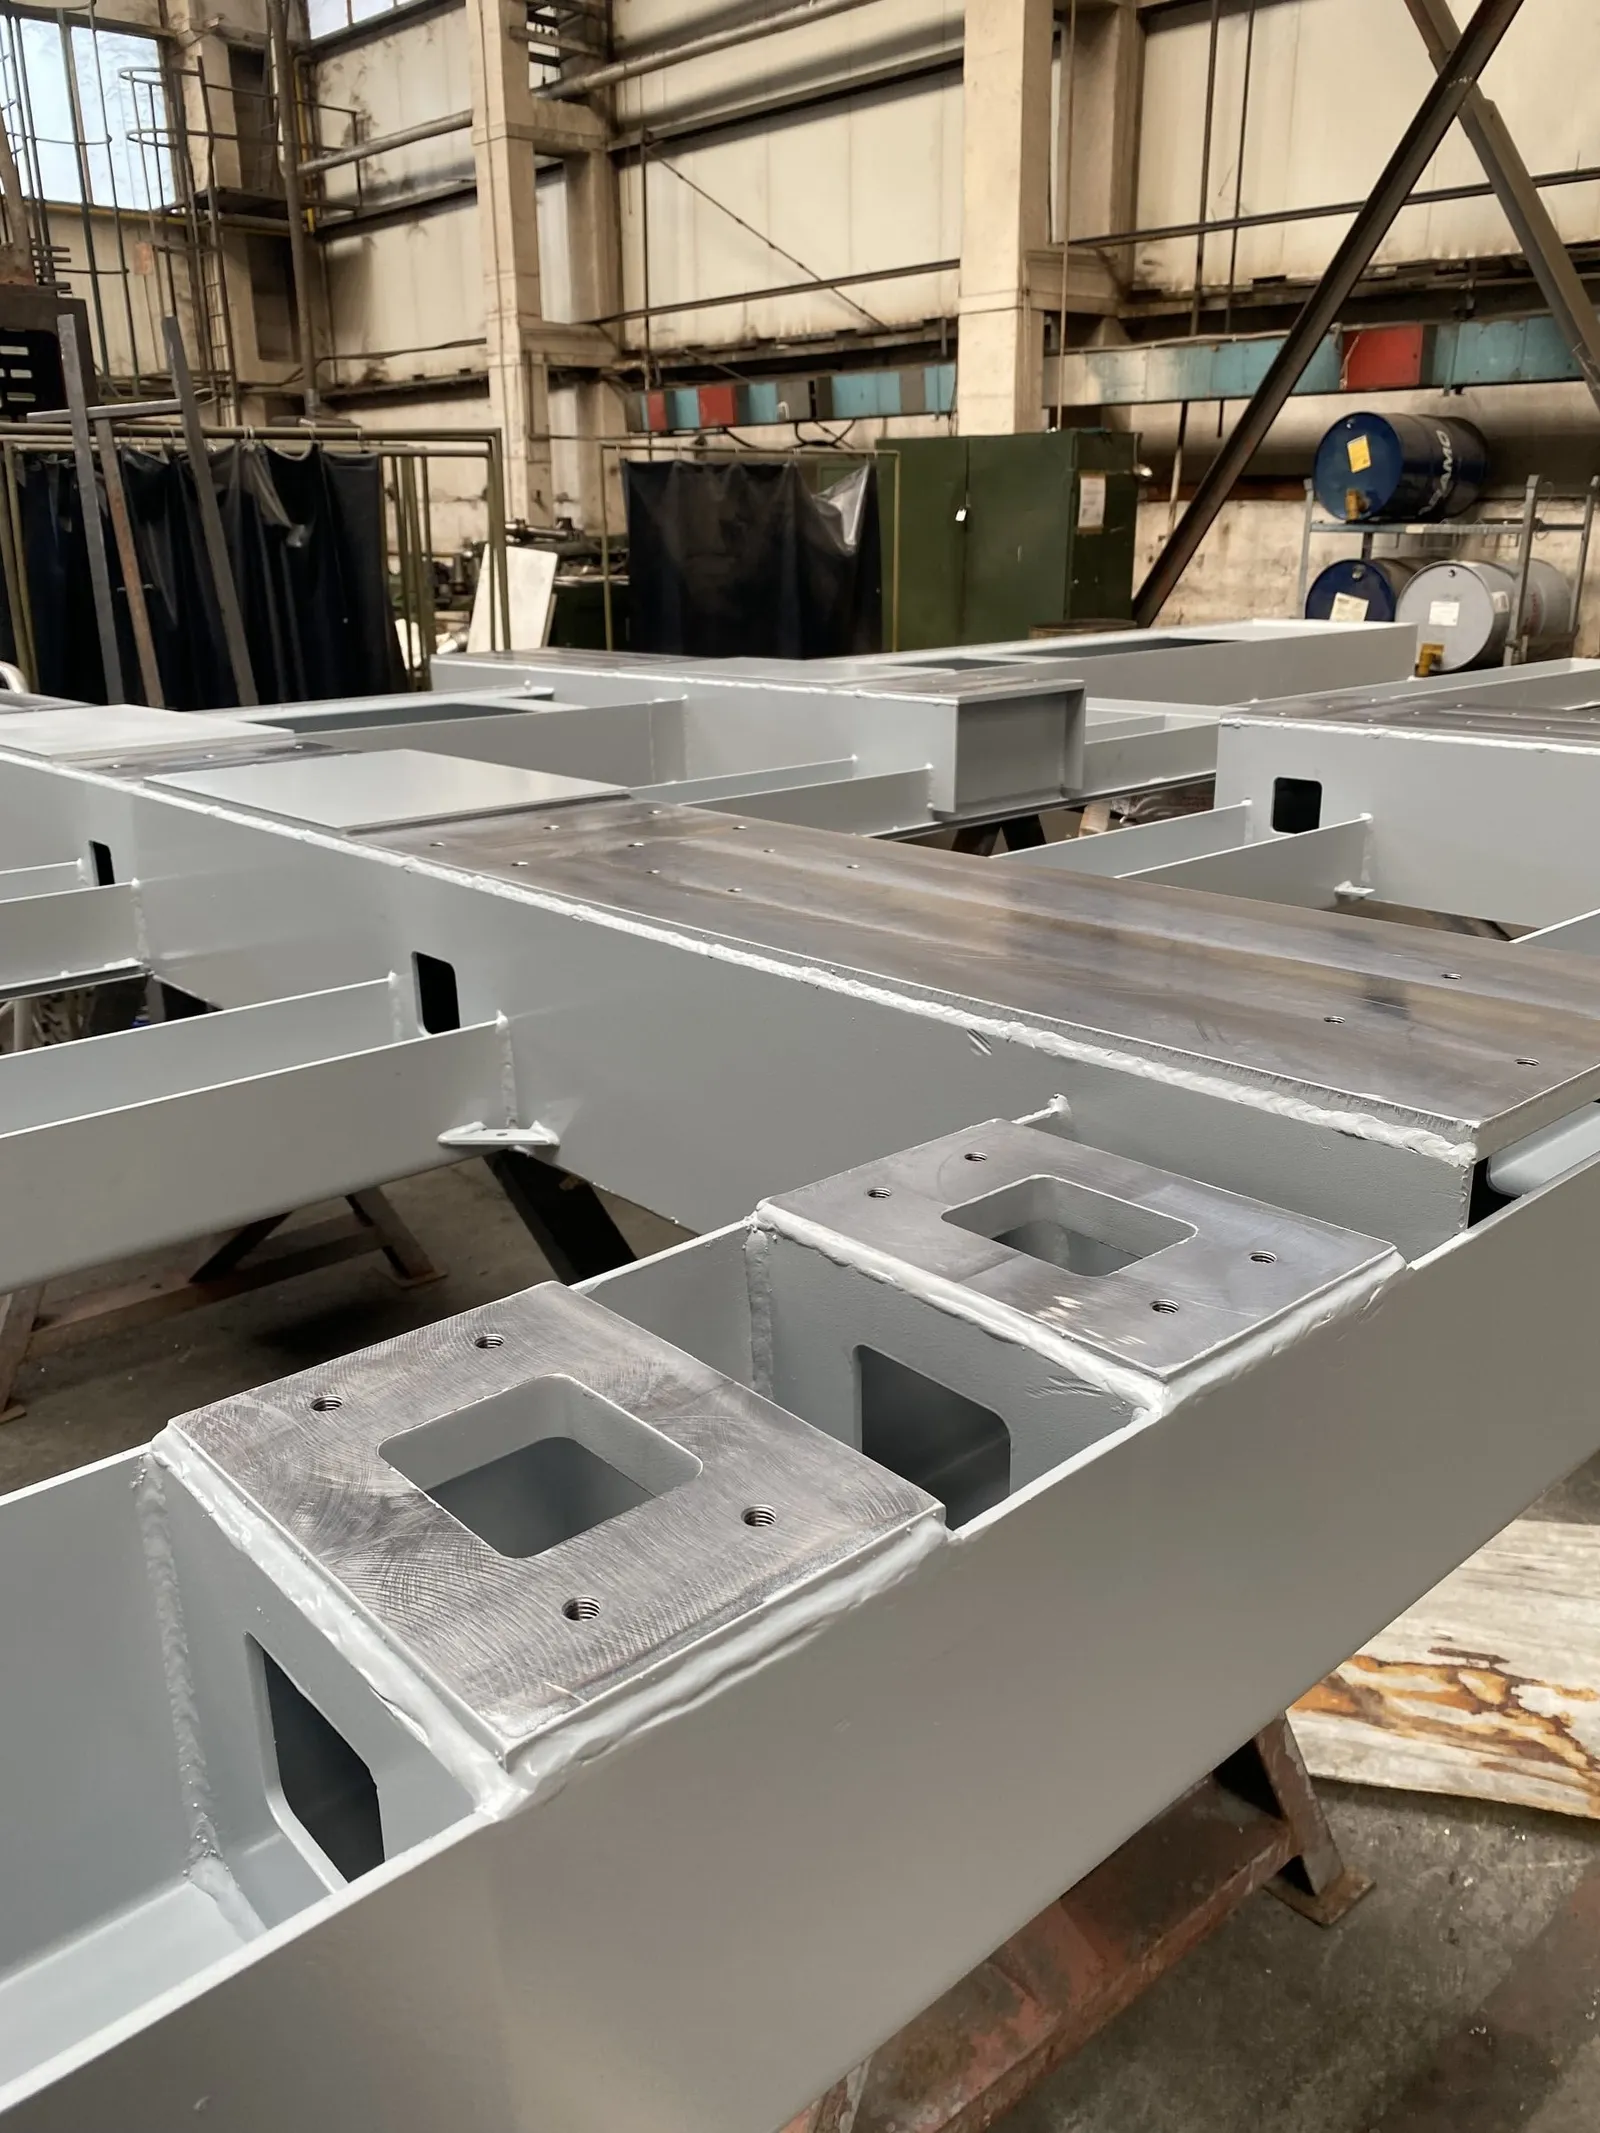
Long machine frame, welded and machined 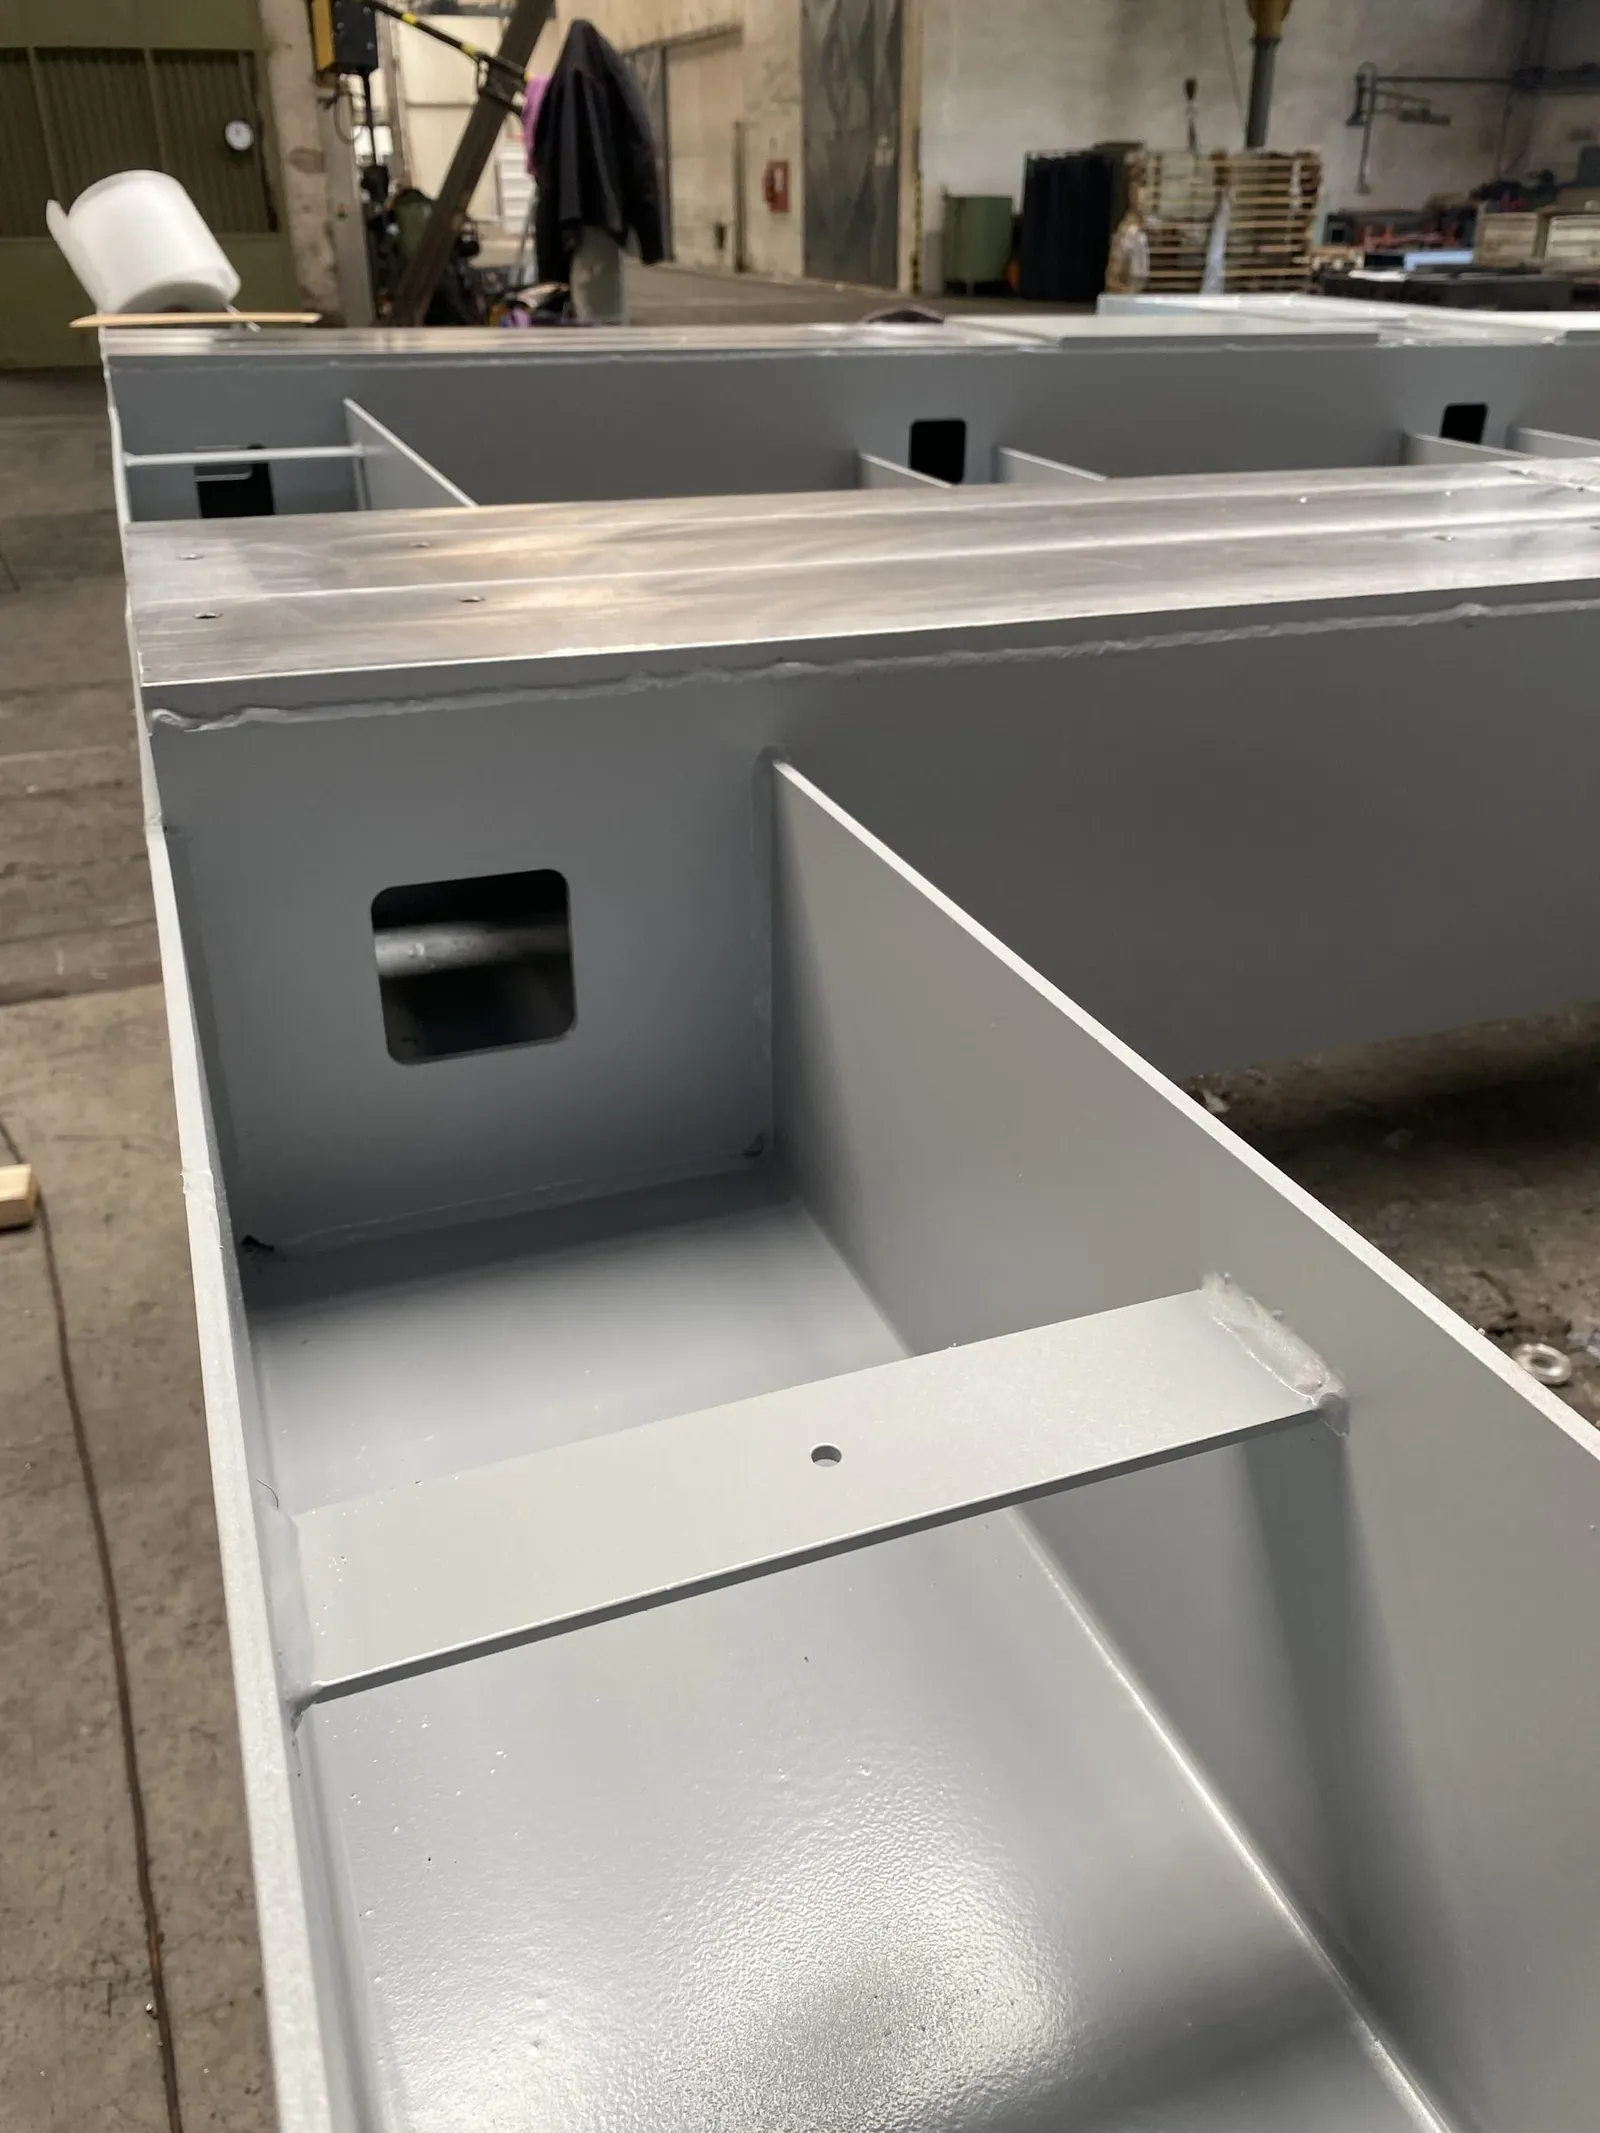
Machine frame with bored mounting holes 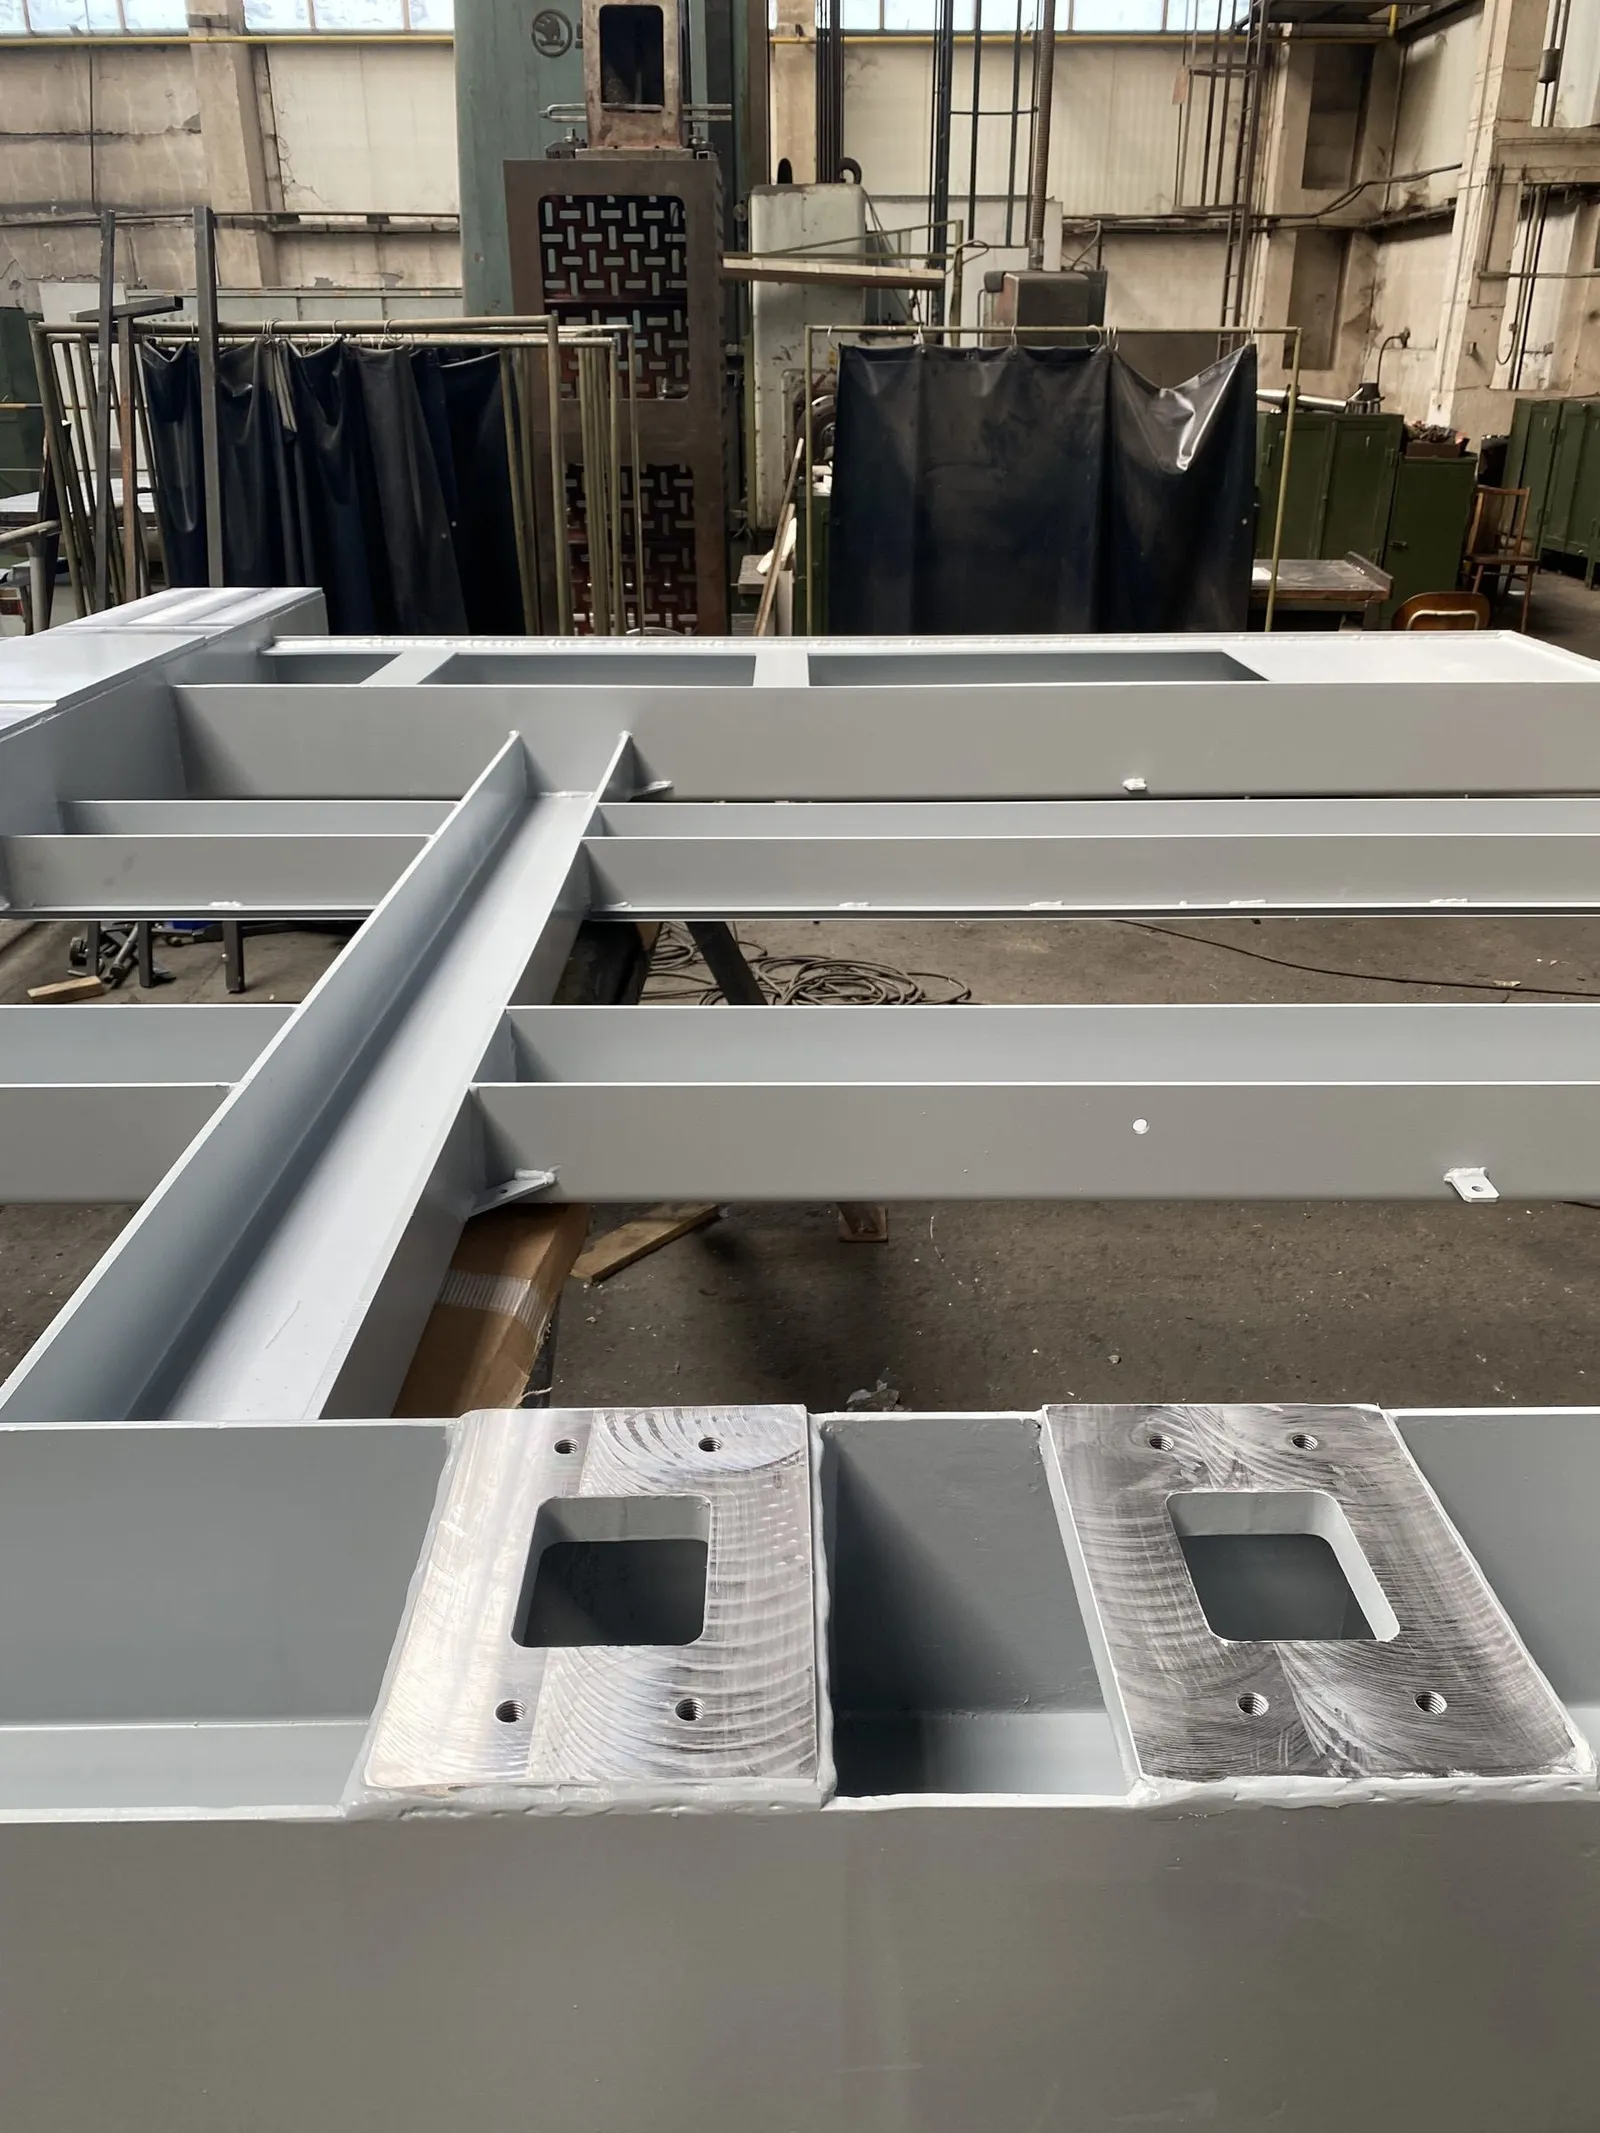
Machined frame end, painted grey
Loader chassis and subframes
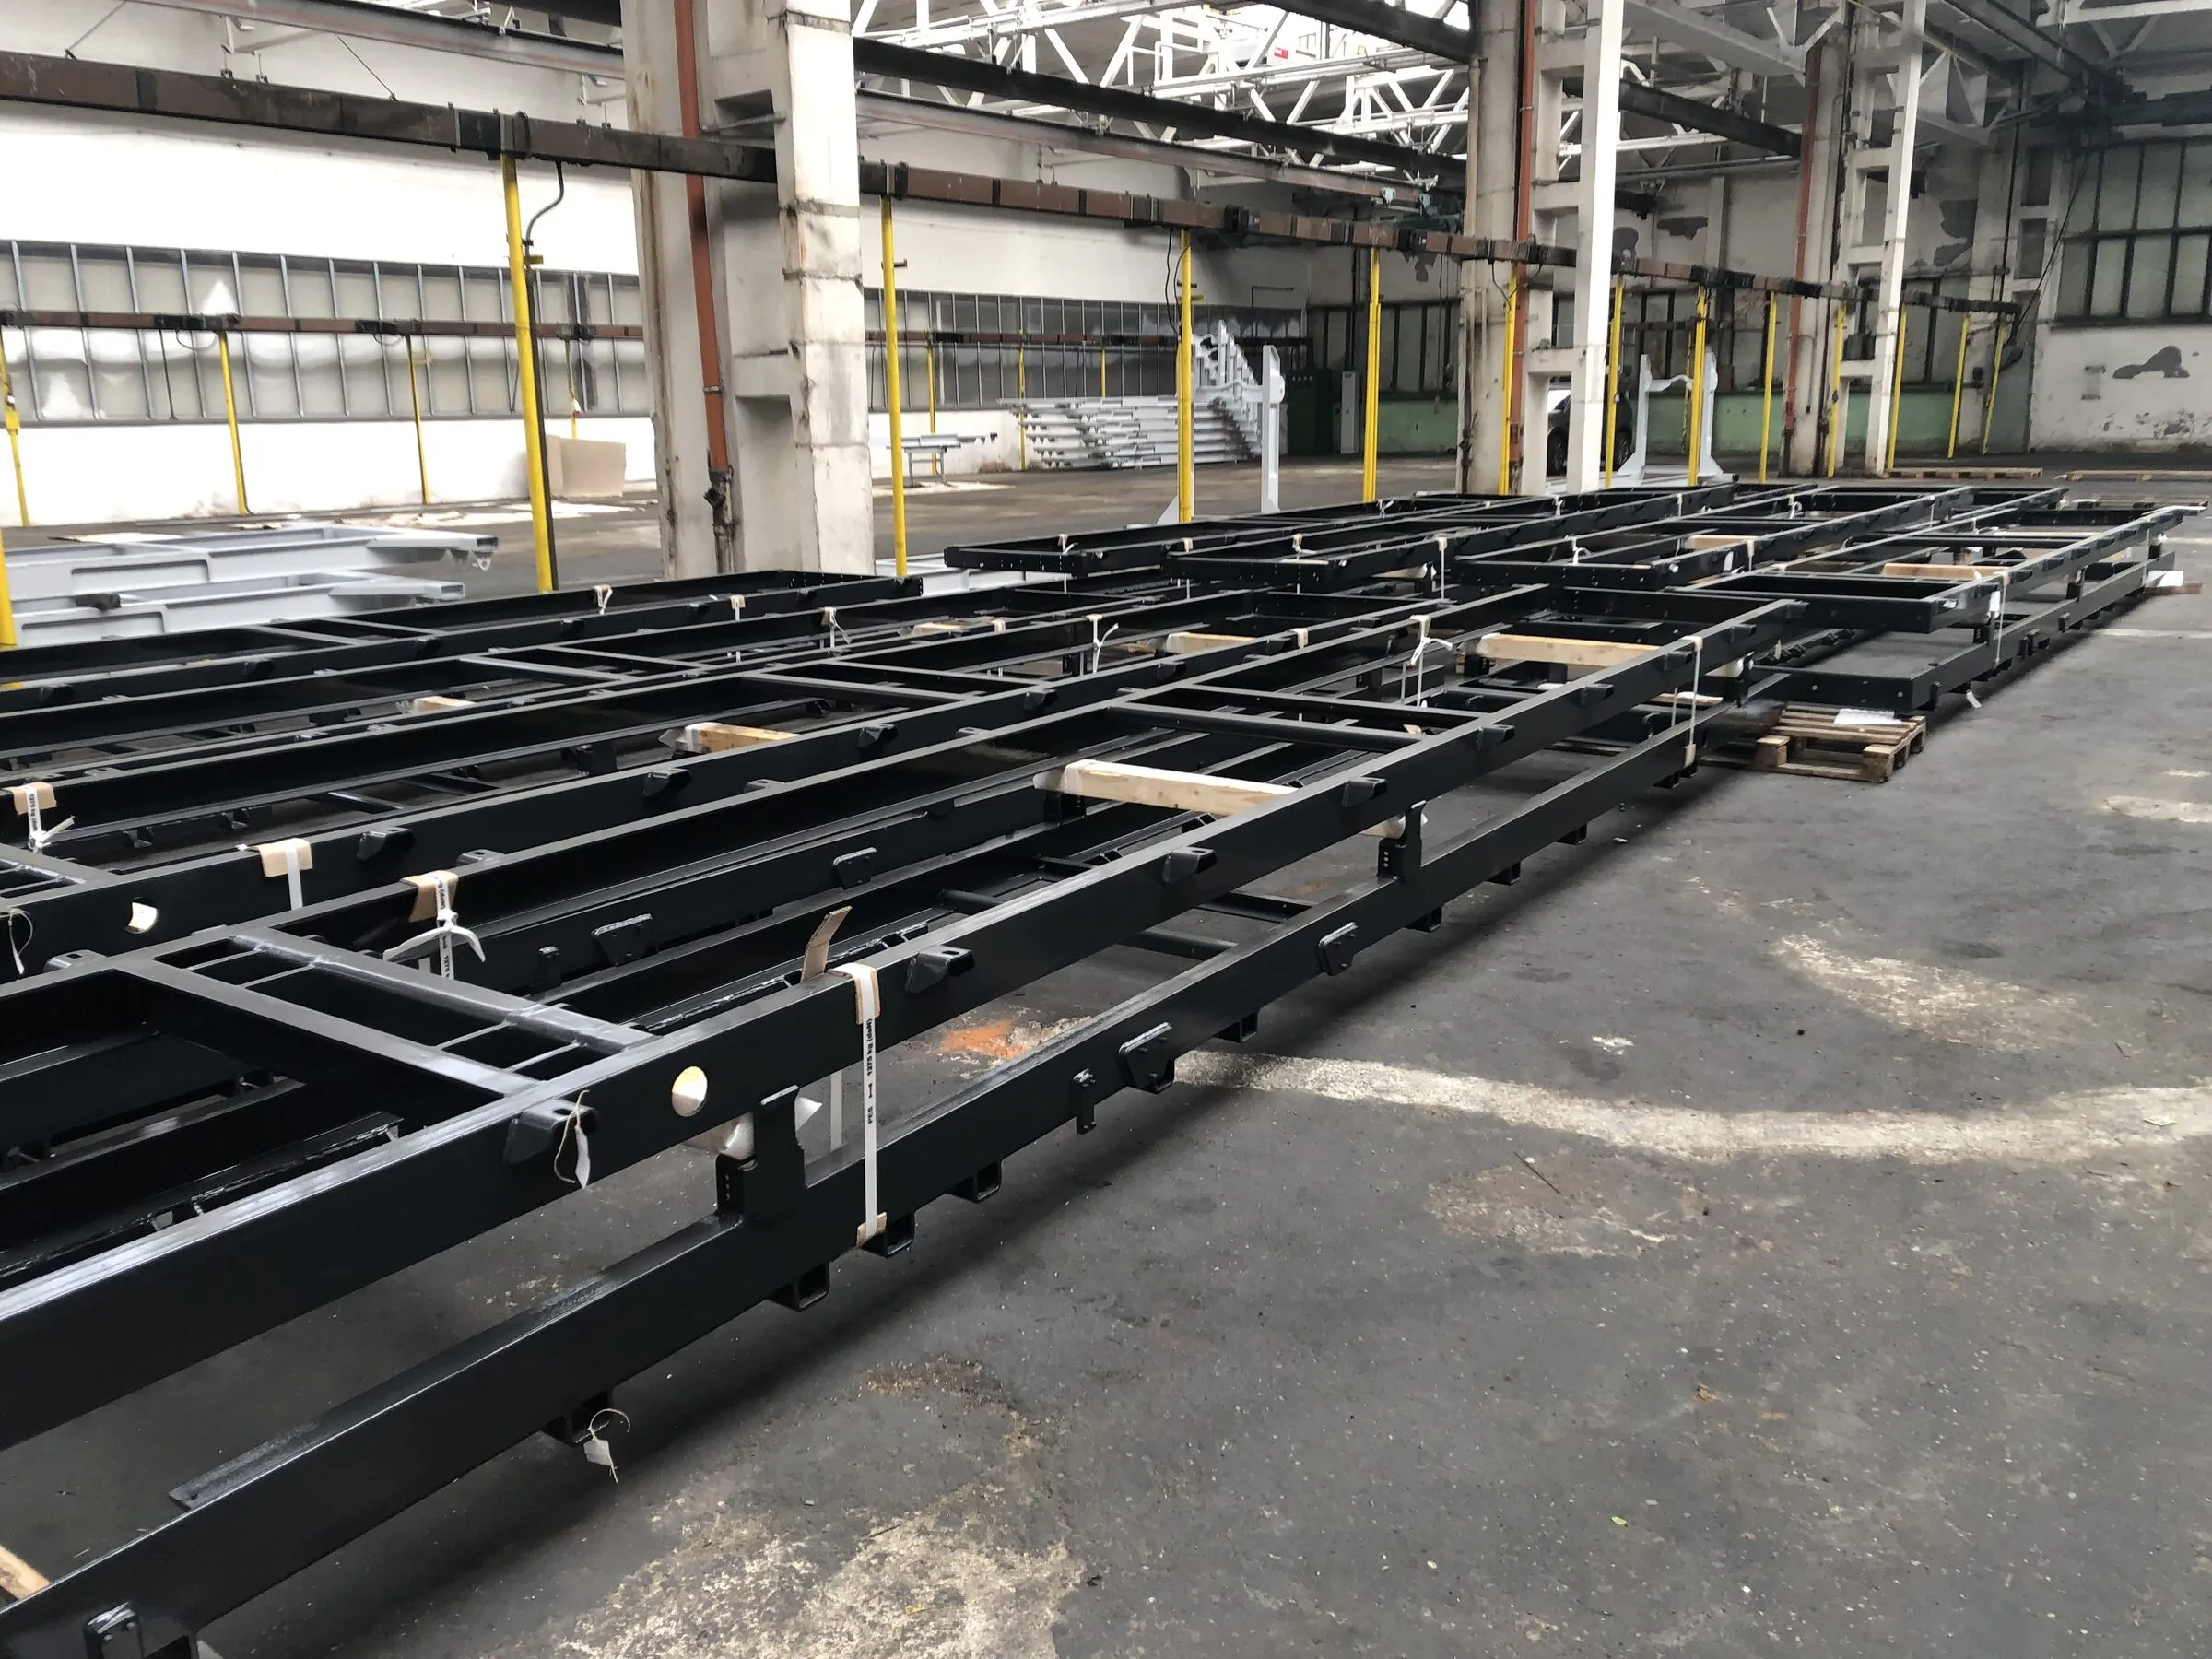
Black welded loader chassis frames on the hall floor 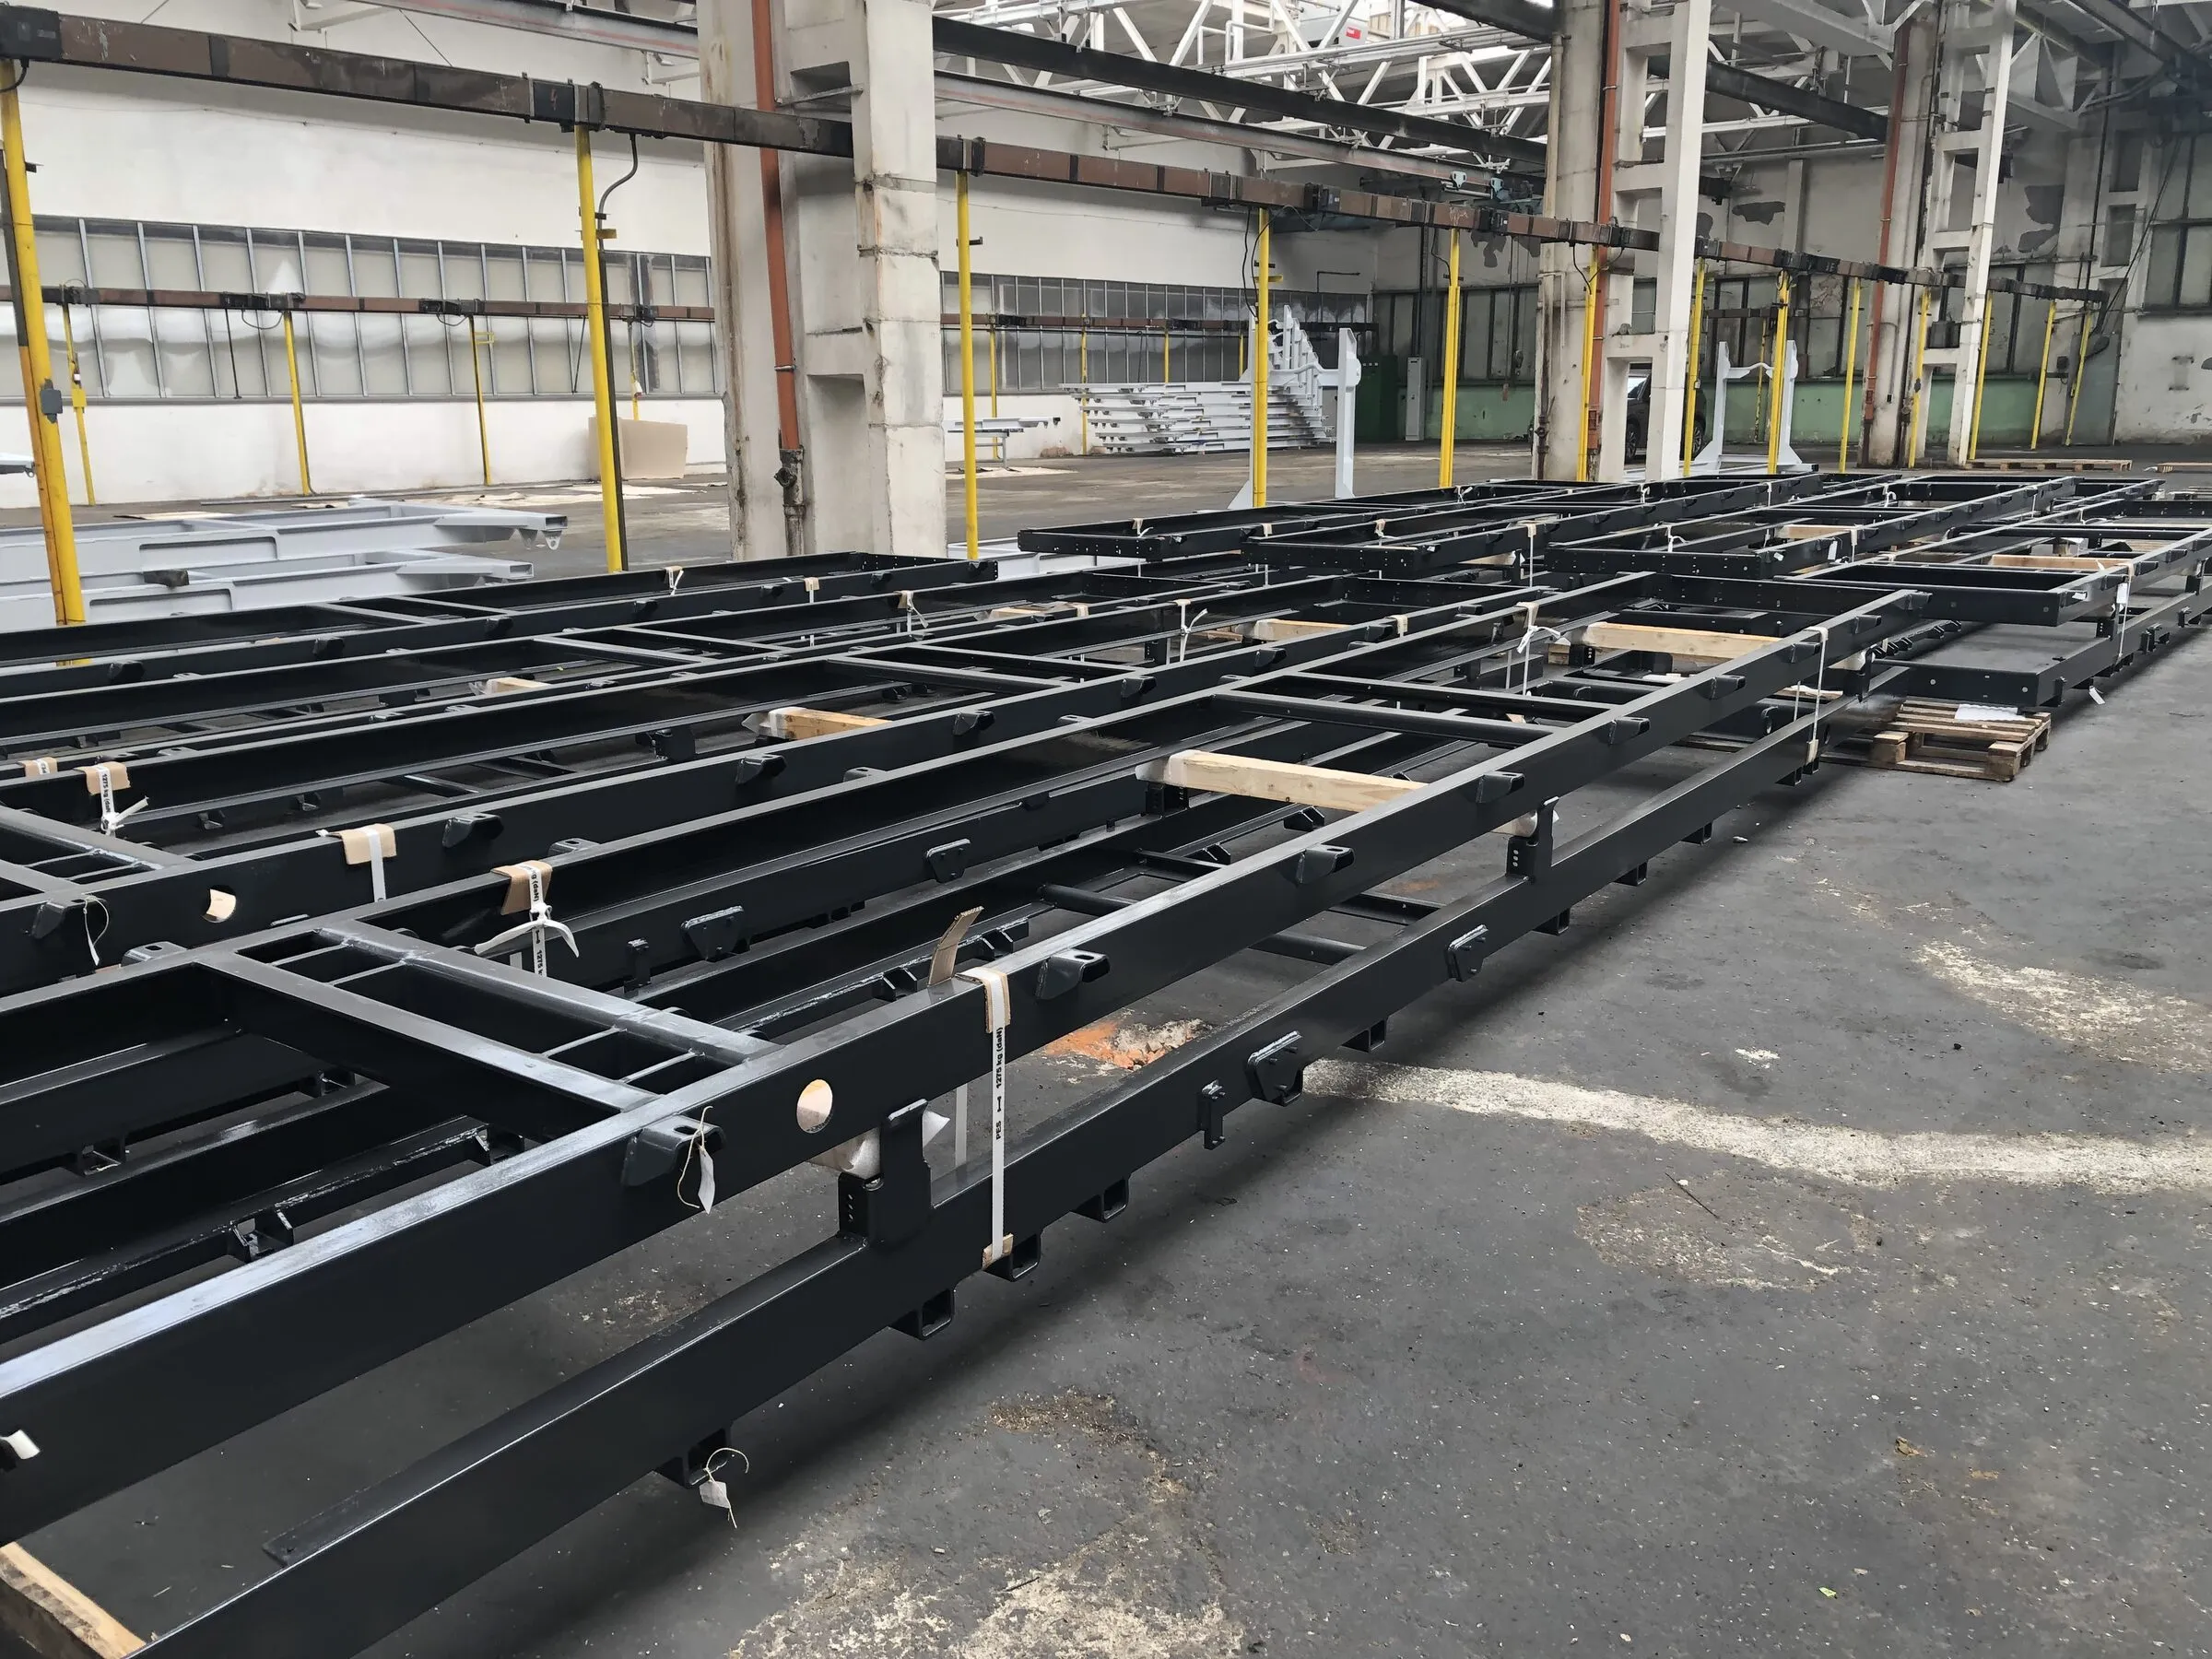
Loader chassis, second angle 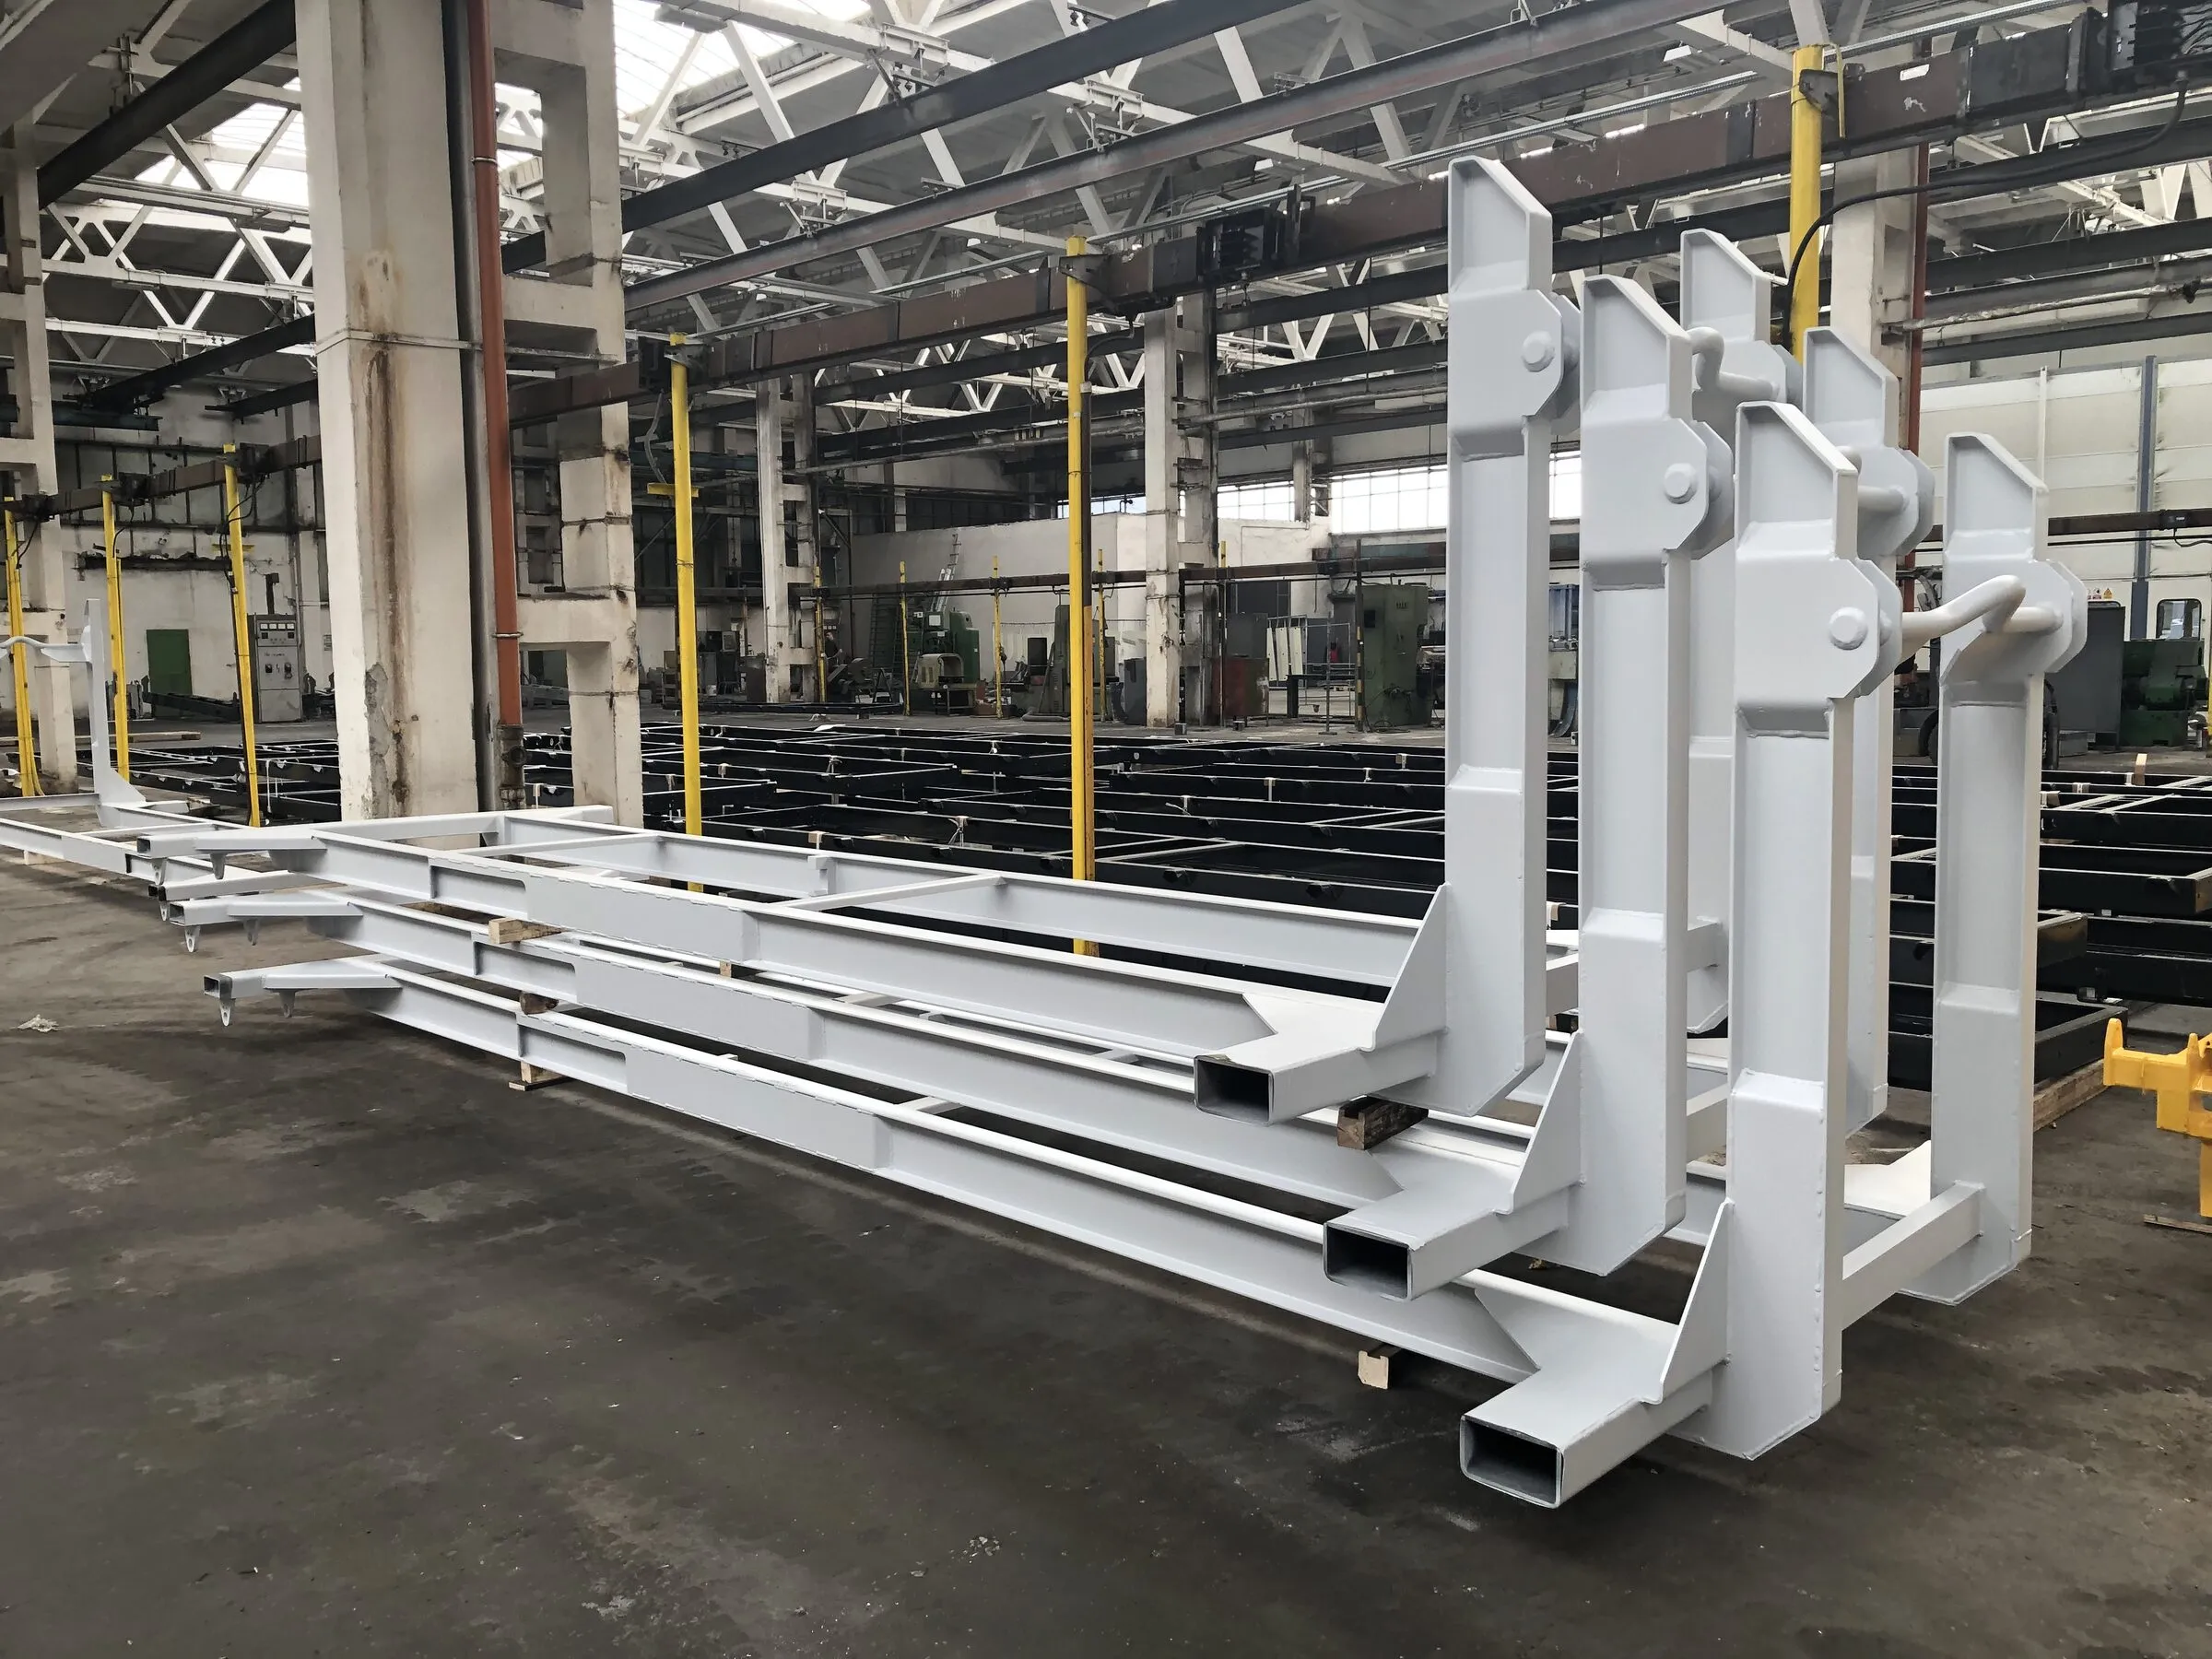
White painted chassis frames with upright posts 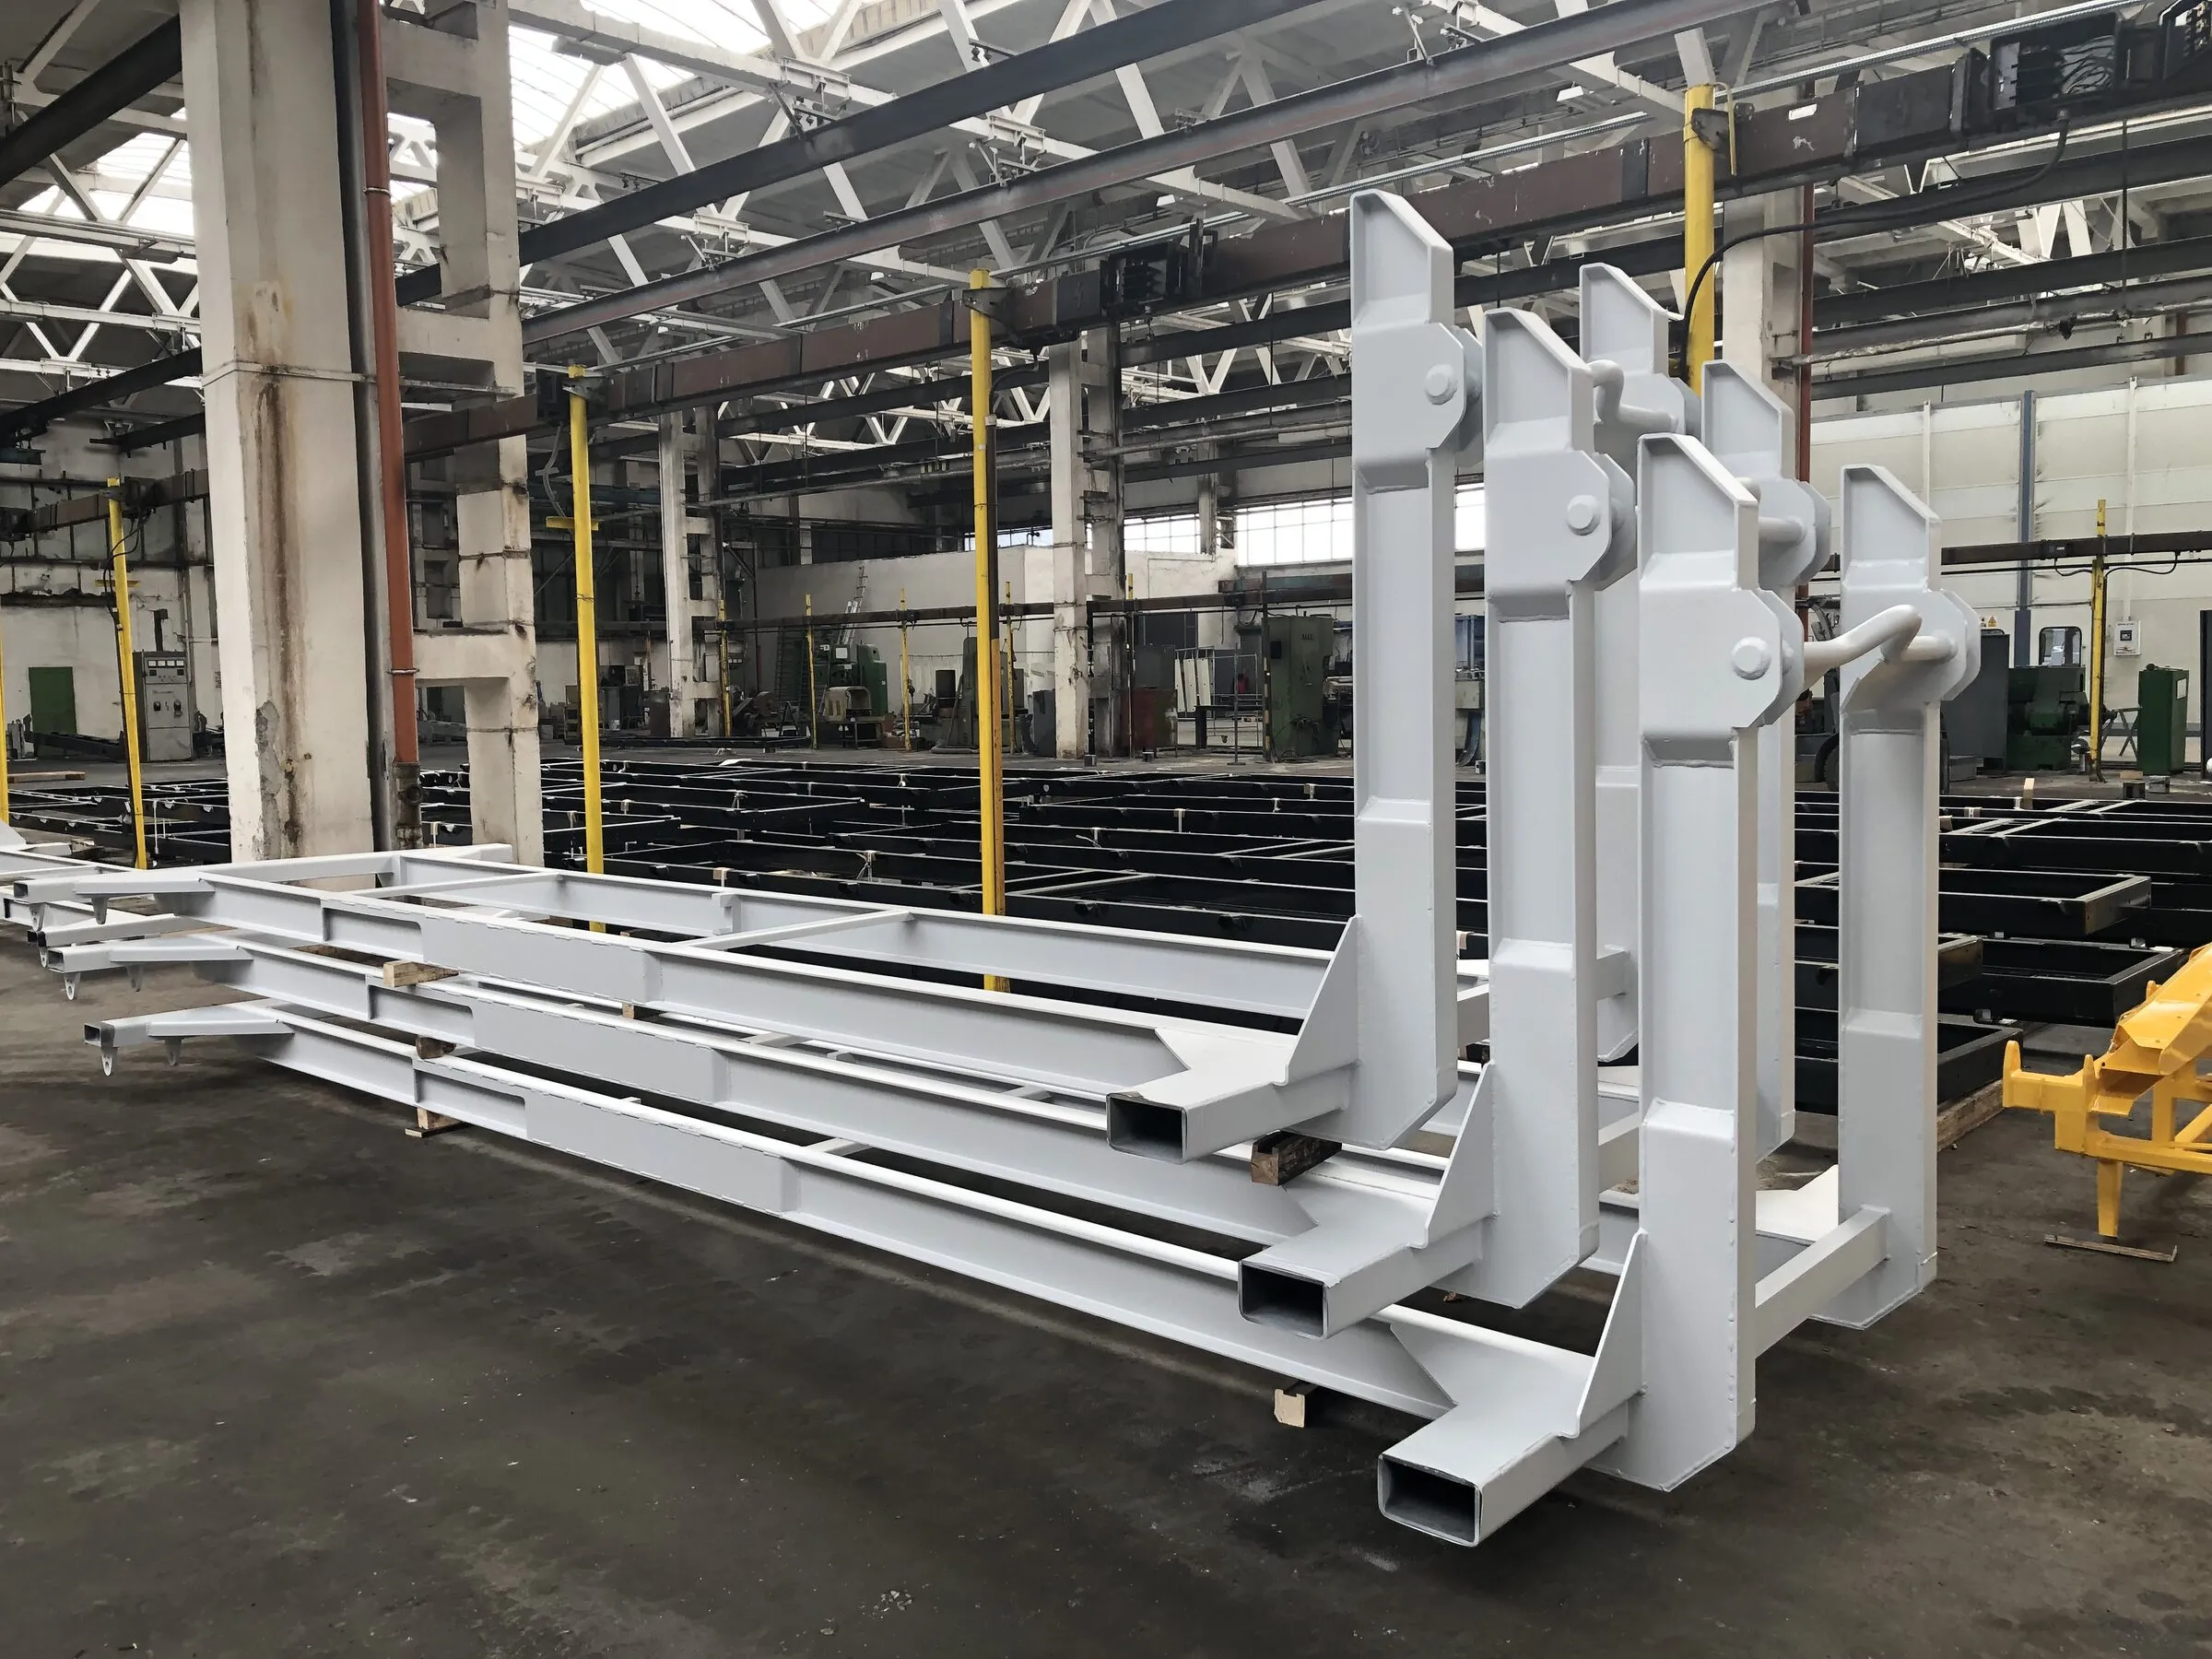
White chassis frames, end view 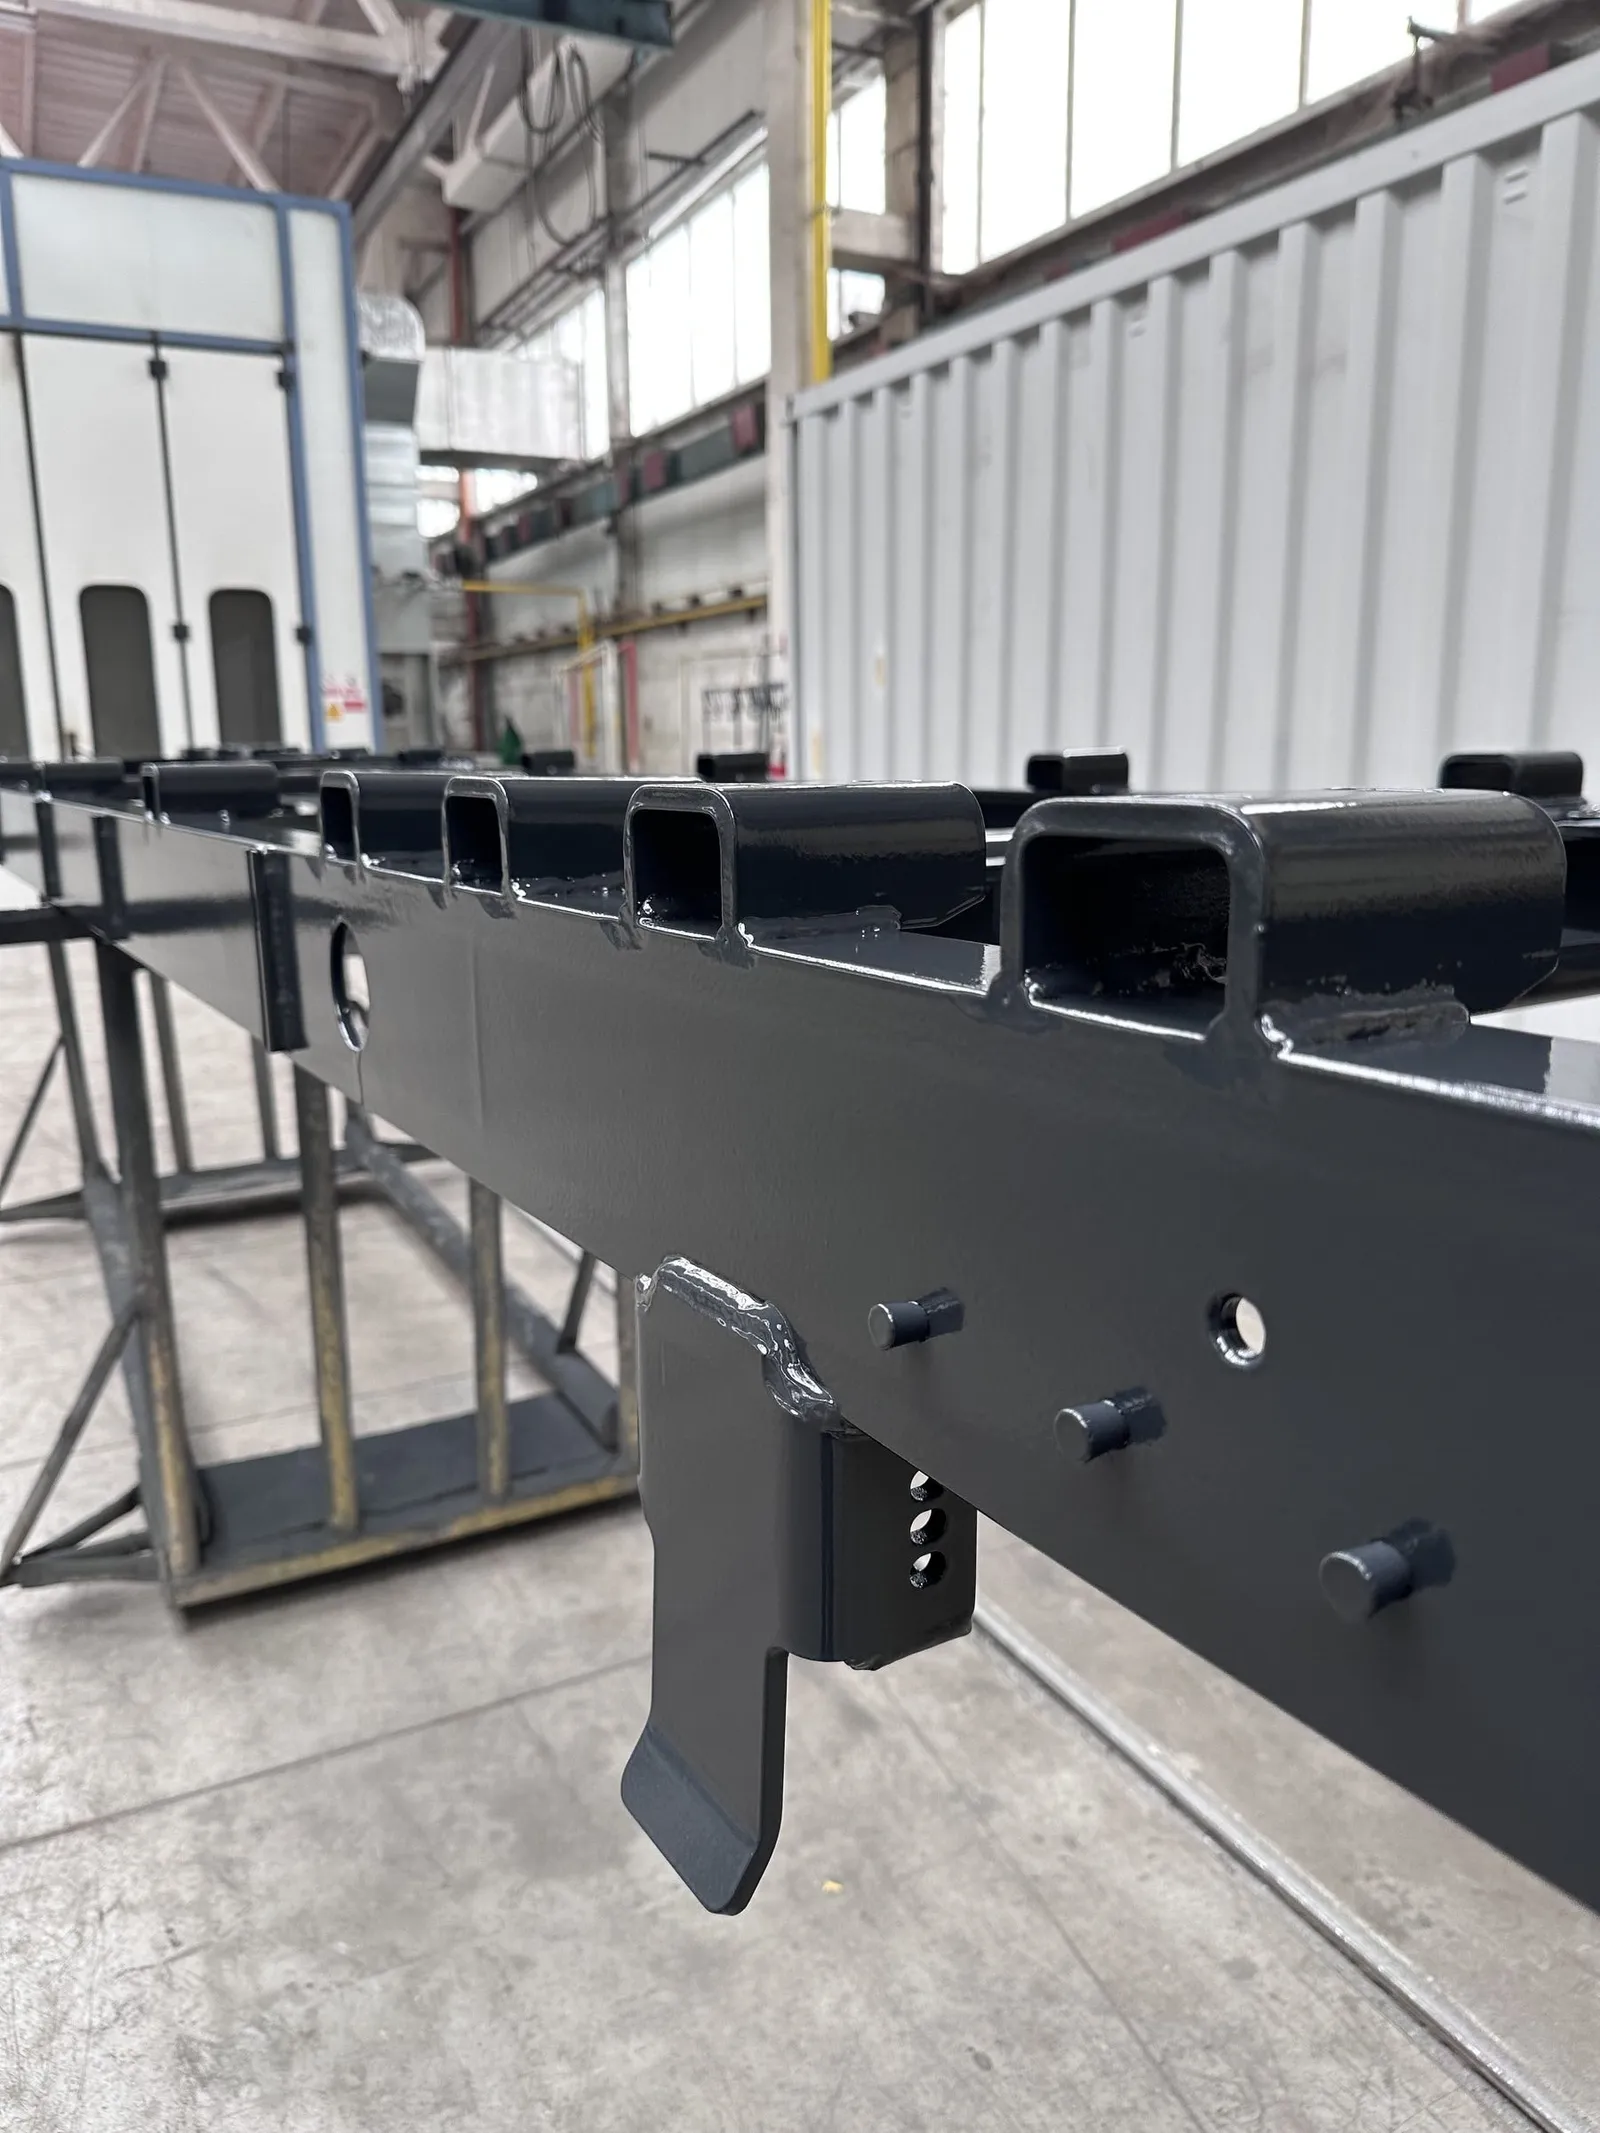
Chassis frame bracket detail 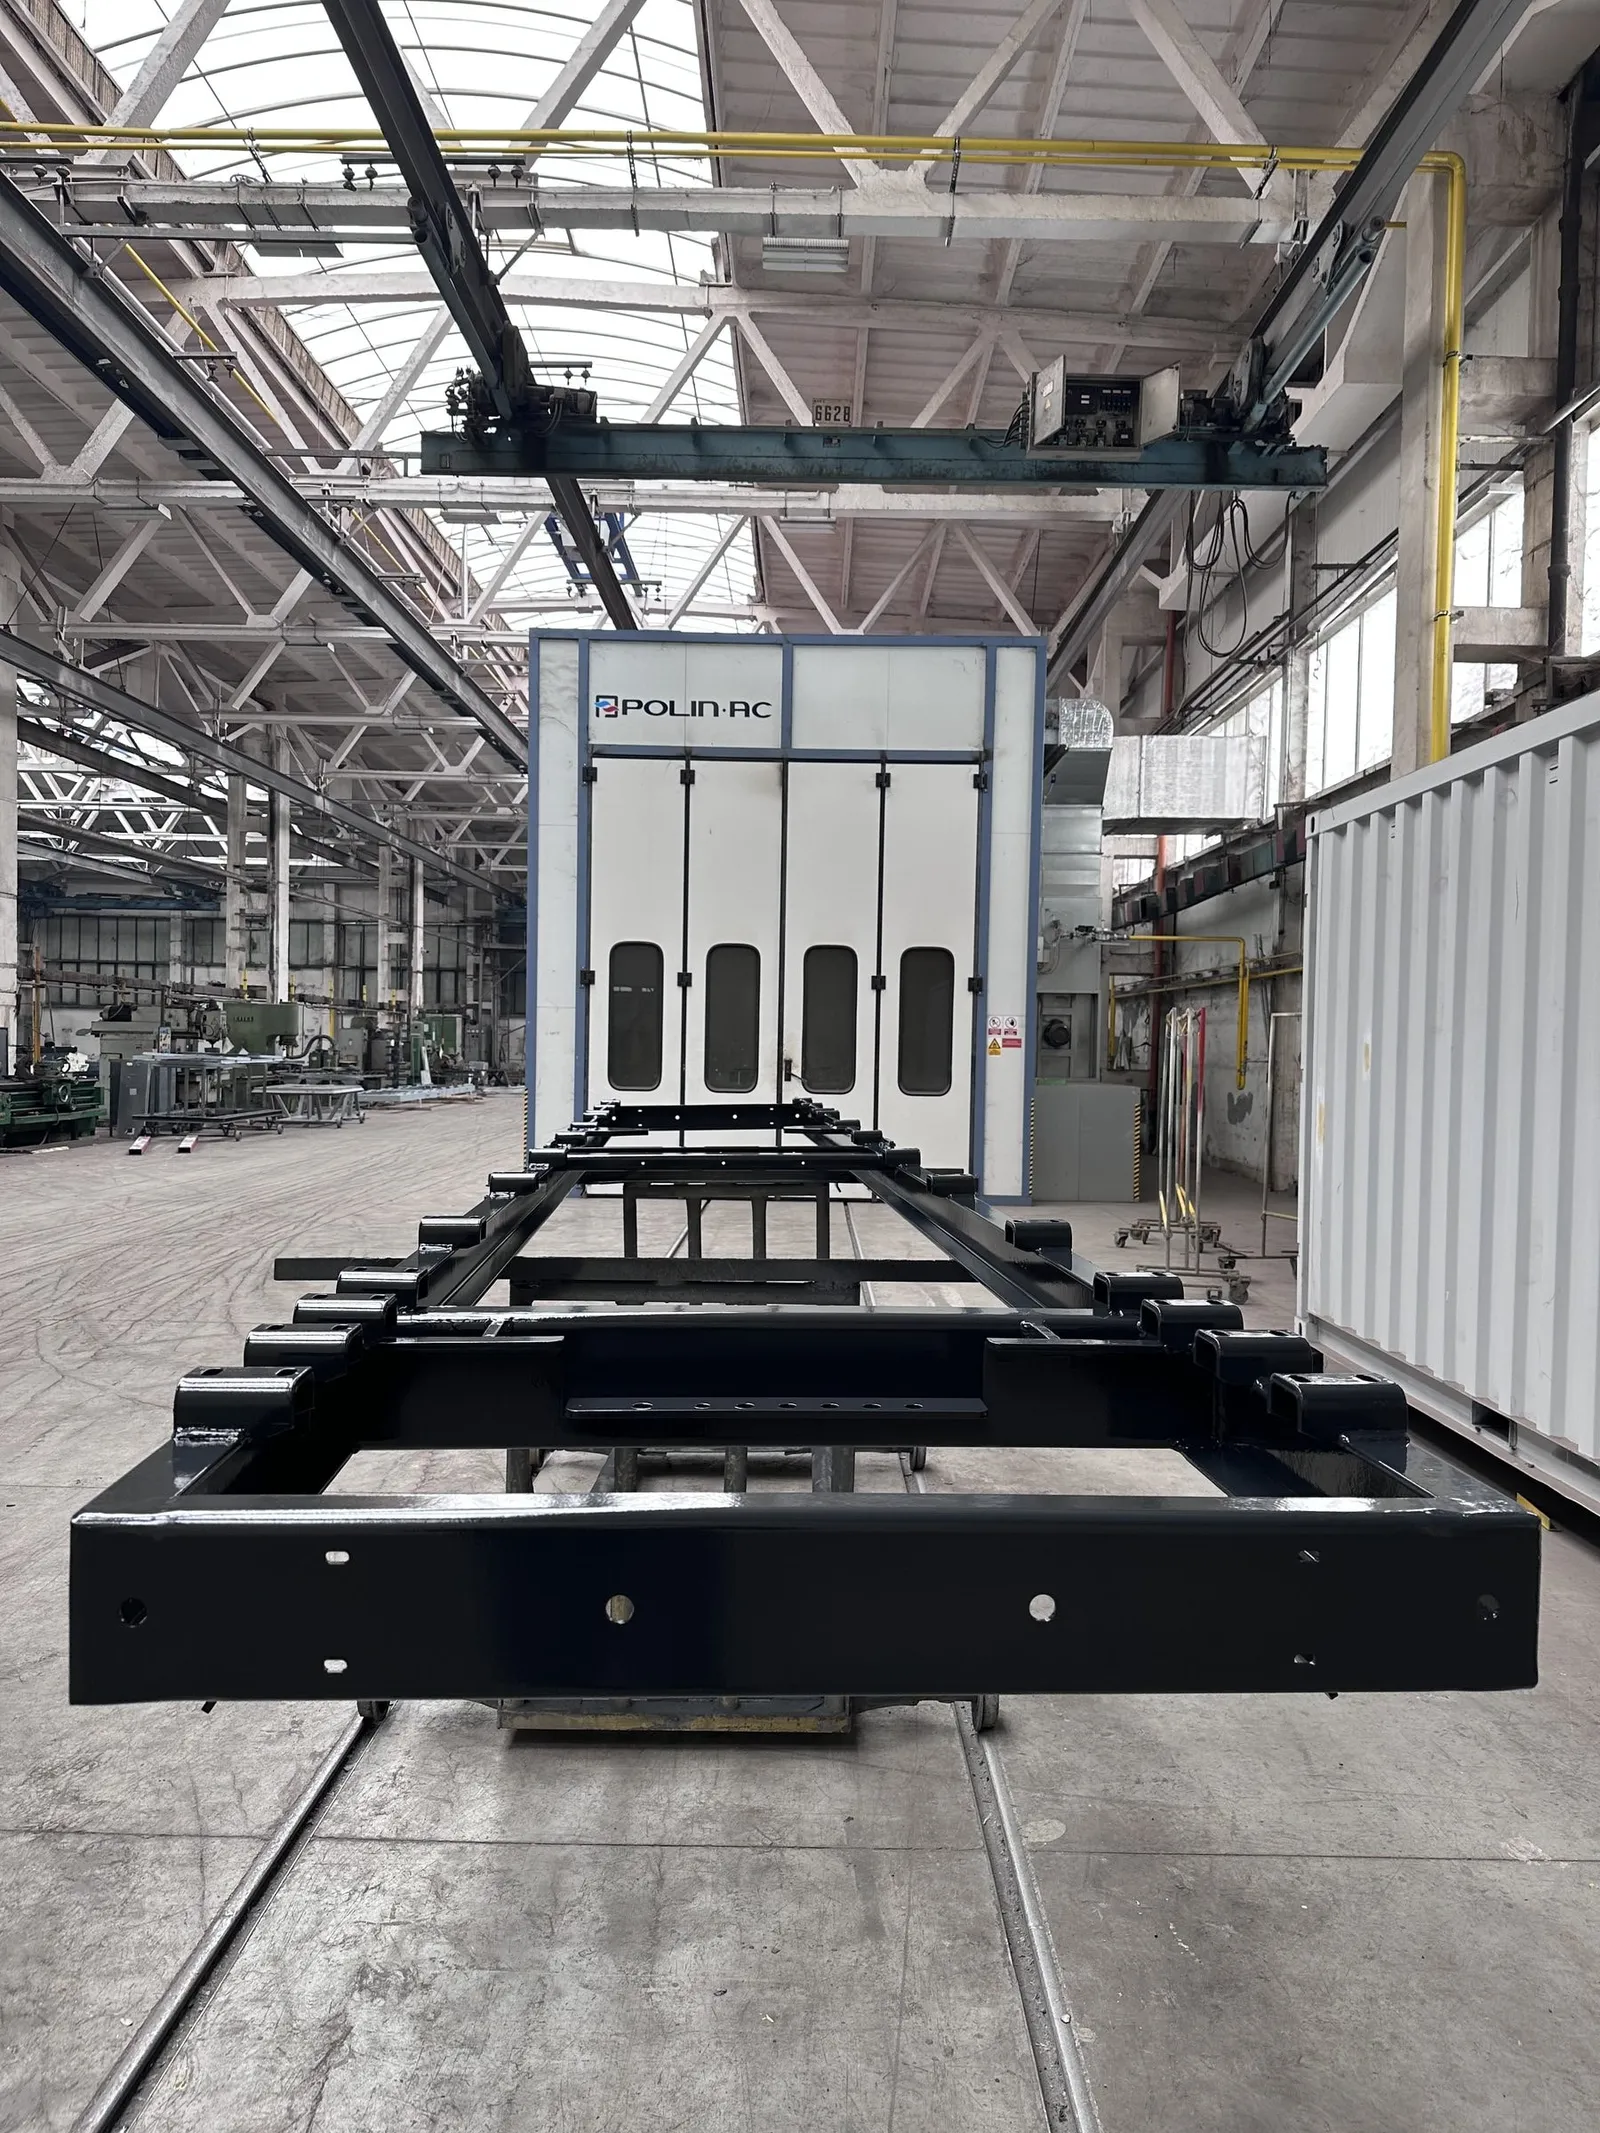
Chassis frame on stands in the hall 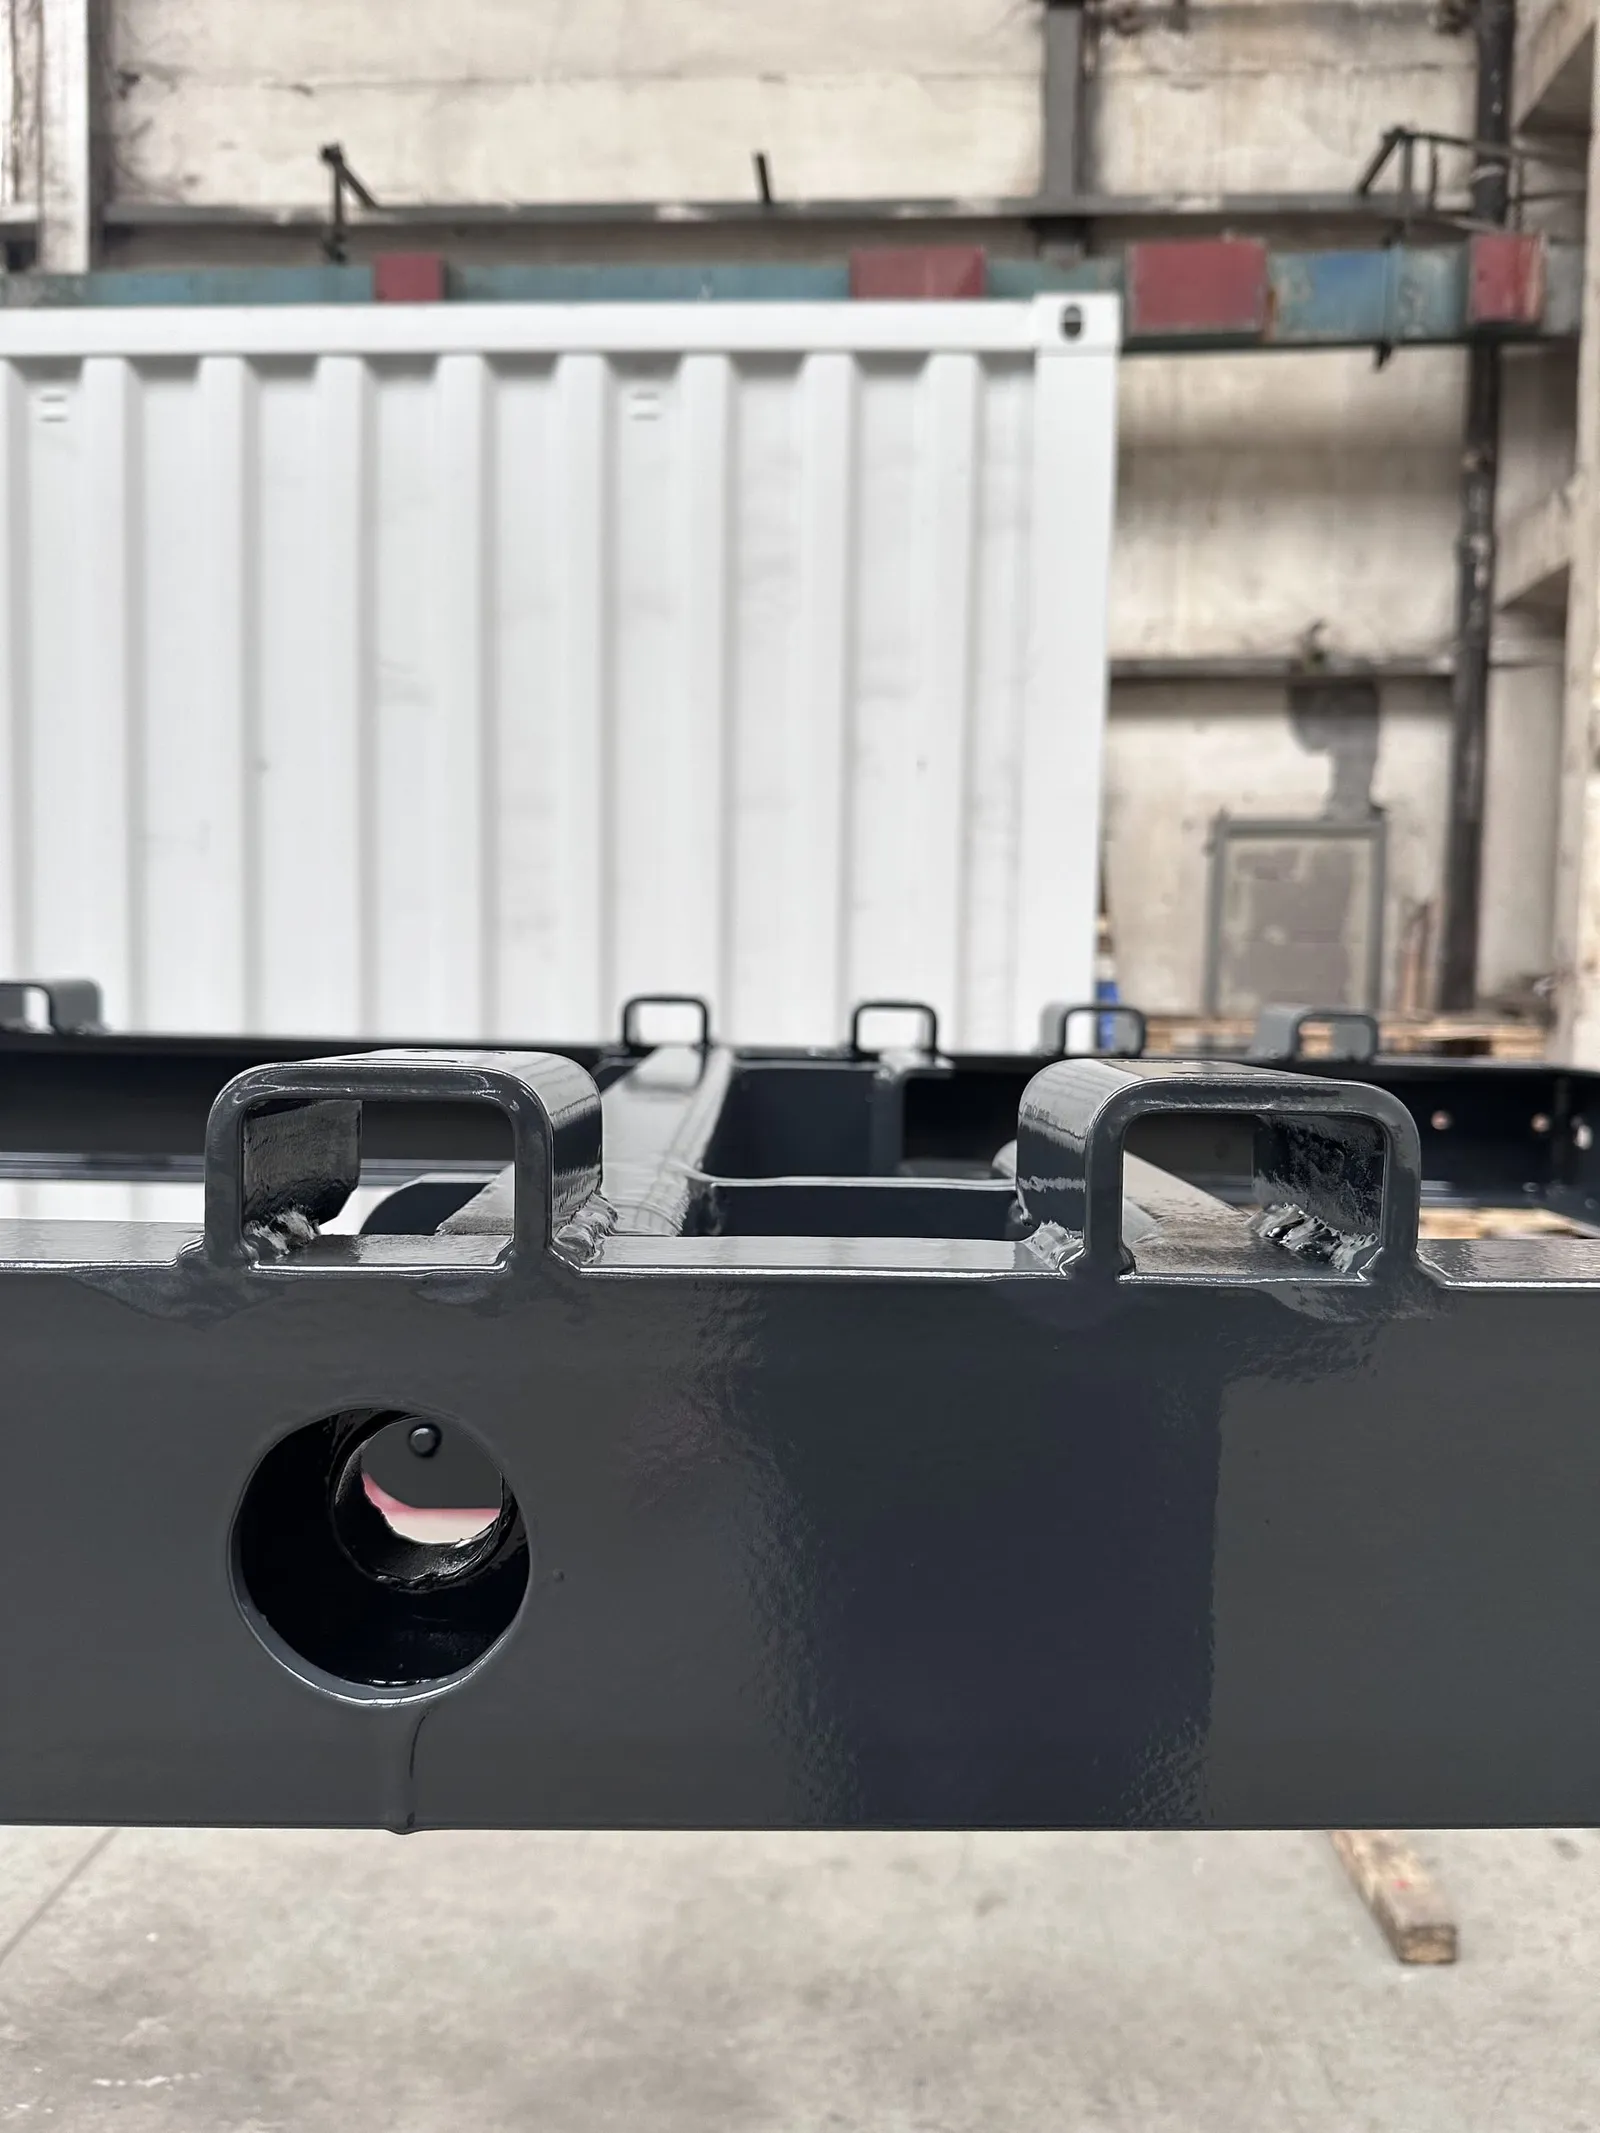
Chassis frame end detail, a white container behind
Racking systems
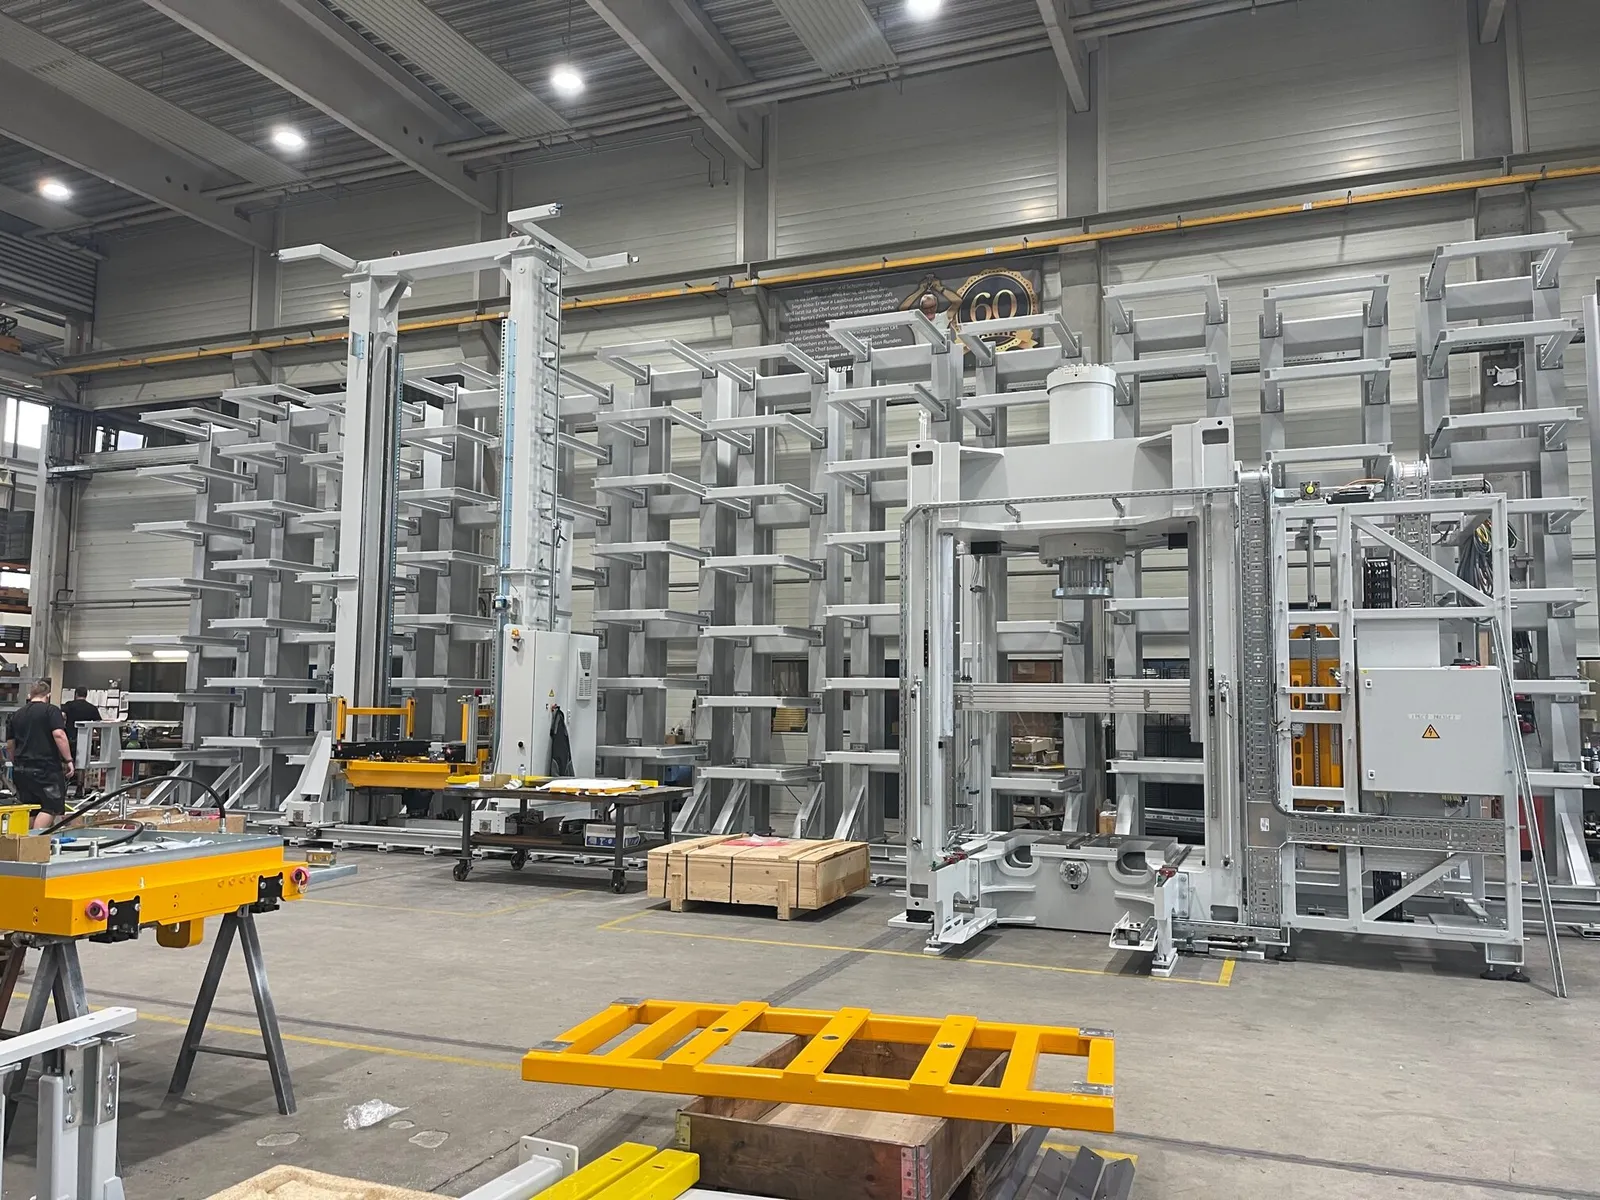
Tall racking structures assembled in the hall, third view
Agricultural OEM parts
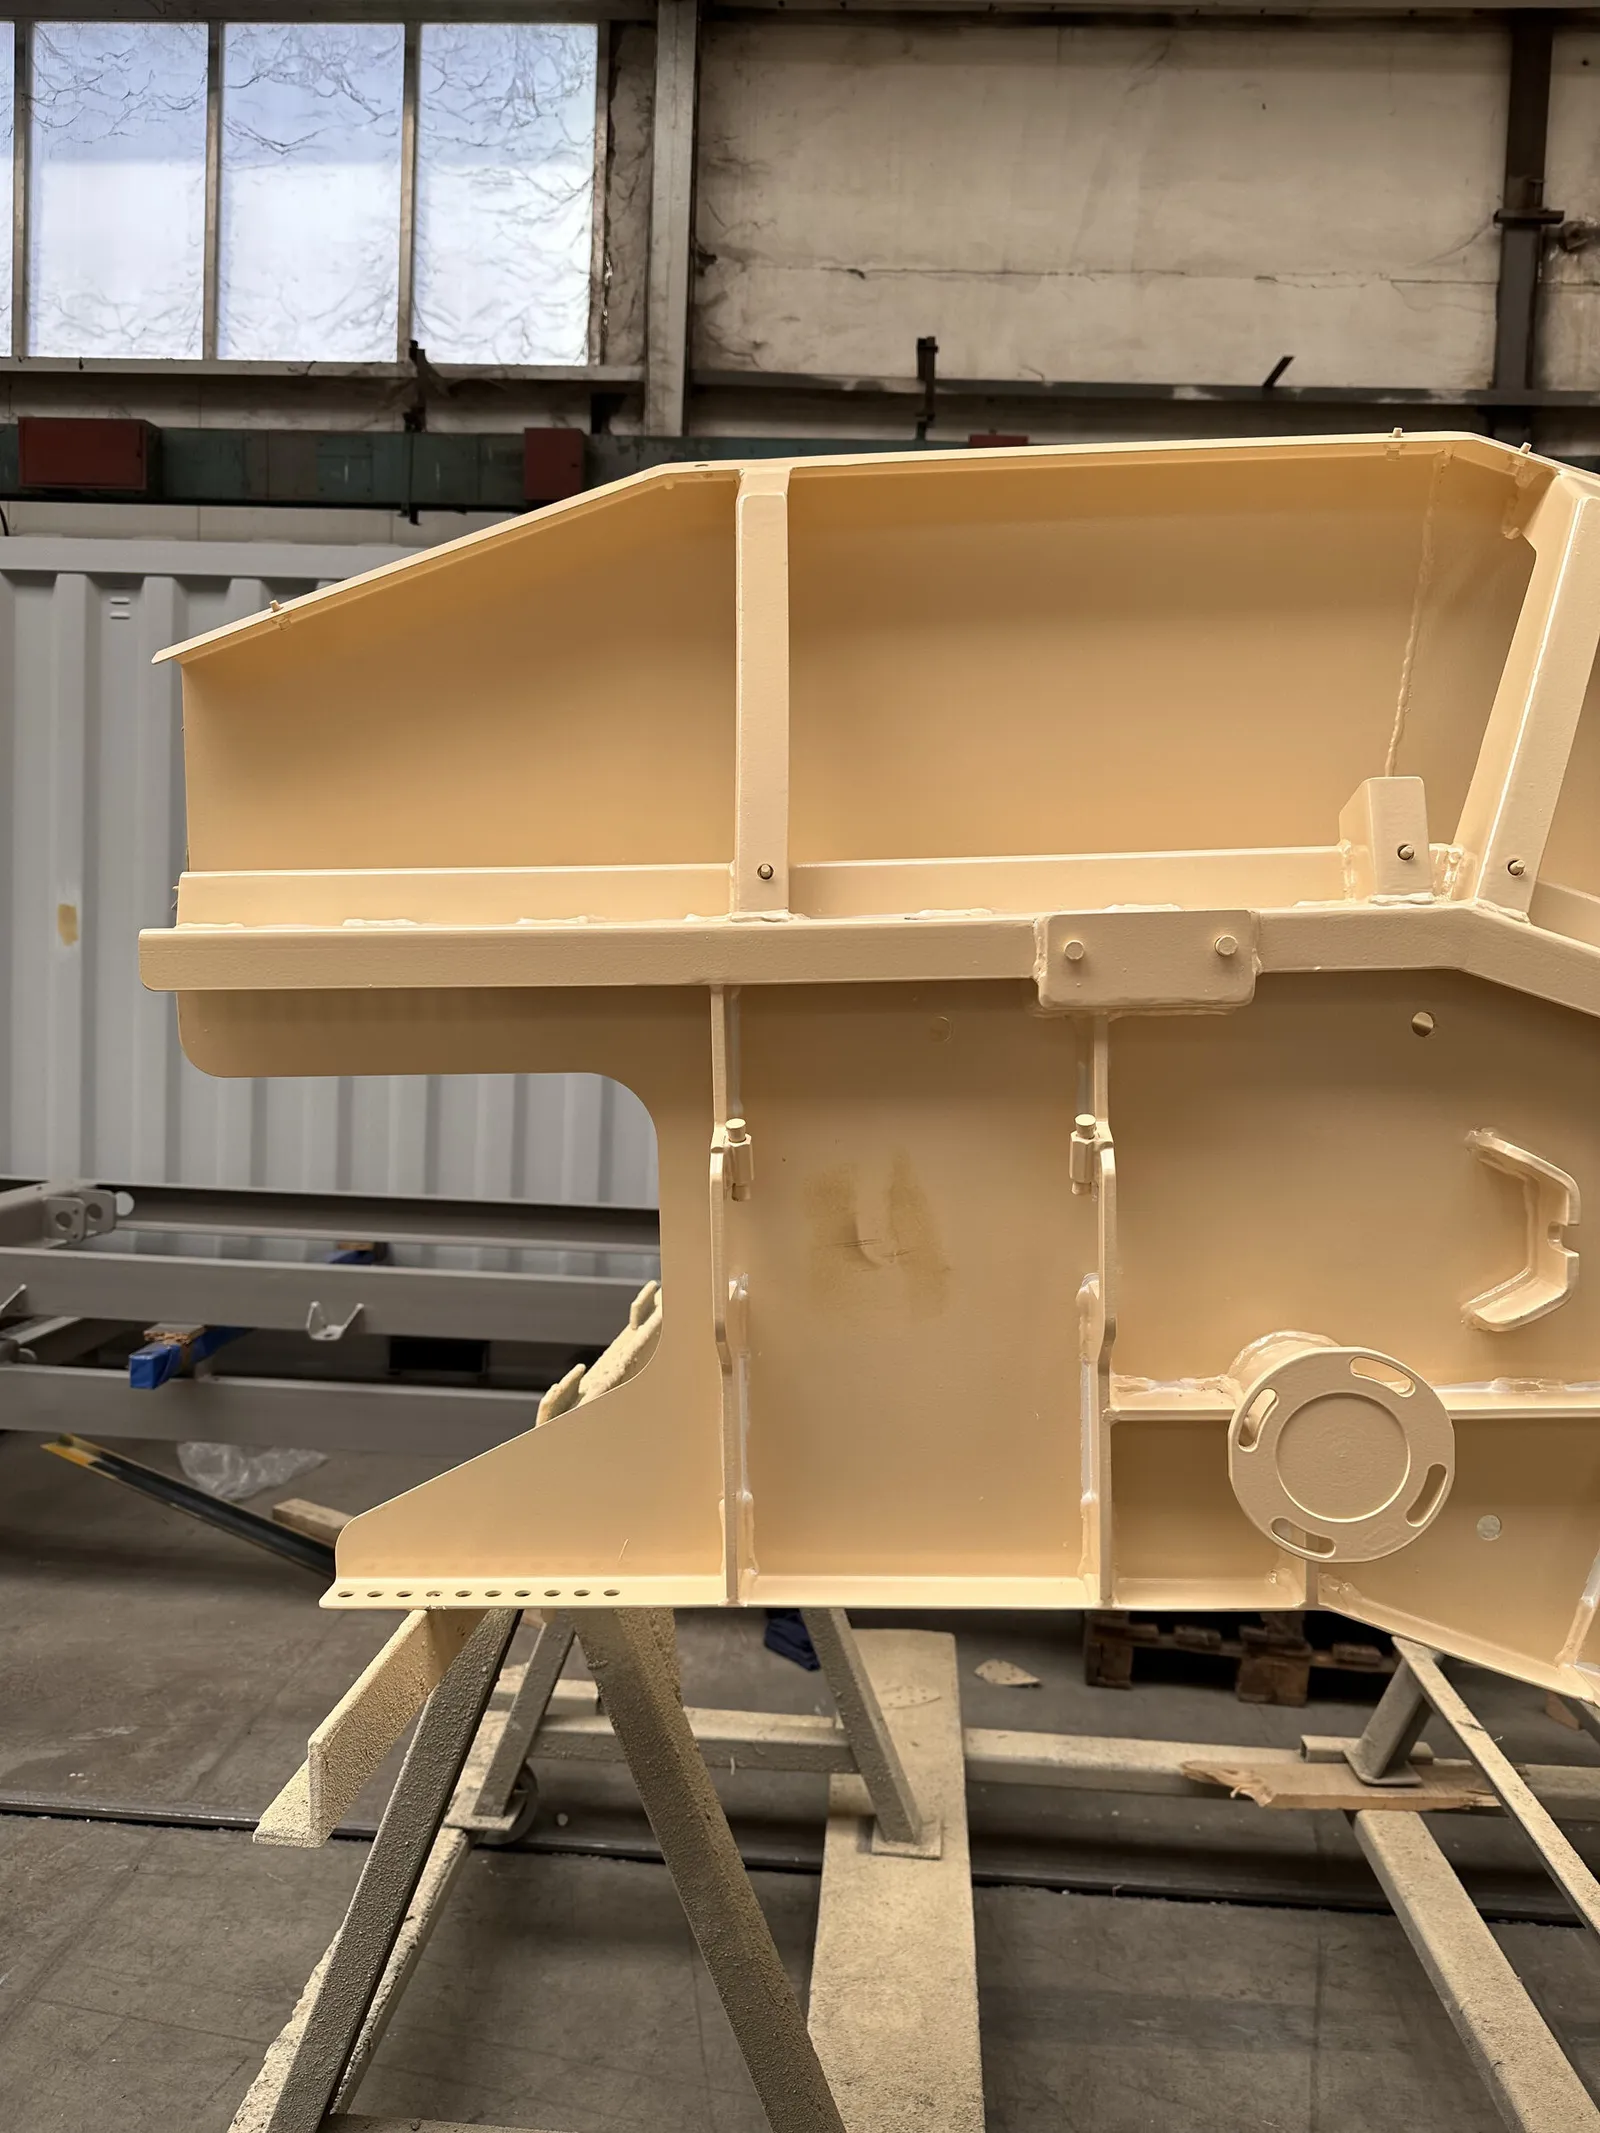
Beige welded hopper section on a stand, second angle 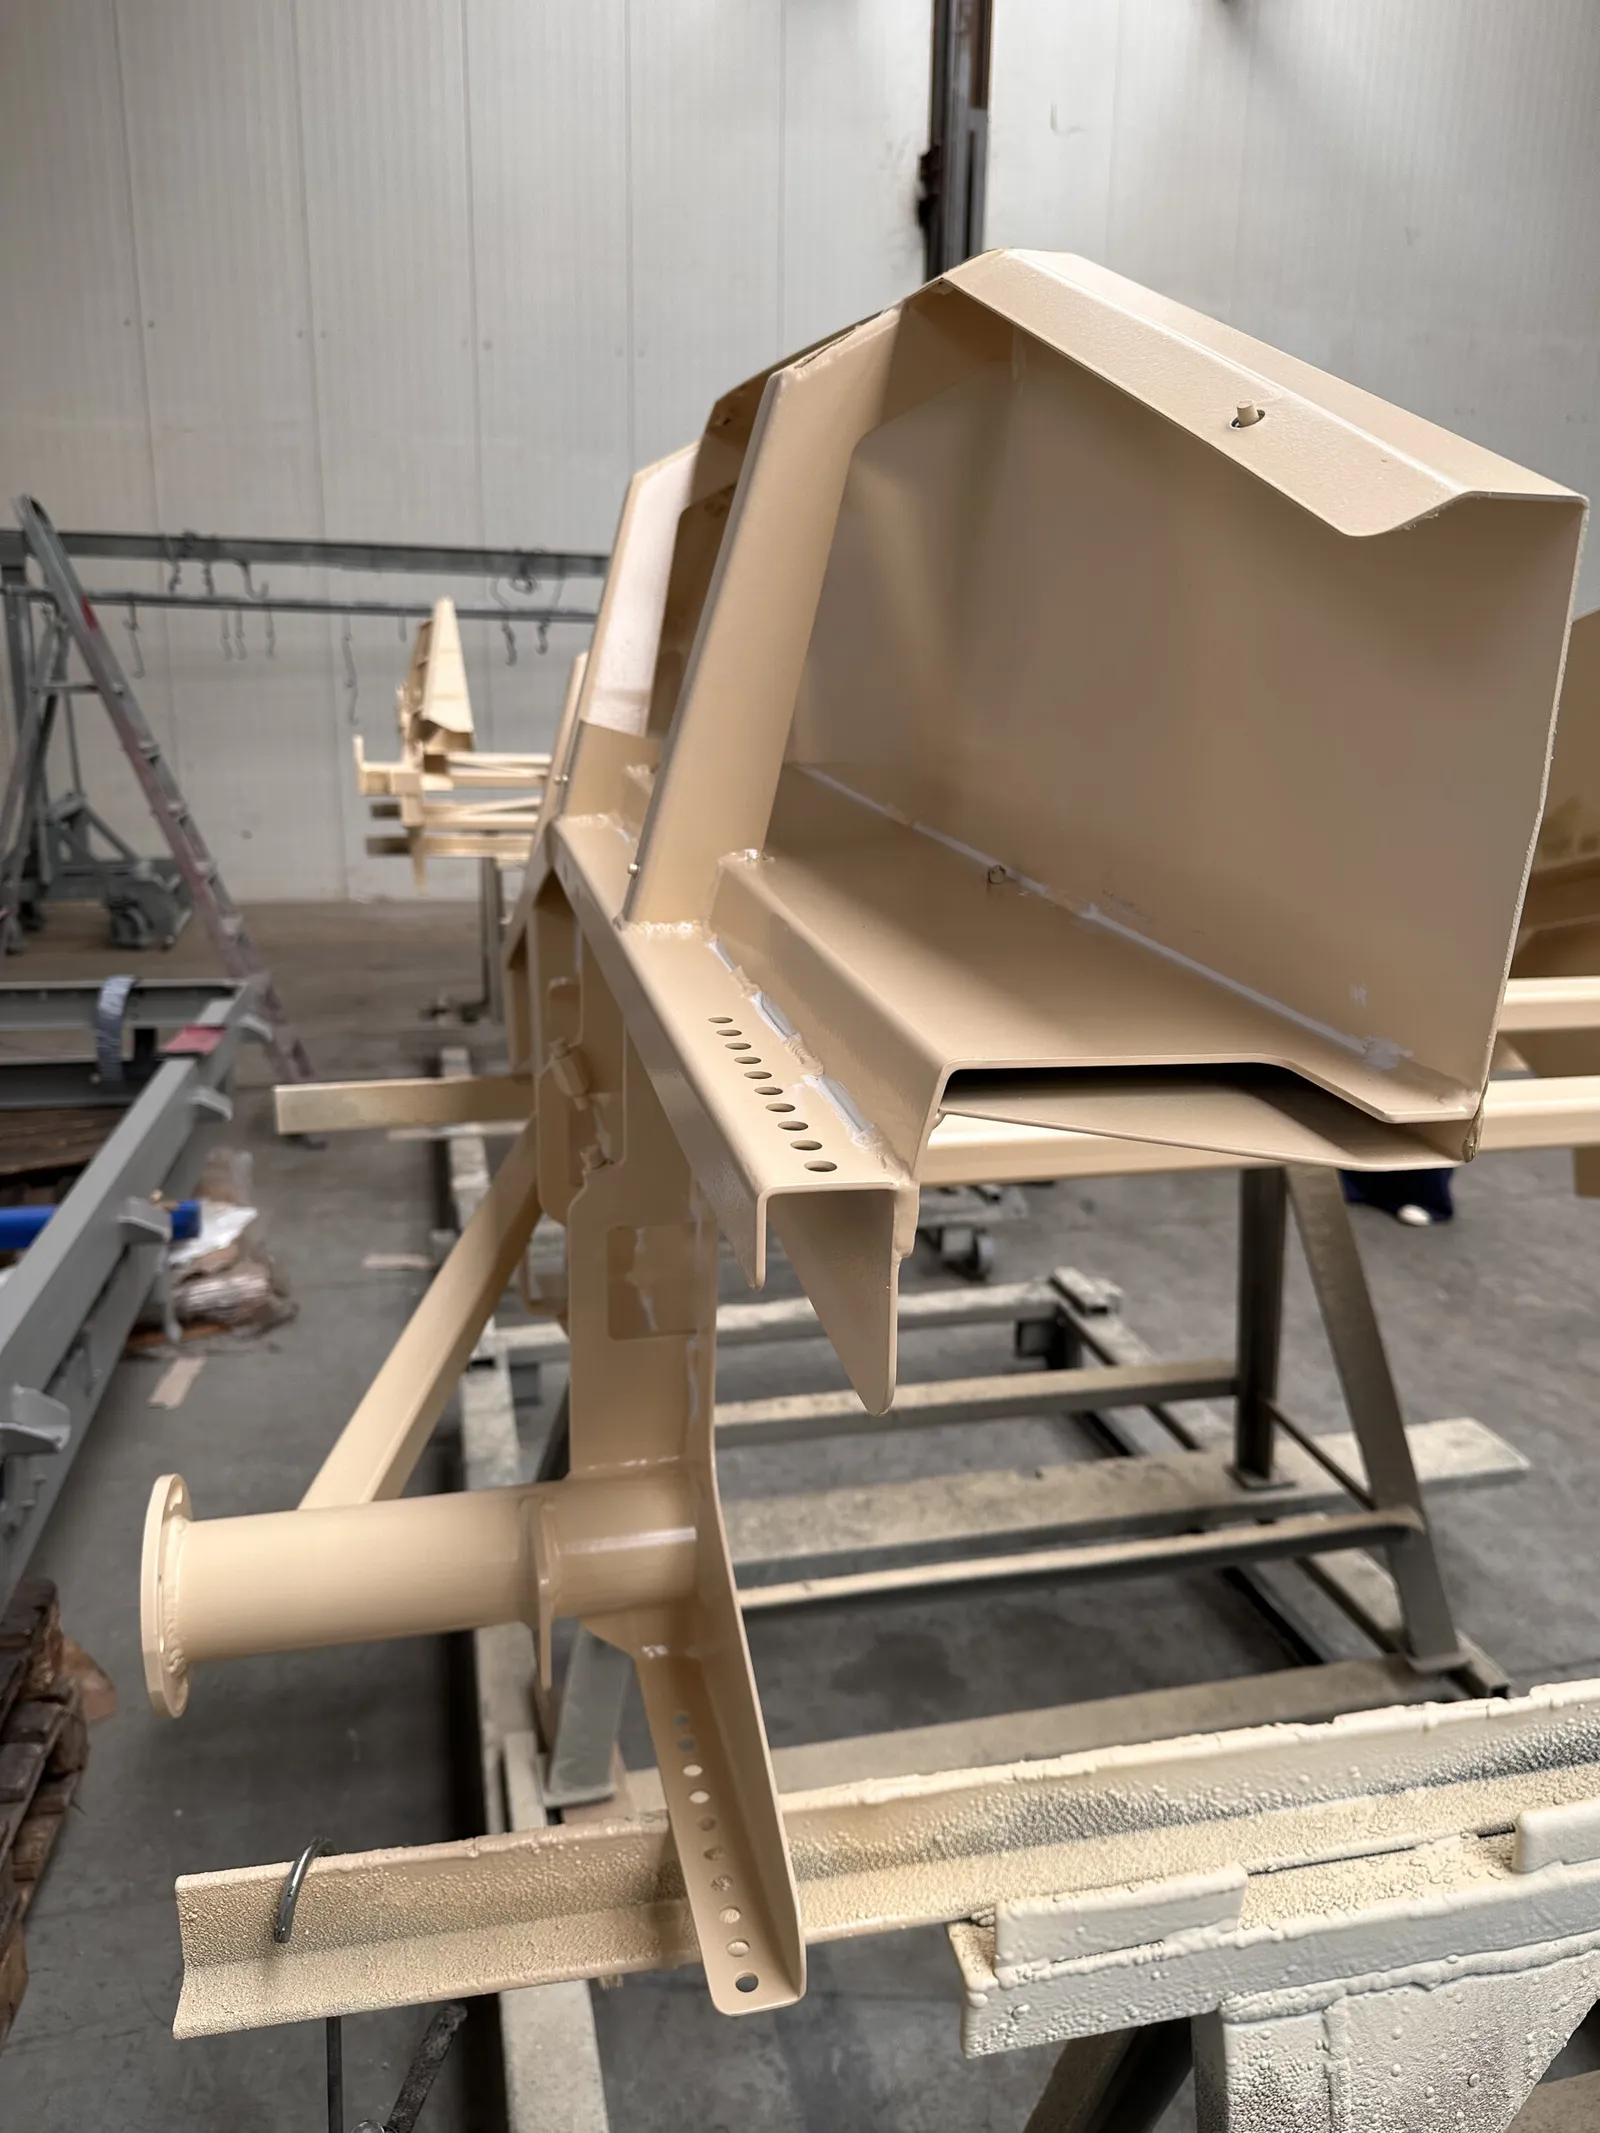
Beige welded part, end view 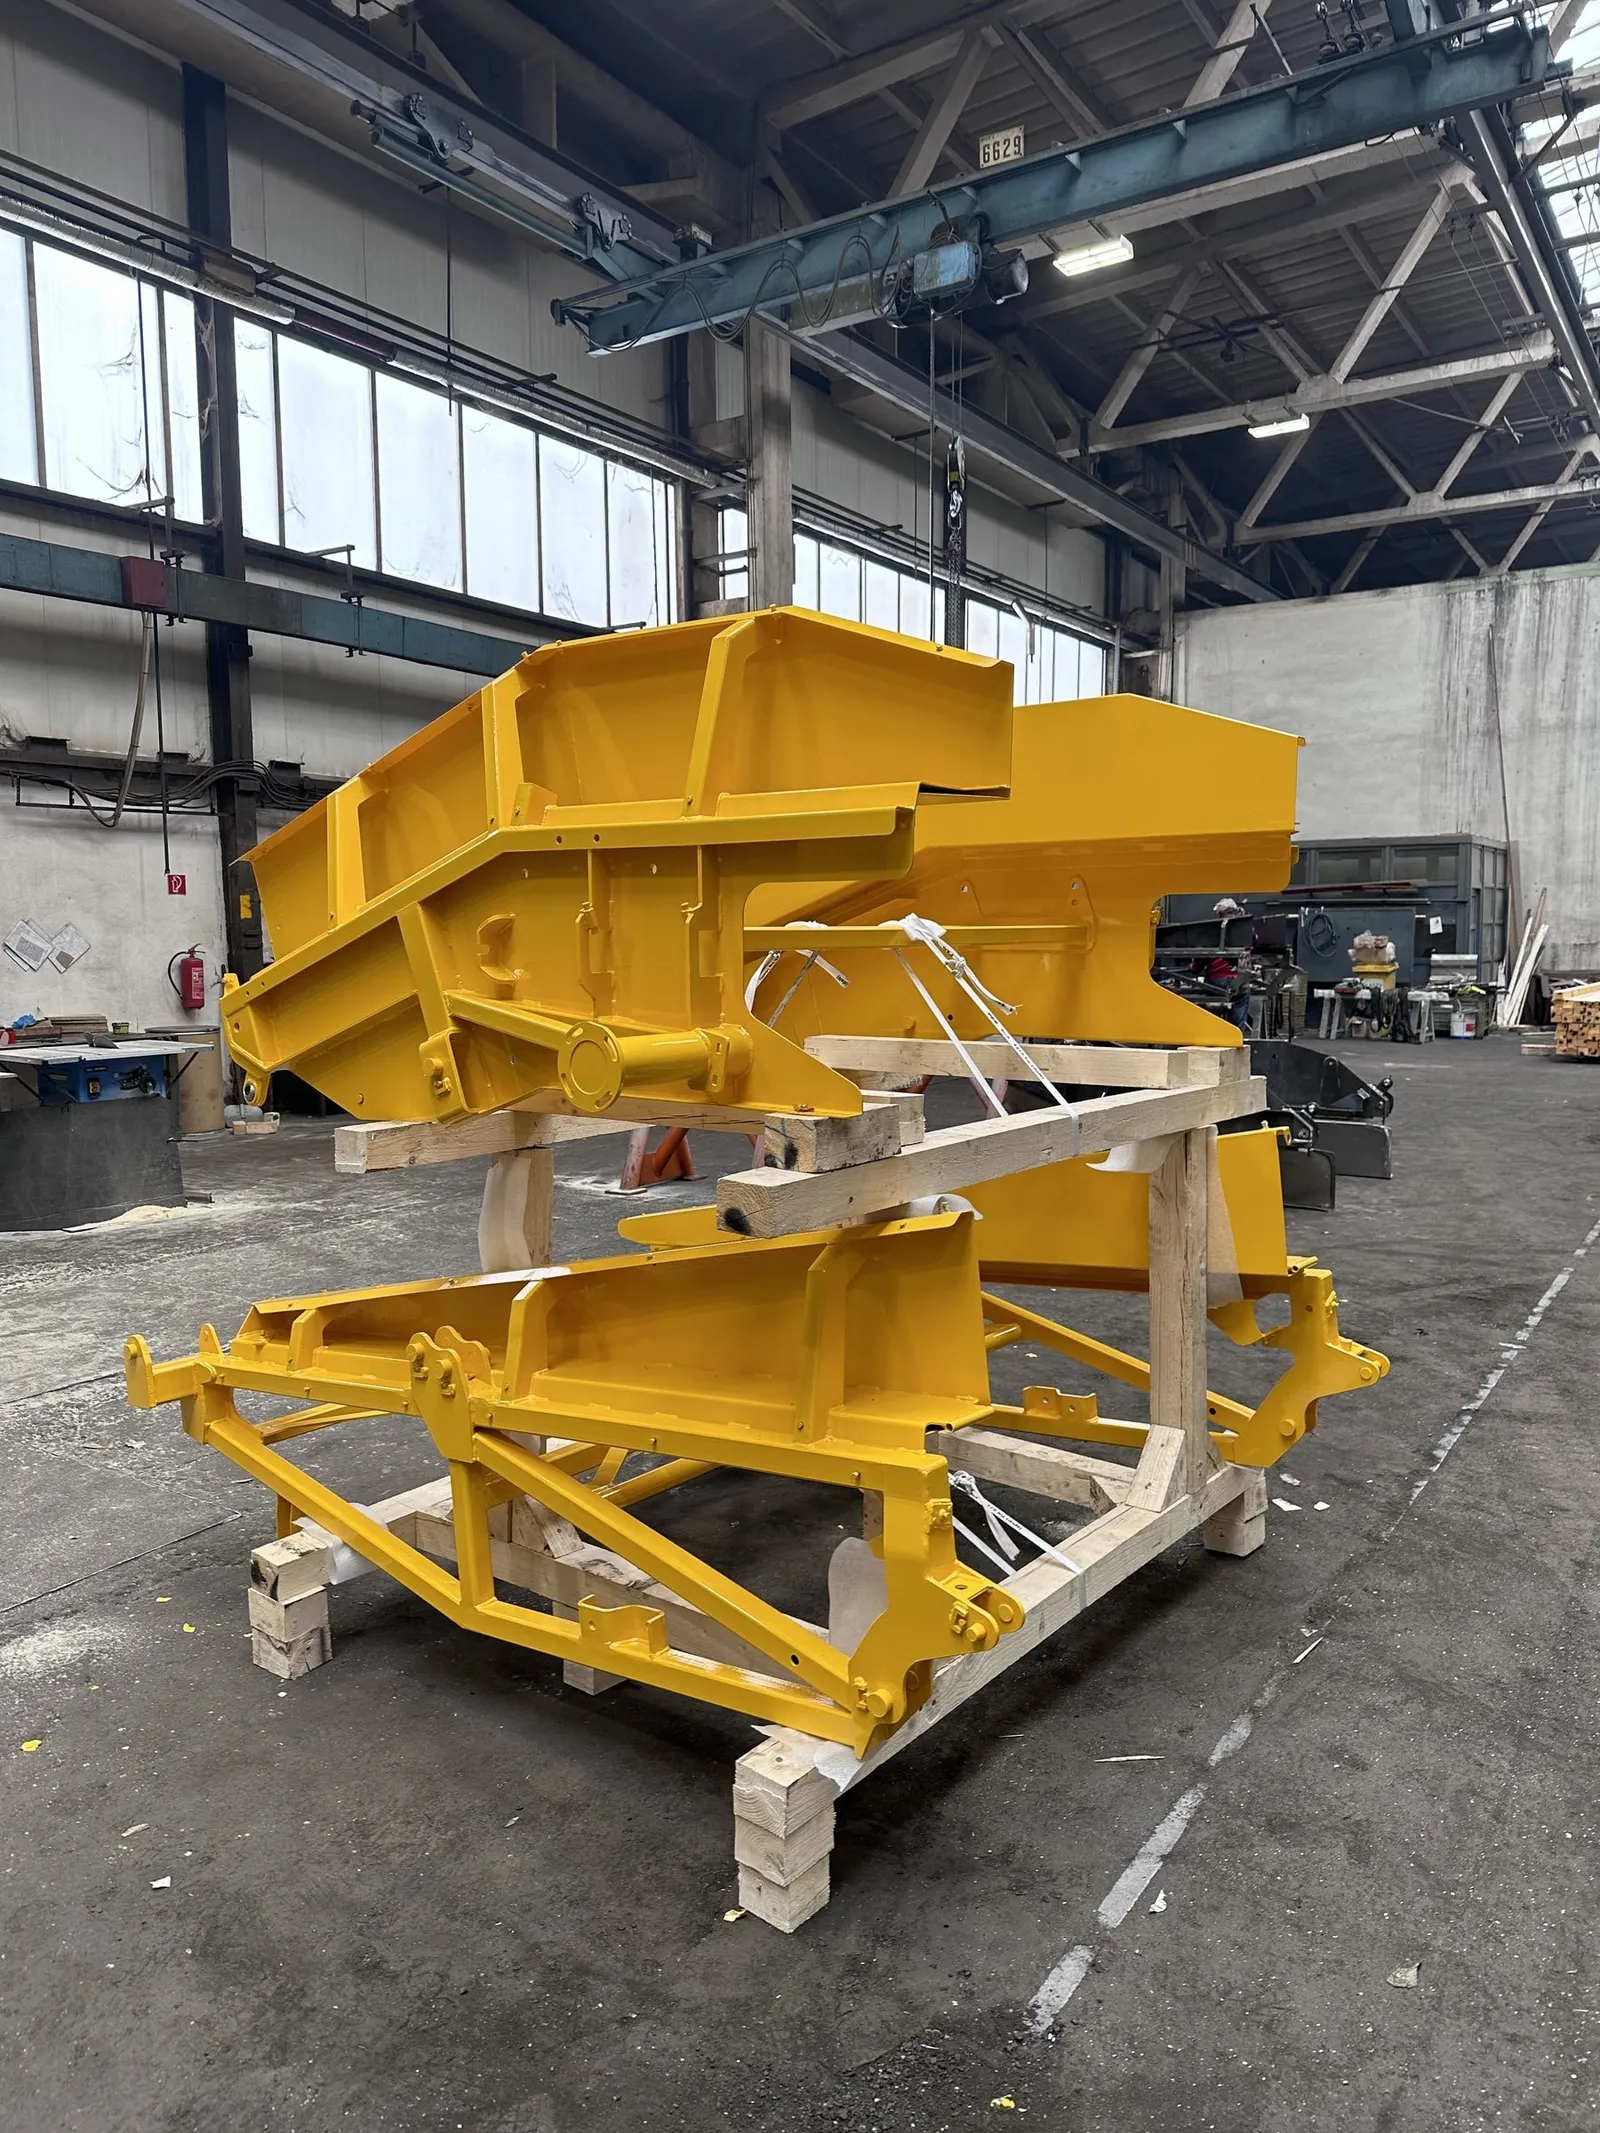
Yellow welded frame assembly on a stand 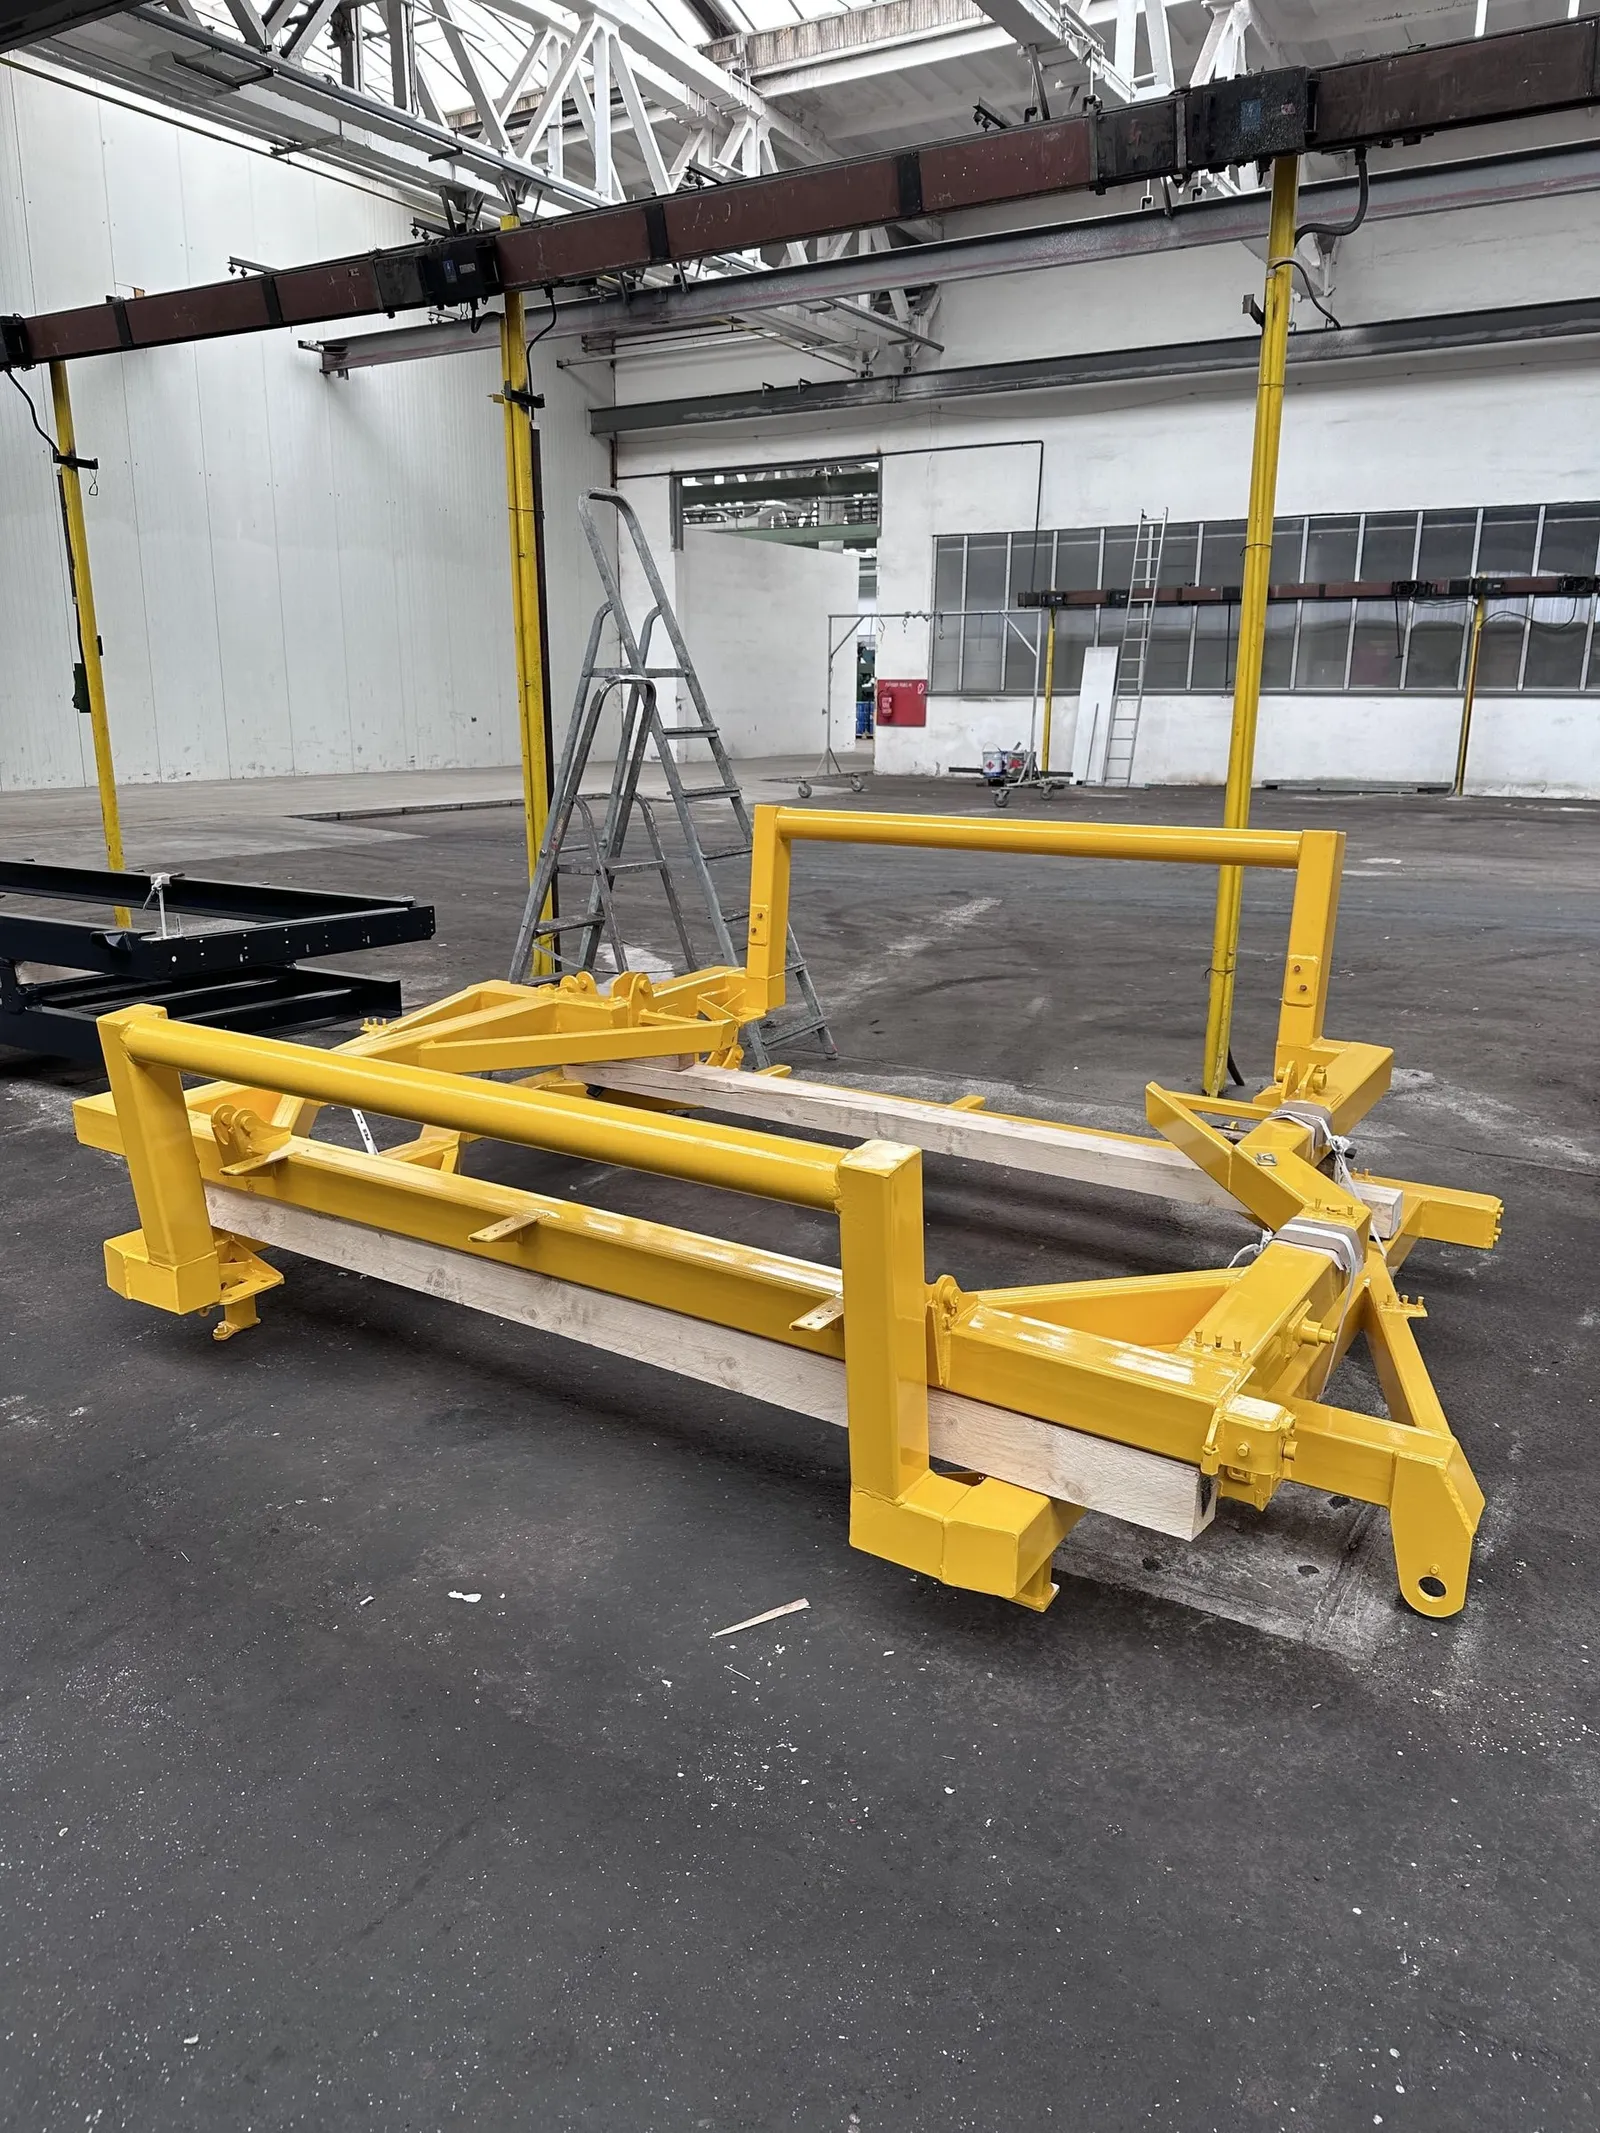
Yellow welded frame on the hall floor 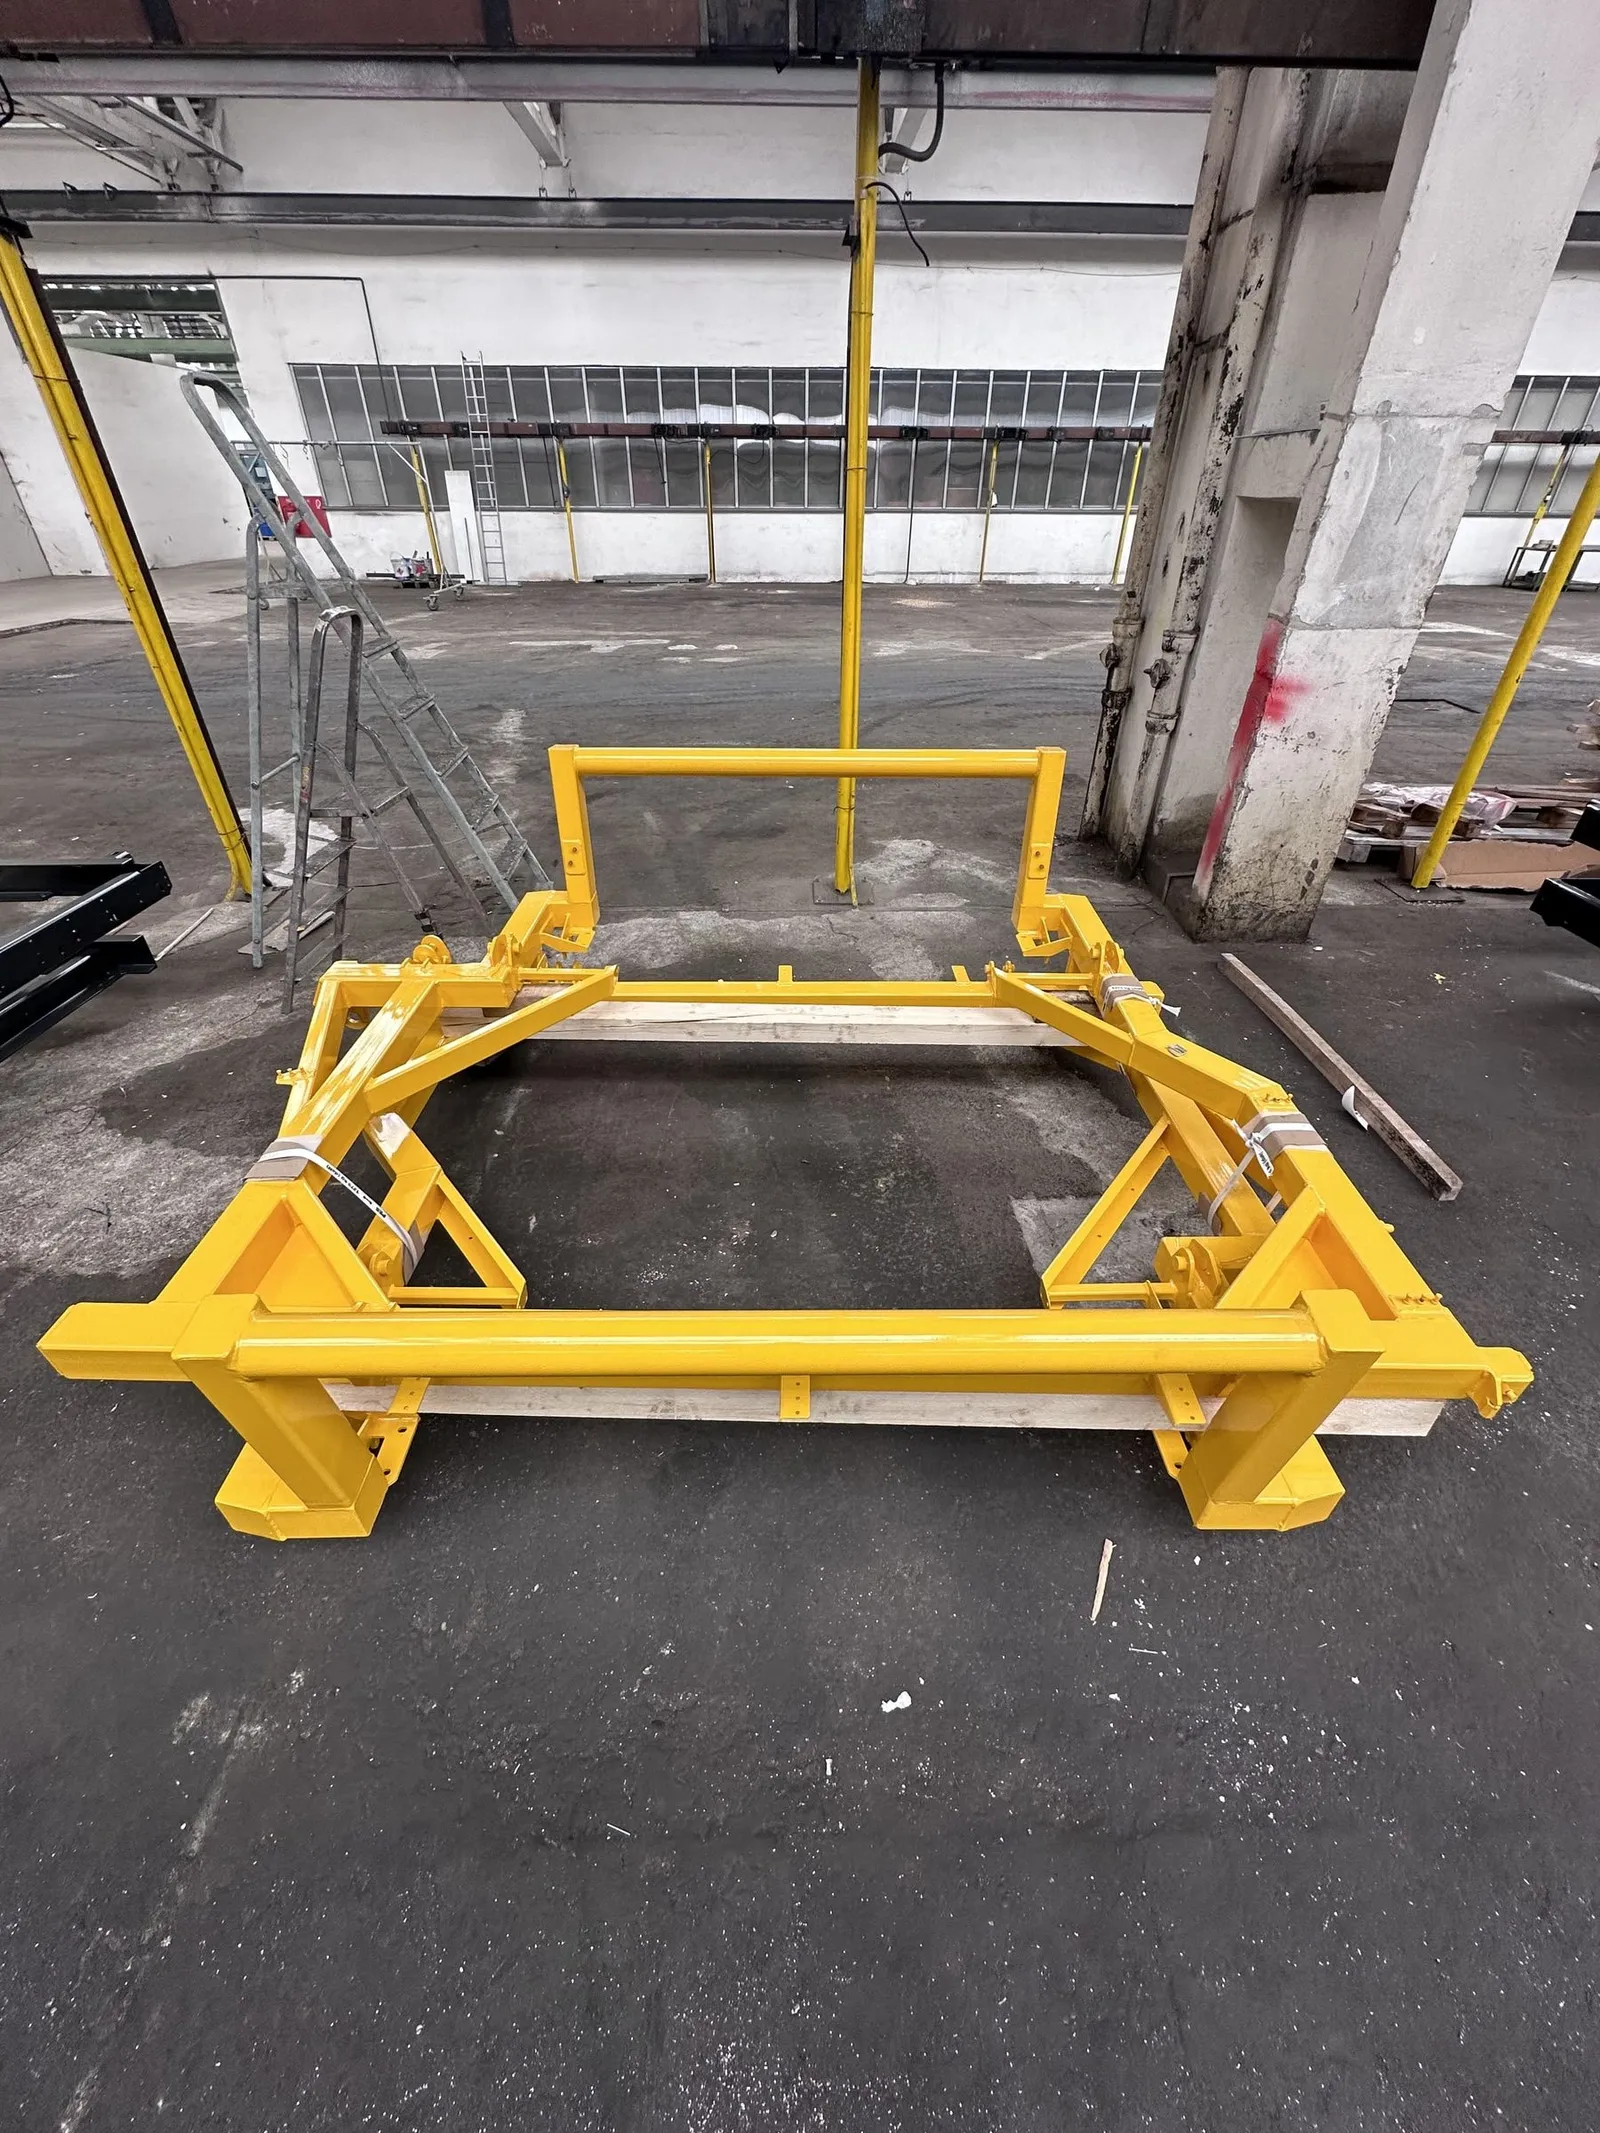
Yellow frame, top view 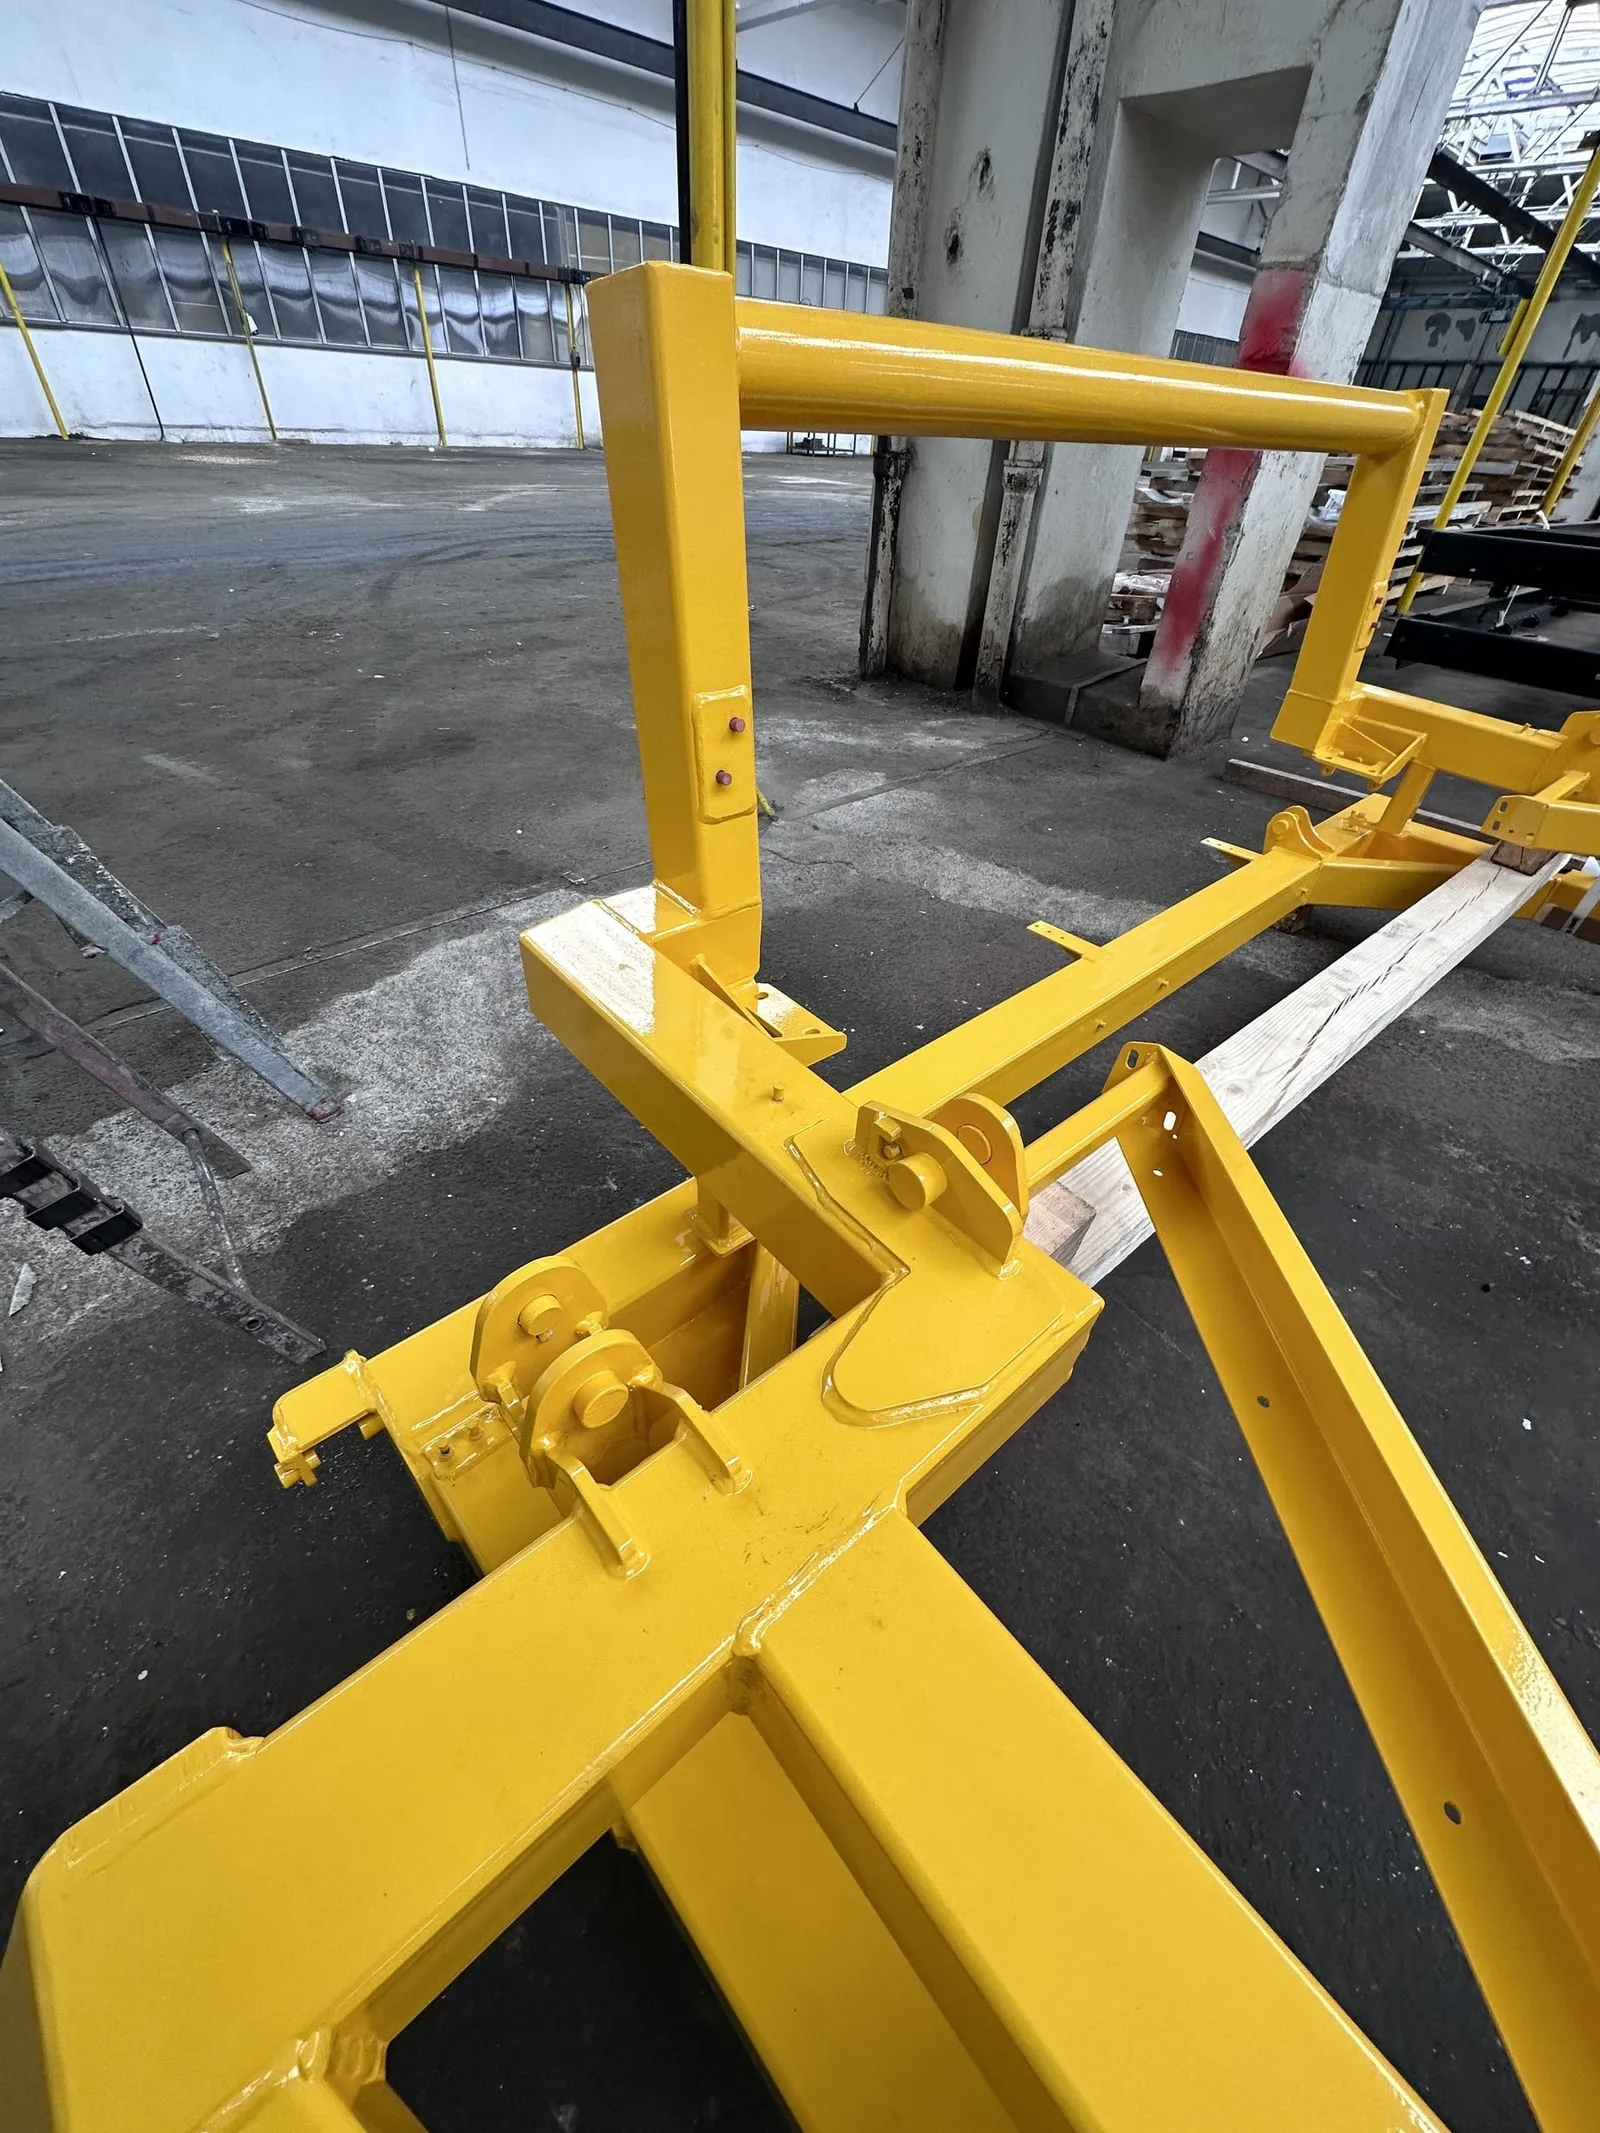
Yellow frame with mounting brackets, close-up 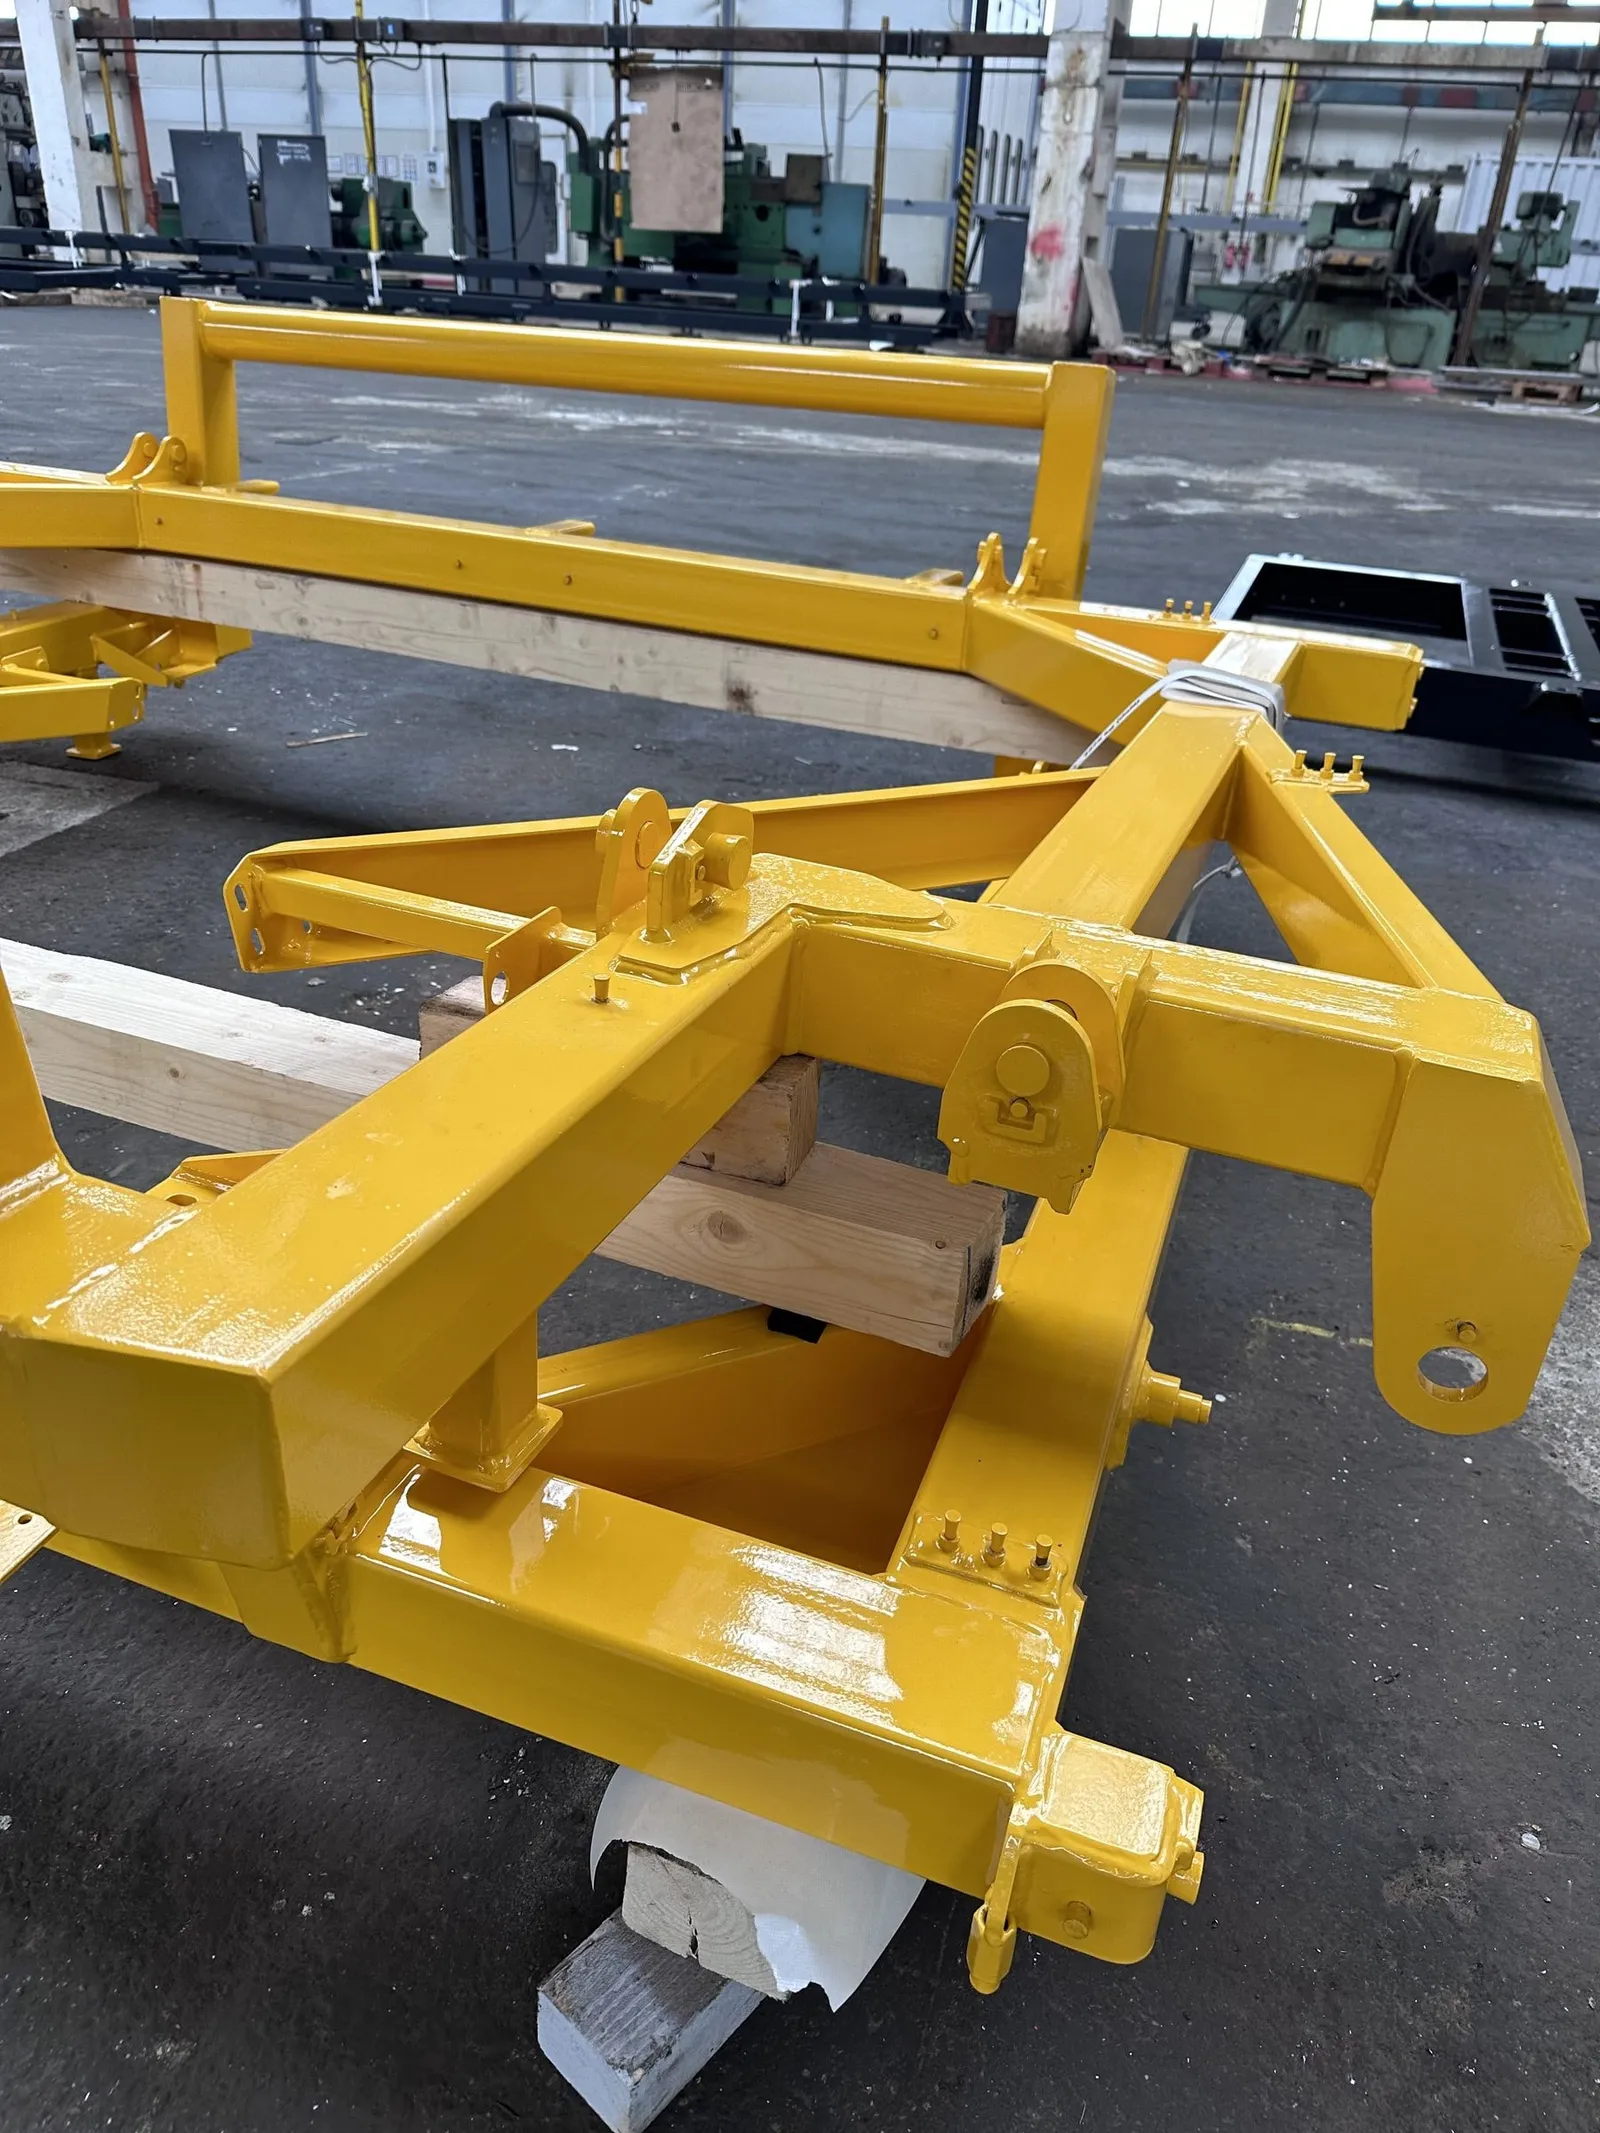
Yellow frame, second angle
Standards
What we build to and what we issue
- EN 1090-1, EXC2
- EN ISO 3834-2
- EN ISO 9606
- ISO 9001 / ISO 14001
- ISO 12944 / EN ISO 8501-1 / ISO 2808
- EN 10204 3.1
| Standard | What it covers |
|---|---|
| EN 1090-1, EXC2 | Execution of steel structures, CE marking |
| EN ISO 3834-2 | Comprehensive welding quality requirements |
| EN ISO 9606 | Welder qualification testing |
| ISO 9001 / ISO 14001 | Quality and environmental management |
| ISO 12944 / EN ISO 8501-1 / ISO 2808 | Coating durability, preparation, thickness |
| EN 10204 3.1 | Material certification on request |
Documentation issued
Material certificates, welding procedure specifications and welder qualifications, dimensional report including 3D measurement, coating specification and thickness report, CE declaration of performance for EXC2 structures, packing list and loading diagram.
Proof
Deployments with a number in them
- 01
Repeat frame agreements
With European machinery OEMs in crushing and screening, agricultural harvesting, and trailer and vehicle equipment: the work that has kept this hall running for decades.
- 02
A discharge belt conveyor
Quoted at serial and prototype prices, galvanised and assembled, with customer-supplied components fitted, for a Swiss carbon-capture technology company.
- 03
14 parts shortlisted
From two OEM product families for robotic welding, with the first four weldments going to fixture design: the working method, not a slogan.
Scope
What the price includes, and what it does not
Included
- Design for manufacture review
- Jig and fixture design and build
- Cutting, forming, welding, machining
- Blasting and coating
- Inspection and documentation
- Packing
Not included
- Raw material free-issue unless agreed
- Third-party notified-body certification where required
- Site erection unless quoted
- Transport
If we have not built exactly this before, we will say so and tell you what we have built that is closest. Two prototype programmes in this factory were delivered below cost because nobody said that early enough. We do not do that any more, to you or to us.
Lead times
By variant
| Variant | Lead time |
|---|---|
| Quotation from a complete pack | 5-10 working days |
| Prototype or first article | 8-12 weeks |
| Repeat batch on an established jig | 4-8 weeks |
| Serial, repeat frame agreement | to schedule |
Engagement
Four ways to buy
Buy a catalogue unit
Pick from 94 published SKUs with full specifications, get a price, get a delivery date.
Modify a catalogue unit
Start from a standard shell and change what needs changing. Fastest route to a non-standard requirement.
Build to your specification
You bring the specification or the drawings, we review them, we build. Prototype and serial priced separately.
Subcontract fabrication
You are the prime, we are the hall. EN 1090-1 EXC2 capacity with AQAP 2110 assurance behind it.
Process
Specification to delivery in five steps
- 01
Send the specification.
A drawing, a tender annex, or three sentences. Whichever you have.
- 02
Review, in writing.
We tell you what is missing or contradictory before anyone quotes. 3-5 working days.
- 03
Quotation.
Bottom-up: material at purchase cost, co-operation, direct hours at a fully absorbed rate. 2-3 weeks for a complex build.
- 04
Design freeze and build.
Changes after freeze are variations, priced and agreed.
- 05
Test, document, deliver.
Factory acceptance where specified, full document pack, delivery and installation where quoted.
FAQ
Questions procurement asks
Do you take EN 1090 EXC3 work?
EXC2 is certified. EXC3 is assessed case by case with the customer's designer.
How big can you machine?
6,200 × 3,000 × 1,600 mm on the large horizontal borer, up to 16 tonnes on the table.
Can you build our welding jigs?
Yes, that is a service in its own right, including jigs you then use in your own plant.
Do you galvanise?
Through a co-operating plant, hot-dip, coordinated by us as part of the job.
Will you do one prototype?
Yes, and we will price the serial run alongside it.
Do you certify welders?
Welders are qualified to EN ISO 9606 and the welding quality system is EN ISO 3834-2, audited.
Send us the specification. A drawing, a tender annex, or three sentences.
You will get a written review of it inside a week, whether or not you buy anything.
Where to go next
Related families
Related sectors